IN
₹
Apparel & Fashion
Description
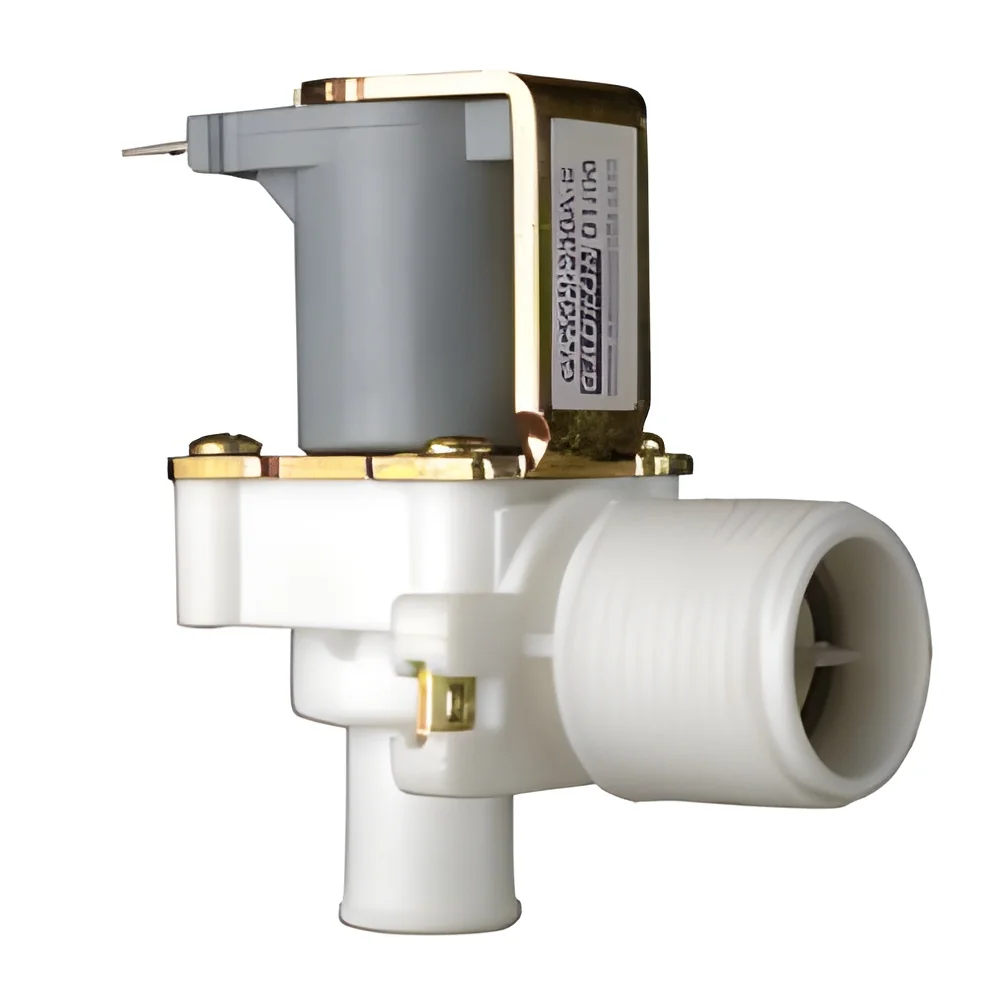
The Industrial Water Feed Valve GV 506 represents high-performance engineering for precise water flow management in demanding industrial settings. Manufactured from premium materials using advanced technology, this valve guarantees durability, leak-proof operation, and consistent performance under varying pressure conditions. Designed to meet international quality standards, it ensures compatibility with global industrial systems while offering easy installation, minimal maintenance requirements, and extended service life. Each unit undergoes rigorous testing to deliver flawless operation and customer satisfaction, making it a reliable solution for businesses seeking efficient water management without compromise.

This valve finds extensive application across multiple industrial sectors, including manufacturing, water treatment, HVAC, agriculture, and energy production. Manufacturing plants utilize it for regulating coolant and process water flow in production equipment. Water treatmen...
The Industrial Water Feed Valve GV 506 represents high-performance engineering for precise water flow management in demanding industrial settings. Manufactured from premium materials using advanced technology, this valve guarantees durability, leak-proof operation, and consistent performance under varying pressure conditions. Designed to meet international quality standards, it ensures compatibility with global industrial systems while offering easy installation, minimal maintenance requirements, and extended service life. Each unit undergoes rigorous testing to deliver flawless operation and customer satisfaction, making it a reliable solution for businesses seeking efficient water management without compromise.

This valve finds extensive application across multiple industrial sectors, including manufacturing, water treatment, HVAC, agriculture, and energy production. Manufacturing plants utilize it for regulating coolant and process water flow in production equipment. Water treatment facilities depend on its precision for filtration and distribution control, while HVAC systems integrate it into cooling towers and heating circuits. Agricultural operations implement the valve in automated irrigation setups, and energy plants rely on it for critical water feed in boiler systems where accuracy ensures safety and efficiency. Its versatility makes it preferred by OEMs, system integrators, and maintenance teams worldwide.

Businesses select the Water Feed Valve GV 506 for its proven reliability that reduces downtime and maintenance costs significantly. The robust design ensures suitability for high-pressure and corrosive environments, delivering long service life and consistent performance. By minimizing water wastage and improving flow control accuracy, this valve contributes directly to operational efficiency and sustainability objectives. Comprehensive quality assurance and testing protocols provide complete peace of mind, establishing it as a trusted component for serious buyers focused on long-term value, performance reliability, and system integration excellence.

Key Features:
- High-grade construction materials ensure exceptional durability and corrosion resistance
- Advanced manufacturing technology guarantees precision engineering and reliable operation
- Simplified installation design reduces setup time and integration complexity
- Rigorous testing protocols validate performance against international quality standards
- Robust sealing mechanism prevents leaks even under extreme pressure conditions

Benefits:
- Extended service life reduces replacement frequency and long-term costs
- Consistent performance minimizes system downtime and maintenance requirements
- Enhanced flow control accuracy improves process efficiency and resource utilization
- Corrosion-resistant construction ensures reliability in harsh industrial environments
- Quality-assured design provides operational safety and peace of mind
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
The GV 506 Water Feed Valve provides precise water flow regulation in demanding industrial environments. Its robust construction withstands high-pressure conditions, ensuring reliable performance in cooling systems, automated water networks, and processes where consistent flow and leak prevention are essential for operational continuity and safety.
This valve serves diverse sectors requiring dependable fluid control, including manufacturing plants, HVAC installations, water treatment facilities, and agricultural irrigation systems. Its adaptable design allows straightforward integration with existing pipelines and machinery, supporting both manual and automated operations to enhance efficiency and system reliability across various industrial setups.
- Regulating water supply in industrial boilers and steam generation systems
- Controlling coolant flow in machining equipment and manufacturing processes
- Managing water distribution in HVAC cooling towers and heating systems
- Automating water feed in agricultural irrigation and landscaping projects
- Ensuring precise flow control in water filtration and purification plants
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile

Gadson Electronics, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
South Asia
Industrial Water Feed Valve GV 506 High Pressure Durable Control
Industrial Water Feed Valve GV 506 delivers high-pressure durable water flow control for industrial systems. Premium construction ensures reliability, low maintenance, and seamless integration across various applications.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Gadson Electronics
 Maharashtra, India
Industrial Equipment & MachineryManufacturer