IN
₹
Apparel & Fashion
Description
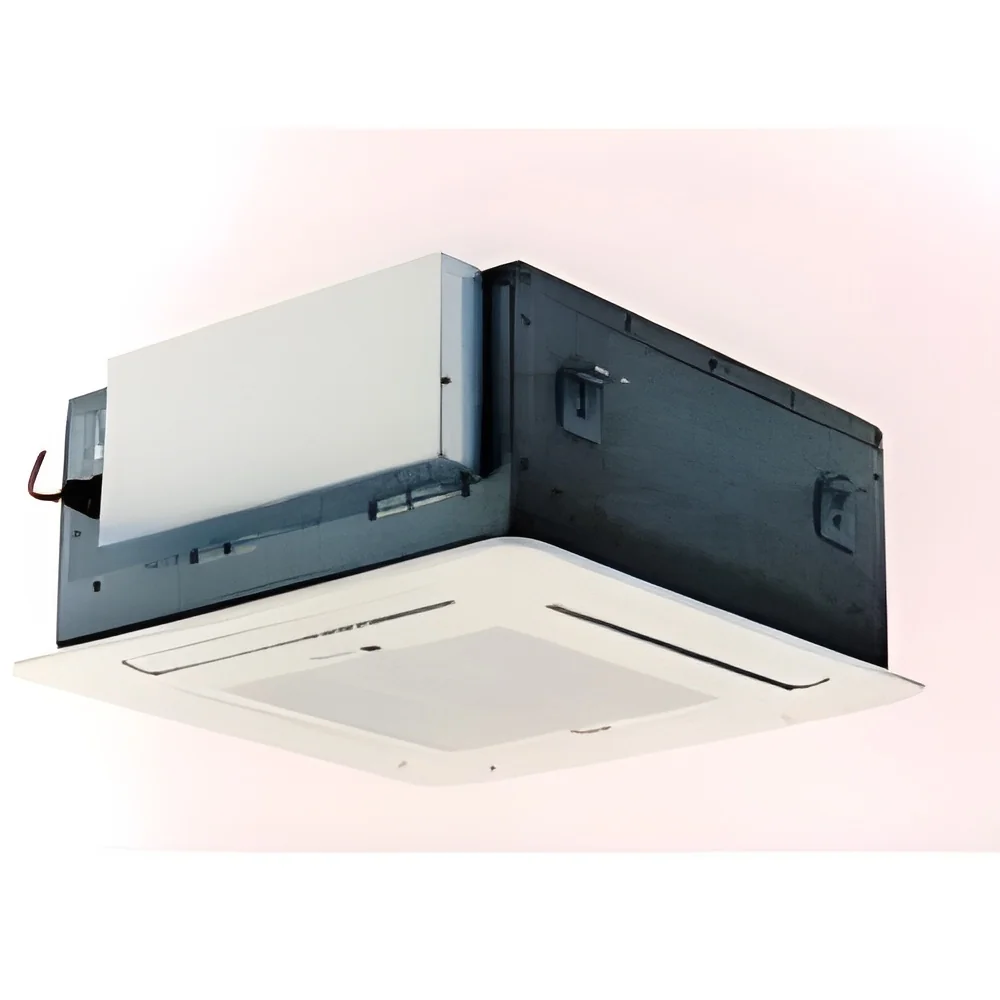
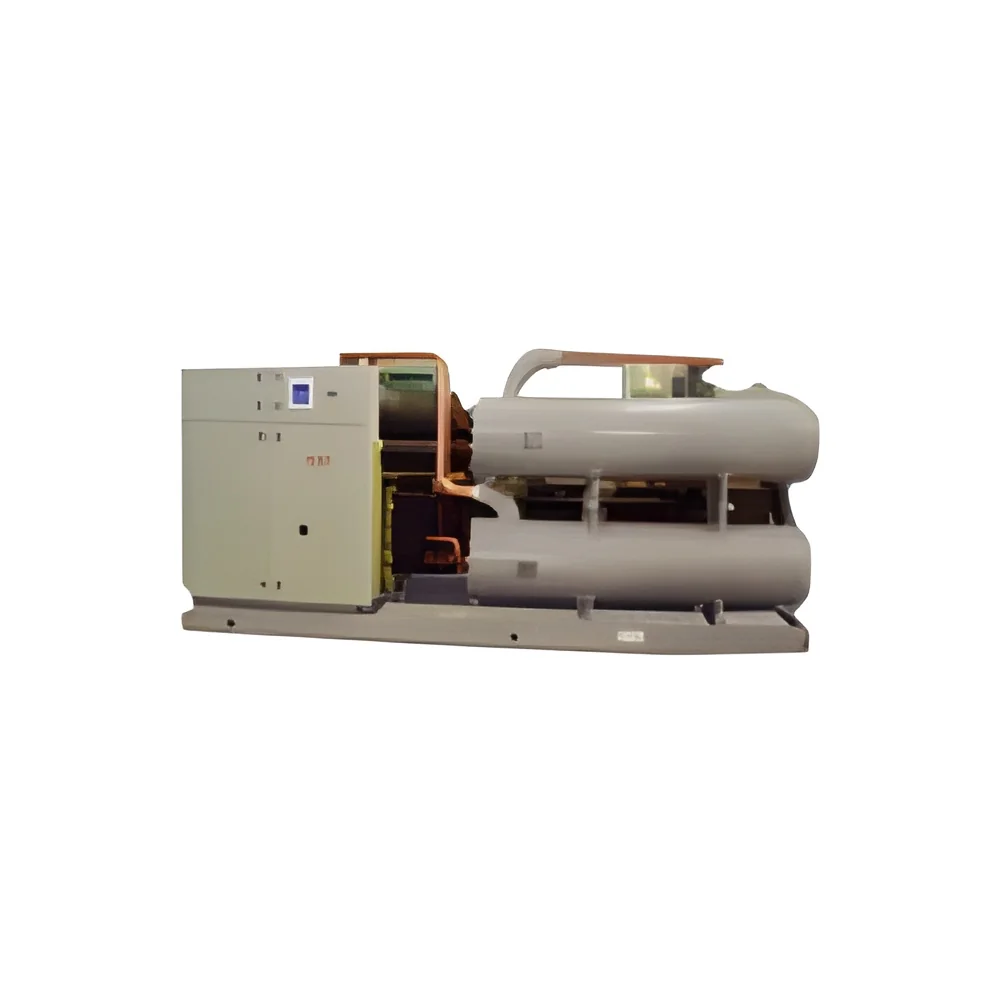
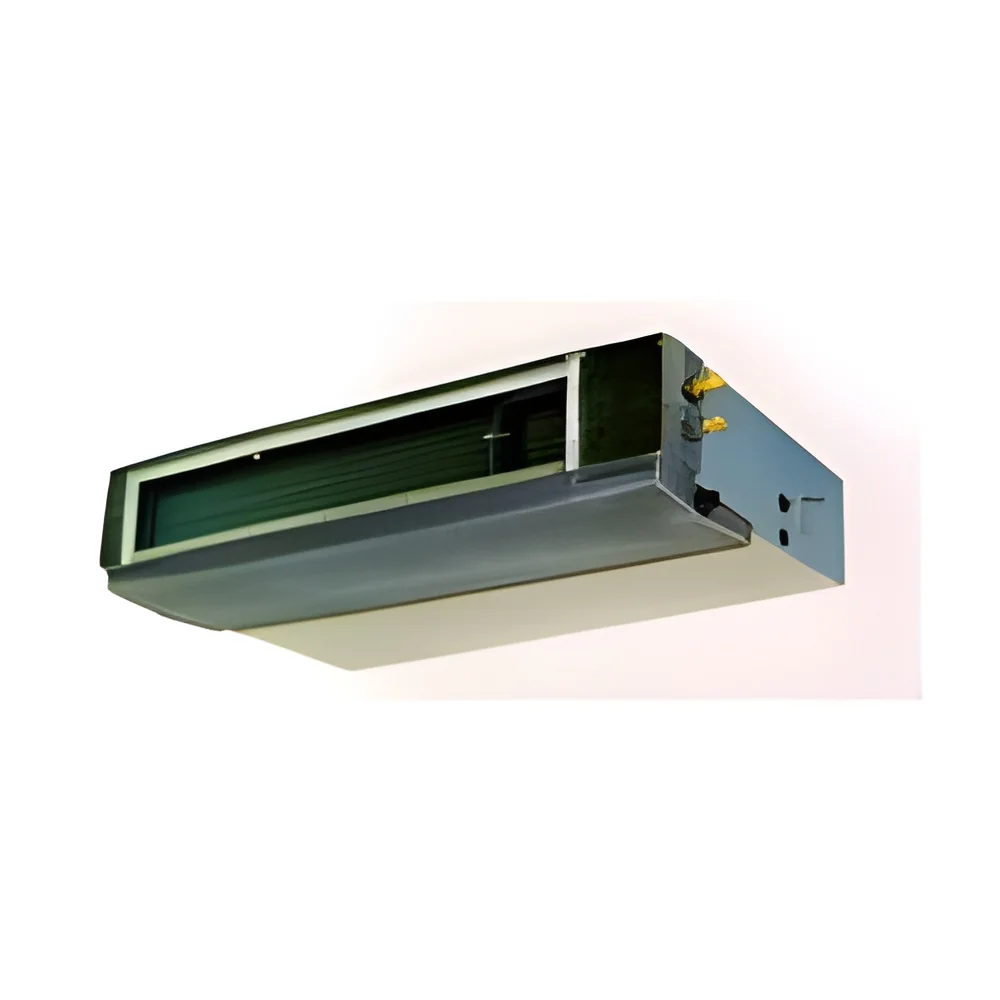
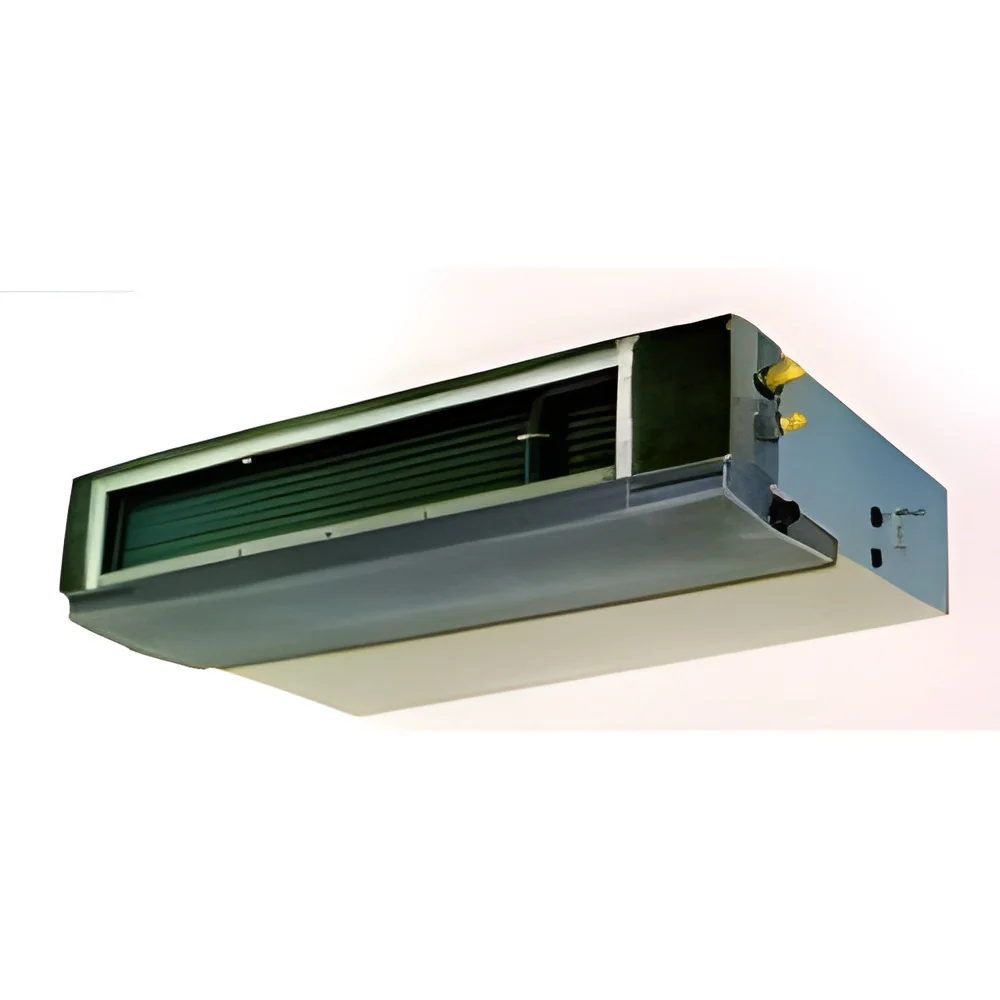
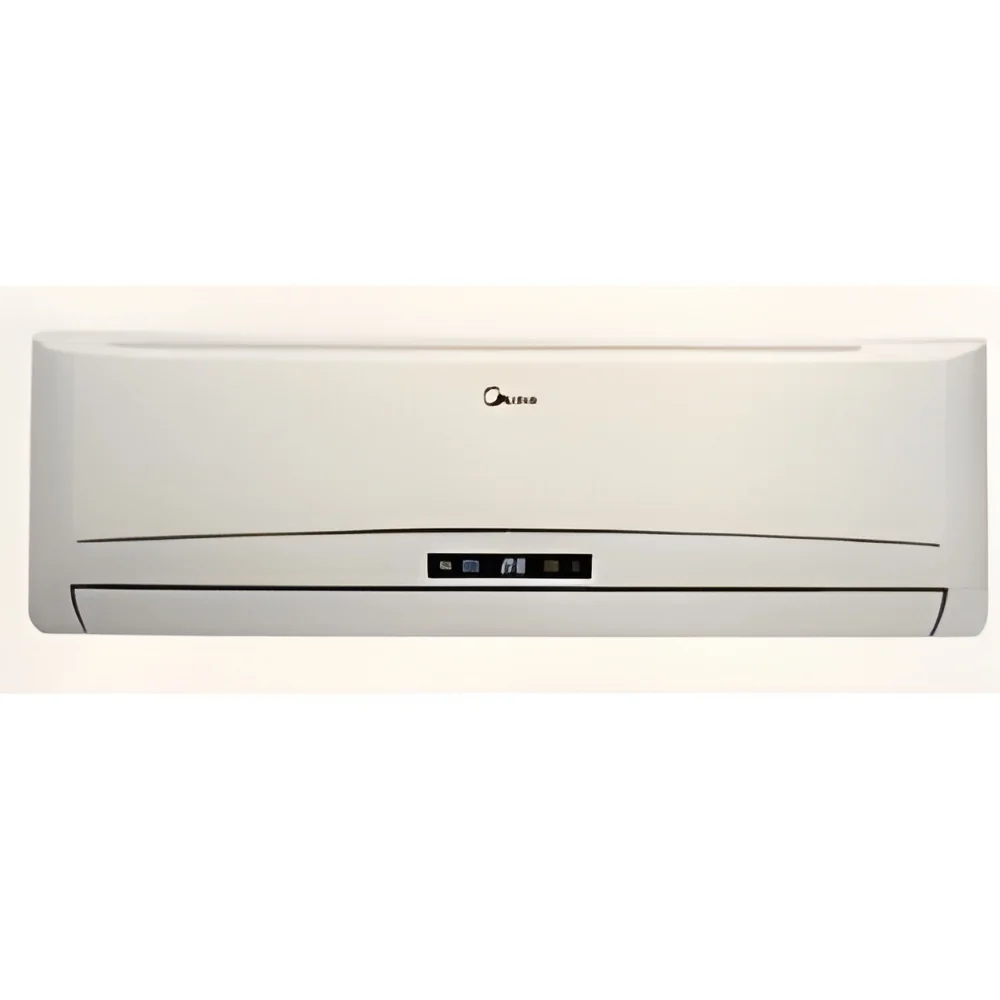
Our industrial wall mounted coolers feature advanced copper tube and aluminum fin construction designed specifically for high capacity cooling applications. These units are engineered to handle chilled water, glycols, and inorganic brines with exceptional efficiency and reliability. The robust design ensures optimal thermal performance in demanding industrial environments where consistent temperature control is critical. Built for longevity and minimal maintenance, these coolers provide dependable operation in various cooling scenarios, making them an ideal choice for facilities requiring precise climate management.

These cooling systems serve multiple industries including food processing, pharmaceuticals, agriculture, and manufacturing. They are particularly effective in cold storage applications where perishable goods such as dairy products, fruits, vegetables, meats, and seafood require precise temperature maintenance. The units also support industrial process cooling needs in manu...
Our industrial wall mounted coolers feature advanced copper tube and aluminum fin construction designed specifically for high capacity cooling applications. These units are engineered to handle chilled water, glycols, and inorganic brines with exceptional efficiency and reliability. The robust design ensures optimal thermal performance in demanding industrial environments where consistent temperature control is critical. Built for longevity and minimal maintenance, these coolers provide dependable operation in various cooling scenarios, making them an ideal choice for facilities requiring precise climate management.

These cooling systems serve multiple industries including food processing, pharmaceuticals, agriculture, and manufacturing. They are particularly effective in cold storage applications where perishable goods such as dairy products, fruits, vegetables, meats, and seafood require precise temperature maintenance. The units also support industrial process cooling needs in manufacturing facilities and provide climate control in storage warehouses. Their versatile design allows integration into various operational setups, ensuring reliable performance across different industrial applications and environmental conditions.

The business value of these coolers lies in their exceptional reliability, energy efficiency, and long-term cost-effectiveness. Their durable construction minimizes maintenance requirements and reduces operational downtime, providing significant savings over the product lifecycle. The efficient heat transfer capabilities ensure optimal cooling performance while keeping energy consumption low. These features combine to deliver strong return on investment for businesses, making them a trusted solution for importers, distributors, and wholesalers seeking high-performance cooling equipment.

Key Features:
- Copper tube and aluminum fin construction for superior heat transfer efficiency
- High capacity design suitable for large-scale industrial cooling requirements
- Compatible with chilled water, glycols, and inorganic brine solutions
- Wall mounted installation for space-efficient operation
- Robust construction ensuring long-term durability and reliability

Benefits:
- Enhanced cooling efficiency through optimized heat transfer technology
- Reduced energy consumption leading to lower operational costs
- Minimal maintenance requirements and extended service life
- Reliable performance in demanding industrial environments
- Flexible installation options to accommodate various facility layouts
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
These high capacity wall mounted coolers are engineered for demanding industrial environments where precise temperature control is essential. They efficiently handle chilled water, glycols, and inorganic brines, providing versatile cooling solutions for various operational requirements. The robust construction ensures consistent performance in challenging conditions, making them suitable for facilities that demand reliable temperature management around the clock.
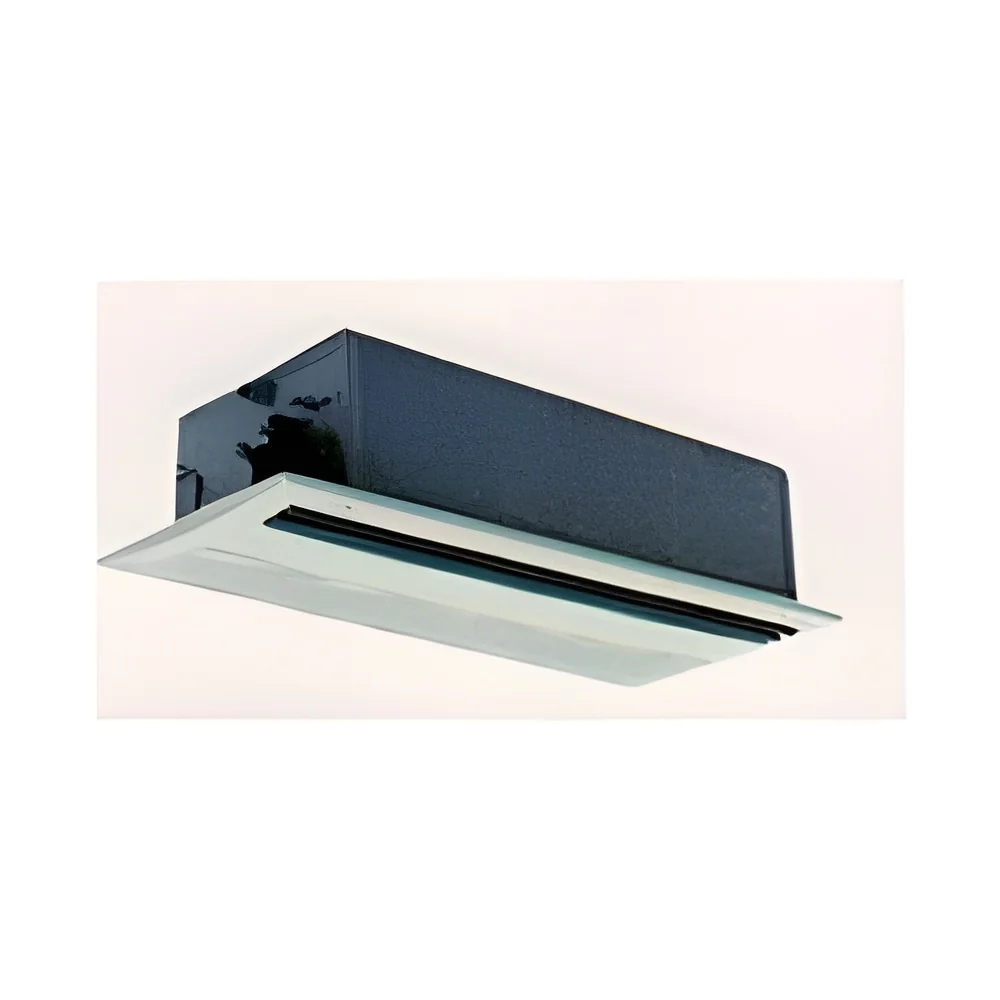
Designed for multiple industrial sectors, these cooling units offer flexible installation options including wall and ceiling mounting to accommodate space constraints. Their high capacity performance supports critical cooling needs in food processing plants, cold storage facilities, and manufacturing operations. The durable copper tube and aluminum fin construction guarantees long-term reliability while maintaining efficient heat transfer capabilities for optimal cooling performance.
- Cold storage preservation for dairy products, meats, and seafood in food processing facilities
- Temperature-controlled storage for fruits and vegetables in agricultural supply chains
- Climate control in pharmaceutical storage warehouses ensuring product integrity
- Industrial process cooling in manufacturing units using glycol or brine solutions
- Commercial kitchen cooling systems for restaurants and food service establishments
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Chill Tech Engineers Private Limited, Tamil Nadu
 Tamil Nadu, India
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Wall Mounted Coolers Copper Tube Aluminum Fin High Capacity
Industrial wall mounted coolers with copper tube aluminum fin construction deliver high capacity cooling for chilled water, glycols, and inorganic brines. Ideal for cold storage, food processing, and industrial cooling applications requiring reliable performance.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Chill Tech Engineers Private Limited
 Tamil Nadu, India