IN
₹
Apparel & Fashion
Description
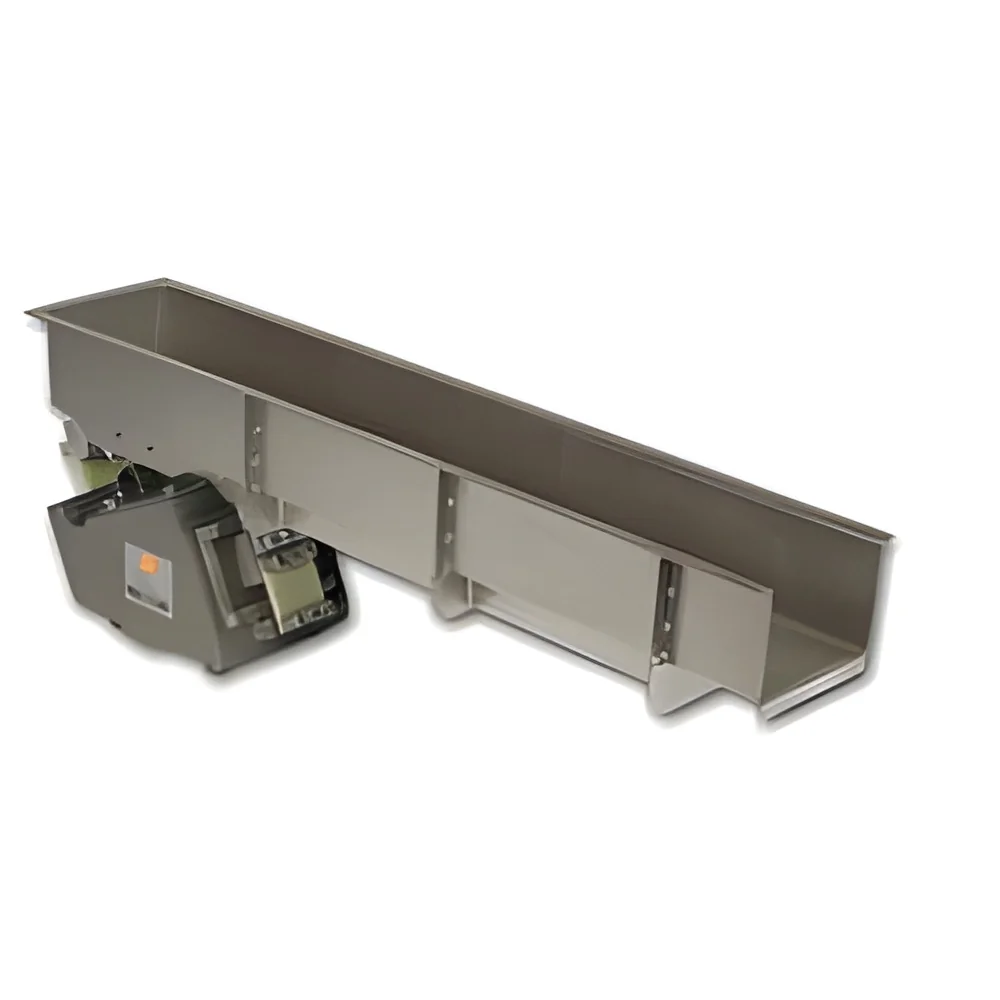
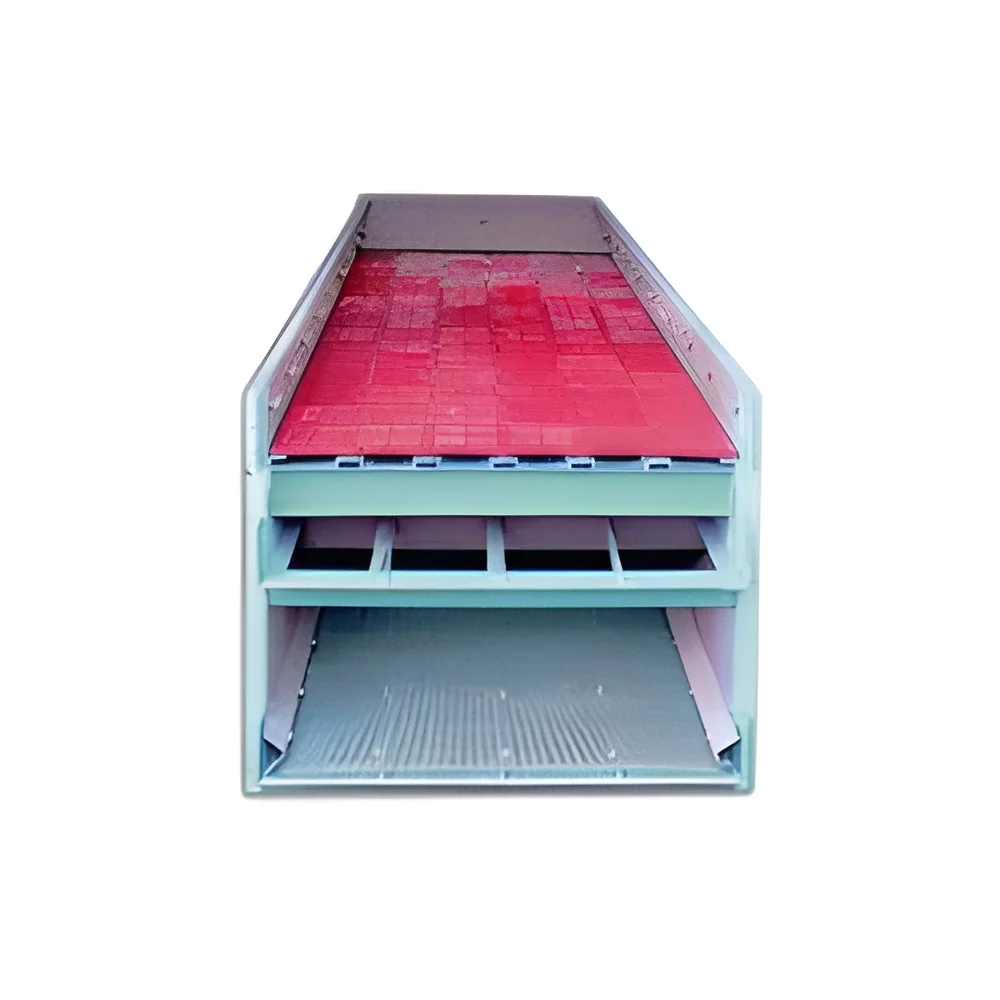
Heavy-duty circular motion vibrating screens represent advanced engineering for efficient material separation in industrial applications. Designed specifically for demanding processing environments, these screens incorporate robust components including reinforced frames, high-torque electric motors, precision couplers, durable screen webs, eccentric block mechanisms, and industrial-grade rubber springs. The circular motion design ensures optimal material movement across the screening surface, providing consistent separation performance while maintaining structural integrity throughout extended operational periods. These screens are built to handle various material types with reliability and precision, making them suitable for continuous heavy-duty use in challenging industrial conditions.

These vibrating screens serve critical functions across multiple industrial sectors including mining operations, quarrying facilities, construction materials processing, recycling plants, and chemica...
Heavy-duty circular motion vibrating screens represent advanced engineering for efficient material separation in industrial applications. Designed specifically for demanding processing environments, these screens incorporate robust components including reinforced frames, high-torque electric motors, precision couplers, durable screen webs, eccentric block mechanisms, and industrial-grade rubber springs. The circular motion design ensures optimal material movement across the screening surface, providing consistent separation performance while maintaining structural integrity throughout extended operational periods. These screens are built to handle various material types with reliability and precision, making them suitable for continuous heavy-duty use in challenging industrial conditions.

These vibrating screens serve critical functions across multiple industrial sectors including mining operations, quarrying facilities, construction materials processing, recycling plants, and chemical processing facilities. In mining applications, they efficiently separate ores and minerals by particle size, ensuring proper material classification. Aggregate processing plants utilize them for grading crushed stone, sand, and gravel materials to meet specific size requirements. Recycling facilities depend on these screens for sorting waste streams and recovering valuable materials, while chemical processing plants employ them for separating powdered compounds with accuracy and consistency in various production processes.

The business value of these heavy-duty vibrating screens lies in their exceptional operational reliability, reduced maintenance requirements, and consistent performance efficiency. Engineered for continuous heavy-duty operation, they minimize production downtime through robust construction and quality component selection. The energy-efficient design reduces operational costs while maintaining high throughput capacity, contributing to improved processing economics. The low noise operation and minimal vibration transmission enhance working conditions and reduce structural stress on supporting facilities, providing long-term operational benefits and cost savings for industrial operations.

Key Features:
- Reinforced main frame construction for enhanced durability and operational stability
- High-torque electric motor delivering consistent power output for reliable performance
- Precision engineered eccentric block mechanism ensuring optimal vibration patterns
- Industrial-grade rubber springs reducing noise levels and vibration transmission
- Durable screen web configurations suitable for various material types and sizes

Benefits:
- Continuous reliable operation in demanding industrial environments with minimal downtime
- Efficient material separation and classification improving processing quality
- Reduced maintenance requirements and extended operational service life
- Energy-efficient design lowering operational costs and power consumption
- Enhanced working conditions through low noise operation and vibration control
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our heavy-duty circular motion vibrating screens deliver precise material separation across demanding industrial operations. Engineered with robust components including rubber springs and eccentric blocks, these screens maintain consistent performance while handling various material types and processing requirements. The circular motion design ensures efficient sorting and classification through precise vibration patterns, making them ideal for continuous operation in challenging environments where reliability is critical.
These industrial-grade vibrating screens serve multiple sectors requiring efficient particle size separation and material classification. Their durable construction withstands heavy loads and continuous operation while maintaining separation accuracy. The reliable performance reduces operational interruptions and maintenance needs, providing consistent output quality across different material types and processing conditions in various industrial settings.
- Mining operations for separating ores and minerals by particle size
- Aggregate processing plants for grading crushed stone and sand materials
- Recycling facilities for sorting waste materials and recovered commodities
- Chemical processing plants for separating powdered compounds and materials
- Construction material facilities for sorting and grading raw materials
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Able Industrial Equip Makers, Tamil Nadu
 Tamil Nadu, India
Manufacturer•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Heavy Duty Circular Motion Vibrating Screens For Material Separation
Heavy-duty circular motion vibrating screens for efficient material separation in mining and aggregate industries. Built with robust rubber springs and eccentric blocks for reliable continuous operation in demanding industrial processing environments.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Able Industrial Equip Makers
 Tamil Nadu, India
Manufacturer