IN
₹
Apparel & Fashion
Description
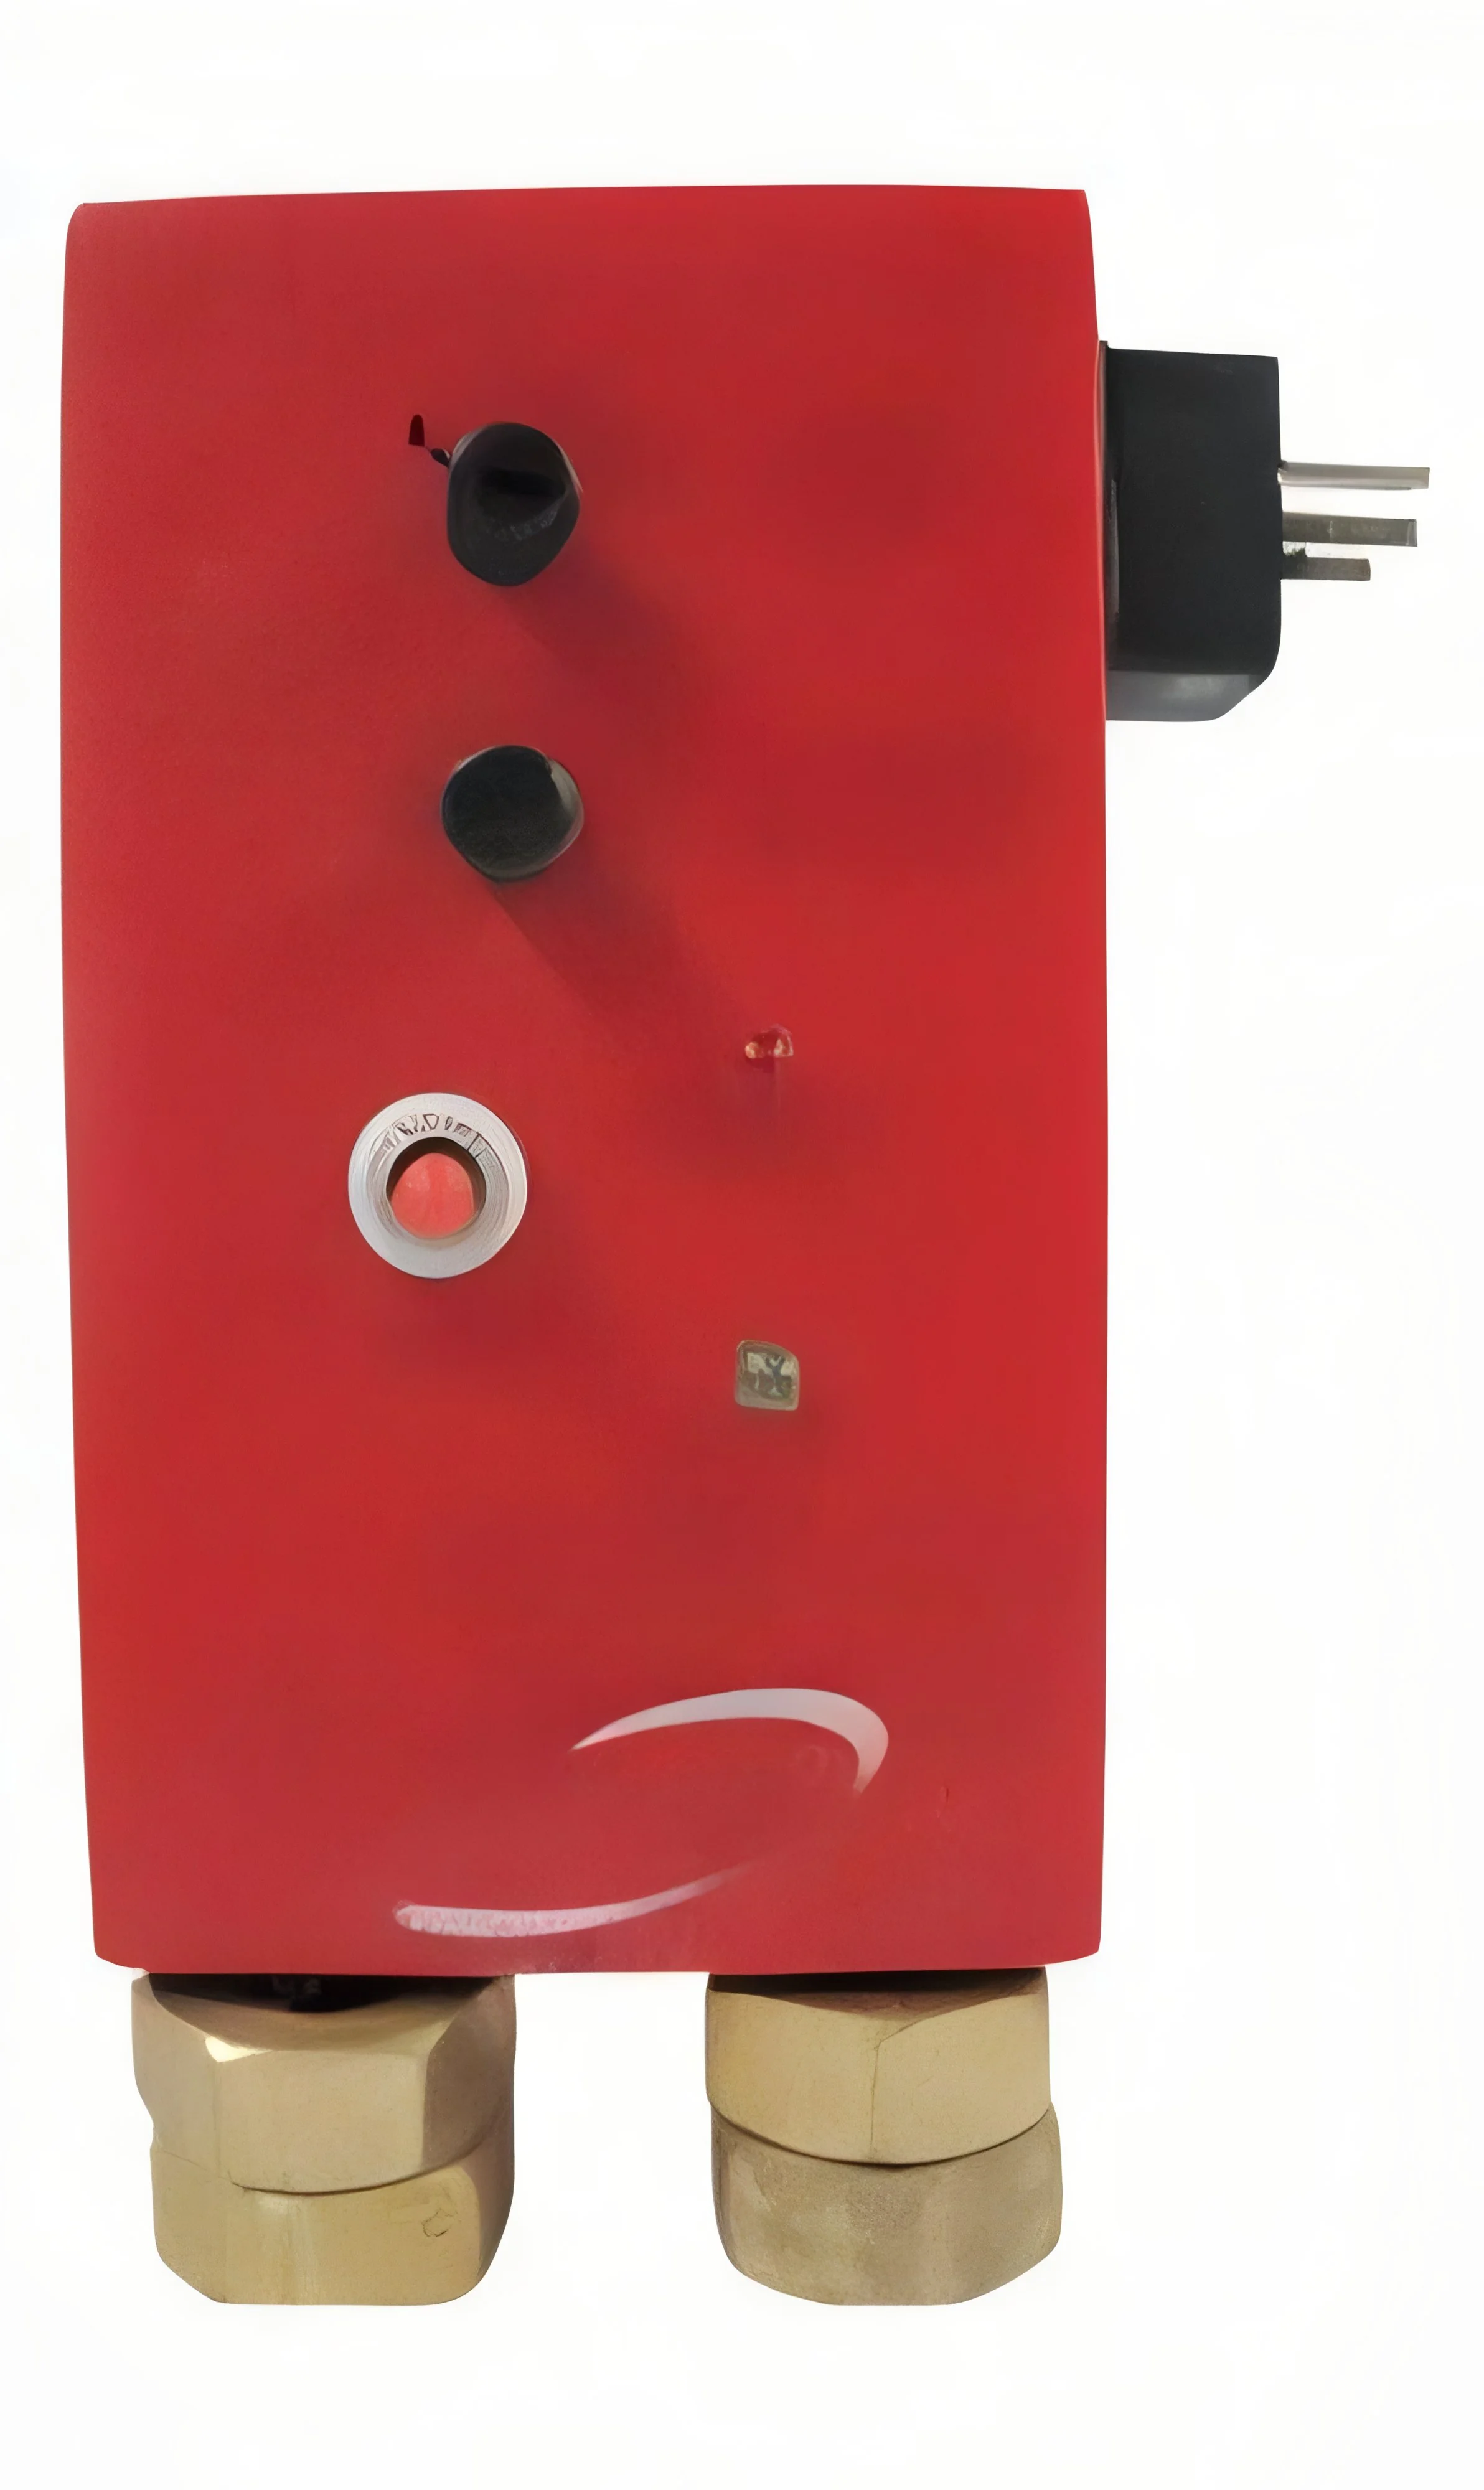
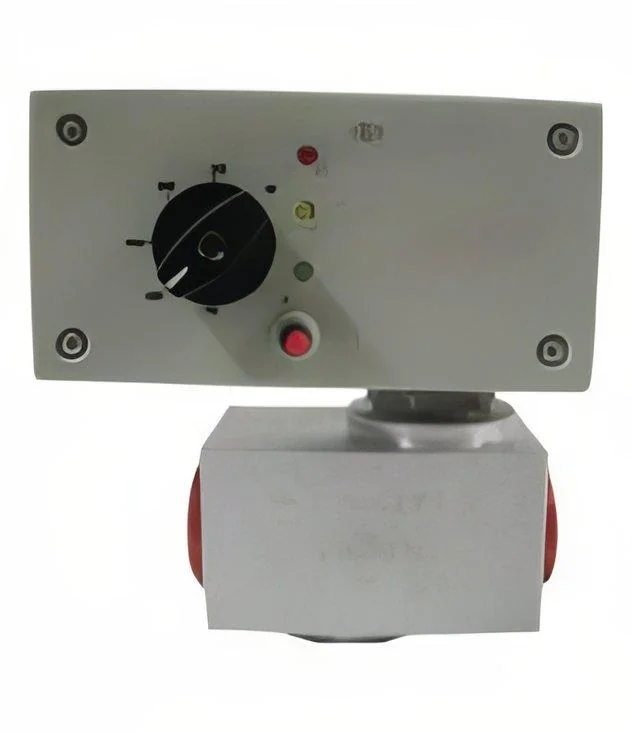
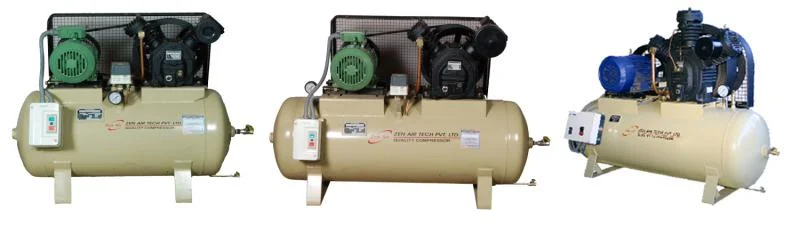
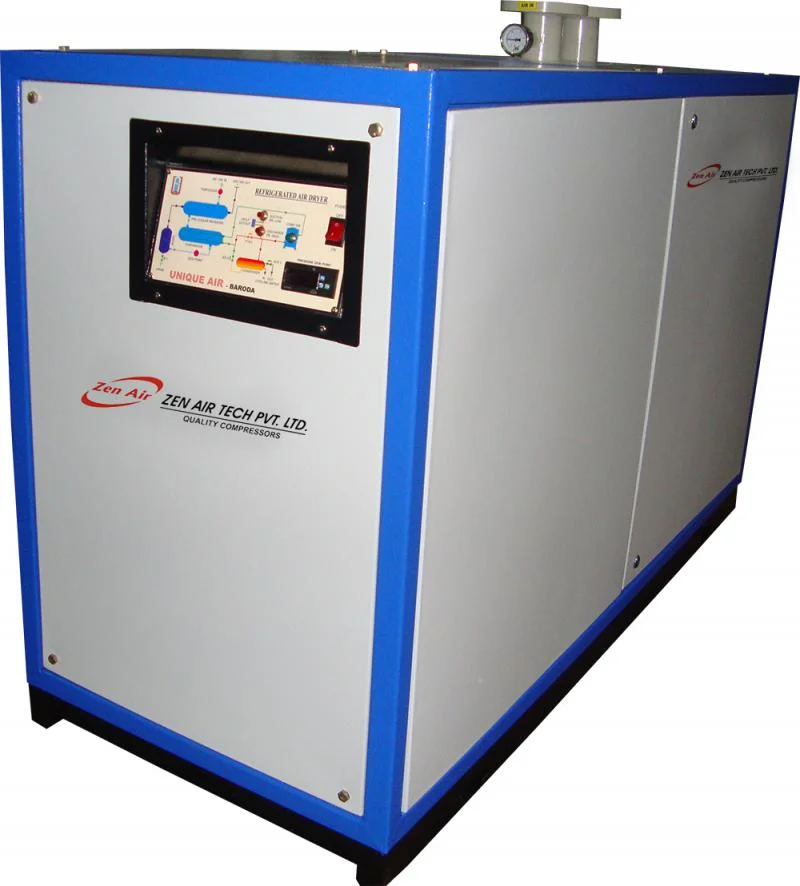
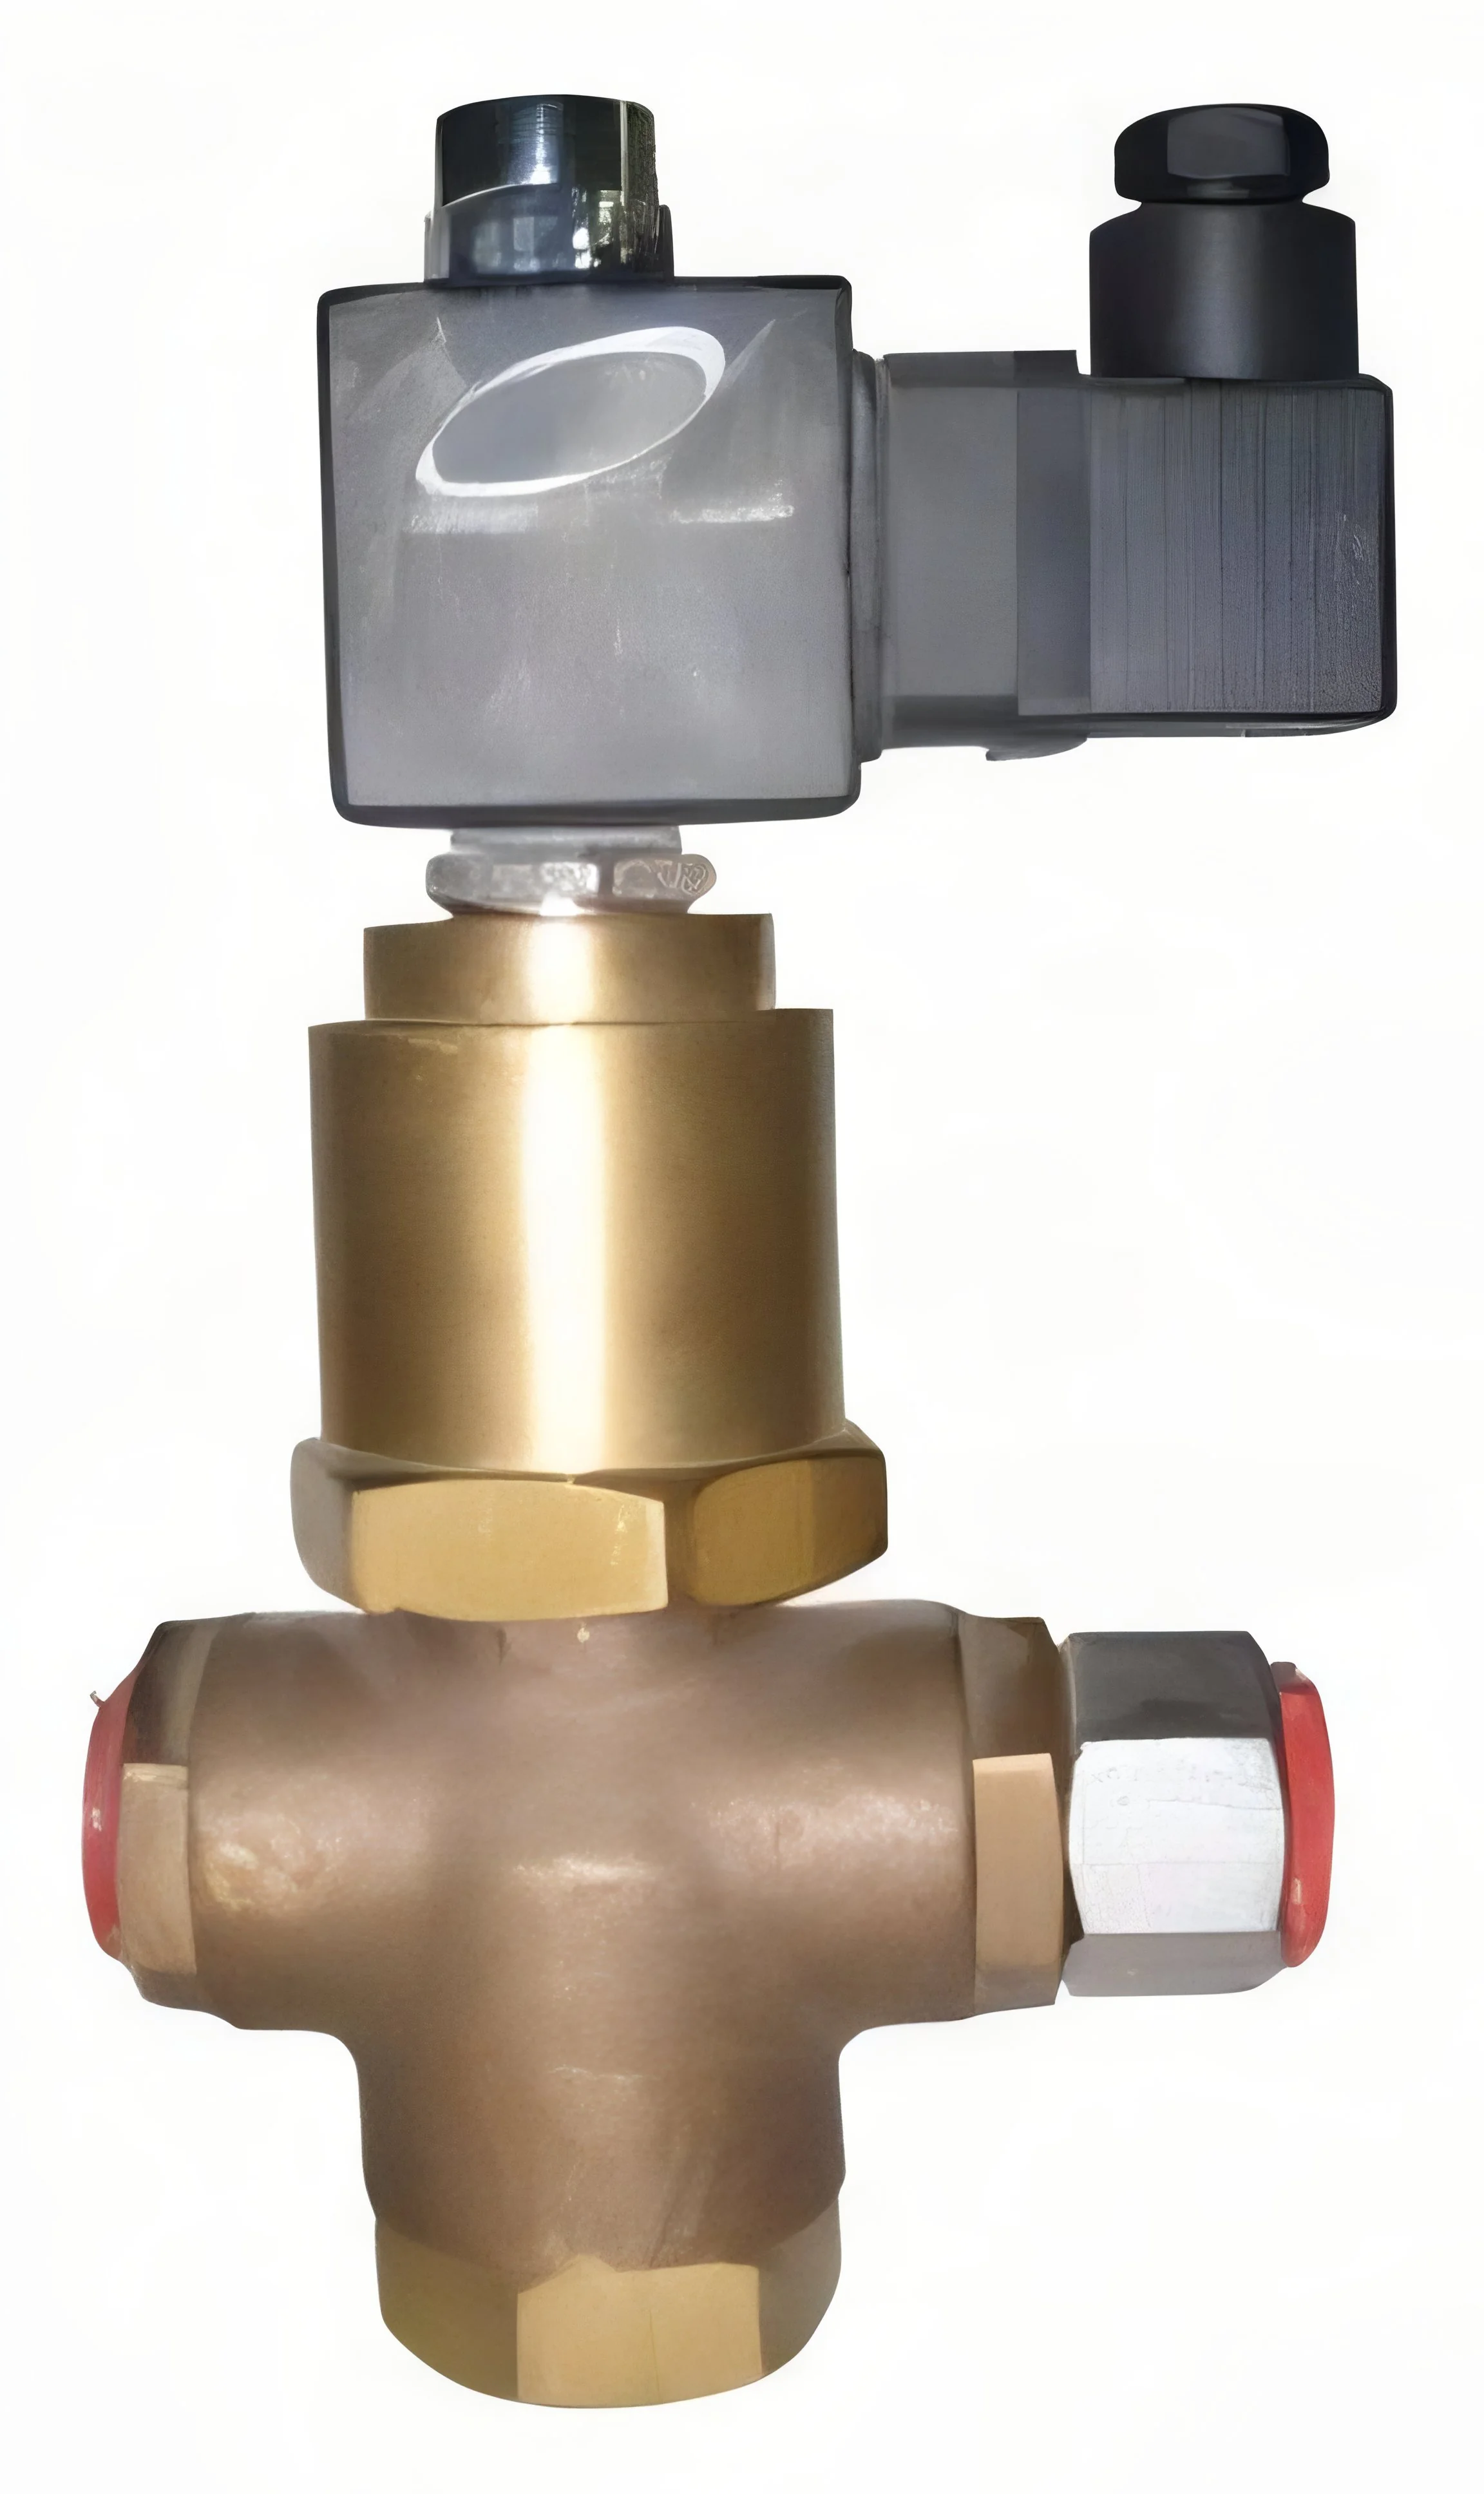
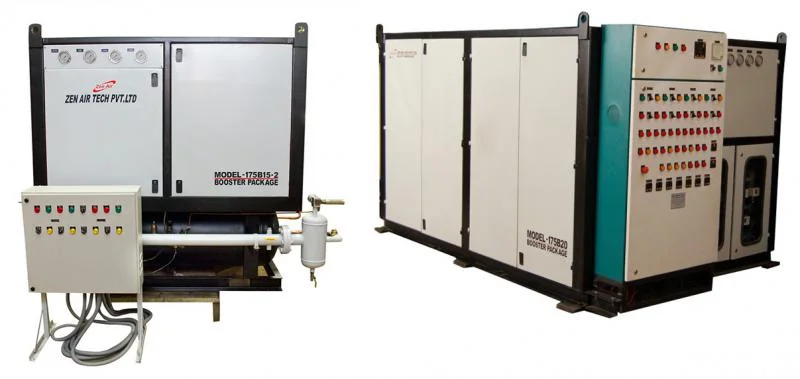
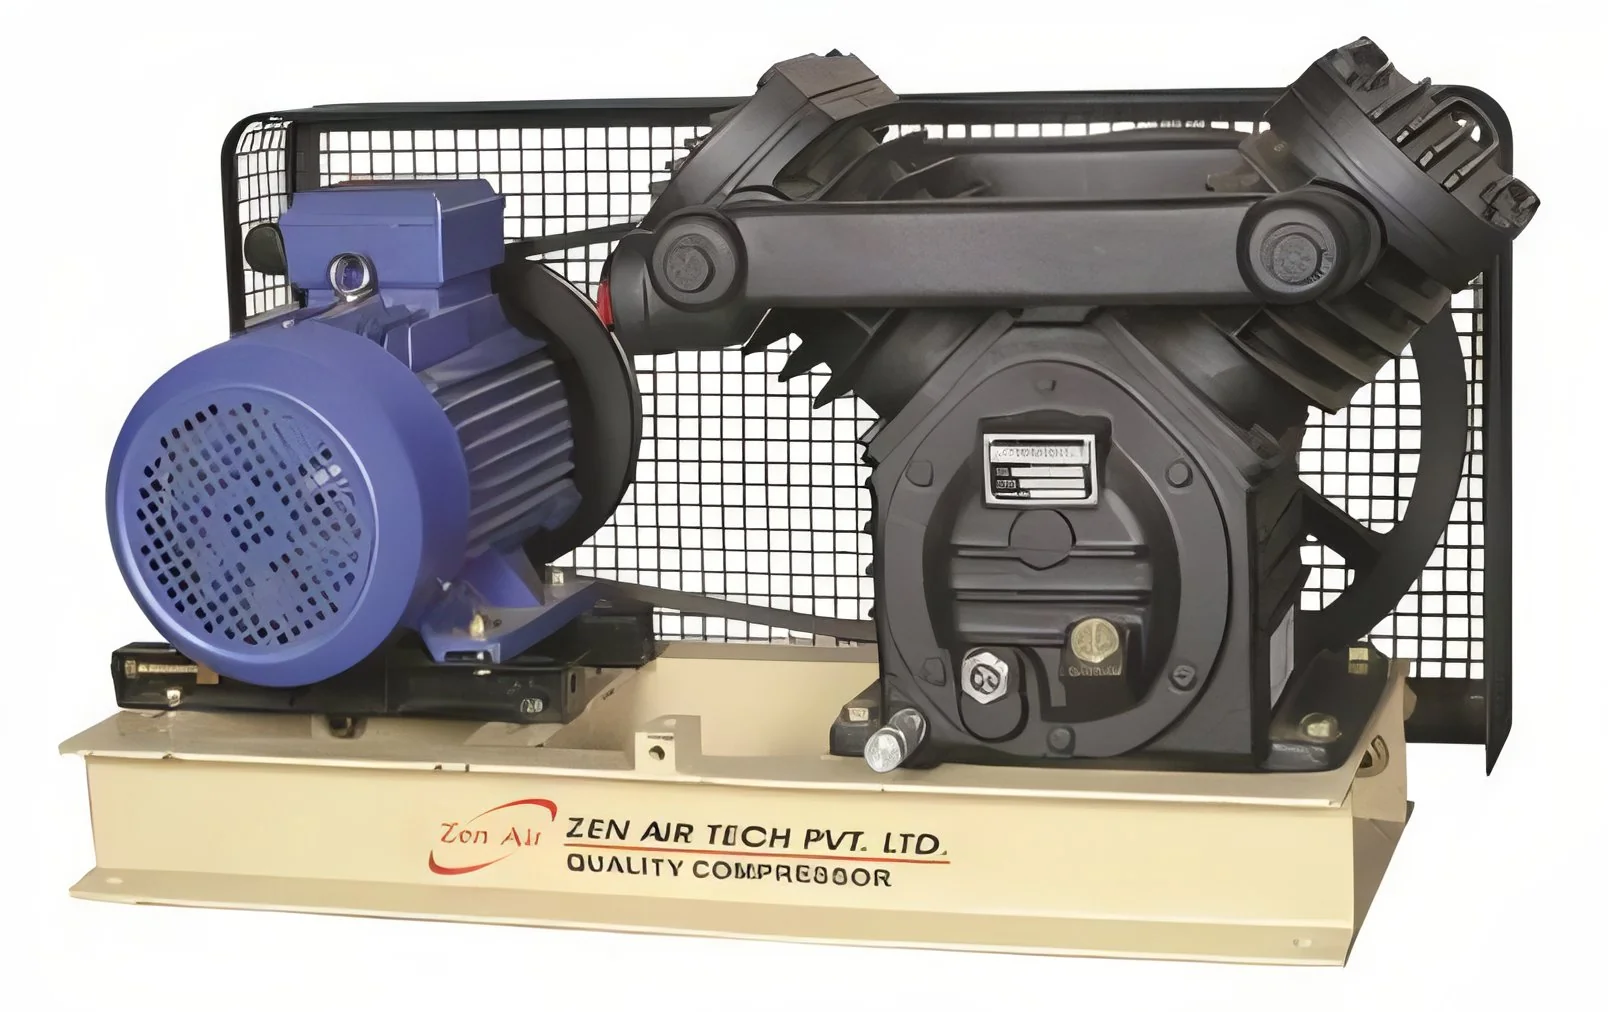
Our industrial air piston vacuum pumps represent reliable performance in industrial vacuum technology, designed for demanding applications where operational continuity is essential. These robust single and two stage systems provide consistent vacuum pressure for critical processes across various industrial settings. Engineered with precision components and durable construction, these pumps deliver exceptional performance across different pressure ranges and operational conditions. The dual-stage configuration offers flexibility for varying vacuum requirements, while the piston-driven mechanism ensures reliable operation with minimal maintenance needs. Built to withstand continuous operation in challenging industrial environments, these units provide years of dependable service without compromising on performance or efficiency.

These vacuum pumps serve essential functions across multiple industrial sectors including ceramic manufacturing, paper production, healthcare facilities, and sp...
Our industrial air piston vacuum pumps represent reliable performance in industrial vacuum technology, designed for demanding applications where operational continuity is essential. These robust single and two stage systems provide consistent vacuum pressure for critical processes across various industrial settings. Engineered with precision components and durable construction, these pumps deliver exceptional performance across different pressure ranges and operational conditions. The dual-stage configuration offers flexibility for varying vacuum requirements, while the piston-driven mechanism ensures reliable operation with minimal maintenance needs. Built to withstand continuous operation in challenging industrial environments, these units provide years of dependable service without compromising on performance or efficiency.

These vacuum pumps serve essential functions across multiple industrial sectors including ceramic manufacturing, paper production, healthcare facilities, and specialized processing plants. In ceramic industries, they facilitate efficient mold evacuation and material handling processes. Paper mills utilize them for reliable suction systems in paper feeding and processing equipment. Medical facilities depend on these pumps for central vacuum systems supporting various healthcare procedures. Carbon processing plants employ them for resin infusion processes, while industrial facilities use them for controlled material extraction and safety systems. The versatility and reliability make them suitable for any application requiring consistent air evacuation capabilities.

The operational value of these vacuum pumps lies in their exceptional reliability, reduced maintenance costs, and consistent performance. These systems are engineered for continuous operation, significantly minimizing downtime and associated production losses. The energy-efficient design lowers operational expenses while the durable construction reduces replacement part requirements. The proven reliability track record means operations can depend on these pumps for critical processes, making them a valuable long-term investment for any facility requiring consistent vacuum performance. Their robust design ensures they withstand demanding conditions while maintaining operational efficiency.

Key Features:
- Single and two stage configurations for flexible vacuum pressure requirements
- Easy installation with simple pipe connections and power setup
- Fully automatic operation adapting to system demands without complex controls
- Consistent pressure dew point ensuring effective moisture removal
- Timer operated drain system with isolation valve and strainer protection

Benefits:
- Flexible operation options suitable for various industrial applications
- Quick setup and integration into existing systems
- Automated performance reducing operator intervention needs
- Efficient moisture control maintaining system reliability
- Protected drainage system ensuring long-term operational integrity
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our industrial air piston vacuum pumps deliver reliable performance across demanding environments where consistent air evacuation is critical. These robust systems handle various pressure requirements with precision, making them suitable for both industrial and specialized applications where operational continuity is essential. The pumps maintain stable operation even in challenging conditions, ensuring processes continue without interruption or downtime.
These vacuum pumps serve multiple sectors including manufacturing, healthcare, and material processing industries. Their durable design allows integration into existing systems with minimal modification requirements. From industrial material handling to medical air systems, these pumps provide necessary vacuum force for efficient operations while maintaining energy efficiency and operational reliability across diverse working conditions.
- Ceramic manufacturing plants for mold evacuation and material handling systems
- Paper production mills for suction systems in paper feeding equipment
- Hospital facilities for central medical vacuum and air evacuation
- Carbon processing units for resin infusion and composite molding
- Industrial plants for controlled material extraction and processing systems
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Zen Air Tech Pvt Ltd, Gujarat
 Gujarat, India
Industrial Equipment & Machinery•Manufacturer
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
South Asia
Industrial Air Piston Vacuum Pumps For Ceramic Paper Mills Hospitals
Reliable single and two stage industrial air piston vacuum pumps for ceramic, paper mills, hospitals, and carbon processing applications. Built for durability with consistent performance in demanding environments.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Zen Air Tech Pvt Ltd
 Gujarat, India
Industrial Equipment & MachineryManufacturer