IN
₹
Apparel & Fashion
Description
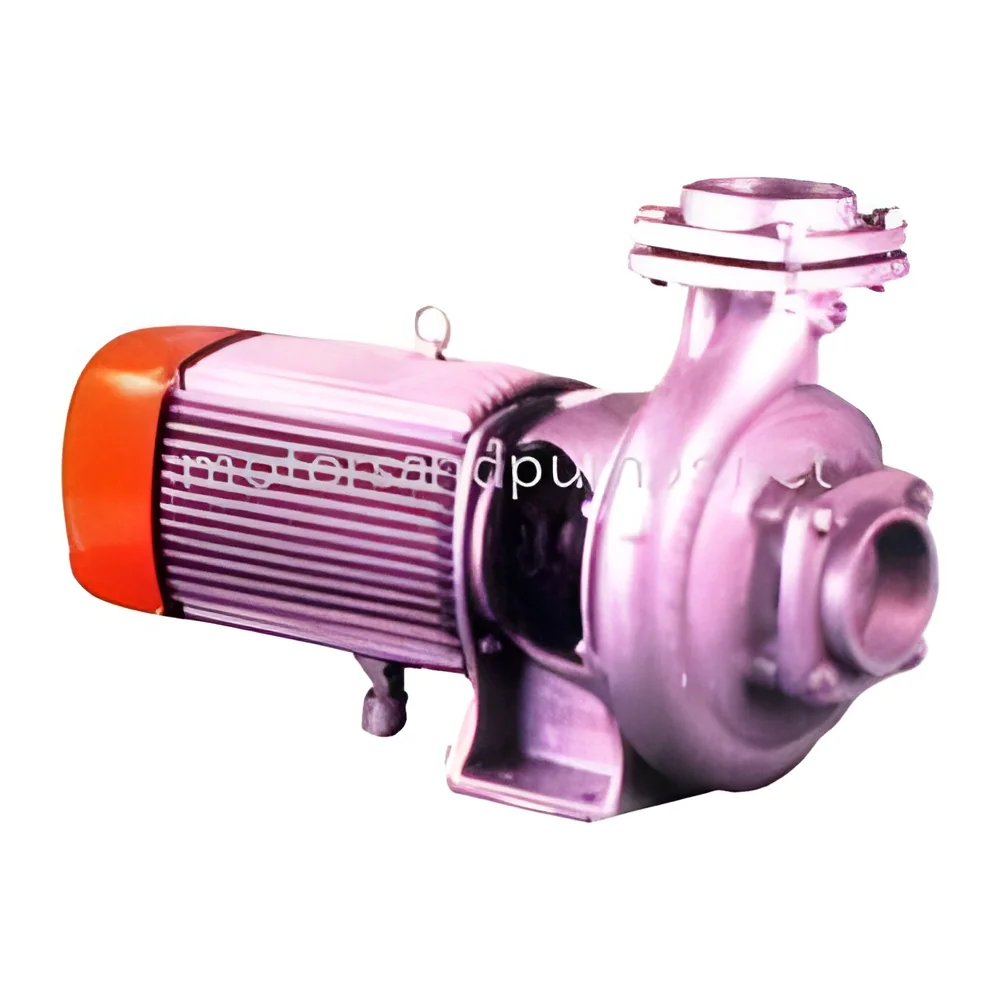
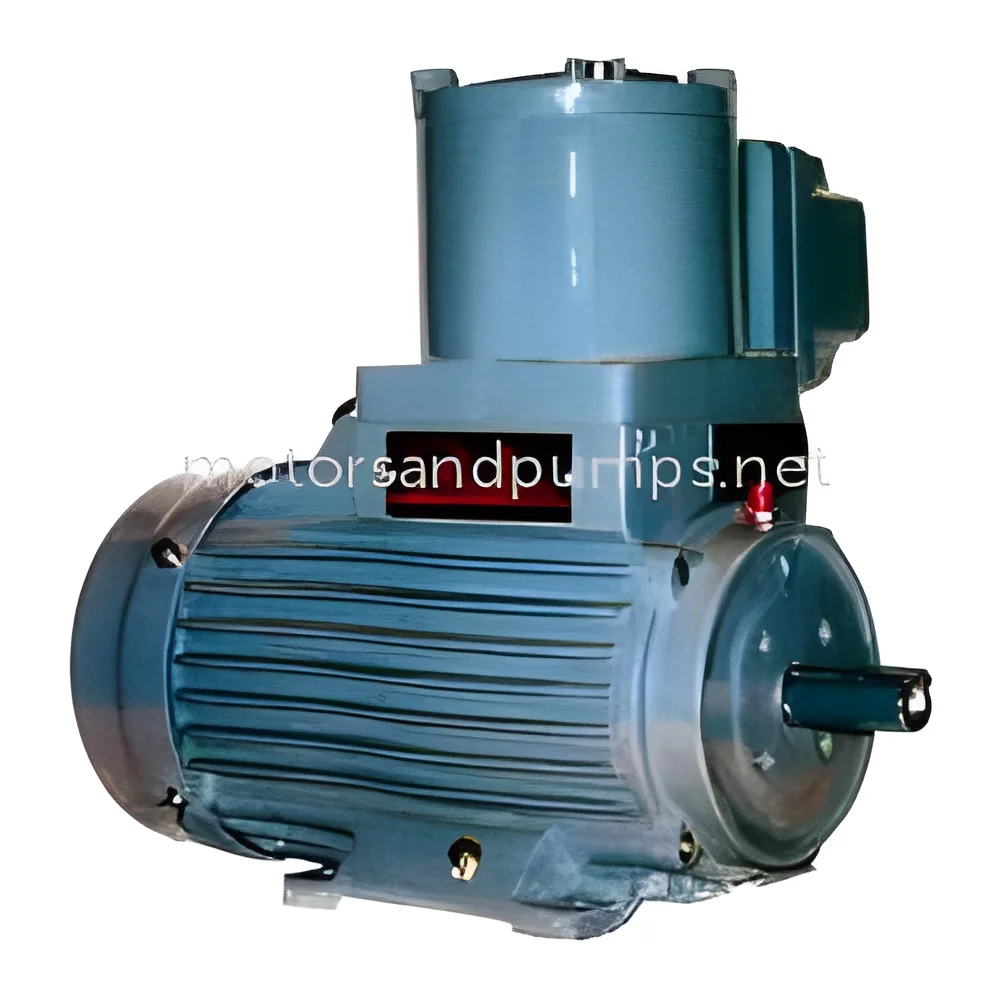
Industrial vacuum pumps are engineered for demanding applications where performance and durability cannot be compromised. These high-performance units deliver consistent vacuum pressure through precision engineering and durable component construction. Advanced sealing technology ensures vacuum integrity while efficient motor systems optimize energy consumption. Built for continuous operation in challenging environments, these pumps provide reliable service with minimal maintenance requirements, making them ideal for operations where equipment failure is not an option. Their robust design withstands varying operational conditions while maintaining consistent output.

These vacuum pumps serve critical functions across multiple industrial sectors. In pharmaceutical manufacturing, they maintain sterile environments during production processes. Food processing facilities utilize them for packaging and preservation applications. Chemical plants rely on them to handle aggressive vapors and ga...
Industrial vacuum pumps are engineered for demanding applications where performance and durability cannot be compromised. These high-performance units deliver consistent vacuum pressure through precision engineering and durable component construction. Advanced sealing technology ensures vacuum integrity while efficient motor systems optimize energy consumption. Built for continuous operation in challenging environments, these pumps provide reliable service with minimal maintenance requirements, making them ideal for operations where equipment failure is not an option. Their robust design withstands varying operational conditions while maintaining consistent output.

These vacuum pumps serve critical functions across multiple industrial sectors. In pharmaceutical manufacturing, they maintain sterile environments during production processes. Food processing facilities utilize them for packaging and preservation applications. Chemical plants rely on them to handle aggressive vapors and gases safely. The automotive industry employs them for brake system testing and emission analysis, while electronics manufacturers depend on them for creating contamination-free environments during circuit board production. Their versatility extends to plastics manufacturing for molding processes and medical facilities where diagnostic and treatment equipment requires stable vacuum sources.

Businesses select these industrial vacuum pumps for their proven reliability and operational value. The durable construction minimizes maintenance needs and reduces unexpected downtime, while energy-efficient operation lowers long-term running costs. These pumps deliver consistent performance across diverse industrial settings, providing buyers with confidence in their investment. The equipment's ability to maintain precise vacuum levels under varying conditions ensures process consistency and product quality. With a focus on operational efficiency and reduced total cost of ownership, these pumps represent a sound investment for serious industrial operations.

Key Features:
- High-efficiency motor design optimized for reduced energy consumption during continuous operation
- Corrosion-resistant construction suitable for handling harsh chemical environments and vapors
- Advanced sealing technology that maintains vacuum integrity and prevents leakage
- Integrated thermal protection system to prevent overheating during extended operation
- Modular design allowing straightforward maintenance and component replacement

Benefits:
- Consistent performance reduces process variability and improves product quality
- Durable construction minimizes maintenance requirements and extends service life
- Energy-efficient operation lowers electricity consumption and operational costs
- Reliable vacuum maintenance ensures process stability and reduces downtime
- Versatile application across multiple industries provides flexible usage options
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
These industrial vacuum pumps provide reliable suction power for continuous operation in demanding environments. They handle material transfer, degassing, and process evacuation with precision, ensuring minimal downtime and consistent performance where operational reliability is critical.
Engineered for stability across varying pressures and temperatures, these pumps support sensitive production processes requiring contamination-free vacuum solutions. Their robust construction makes them suitable for industries where equipment must perform consistently under challenging conditions while maintaining efficiency and operational integrity.
- Removing air from packaging systems to preserve product freshness in food and pharmaceutical sectors
- Evacuating gases and vapors during chemical manufacturing and distillation processes
- Providing suction for automated material handling, lifting, and transfer systems in manufacturing
- Creating controlled vacuum environments for semiconductor fabrication and electronics production
- Supporting medical and laboratory equipment that requires precise, stable vacuum pressure for accurate operation
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Petece Enviro Engineers, Tamil Nadu
 Tamil Nadu, India
Electronics & Electrical•Trading Company•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
North America
Northern Europe
Mid East
Southern Europe
Eastern Europe
South Asia
Western Europe
Africa
Domestic
Industrial Vacuum Pumps For High Performance Durable Applications
Industrial vacuum pumps deliver high-performance, durable operation for demanding applications. Trusted by global importers for consistent quality and efficiency across manufacturing, processing, and packaging industries.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Petece Enviro Engineers
 Tamil Nadu, India
Electronics & ElectricalTrading Company