IN
₹
Apparel & Fashion
Description
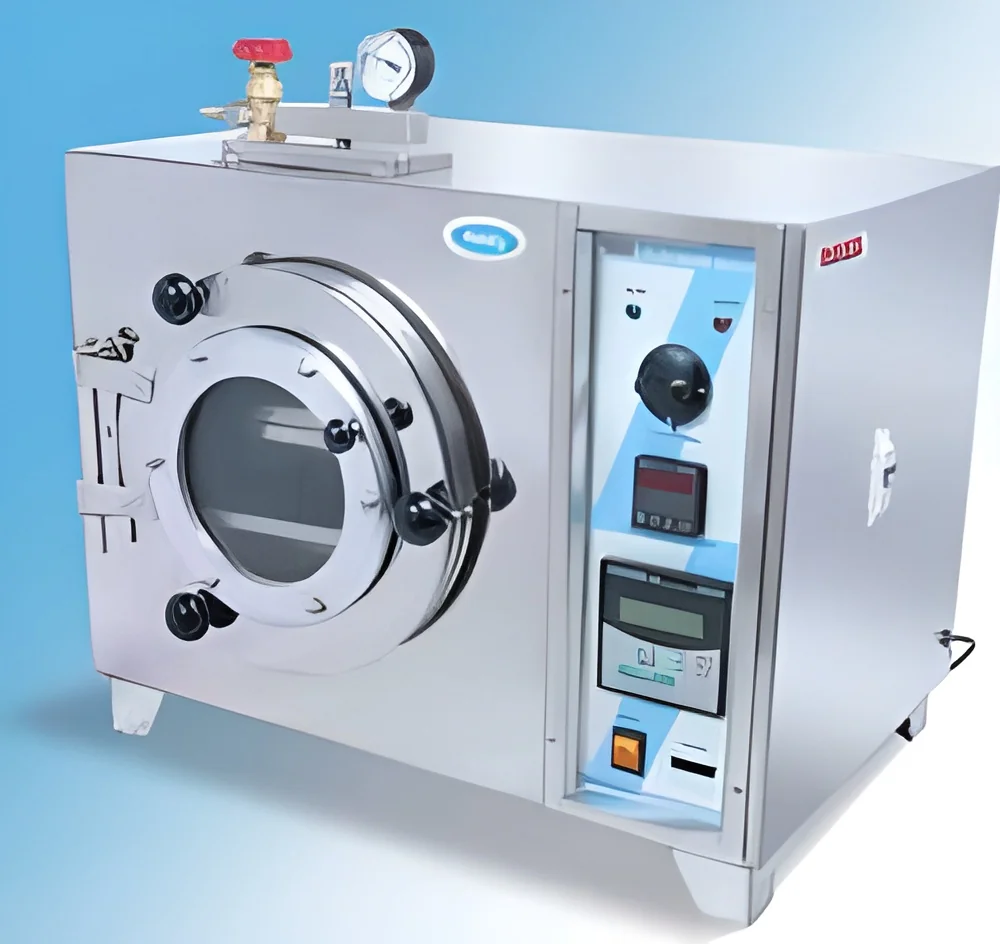
Our industrial vacuum ovens provide precision drying and heat treatment solutions for demanding industrial environments. Engineered with a stainless steel chamber, these units deliver excellent vacuum performance and uniform heating capabilities. The reliable temperature control system ensures consistent results while the robust construction guarantees long-term durability. These vacuum ovens maintain precise environmental conditions essential for sensitive materials and critical processes, offering dependable performance for various industrial applications.

These vacuum ovens serve essential functions across multiple industries where precise environmental control is crucial. Pharmaceutical manufacturers utilize them for drying heat-sensitive compounds and preparing samples without contamination. Electronics producers rely on them for moisture removal from delicate components where conventional methods would cause damage. Research facilities employ these units for material testing and...
Our industrial vacuum ovens provide precision drying and heat treatment solutions for demanding industrial environments. Engineered with a stainless steel chamber, these units deliver excellent vacuum performance and uniform heating capabilities. The reliable temperature control system ensures consistent results while the robust construction guarantees long-term durability. These vacuum ovens maintain precise environmental conditions essential for sensitive materials and critical processes, offering dependable performance for various industrial applications.

These vacuum ovens serve essential functions across multiple industries where precise environmental control is crucial. Pharmaceutical manufacturers utilize them for drying heat-sensitive compounds and preparing samples without contamination. Electronics producers rely on them for moisture removal from delicate components where conventional methods would cause damage. Research facilities employ these units for material testing and experimental processes requiring exact conditions. Food processing operations benefit from gentle drying that preserves nutritional value, while chemical industries depend on them for solvent removal and specialized material processing under controlled atmospheric conditions.

Businesses investing in our vacuum ovens gain reliable performance that reduces operational costs and improves process efficiency. The durable construction ensures years of trouble-free operation with minimal maintenance requirements, providing excellent return on investment. Precise temperature and vacuum control capabilities enable consistent results batch after batch, reducing material waste and enhancing product quality. The energy-efficient design minimizes heat loss, lowering electricity consumption and operational expenses. Safety features including secure sealing mechanisms and front-mounted controls protect both operators and products, ensuring safe operation in industrial settings.

Key Features:
- Stainless steel chamber construction for durability and contamination-free operation
- Uniform heating system for consistent temperature distribution throughout chamber
- Reliable temperature control with precise accuracy for consistent process results
- Excellent vacuum performance for controlled atmospheric conditions
- Robust construction ensuring long-term reliability in industrial environments

Benefits:
- Consistent process results through precise temperature and vacuum control
- Reduced operational costs with energy-efficient design and minimal maintenance
- Enhanced product quality with uniform heating and contamination-free environment
- Long-term reliability with durable construction and quality components
- Improved process efficiency with reliable performance and consistent operation
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our industrial vacuum ovens deliver precise drying and heat treatment for critical processes requiring contamination-free environments. The stainless steel chamber ensures product purity while uniform heating and accurate temperature control provide consistent results across various industrial applications. These reliable units maintain precise vacuum conditions essential for sensitive materials and delicate components.
Manufacturers choose these vacuum ovens for their robust construction and dependable performance in demanding environments. The excellent vacuum performance and reliable temperature control make these units suitable for industries where process consistency and material integrity are paramount. The stainless steel interior resists corrosion while maintaining clean operating conditions for sensitive applications.
- Pharmaceutical manufacturing for drying heat-sensitive compounds without degradation
- Electronics production for moisture removal from delicate components and circuit boards
- Research laboratories for experimental processes requiring precise environmental control
- Food processing facilities for gentle drying of ingredients while preserving quality
- Chemical industries for solvent removal and material processing under controlled conditions
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Abhishek Scientific Company, Maharashtra
 Maharashtra, India
Electronics & Electrical•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Vacuum Oven For Drying Heat Treatment Stainless Steel Chamber
Industrial vacuum oven for precise drying and heat treatment with stainless steel chamber. Features uniform heating, reliable temperature control, and excellent vacuum performance for demanding industrial applications.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Abhishek Scientific Company
 Maharashtra, India
Electronics & ElectricalManufacturer