IN
₹
Apparel & Fashion

Description
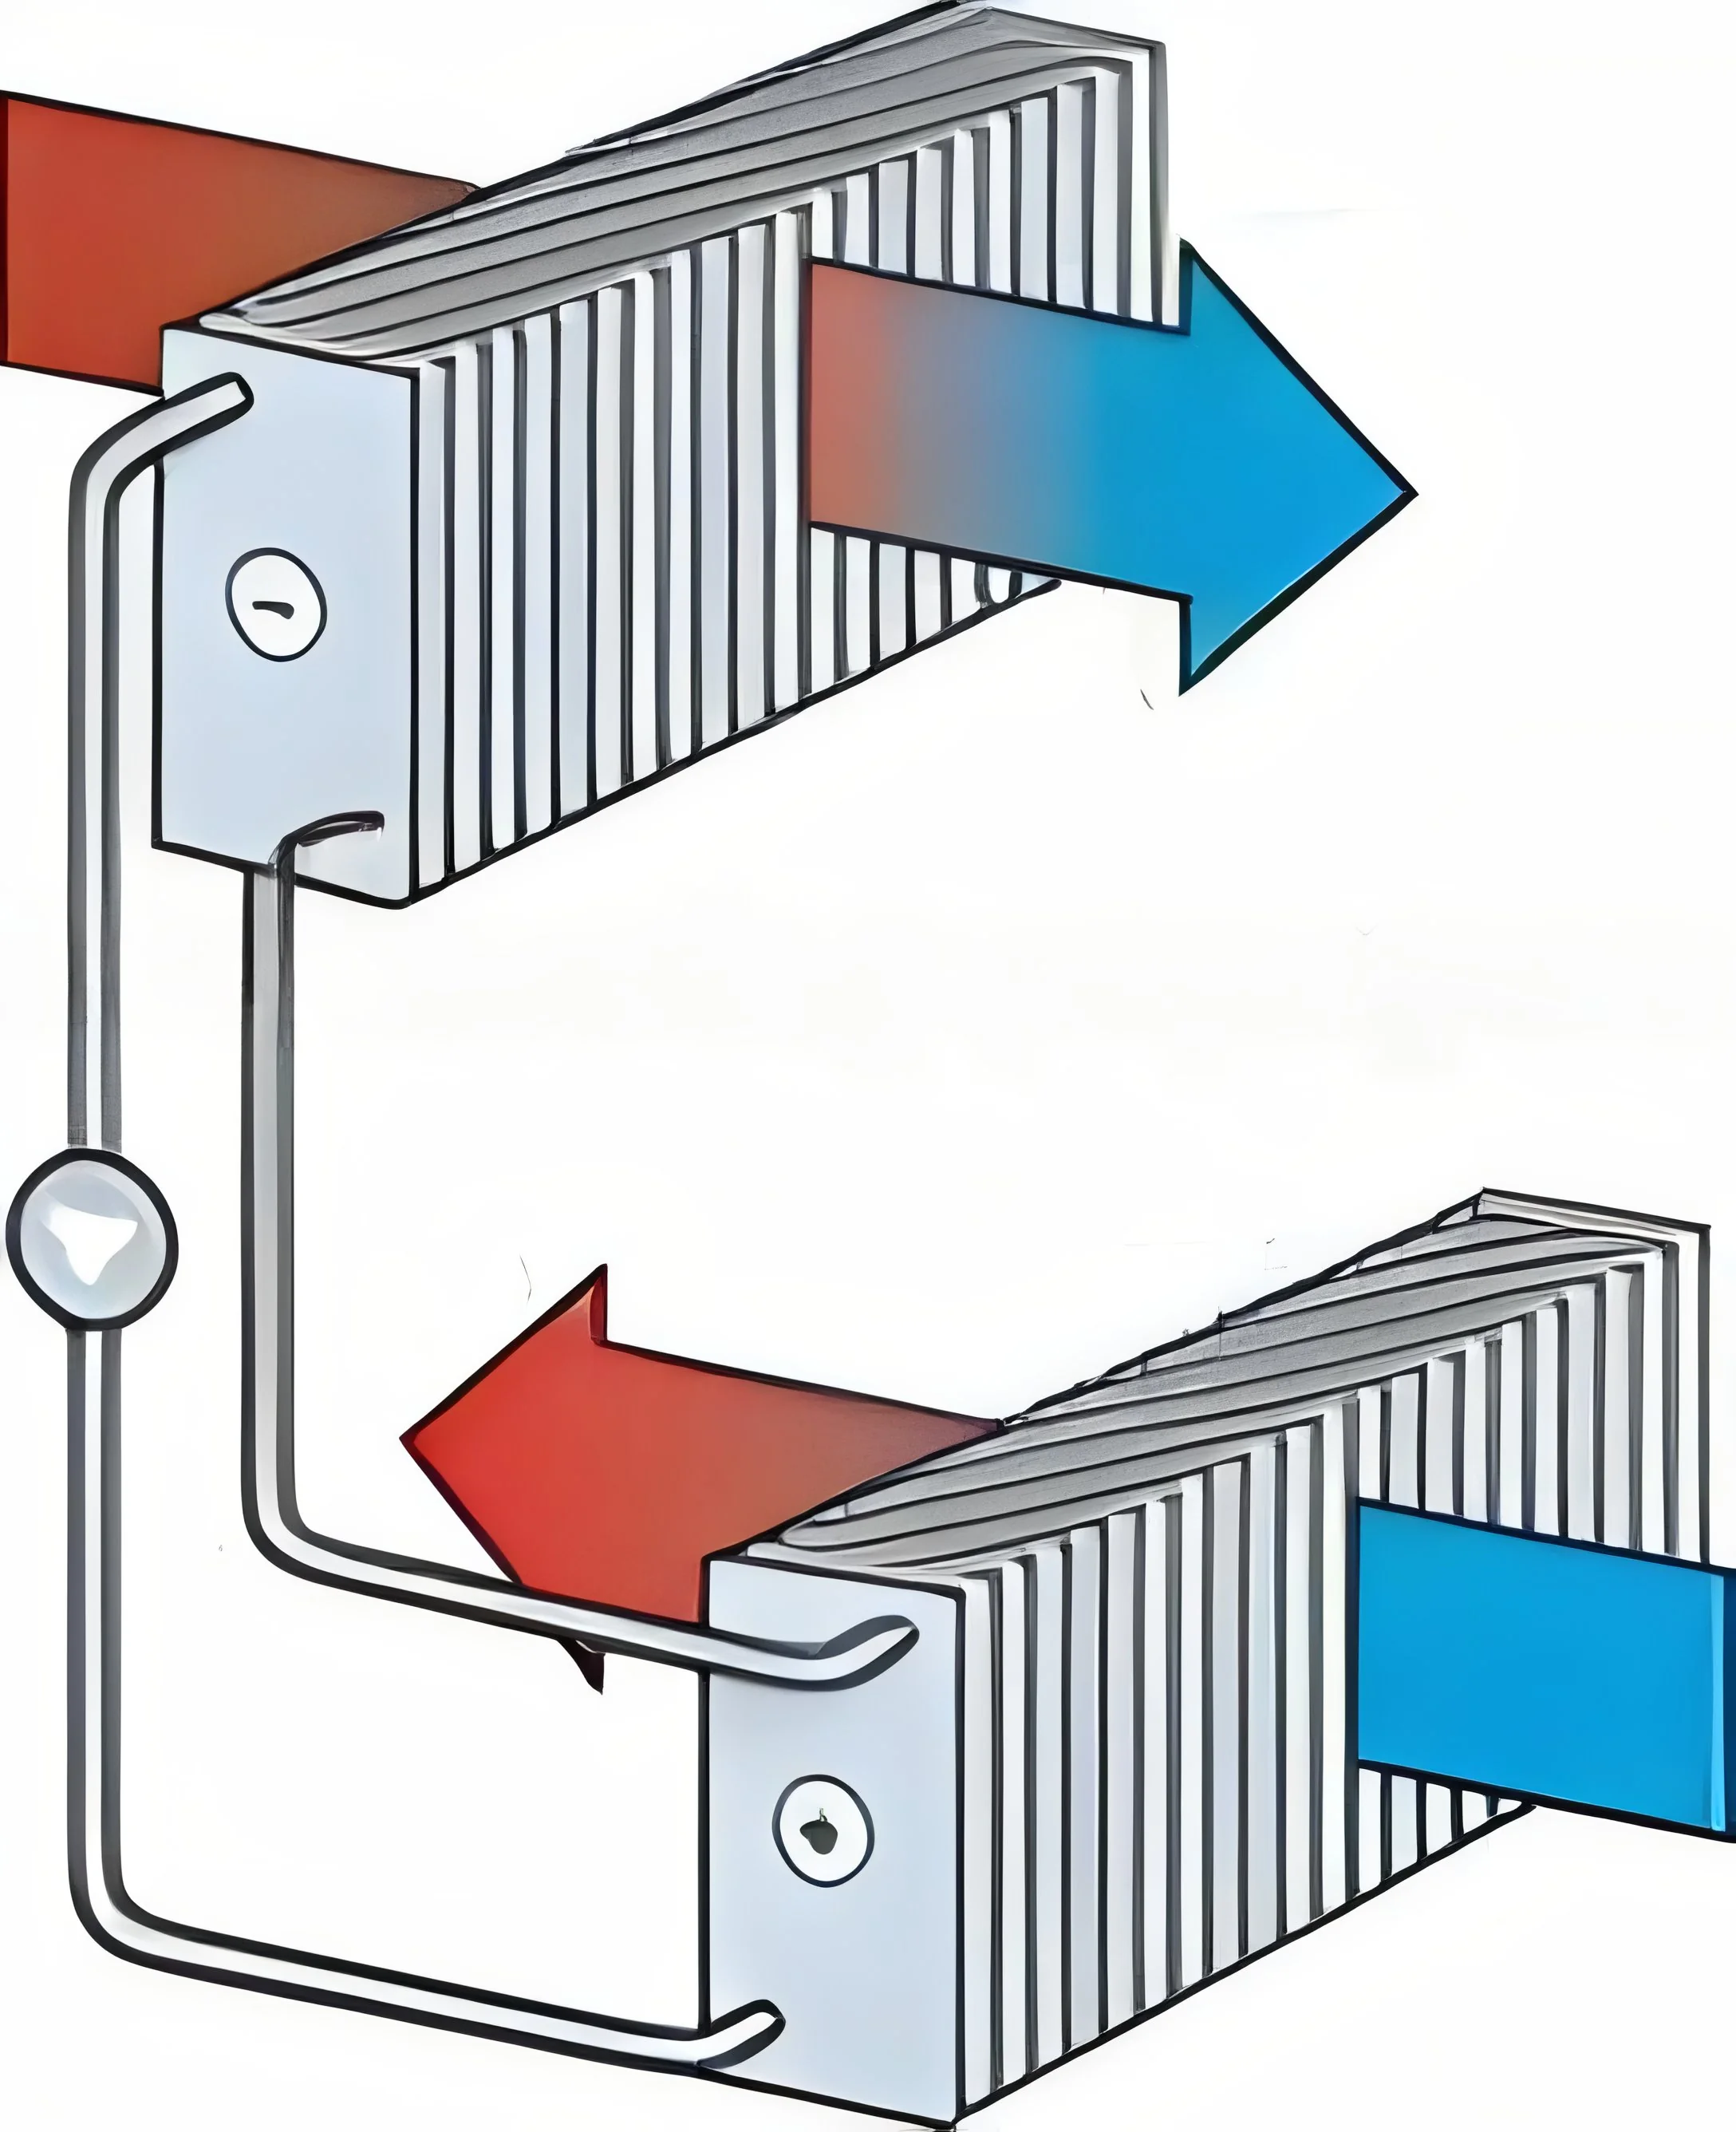
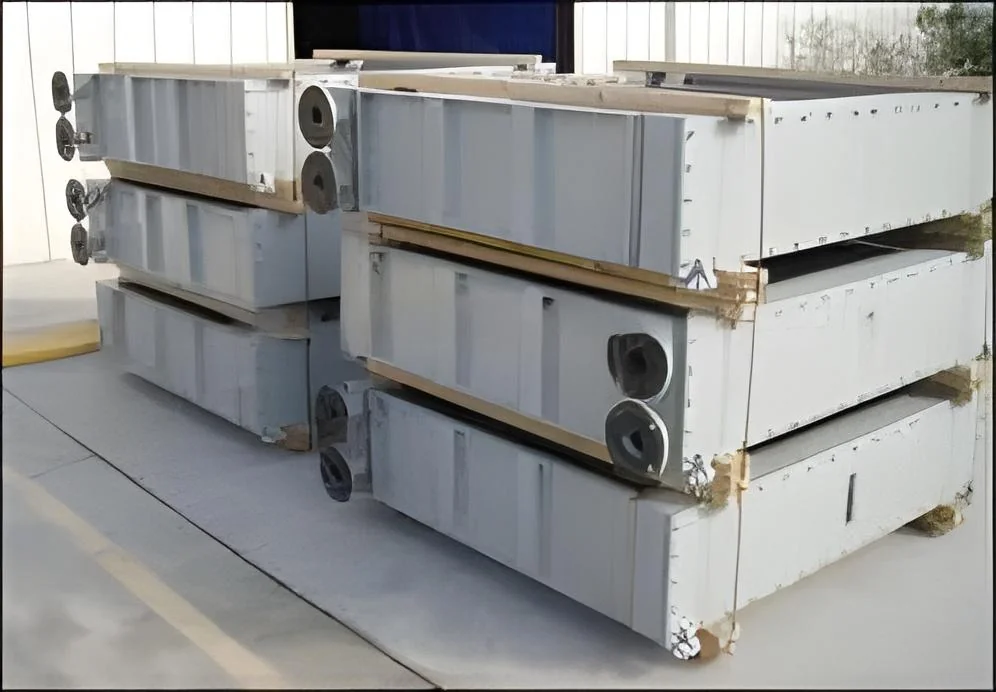
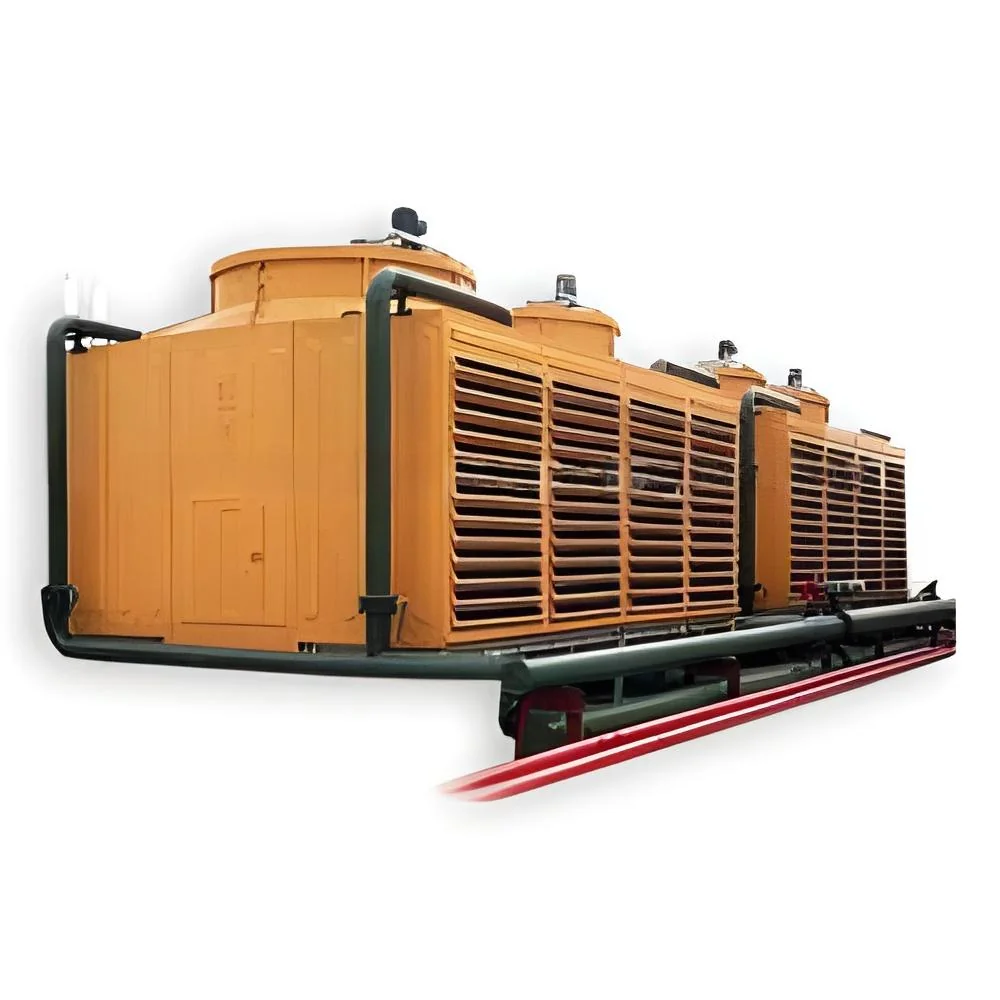
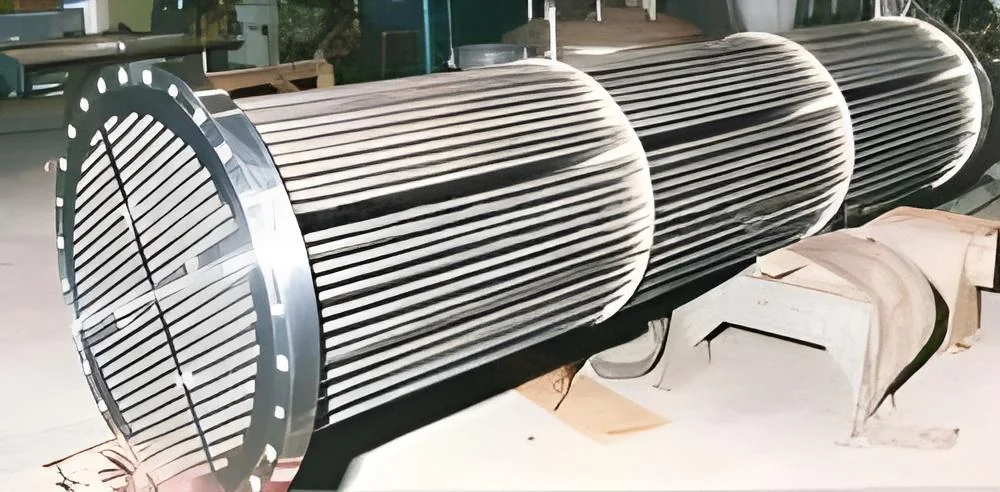
Our industrial tube heat exchanger represents advanced thermal management technology engineered for demanding industrial environments. This high-performance unit delivers 400kW capacity with a robust 40Bar pressure rating and versatile 5-30 m/s flow rates, ensuring efficient heat transfer across diverse operating conditions. The construction emphasizes durability and reliability, featuring materials selected for exceptional corrosion resistance and long service life. Designed to maintain consistent performance under high-pressure operations, this heat exchanger provides dependable thermal management where equipment failure is not an option.

This tube heat exchanger serves critical functions across multiple industries where precise thermal control is essential for operational efficiency. In power generation facilities, it supports condenser and boiler applications, while chemical processing plants rely on it for reactor cooling and heating operations. HVAC systems utilize these units f...
Our industrial tube heat exchanger represents advanced thermal management technology engineered for demanding industrial environments. This high-performance unit delivers 400kW capacity with a robust 40Bar pressure rating and versatile 5-30 m/s flow rates, ensuring efficient heat transfer across diverse operating conditions. The construction emphasizes durability and reliability, featuring materials selected for exceptional corrosion resistance and long service life. Designed to maintain consistent performance under high-pressure operations, this heat exchanger provides dependable thermal management where equipment failure is not an option.

This tube heat exchanger serves critical functions across multiple industries where precise thermal control is essential for operational efficiency. In power generation facilities, it supports condenser and boiler applications, while chemical processing plants rely on it for reactor cooling and heating operations. HVAC systems utilize these units for temperature regulation in commercial and industrial buildings, and the oil and gas industry employs them for heat recovery systems. Food processing plants benefit from precise temperature control during pasteurization and sterilization processes, ensuring product quality and safety.

The business value of our tube heat exchanger lies in its ability to significantly reduce operational costs through energy savings and minimal maintenance requirements. Engineered for seamless integration into existing systems, it minimizes installation downtime and supports operational continuity. The robust construction ensures extended service life and enhanced system reliability, making it an ideal investment for industries requiring uninterrupted thermal management. This technology delivers long-term returns through improved process efficiency, reduced energy consumption, and increased productivity across various industrial applications.

Key Features:
- 40Bar maximum working pressure for high-pressure industrial applications
- 5-30 m/s liquid flow rate range for versatile operational requirements
- 400kW power capacity for efficient large-scale thermal management
- 380V voltage compatibility for industrial electrical systems
- Tube heat exchanger structure for reliable heat transfer performance

Benefits:
- Reduced operational costs through significant energy savings
- Minimal maintenance requirements for lower total cost of ownership
- Seamless integration into existing systems to minimize downtime
- Extended service life with durable, corrosion-resistant construction
- Improved process efficiency and productivity across applications
Specifications
| Key Attributes | |
|---|---|
| Condition | New |
| Dimension(L*W*H) | Customize |
| Liquid Flow Rate | 5 - 30 m/s |
| Maximum Working Pressure | 40Bar |
| Power(W) | Kilowatt,400 |
| Structure | Tube Heat Exchanger |
| Type | Heat Exchanger |
| Voltage | Volt,380 |
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
This industrial tube heat exchanger provides robust thermal management solutions for demanding environments requiring precise temperature control and energy efficiency. With pressure capabilities up to 40Bar and flow rates between 5-30 m/s, it handles both liquid-to-liquid and gas-to-liquid applications across multiple industrial sectors where reliable heat transfer is critical for operational success.
The versatile design supports various industrial processes where heat recovery or cooling is essential. The customizable dimensions and configurations enable seamless integration into existing systems, ensuring optimal performance in high-pressure environments while maintaining consistent heat transfer efficiency and operational reliability for continuous industrial operations.
- HVAC systems for commercial and industrial building climate control
- Power generation plants for condenser and boiler applications
- Chemical processing facilities for reactor cooling and heating
- Oil and gas refineries for heat recovery and process optimization
- Food and beverage industry for pasteurization and sterilization processes
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Precision Cooling System, Tamil Nadu
 Tamil Nadu, India
Industrial Equipment & Machinery•Manufacturer•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
No. of Production Lines2
Annual Production Capacity0 a:2:{i:0;s:6:"Pieces";i:1;s:6:"Pieces";}
Main Markets
Domestic
Industrial Tube Heat Exchanger 40Bar 5 30 m/s 400kW 380V
Industrial tube heat exchanger delivers 400kW capacity with 40Bar pressure rating and 5-30 m/s flow rates for HVAC, power generation, and chemical processing applications requiring reliable thermal management.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Precision Cooling System
 Tamil Nadu, India
Industrial Equipment & MachineryManufacturer