IN
₹
Description
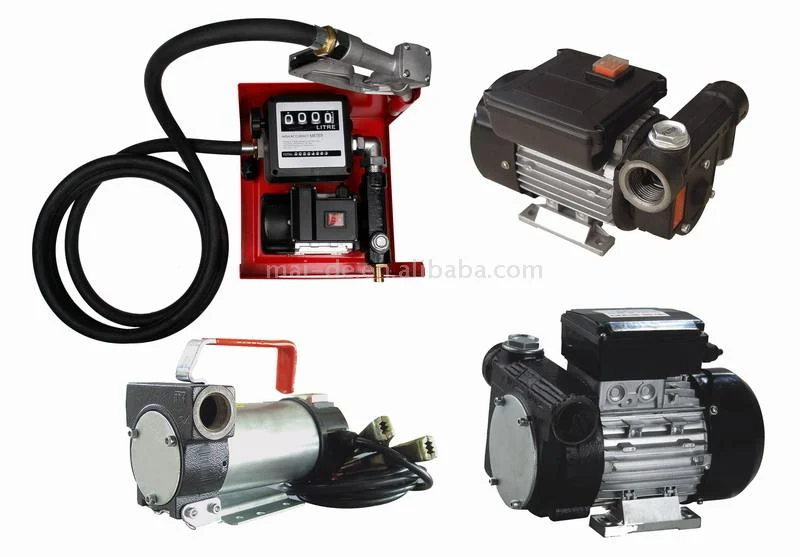
Our industrial transfer pumps represent advanced fluid handling technology designed specifically for commercial and industrial applications. These robust pumps deliver exceptional performance in demanding environments through precision manufacturing and quality materials. They efficiently handle various viscosities and liquid types, from thin solvents to thicker oils and chemicals. Built with durability as a primary focus, these units offer long service life with minimal maintenance requirements. The available customization options ensure each pump can be tailored to specific operational needs, flow rate requirements, and space constraints. This flexibility makes our transfer pumps suitable for diverse industrial settings where reliability and performance are essential for continuous operations.

These transfer pumps find extensive application across numerous industries requiring efficient and safe fluid transfer solutions. In chemical manufacturing, they handle corrosive substances an...
Our industrial transfer pumps represent advanced fluid handling technology designed specifically for commercial and industrial applications. These robust pumps deliver exceptional performance in demanding environments through precision manufacturing and quality materials. They efficiently handle various viscosities and liquid types, from thin solvents to thicker oils and chemicals. Built with durability as a primary focus, these units offer long service life with minimal maintenance requirements. The available customization options ensure each pump can be tailored to specific operational needs, flow rate requirements, and space constraints. This flexibility makes our transfer pumps suitable for diverse industrial settings where reliability and performance are essential for continuous operations.

These transfer pumps find extensive application across numerous industries requiring efficient and safe fluid transfer solutions. In chemical manufacturing, they handle corrosive substances and sensitive compounds with precision and safety. The automotive and fuel industries utilize these pumps for petroleum products and lubricants transfer. Manufacturing plants employ them for coolant circulation and hydraulic fluid management. Water treatment facilities rely on these pumps for chemical dosing and processed water transfer. The food processing industry benefits from specially configured models meeting hygiene standards while handling edible liquids. Agricultural operations use these pumps for fertilizer distribution and irrigation systems, demonstrating their versatility across multiple sectors and applications.

The business value of these transfer pumps lies in their exceptional reliability and operational efficiency, directly translating to reduced downtime and lower maintenance costs. Their robust construction ensures consistent performance even in challenging conditions, protecting operations from unexpected failures. The customization capabilities provide equipment specifically designed for unique requirements, eliminating compromise and improving system integration. These pumps meet international quality standards, ensuring compliance with industry regulations and safety requirements. The long service life and minimal maintenance needs result in significant cost savings over time, making them a smart investment for businesses focused on operational excellence and sustainable performance.

Key Features:
- Heavy-duty construction with corrosion-resistant materials for extended lifespan
- Customizable configurations to meet specific flow rate and pressure requirements
- Compatible with various liquid types including fuels, chemicals, and water
- Efficient motor design ensuring optimal energy consumption and performance
- Easy maintenance access points and user-friendly operational controls

Benefits:
- Reduced operational downtime through reliable performance in demanding conditions
- Lower maintenance costs with durable construction and easy service access
- Enhanced operational efficiency with customizable configurations for specific needs
- Versatile application across multiple industries and fluid types
- Long-term cost savings through extended service life and energy efficiency
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our industrial transfer pumps are engineered for demanding fluid management across multiple sectors, handling various liquids including fuels, chemicals, water, and oils with consistent performance and minimal maintenance. These robust units operate efficiently in challenging environments where reliability is critical, ensuring uninterrupted operations and long-term service life in industrial settings worldwide.
These pumps serve essential roles in manufacturing plants, processing facilities, and industrial operations requiring precise fluid control and contamination prevention. They efficiently transfer materials between containers, tanks, or processing equipment while offering customization options for specific operational requirements and space constraints, making them adaptable to diverse industrial needs and applications.
- Chemical manufacturing plants for safe transfer of corrosive liquids and solvents
- Fuel distribution centers and automotive industries for handling petroleum products
- Water treatment facilities for moving processed water and treatment chemicals
- Food processing plants for transferring edible oils, syrups, and food-grade liquids
- Agricultural operations for fertilizer distribution and irrigation system management
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Anmol Pharma Equipments, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Transfer Pumps For Heavy Duty Fluid Handling
Industrial transfer pumps deliver reliable heavy-duty fluid handling for manufacturing and chemical sectors. Built for durability with customizable configurations to meet specific operational requirements and ensure seamless integration.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Anmol Pharma Equipments
 Maharashtra, India
Industrial Equipment & MachineryManufacturer