IN
₹
Apparel & Fashion
Description
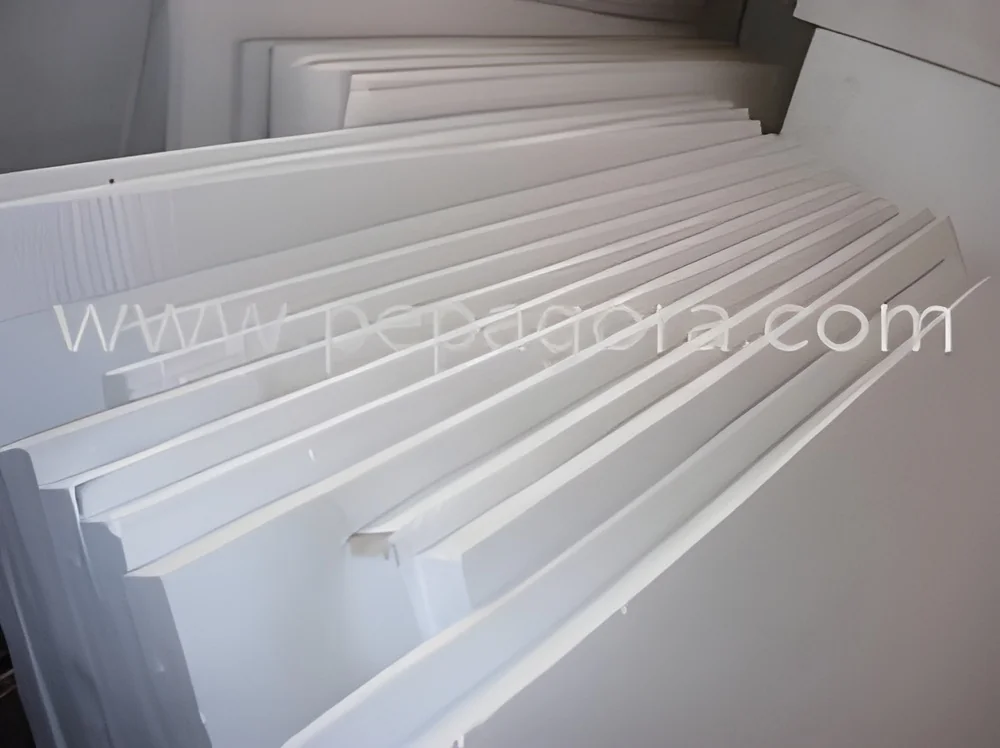
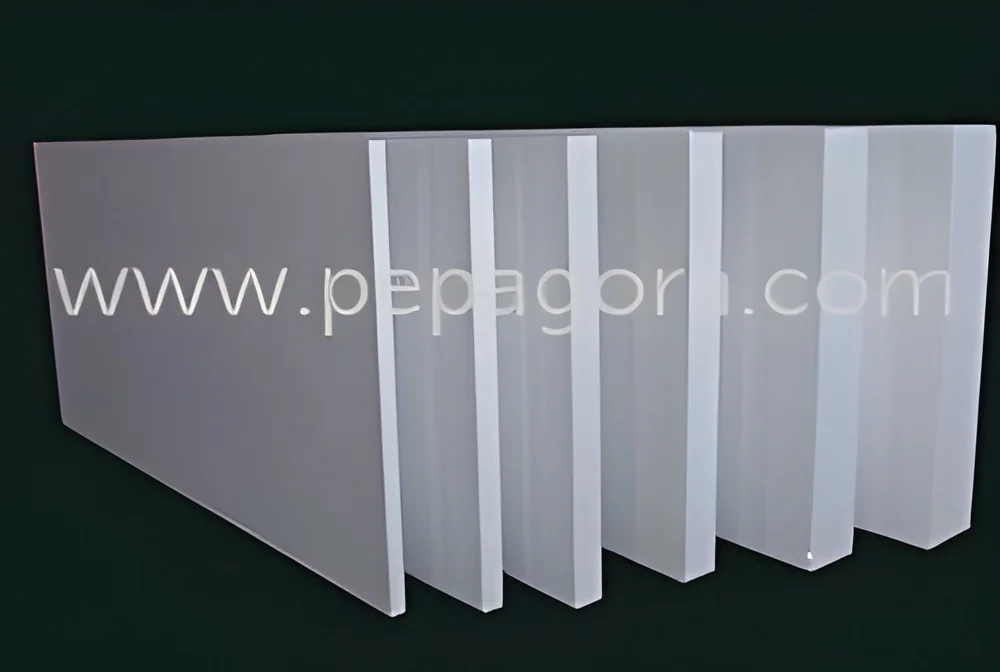
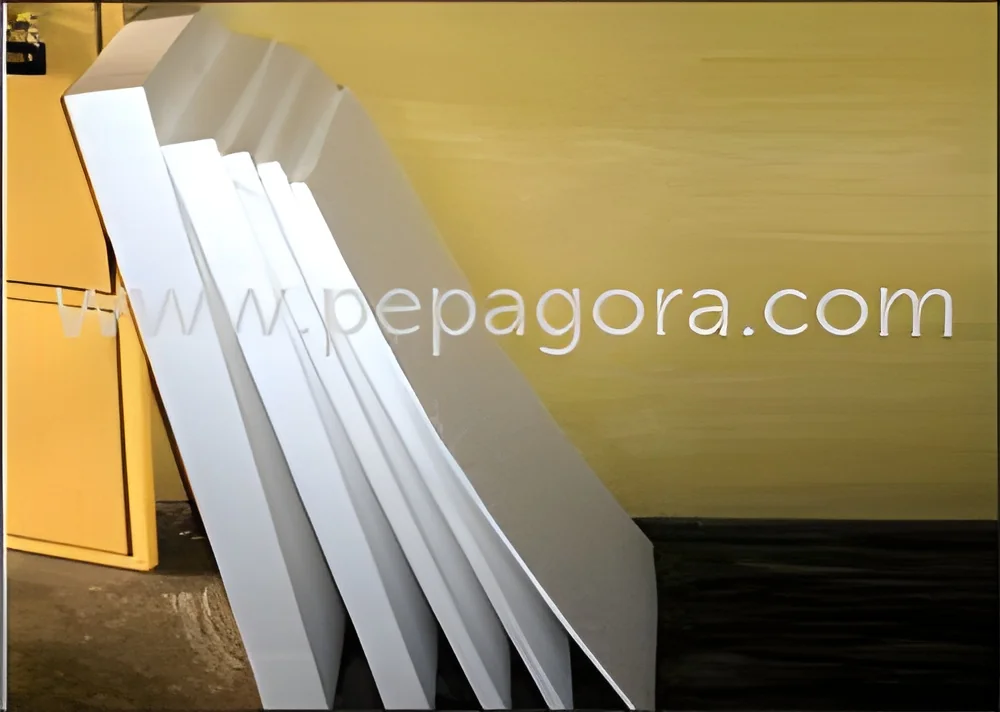
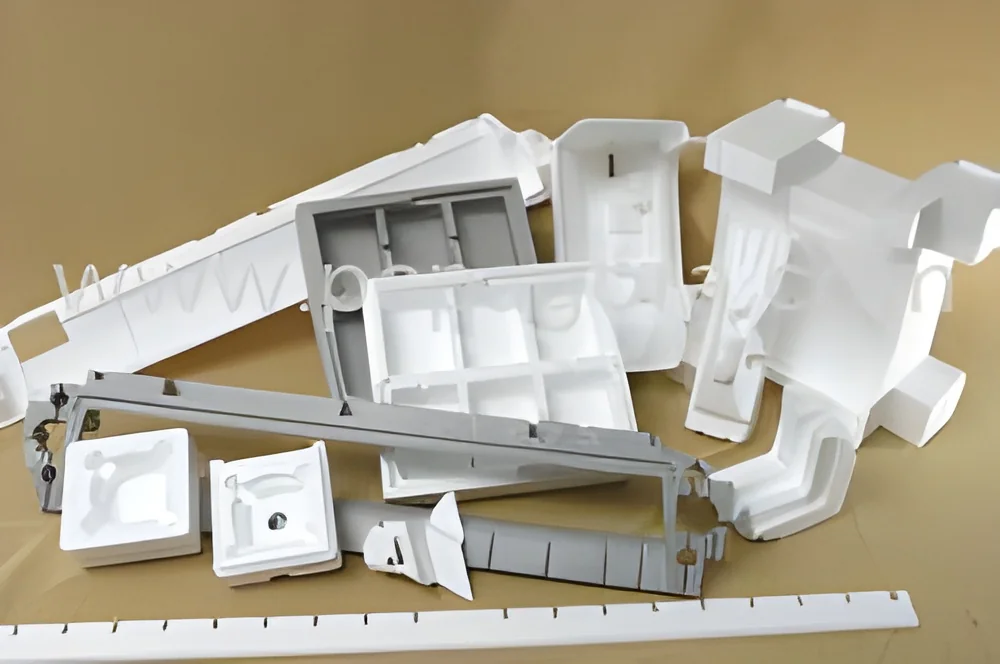
Our Thermocol boxes represent premium protective packaging solutions for businesses requiring uncompromised product safety during shipping and storage. These engineered containers utilize expanded polystyrene's closed-cell structure to deliver exceptional thermal insulation and shock absorption properties. This creates a secure environment for delicate, temperature-sensitive items while maintaining consistent internal conditions. We implement rigorous quality control throughout manufacturing, ensuring every box meets precise dimensional accuracy and performance standards demanded by industrial applications.

These containers serve critical functions across multiple industries where product integrity cannot be compromised. Pharmaceutical companies rely on them for maintaining cold chain integrity during vaccine distribution and medicine transportation. Electronics manufacturers utilize them to prevent damage to sensitive components from impact and static electricity. Food processing ope...
Our Thermocol boxes represent premium protective packaging solutions for businesses requiring uncompromised product safety during shipping and storage. These engineered containers utilize expanded polystyrene's closed-cell structure to deliver exceptional thermal insulation and shock absorption properties. This creates a secure environment for delicate, temperature-sensitive items while maintaining consistent internal conditions. We implement rigorous quality control throughout manufacturing, ensuring every box meets precise dimensional accuracy and performance standards demanded by industrial applications.

These containers serve critical functions across multiple industries where product integrity cannot be compromised. Pharmaceutical companies rely on them for maintaining cold chain integrity during vaccine distribution and medicine transportation. Electronics manufacturers utilize them to prevent damage to sensitive components from impact and static electricity. Food processing operations depend on them for shipping perishable items while maintaining required temperature ranges. Chemical manufacturers trust them for safe transport of temperature-sensitive reagents, while research institutions use them for protecting valuable laboratory specimens during inter-facility transit.

The business value extends beyond basic packaging to strategic supply chain reliability that directly impacts operational efficiency. By minimizing product damage during shipping, these boxes reduce financial losses from returns and replacements while protecting brand reputation for quality delivery. Their lightweight construction significantly lowers shipping costs compared to alternative packaging materials. The thermal insulation properties can reduce dependency on expensive refrigerated shipping in appropriate scenarios, creating additional cost savings while maintaining product integrity. Our established production systems support consistent supply without inventory bottlenecks.

Key Features:
- Excellent thermal insulation properties maintaining temperature stability
- Superior shock absorption and impact resistance for product protection
- Lightweight construction reducing overall shipping costs
- Rigorous quality control ensuring dimensional accuracy and consistency
- Reliable performance across varying environmental conditions

Benefits:
- Maintains product integrity through temperature control and impact protection
- Reduces shipping costs through lightweight design and efficient packaging
- Minimizes product damage and associated financial losses during transit
- Ensures reliable performance across diverse industrial applications
- Supports supply chain efficiency through consistent quality and protection
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Thermocol boxes deliver essential protection for temperature-sensitive products during shipping and storage. Their superior insulation maintains consistent internal temperatures, making them vital for pharmaceuticals, biologics, and perishable food items. These containers also protect fragile electronics, laboratory samples, and industrial components from impact damage during transportation across supply chains.
Beyond temperature management, these boxes provide excellent cushioning against shocks and vibrations during transit. They serve critical roles across healthcare, food processing, electronics manufacturing, and chemical industries. The lightweight design reduces shipping costs while ensuring unmatched product protection for both domestic and international logistics operations.
- Secure transportation of vaccines and temperature-sensitive pharmaceuticals
- Protective packaging for electronics including medical devices and components
- Shipping containers for fresh seafood, frozen foods, and dairy products
- Safe transport for laboratory specimens and medical diagnostic kits
- Insulated containers for chemical samples and temperature-sensitive industrial materials
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Niraj Thermocols, Maharashtra
 Maharashtra, India
Electronics & Electrical•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Thermocol Boxes For Secure Shipping Temperature Sensitive Storage
Thermocol boxes provide secure shipping and temperature-sensitive storage for pharmaceuticals, electronics, and perishables. These reliable, lightweight containers offer excellent insulation and impact protection for sensitive products during transit.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Niraj Thermocols
 Maharashtra, India
Electronics & ElectricalManufacturer