IN
₹
Apparel & Fashion
Description
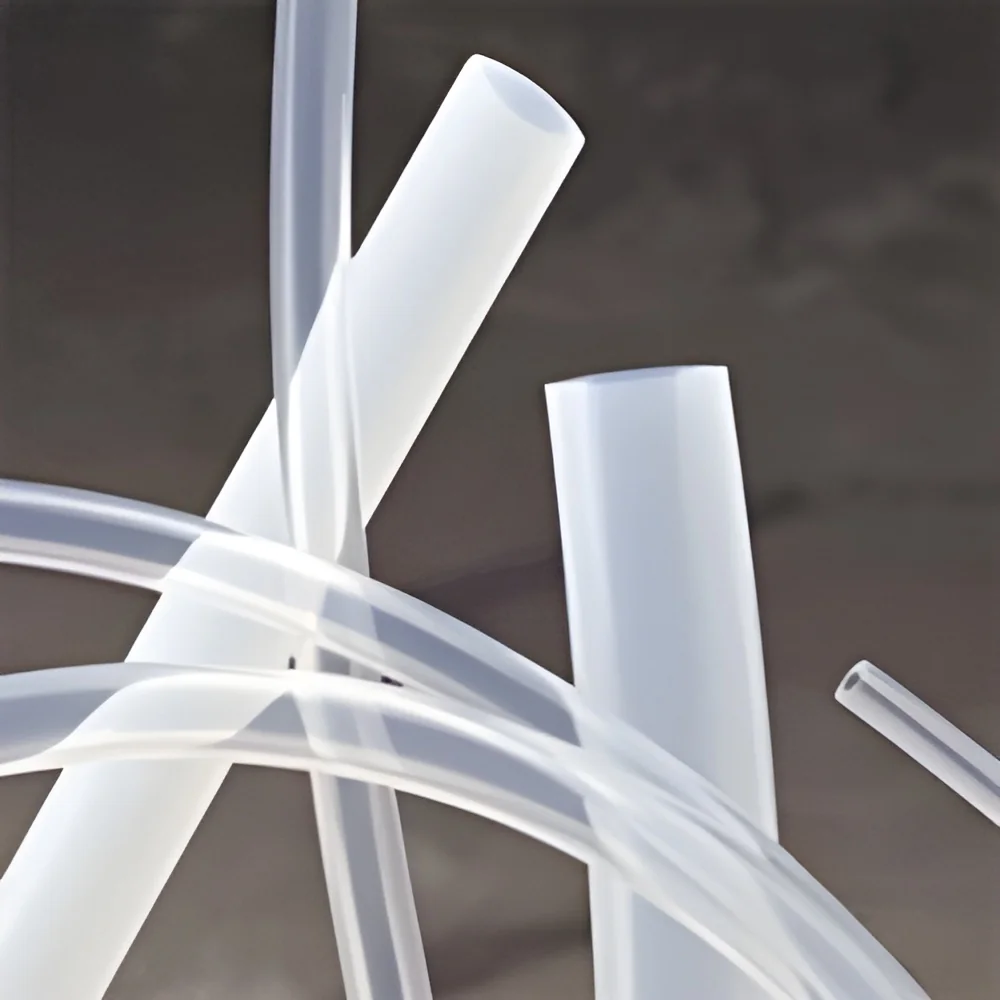
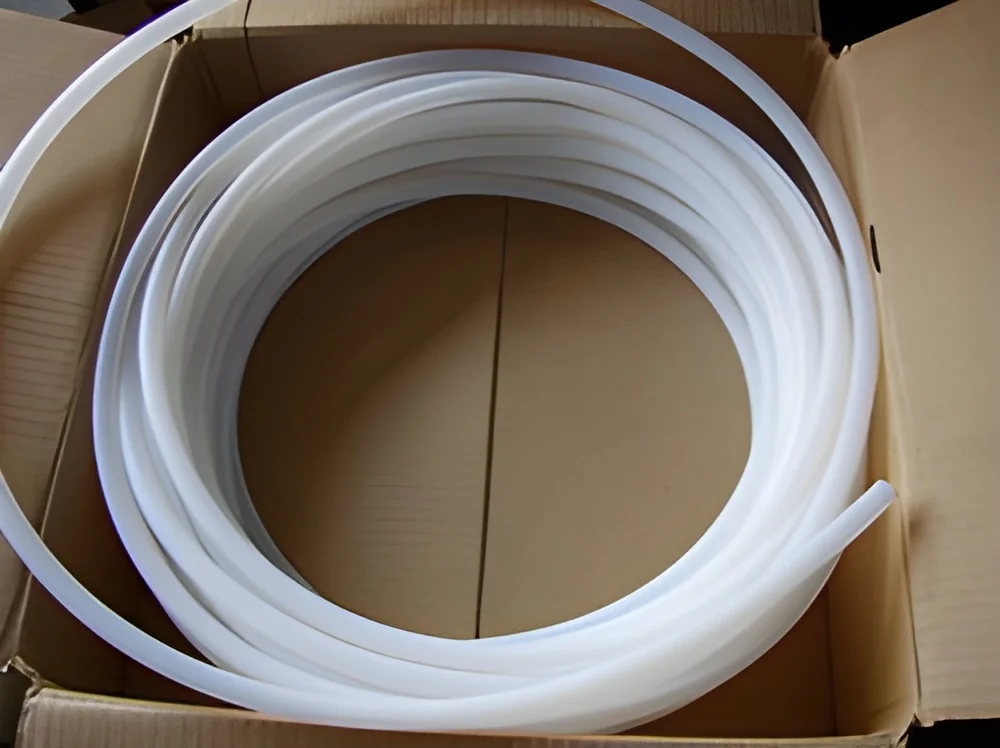
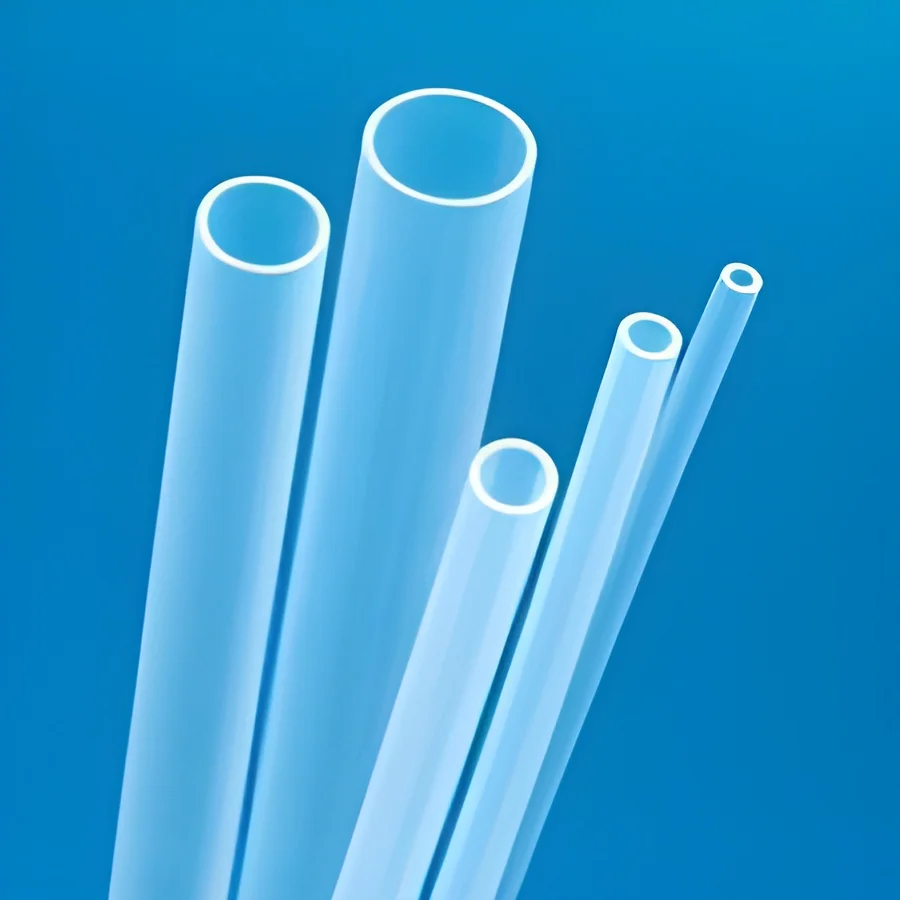
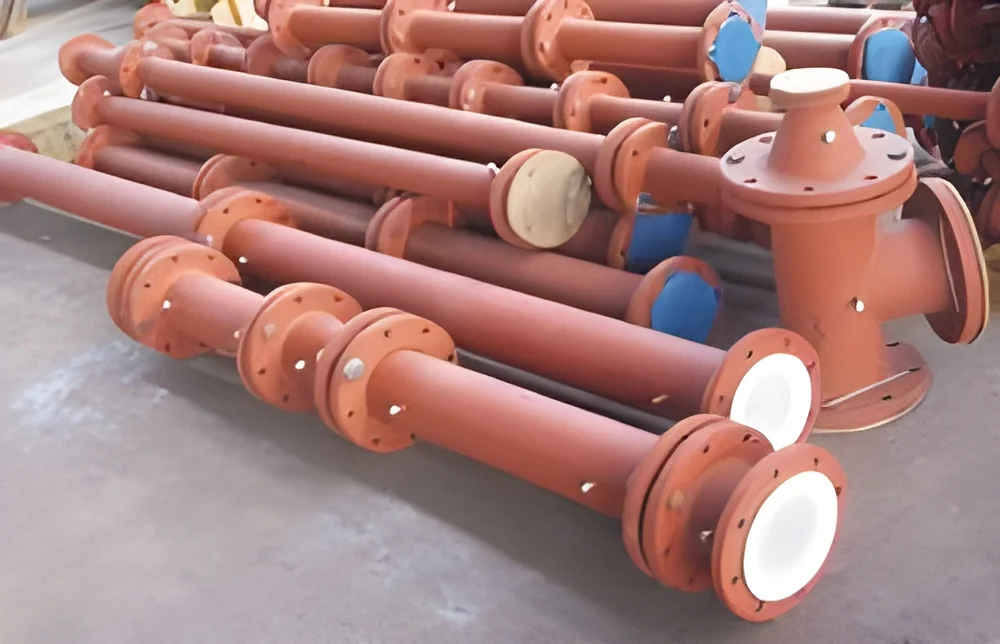
Industrial Teflon tubing, crafted from premium PTFE, sets the benchmark for reliability in demanding fluid transfer systems. It is specifically designed to withstand the most challenging industrial environments, offering unmatched resistance to a vast array of aggressive chemicals including strong acids, bases, and organic solvents. The material's inherent non-stick properties prevent material adhesion and buildup, ensuring consistent flow and drastically reducing maintenance needs. With an operational temperature range from -100°C to +260°C, this tubing maintains its structural integrity and performance across extreme thermal cycles that would cause conventional materials to fail. The smooth inner bore minimizes pressure drop, prevents bacterial colonization, and guarantees purity, making it the ideal choice for applications where reliability and contamination control are critical to operational success and safety.

This tubing is a cornerstone component across multiple high-stakes in...
Industrial Teflon tubing, crafted from premium PTFE, sets the benchmark for reliability in demanding fluid transfer systems. It is specifically designed to withstand the most challenging industrial environments, offering unmatched resistance to a vast array of aggressive chemicals including strong acids, bases, and organic solvents. The material's inherent non-stick properties prevent material adhesion and buildup, ensuring consistent flow and drastically reducing maintenance needs. With an operational temperature range from -100°C to +260°C, this tubing maintains its structural integrity and performance across extreme thermal cycles that would cause conventional materials to fail. The smooth inner bore minimizes pressure drop, prevents bacterial colonization, and guarantees purity, making it the ideal choice for applications where reliability and contamination control are critical to operational success and safety.

This tubing is a cornerstone component across multiple high-stakes industries due to its unparalleled performance profile. Chemical processing facilities depend on it for the safe and efficient transfer of corrosive substances, where any material failure could compromise safety and process continuity. Pharmaceutical manufacturers trust its ultra-clean, non-leaching characteristics for sterile processing, drug formulation, and bioprocessing applications. The food industry utilizes it for its hygienic, FDA-compliant properties in processing sensitive ingredients. In automotive and aerospace, it is specified for fuel, oil, and hydraulic systems that demand reliability under extreme pressure and temperature conditions. Research and semiconductor facilities rely on it for analytical instrumentation and high-purity chemical delivery, where even trace contamination can invalidate results or damage sensitive equipment.

Choosing this Industrial Teflon tubing delivers tangible business value through enhanced reliability and operational efficiency. Its exceptional durability translates to an extended service life, significantly reducing the frequency and cost of replacements while minimizing disruptive downtime. The absolute resistance to chemical degradation safeguards product quality, protects expensive downstream equipment, and preserves brand reputation by eliminating contamination risks. The tubing's compliance with stringent international standards provides assurance of consistent quality and performance, making it a trusted, low-risk specification for critical infrastructure. This reliability allows for predictable maintenance scheduling and long-term system planning, ultimately contributing to a lower total cost of ownership and stronger operational resilience compared to alternative tubing materials.

Key Features:
- Superior chemical resistance against virtually all acids, bases, solvents, and aggressive media.
- Exceptional thermal stability with a continuous service range from -100°C to +260°C.
- Non-stick, non-contaminating PTFE surface prevents buildup and ensures product purity.
- Smooth inner bore design reduces friction loss and inhibits bacterial growth.
- Manufactured for high durability and long service life in demanding industrial settings.

Benefits:
- Ensures process safety and integrity by reliably containing hazardous or sensitive fluids.
- Reduces maintenance frequency and operational downtime due to its robust construction.
- Protects product quality and prevents cross-contamination in critical applications.
- Offers long-term cost savings through extended service life and reduced replacement needs.
- Provides peace of mind with proven performance in the most challenging industrial environments.
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial Teflon tubing is engineered for environments where chemical inertness and thermal stability are non-negotiable. Its PTFE construction provides a non-reactive, non-stick surface that prevents contamination and ensures the smooth, reliable transfer of aggressive or sensitive media. This makes it indispensable for maintaining process integrity and product purity in critical operations where material compatibility is paramount.
Industries select this tubing for its exceptional durability and minimal maintenance needs, which directly reduce operational downtime and costs. From handling concentrated acids to transporting sterile pharmaceutical ingredients, it delivers consistent performance without degradation over time. Its flexibility allows for straightforward installation in complex systems, while its proven reliability supports long-term operational planning and system design for serious industrial buyers.
- Chemical processing plants for safe transfer of corrosive acids, alkalis, and aggressive solvents.
- Pharmaceutical manufacturing for contamination-free fluid transfer in sterile drug production and API handling.
- Food and beverage processing for hygienic transfer of ingredients, flavors, and sensitive products.
- Automotive and aerospace industries for reliable fuel, lubricant, and hydraulic fluid lines.
- Analytical laboratories and semiconductor fabrication for ultra-pure chemical delivery and instrumentation.
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Arizona Tech- Zeal, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Trading Company•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Teflon Tubing High Chemical Resistance Thermal Stability
Industrial Teflon tubing provides superior chemical resistance and thermal stability for demanding fluid transfer in chemical processing, pharmaceuticals, and food manufacturing. This reliable tubing ensures purity and performance.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Arizona Tech- Zeal
 Maharashtra, India
Industrial Equipment & MachineryTrading Company