IN
₹
Apparel & Fashion
Description
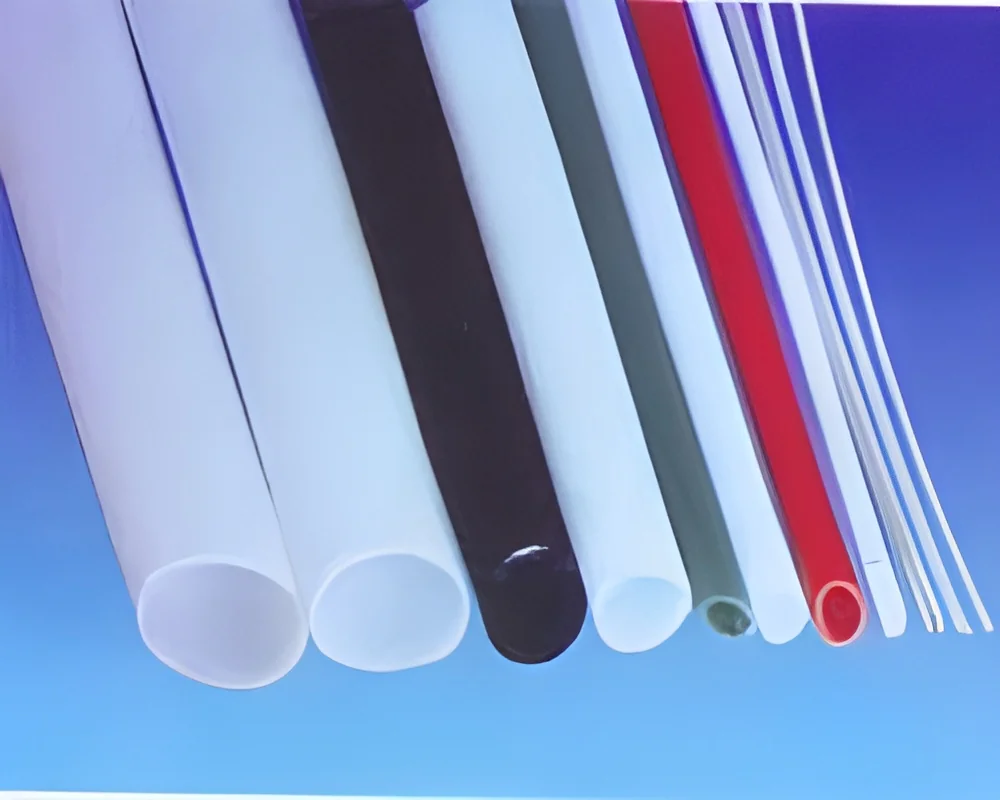
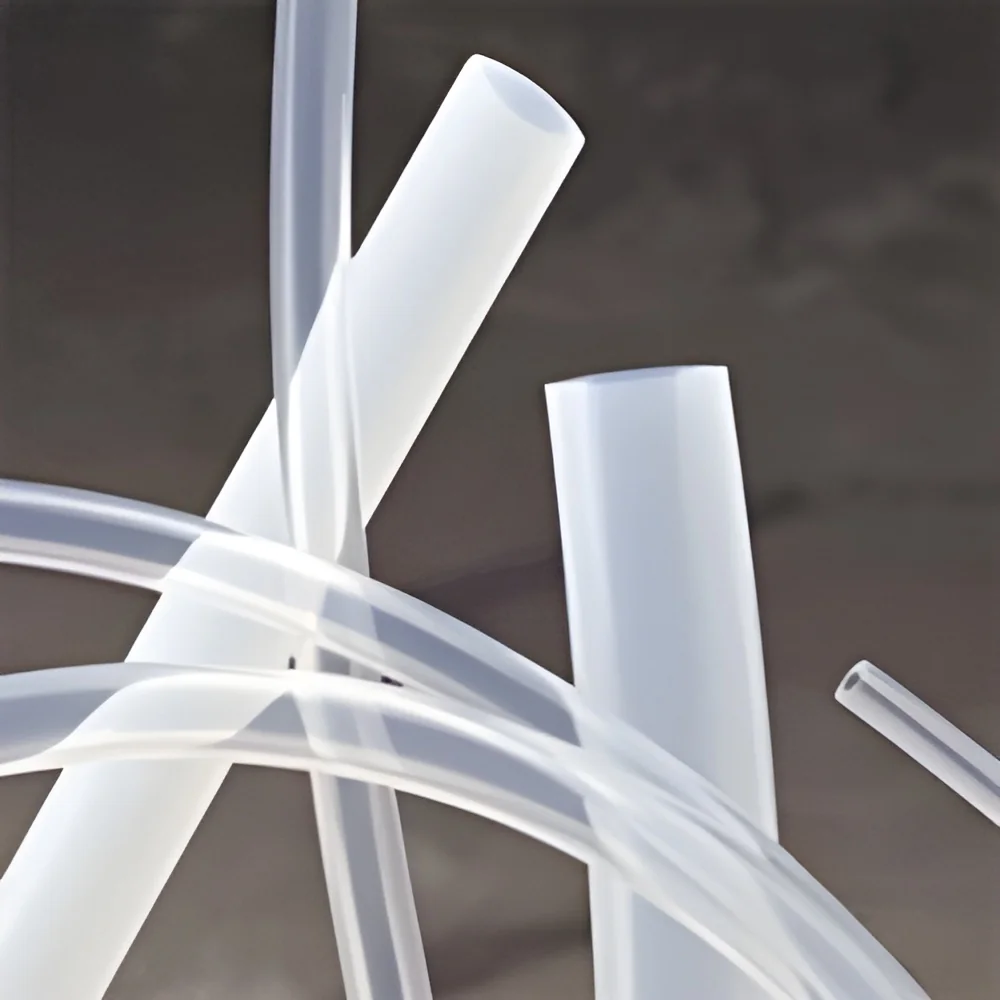
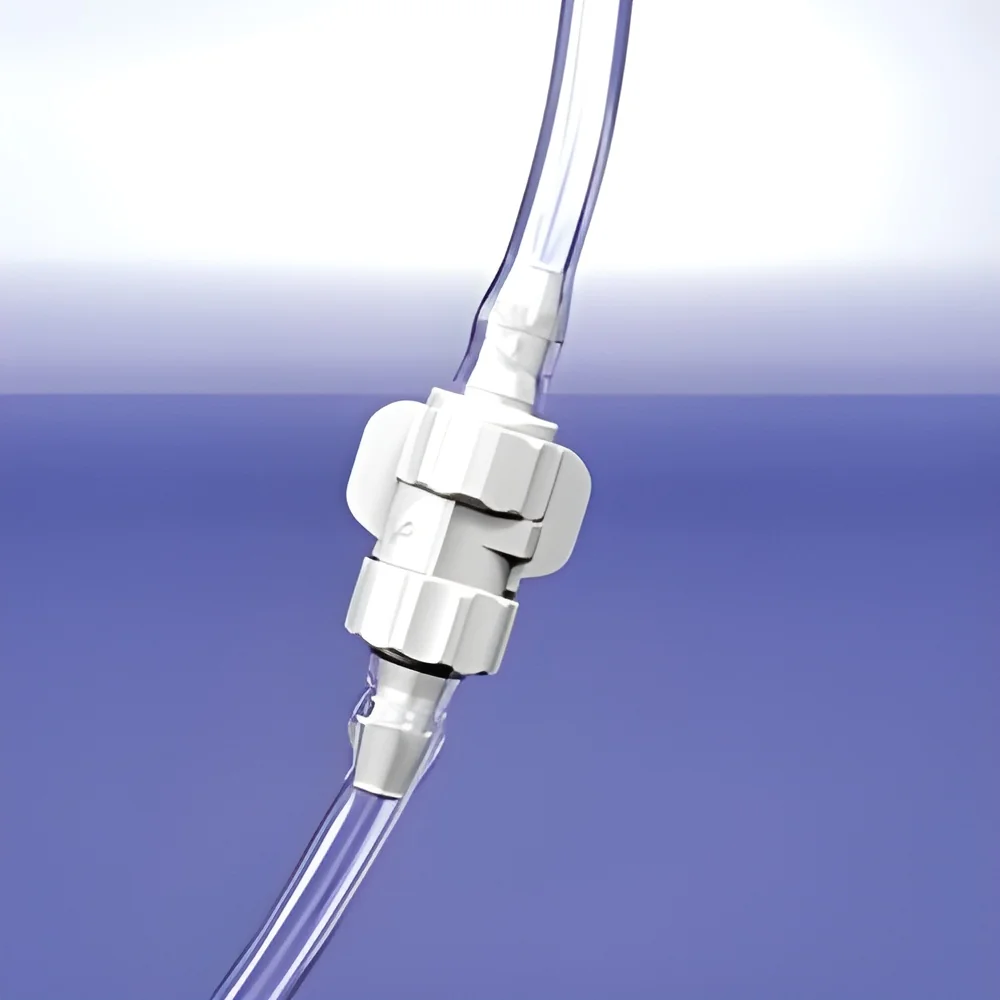
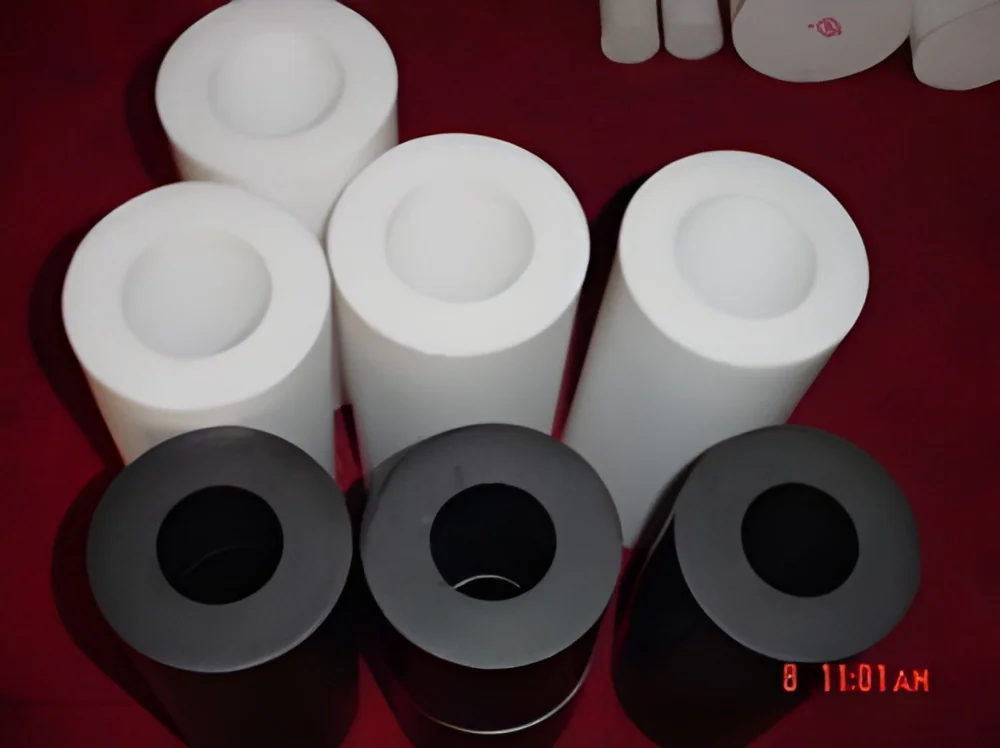
Our Industrial Teflon tubes represent premium-grade PTFE tubing solutions engineered for the most demanding industrial applications. Manufactured from high-quality PTFE material, these tubes offer exceptional chemical resistance capable of handling virtually all aggressive chemicals, acids, and solvents without corrosion or degradation. The material maintains excellent mechanical properties across an extensive temperature range from -200°C to +260°C, ensuring reliable performance in both cryogenic environments and high-heat conditions. The non-stick surface prevents material buildup and facilitates easy cleaning, while the smooth internal bore ensures minimal pressure drop in fluid transfer applications. These tubes are available in various standard sizes and can be customized to meet specific operational requirements.

Multiple critical industries rely on Teflon tubes for operations where material failure could result in significant downtime or safety concerns. The chemical processing...
Our Industrial Teflon tubes represent premium-grade PTFE tubing solutions engineered for the most demanding industrial applications. Manufactured from high-quality PTFE material, these tubes offer exceptional chemical resistance capable of handling virtually all aggressive chemicals, acids, and solvents without corrosion or degradation. The material maintains excellent mechanical properties across an extensive temperature range from -200°C to +260°C, ensuring reliable performance in both cryogenic environments and high-heat conditions. The non-stick surface prevents material buildup and facilitates easy cleaning, while the smooth internal bore ensures minimal pressure drop in fluid transfer applications. These tubes are available in various standard sizes and can be customized to meet specific operational requirements.

Multiple critical industries rely on Teflon tubes for operations where material failure could result in significant downtime or safety concerns. The chemical processing industry utilizes these tubes for transferring corrosive acids, caustic solutions, and aggressive solvents in demanding plant environments. Automotive manufacturers incorporate them in fuel systems, brake lines, and transmission systems where reliability under extreme temperature and pressure conditions is essential. The food processing sector values Teflon tubes for their FDA-compliant, non-contaminating properties in processing equipment and transfer lines. Pharmaceutical companies depend on them for high-purity applications where product integrity and sterility are non-negotiable. Electrical and electronics manufacturers use these tubes for insulating high-voltage components and protecting sensitive wiring from environmental factors.

Businesses choose our Teflon tubes for their proven reliability and long-term operational cost effectiveness. The exceptional durability translates to reduced maintenance expenses and extended service intervals, significantly minimizing production downtime and operational disruptions. Our tubes undergo comprehensive quality control processes to ensure consistent performance and precise dimensional accuracy, providing complete confidence for mission-critical applications. The material's non-aging characteristics guarantee that physical and chemical properties remain stable over time, unlike alternative materials that degrade with exposure to environmental factors. We offer customization capabilities to meet specific application requirements, ensuring perfect compatibility and optimal performance for your unique operational needs.

Key Features:
- Superior chemical resistance to virtually all industrial chemicals and solvents
- Extensive temperature range from -200°C to +260°C for versatile applications
- Excellent dielectric properties providing reliable electrical insulation
- Non-stick surface prevents material adhesion and enables easy maintenance
- Available in custom sizes and configurations for specific requirements

Benefits:
- Long service life reduces replacement frequency and maintenance costs
- Reliable performance in extreme conditions ensures operational continuity
- Non-contaminating properties maintain product purity in sensitive applications
- Versatile compatibility with various chemicals and temperature ranges
- Custom sizing options provide perfect fit for specific application needs
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial Teflon tubes deliver exceptional performance in demanding environments where chemical resistance and thermal stability are critical. These tubes withstand aggressive chemicals, extreme temperatures from -200°C to +260°C, and maintain structural integrity under mechanical stress. Their non-stick properties and purity make them suitable for sanitary applications requiring strict hygiene standards and contamination-free operations across multiple industrial sectors.
These versatile tubes serve reliably in fluid transfer systems, electrical insulation applications, and protective conduit applications where standard materials would deteriorate quickly. Industries depend on Teflon tubes for consistent performance in extreme conditions, from high-purity chemical processing to high-temperature manufacturing operations. The material's excellent dielectric properties make it indispensable for electrical and electronic applications requiring reliable, long-lasting insulation protection.
- Chemical plants for transferring corrosive acids, solvents, and aggressive chemicals
- Automotive systems for fuel lines, brake systems, and hydraulic applications
- Food processing equipment for sanitary fluid transfer and processing lines
- Pharmaceutical manufacturing for high-purity processing and transfer systems
- Electrical industry for wire insulation and component protection in harsh environments
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Arizona Tech- Zeal, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Trading Company•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Teflon Tubes High Temp Chemical Resistance Electrical Insulation
Industrial Teflon tubes provide superior chemical resistance, high-temperature tolerance up to 260°C, and excellent electrical insulation. Ideal for automotive, chemical processing, and food industries. Custom sizes available for specific requirements.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Arizona Tech- Zeal
 Maharashtra, India
Industrial Equipment & MachineryTrading Company