IN
₹
Description
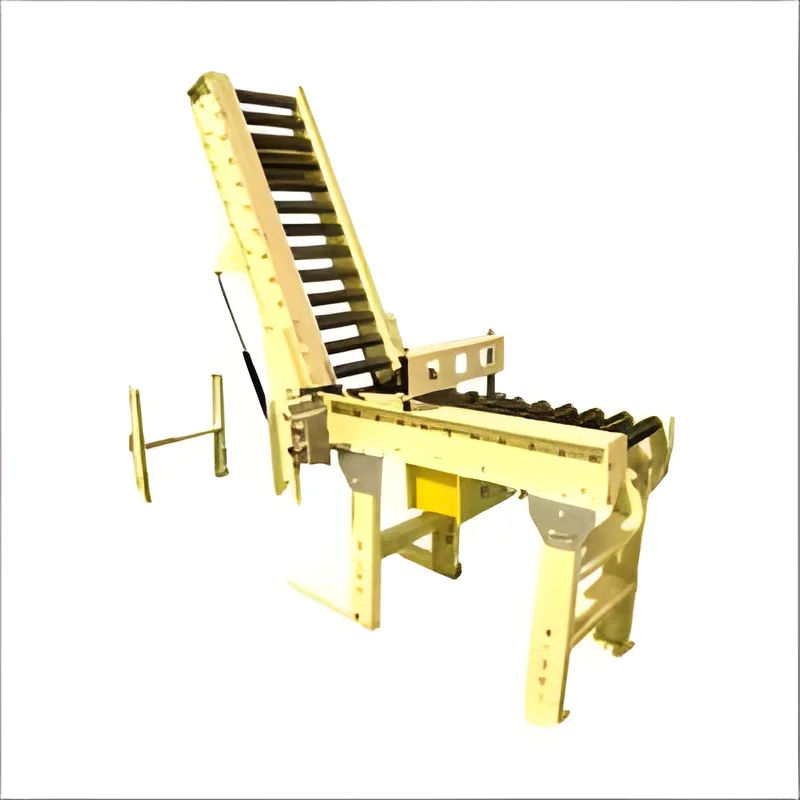
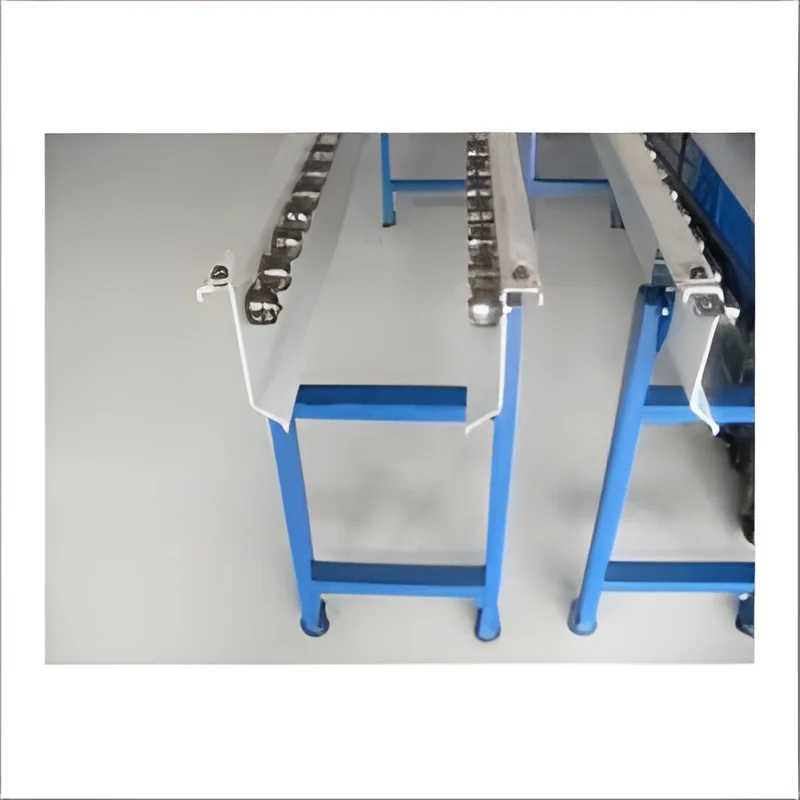
Our warehouse material handling stub roller conveyors represent precision engineering specifically designed for challenging confined spaces. These specialized conveyors feature short rollers that provide optimal support for smaller items while maintaining smooth, consistent transportation flow. Manufactured from premium materials sourced from trusted suppliers, each unit undergoes rigorous quality testing to ensure durability and reliable performance. The compact design allows for straightforward integration into existing systems without requiring extensive modifications, making them an ideal solution for operations seeking to optimize floor space while maintaining efficient material movement. These robust conveyors handle various load capacities while operating quietly and efficiently in demanding industrial environments.

Stub roller conveyors serve critical functions across multiple industries where space optimization is essential. In warehousing and distribution centers, they facil...
Our warehouse material handling stub roller conveyors represent precision engineering specifically designed for challenging confined spaces. These specialized conveyors feature short rollers that provide optimal support for smaller items while maintaining smooth, consistent transportation flow. Manufactured from premium materials sourced from trusted suppliers, each unit undergoes rigorous quality testing to ensure durability and reliable performance. The compact design allows for straightforward integration into existing systems without requiring extensive modifications, making them an ideal solution for operations seeking to optimize floor space while maintaining efficient material movement. These robust conveyors handle various load capacities while operating quietly and efficiently in demanding industrial environments.

Stub roller conveyors serve critical functions across multiple industries where space optimization is essential. In warehousing and distribution centers, they facilitate efficient parcel sorting and temporary accumulation before shipping operations. Manufacturing facilities utilize them for moving components between assembly stations where full-sized conveyors would be impractical. Packaging operations benefit from their ability to handle boxes and containers in tight spaces, while automotive plants rely on them for parts delivery to assembly lines with limited clearance. The food processing industry also employs these conveyors for moving smaller products through quality control stations. Their versatility makes them suitable for any operation requiring dependable material handling in constrained environments.

Investing in our stub roller conveyors delivers significant operational value through improved efficiency and space utilization. These systems reduce manual handling requirements, lowering labor costs and minimizing workplace injuries. The reliability of our conveyors ensures consistent performance with minimal downtime, protecting your production schedules and operational continuity. The robust construction translates to reduced maintenance costs and extended service life, providing excellent long-term value. Operations benefit from enhanced workflow efficiency, superior space management, and improved overall productivity without compromising on performance or reliability.

Key Features:
- Compact short roller design optimized for space-constrained environments
- Premium quality materials ensuring durability and extended service life
- Excellent load bearing capacity with reinforced structural support
- Friction-free roller operation for smooth material handling
- Reliable performance across various industrial applications

Benefits:
- Maximizes space utilization in confined operational areas
- Reduces manual handling requirements and associated labor costs
- Ensures consistent performance with minimal operational downtime
- Provides long service life with reduced maintenance requirements
- Enhances workflow efficiency and overall productivity
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Stub roller conveyors excel in space-limited environments where traditional systems cannot fit. Their compact short-roller design enables seamless integration into existing production lines without major layout changes. These systems handle small to medium items with precision across various industrial operations requiring efficient material transfer in confined areas.
These conveyors prove particularly valuable for operations needing quick transfers between processing stations or temporary accumulation points. The short roller configuration minimizes product contact while maintaining consistent transportation flow. Businesses achieve reduced manual handling and improved workflow efficiency in areas where standard conveyors would be impractical or too expensive to install.
- Order fulfillment centers for parcel sorting and temporary item accumulation
- Manufacturing assembly lines for component transfer between workstations
- Packaging facilities for box and container movement in tight spaces
- Warehouse loading docks for quick item transfer to shipping vehicles
- Automotive plants for parts delivery to assembly stations with limited clearance
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Abhijeet Enterprise, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Manufacturer
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Warehouse Material Handling Stub Roller Conveyors Compact Design
Warehouse stub roller conveyors feature compact design for efficient material handling in tight spaces. Premium quality construction ensures reliable performance for warehouses, manufacturing, and distribution centers with smooth operation and durable components.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Abhijeet Enterprise
 Maharashtra, India
Industrial Equipment & MachineryManufacturer