IN
₹
Apparel & Fashion
Description
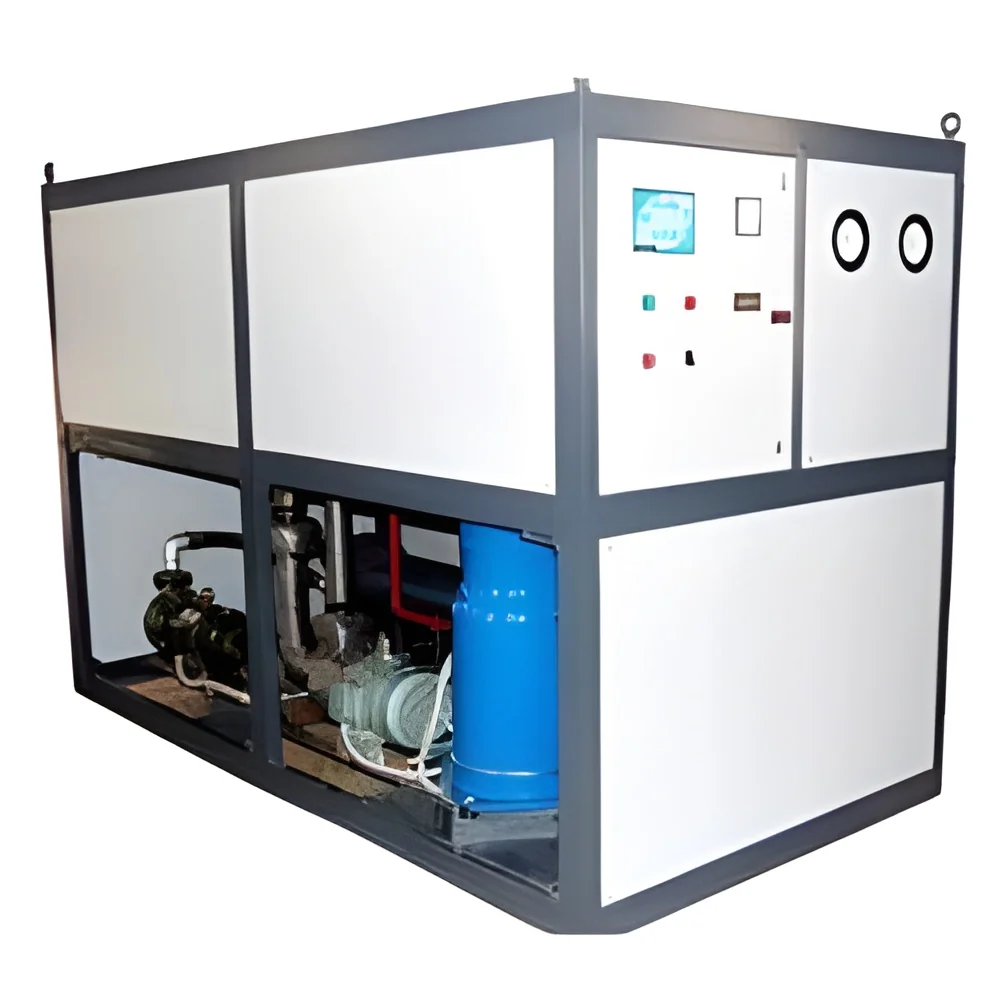
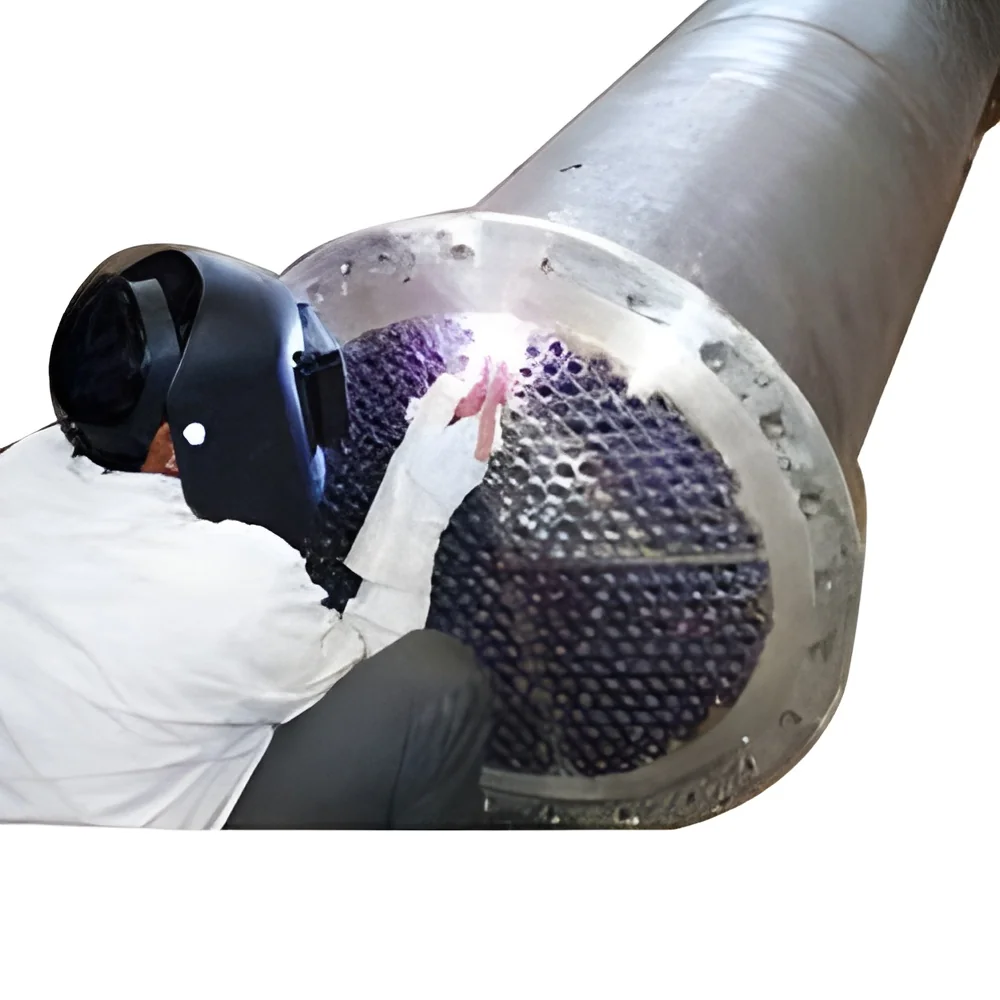
This industrial-grade stainless steel heat exchanger represents the pinnacle of thermal management technology, engineered specifically for demanding industrial applications. Constructed from premium corrosion-resistant materials, it delivers exceptional heat transfer efficiency while maintaining structural integrity under extreme operating conditions. The unit's advanced engineering ensures consistent performance in both heating and cooling applications, with precise temperature control capabilities that meet the most stringent industry requirements. Every component is manufactured to exacting standards, resulting in a reliable thermal management solution that withstands the test of time while optimizing energy usage. The robust construction minimizes maintenance requirements while maximizing operational uptime, making it an indispensable component in critical process systems where thermal management directly impacts productivity and safety.

Multiple industries rely on this heat excha...
This industrial-grade stainless steel heat exchanger represents the pinnacle of thermal management technology, engineered specifically for demanding industrial applications. Constructed from premium corrosion-resistant materials, it delivers exceptional heat transfer efficiency while maintaining structural integrity under extreme operating conditions. The unit's advanced engineering ensures consistent performance in both heating and cooling applications, with precise temperature control capabilities that meet the most stringent industry requirements. Every component is manufactured to exacting standards, resulting in a reliable thermal management solution that withstands the test of time while optimizing energy usage. The robust construction minimizes maintenance requirements while maximizing operational uptime, making it an indispensable component in critical process systems where thermal management directly impacts productivity and safety.

Multiple industries rely on this heat exchanger for their essential thermal management needs. Chemical processing plants utilize it for handling aggressive fluids and maintaining precise temperatures during reactions. Food and beverage manufacturers depend on its hygienic design for pasteurization, cooking, and cooling processes that require strict temperature control. Pharmaceutical companies implement it in sterile manufacturing environments where exact thermal conditions are crucial for product quality. HVAC systems incorporate these units for efficient climate control in large commercial spaces, while power generation facilities use them for heat recovery applications that significantly improve energy efficiency. The versatility and reliability of this heat exchanger make it suitable for virtually any industrial application requiring dependable thermal management.

The business value of this heat exchanger extends far beyond its initial purchase price. Its durable stainless steel construction ensures extended service life with minimal maintenance requirements, significantly reducing total cost of ownership. The high thermal efficiency translates to substantial energy savings over time, lowering operational expenses while supporting sustainability initiatives. Reliability is built into every aspect of the design, with proven performance that minimizes production interruptions and maintenance downtime. The unit's compatibility with various system configurations ensures easy integration into existing operations without requiring extensive modifications. These combined benefits make it a strategic investment that enhances operational efficiency, reduces costs, and supports long-term business growth through dependable thermal management performance.

Key Features:
- Premium stainless steel construction provides exceptional corrosion resistance
- Advanced thermal engineering ensures maximum heat transfer efficiency
- Robust design withstands extreme temperatures and pressure conditions
- Precision manufacturing guarantees consistent performance and reliability
- Compatible with various industrial systems and process requirements

Benefits:
- Extended service life reduces replacement frequency and total cost of ownership
- High energy efficiency lowers operational expenses and utility costs
- Minimal maintenance requirements decrease downtime and service interruptions
- Reliable performance ensures consistent process quality and output
- Versatile application across multiple industries provides flexible usage options
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Stainless steel heat exchangers provide critical thermal management solutions across demanding industrial environments. Their corrosion-resistant construction ensures reliable performance when handling aggressive media, high temperatures, and stringent hygiene requirements. These units maintain consistent heat transfer efficiency in both heating and cooling applications while withstanding challenging operational conditions that would compromise ordinary equipment. The robust design guarantees long service life with minimal maintenance needs, making them ideal for continuous process operations where downtime is not an option. Industries benefit from their adaptability to various system configurations and their ability to maintain precise temperature control in diverse manufacturing processes. Their proven reliability makes them the preferred choice for applications where thermal management directly impacts product quality, safety, and operational efficiency across multiple sectors.
Real-world applications:
- Chemical processing plants utilize these heat exchangers for heating reactive mixtures and cooling processed chemicals safely.
- Food production facilities depend on them for precise temperature control during pasteurization and sterilization processes.
- Pharmaceutical manufacturing employs them in critical sterile processes requiring exact thermal management.
- HVAC systems integrate them for efficient climate control in large commercial and industrial buildings.
- Power generation plants use them for waste heat recovery systems to improve overall energy efficiency.
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
AAB Heat Transfer, Haryana
 Haryana, India
Industrial Equipment & Machinery•Manufacturer•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Stainless Steel Heat Exchanger For Thermal Management
Industrial stainless steel heat exchanger delivers reliable thermal management with superior corrosion resistance and heat transfer efficiency for chemical, food, pharmaceutical, HVAC, and power industries.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
AAB Heat Transfer
 Haryana, India
Industrial Equipment & MachineryManufacturer