IN
₹
Apparel & Fashion
Description
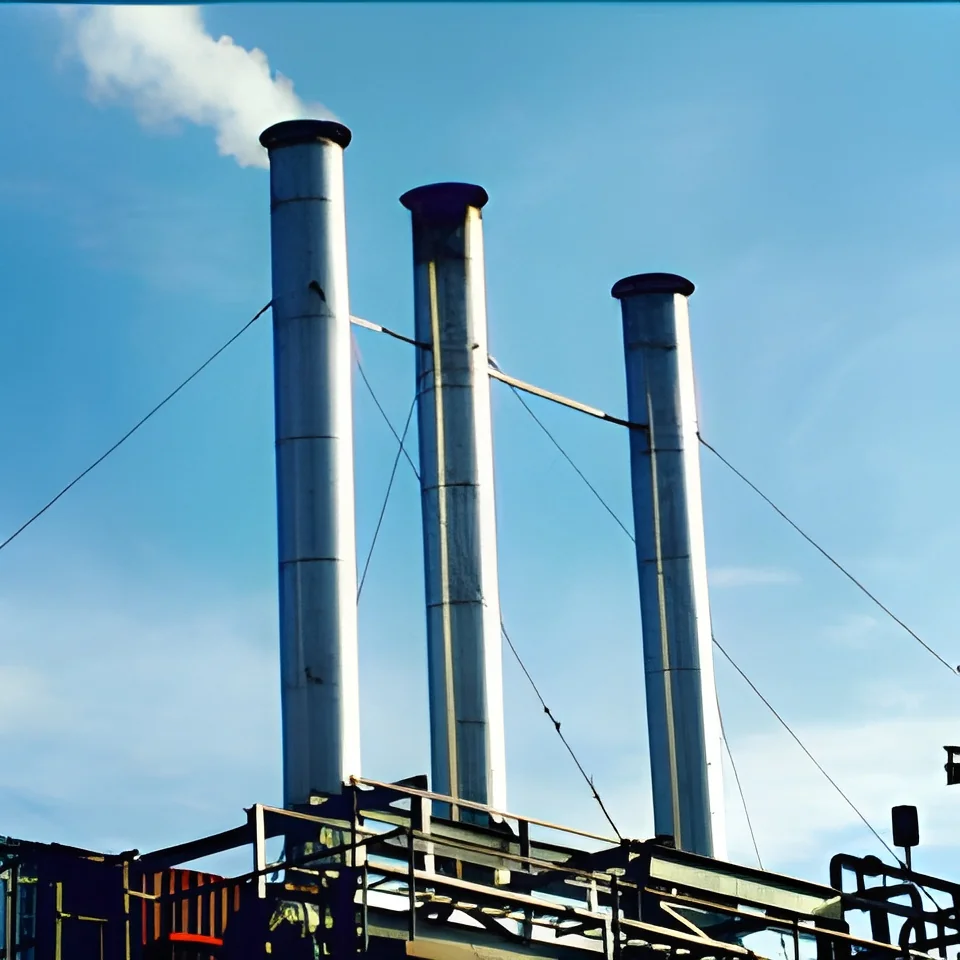
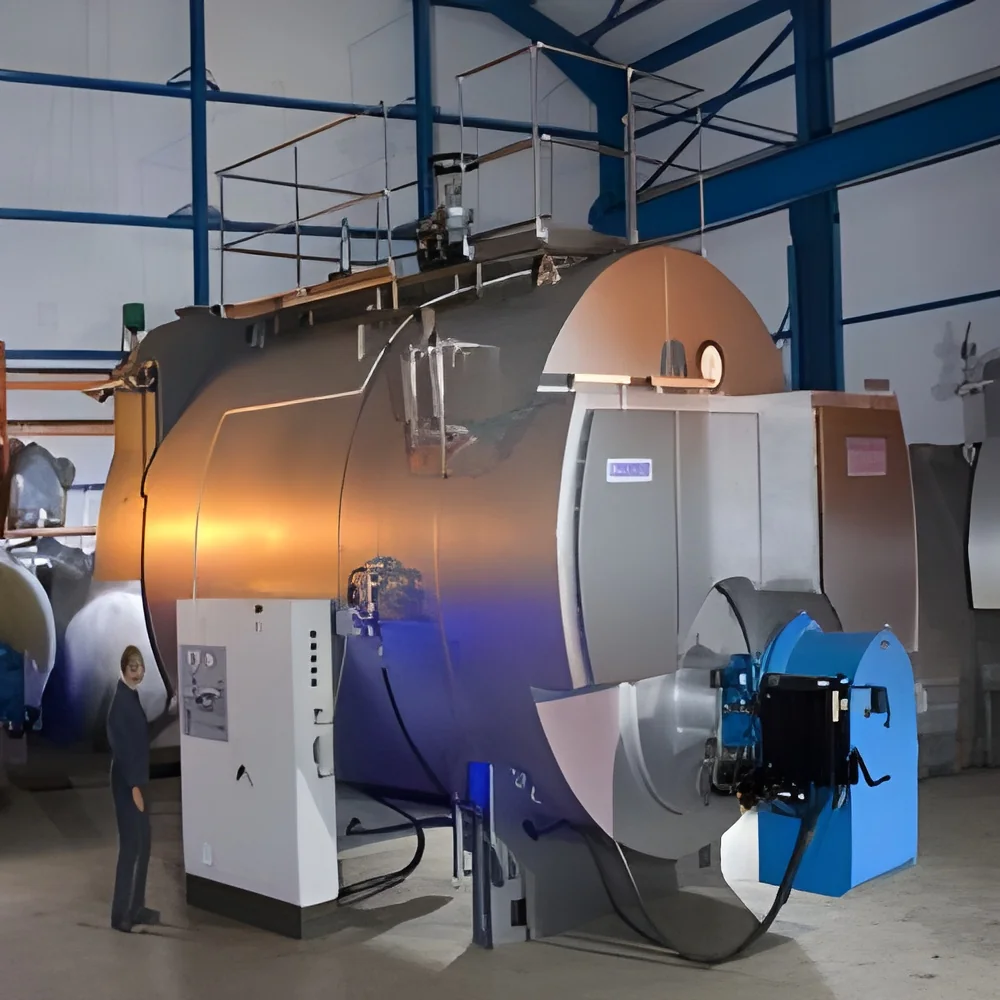
Our industrial stainless steel boilers are premium thermal systems built for demanding applications in food processing and pharmaceutical manufacturing. Constructed from high-grade stainless steel, they offer exceptional resistance to corrosion and scaling, ensuring a long operational life and consistent steam output. Engineered with a focus on durability and efficiency, these boilers are designed to meet the rigorous demands of continuous industrial operation, providing a reliable source of heat and steam for critical processes. Their robust design minimizes maintenance needs, translating to higher uptime and predictable performance for your operations.

These boilers are indispensable in industries where hygiene, purity, and precise thermal control are critical. In food processing, they provide clean steam for cooking, sterilization, and sanitation without risk of contamination. Within pharmaceutical manufacturing, they supply pure steam essential for sterilizing equipment and enviro...
Our industrial stainless steel boilers are premium thermal systems built for demanding applications in food processing and pharmaceutical manufacturing. Constructed from high-grade stainless steel, they offer exceptional resistance to corrosion and scaling, ensuring a long operational life and consistent steam output. Engineered with a focus on durability and efficiency, these boilers are designed to meet the rigorous demands of continuous industrial operation, providing a reliable source of heat and steam for critical processes. Their robust design minimizes maintenance needs, translating to higher uptime and predictable performance for your operations.

These boilers are indispensable in industries where hygiene, purity, and precise thermal control are critical. In food processing, they provide clean steam for cooking, sterilization, and sanitation without risk of contamination. Within pharmaceutical manufacturing, they supply pure steam essential for sterilizing equipment and environments, adhering to strict regulatory standards. The chemical and textile sectors utilize them for consistent heating in reactors and dyeing processes. Their stainless steel construction makes them uniquely suited for these sensitive applications, ensuring product integrity and process reliability across diverse manufacturing landscapes.

The business value lies in superior reliability and a lower total cost of ownership. Investing in these boilers means reduced operational downtime due to their durable construction and minimal maintenance requirements. Their energy-efficient design helps control fuel costs, while their long lifespan protects your capital investment. The inherent quality and compliance with industrial standards mitigate operational risks, ensuring safety and consistency. This combination delivers tangible return on investment through sustained productivity, reduced repair expenses, and dependable performance that supports your core manufacturing processes day in and day out.

Key Features:
- Manufactured from high-grade stainless steel for excellent corrosion and scale resistance.
- Engineered for reliable, consistent steam generation and efficient heat transfer.
- Robust construction ensures durability and a long service life in industrial settings.
- Designed for straightforward operation with low maintenance requirements.
- Built to comply with relevant industrial safety and performance standards.

Benefits:
- Ensures hygienic, contamination-free steam crucial for food and pharmaceutical purity.
- Reduces operational downtime and maintenance costs through durable, reliable design.
- Provides long-term value and protects your investment with an extended operational lifespan.
- Enhances process efficiency and consistency with stable thermal performance.
- Offers peace of mind with built-in reliability and adherence to quality standards.
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our industrial stainless steel boilers are engineered for critical steam and heat applications where hygiene, reliability, and consistent performance are non-negotiable. They excel in environments demanding corrosion resistance and clean operation, supporting continuous processes with minimal downtime. The robust construction ensures stable performance under demanding industrial conditions, making them a dependable core component for thermal systems.
These boilers are specifically designed for industries that require precise temperature control and contamination-free steam. The stainless steel material is ideal for processes where product purity and equipment longevity are paramount. Their adaptability and efficient heat transfer capabilities make them suitable for a wide range of manufacturing and processing applications, providing a solid foundation for operational efficiency.
- Food processing plants for cooking, blanching, sterilization, and cleaning conveyor belts and tanks.
- Pharmaceutical facilities for generating pure steam used in autoclaves, sterilization tunnels, and clean-in-place (CIP) systems.
- Chemical manufacturing units for heating reaction vessels, distillation columns, and maintaining process temperatures.
- Dairy and beverage production for pasteurization processes, bottle washing, and tank heating.
- Textile mills for dyeing vats, fabric drying, and finishing operations requiring consistent heat.
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
B. P. Industries, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Stainless Steel Boilers For Food Processing And Pharmaceuticals
Industrial stainless steel boilers for food processing and pharmaceutical manufacturing deliver reliable steam generation with premium corrosion-resistant construction for durable, low-maintenance operation.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
B. P. Industries
 Maharashtra, India
Industrial Equipment & MachineryManufacturer