IN
₹
Apparel & Fashion
Description
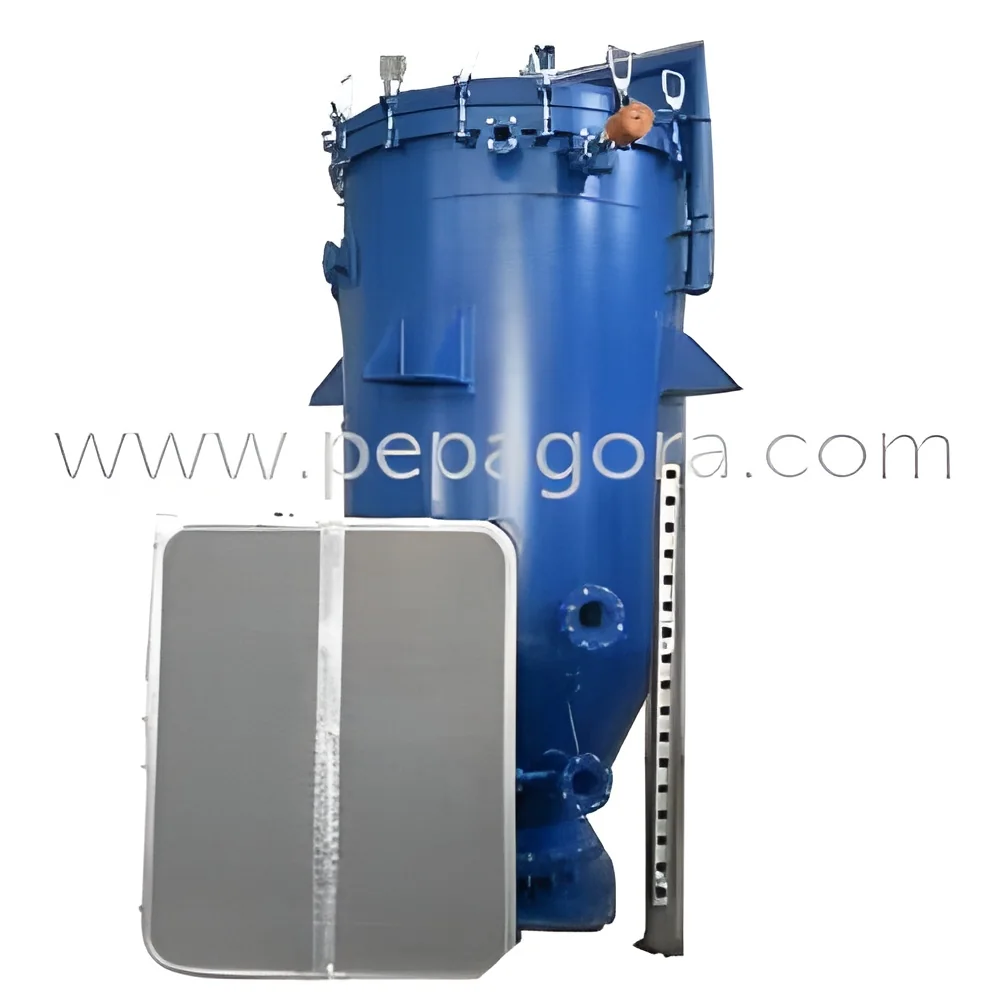
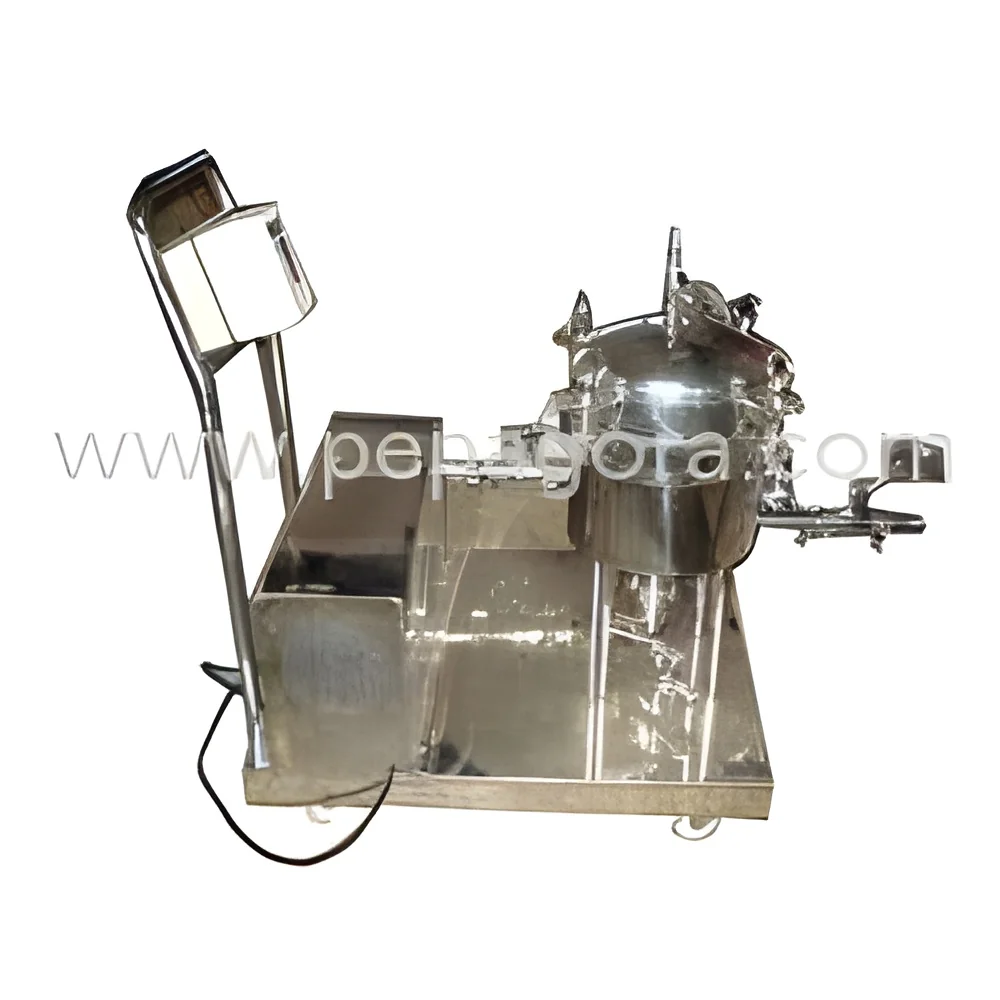
Industrial Sparkler Filters represent advanced filtration technology engineered for demanding industrial environments where purity and reliability are non-negotiable. These filters are constructed with high-quality materials specifically chosen for their durability and chemical resistance, ensuring long-lasting performance even under challenging operational conditions. Designed to deliver exceptional particle retention and clarity improvement, they maintain consistent filtration efficiency across various liquid types, from thin solvents to viscous materials. Their robust build quality and precision engineering make them the preferred choice for businesses that require dependable separation solutions without compromising on process integrity or output quality.

These filters serve essential roles across multiple critical industries, each with unique filtration requirements. In pharmaceutical manufacturing, they ensure sterile filtration and ingredient purification to meet strict regulat...
Industrial Sparkler Filters represent advanced filtration technology engineered for demanding industrial environments where purity and reliability are non-negotiable. These filters are constructed with high-quality materials specifically chosen for their durability and chemical resistance, ensuring long-lasting performance even under challenging operational conditions. Designed to deliver exceptional particle retention and clarity improvement, they maintain consistent filtration efficiency across various liquid types, from thin solvents to viscous materials. Their robust build quality and precision engineering make them the preferred choice for businesses that require dependable separation solutions without compromising on process integrity or output quality.

These filters serve essential roles across multiple critical industries, each with unique filtration requirements. In pharmaceutical manufacturing, they ensure sterile filtration and ingredient purification to meet strict regulatory standards. Food and beverage processors rely on them for contamination removal and clarity improvement to maintain product quality and safety. Chemical production facilities utilize sparkler filters for catalyst recovery and product purification processes. The varnish and resin industries depend on them for quality enhancement and impurity removal, while metal finishing operations use them for bath maintenance and particle control in electroplating solutions. Each application benefits from the filter's ability to handle specific operational challenges while maintaining consistent performance.

The business value of Industrial Sparkler Filters lies in their proven reliability, operational efficiency, and long-term cost-effectiveness. These filters reduce operational downtime through robust construction and straightforward maintenance procedures, ensuring continuous production flow. Their consistent filtration performance protects downstream equipment from contamination damage while ensuring final product quality meets exacting standards. The global recognition of sparkler filter technology provides assurance of proven performance across diverse industrial applications. This reliability translates into reduced operating costs, improved process efficiency, and enhanced product quality, making them a strategic investment for businesses focused on optimizing their filtration processes and maintaining competitive advantage in quality-conscious markets.

Key Features:
- High-quality construction materials ensuring superior durability and chemical resistance
- Exceptional particle retention capabilities for high-purity filtration requirements
- Designed to withstand high-pressure operational conditions without performance degradation
- Effective handling of viscous fluids and challenging industrial materials
- Precision engineering for consistent filtration efficiency and clarity improvement

Benefits:
- Reduced operational downtime through robust construction and reliable performance
- Consistent filtration results that protect downstream equipment and ensure product quality
- Long-term cost-effectiveness through durable materials and efficient operation
- Enhanced process efficiency with reliable separation technology
- Proven performance across diverse industrial applications and challenging environments
Specifications
| Key Attributes | |
|---|---|
| Type | Filtration |
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Sparkler filters deliver critical high-purity liquid filtration where contamination control is essential. These systems handle viscous fluids, chemicals, and food-grade products while maintaining consistent performance under high-pressure conditions, ensuring process integrity and safety compliance across diverse manufacturing environments. Their robust construction and precise particle retention capabilities make them ideal for applications requiring clarity maintenance and reliable separation. The versatile design supports both batch and continuous operations, providing consistent output quality for industries that cannot compromise on filtration standards or product purity.
Real-world applications:
- Pharmaceutical ingredient purification and sterile filtration processes
- Food and beverage processing for clarity improvement and contamination removal
- Chemical manufacturing for catalyst recovery and product purification
- Varnish and resin filtration for quality enhancement and impurity removal
- Electroplating and metal finishing solutions for bath maintenance and particle control
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile

Sruthi Agro Process, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Manufacturer•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
Eastern Asia
Western Europe
Africa
Industrial Sparkler Filters For High Purity Liquid Filtration
Industrial Sparkler Filters provide high-purity liquid filtration for pharmaceuticals, chemicals, and food processing. These robust filters ensure reliable performance, superior particle retention, and durability in demanding industrial applications.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Sruthi Agro Process
 Maharashtra, India
Industrial Equipment & MachineryManufacturer