IN
₹
Apparel & Fashion
Description
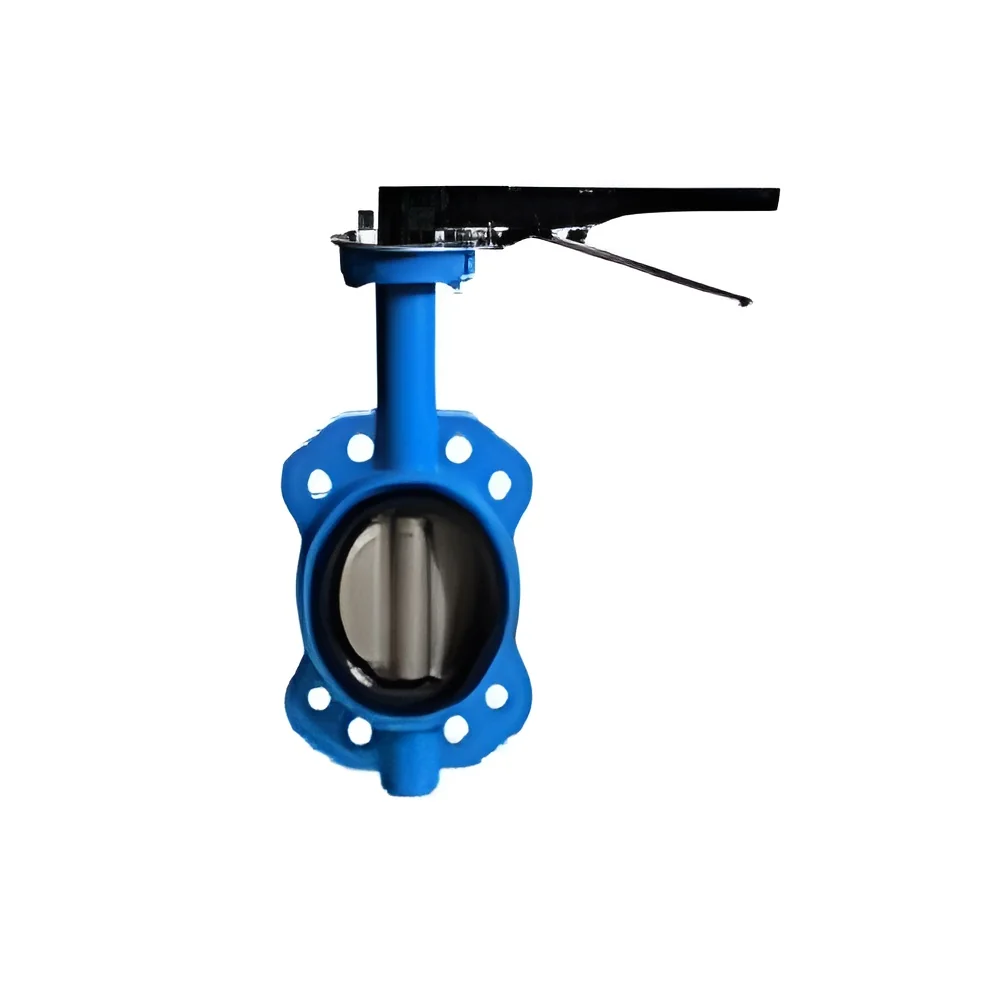
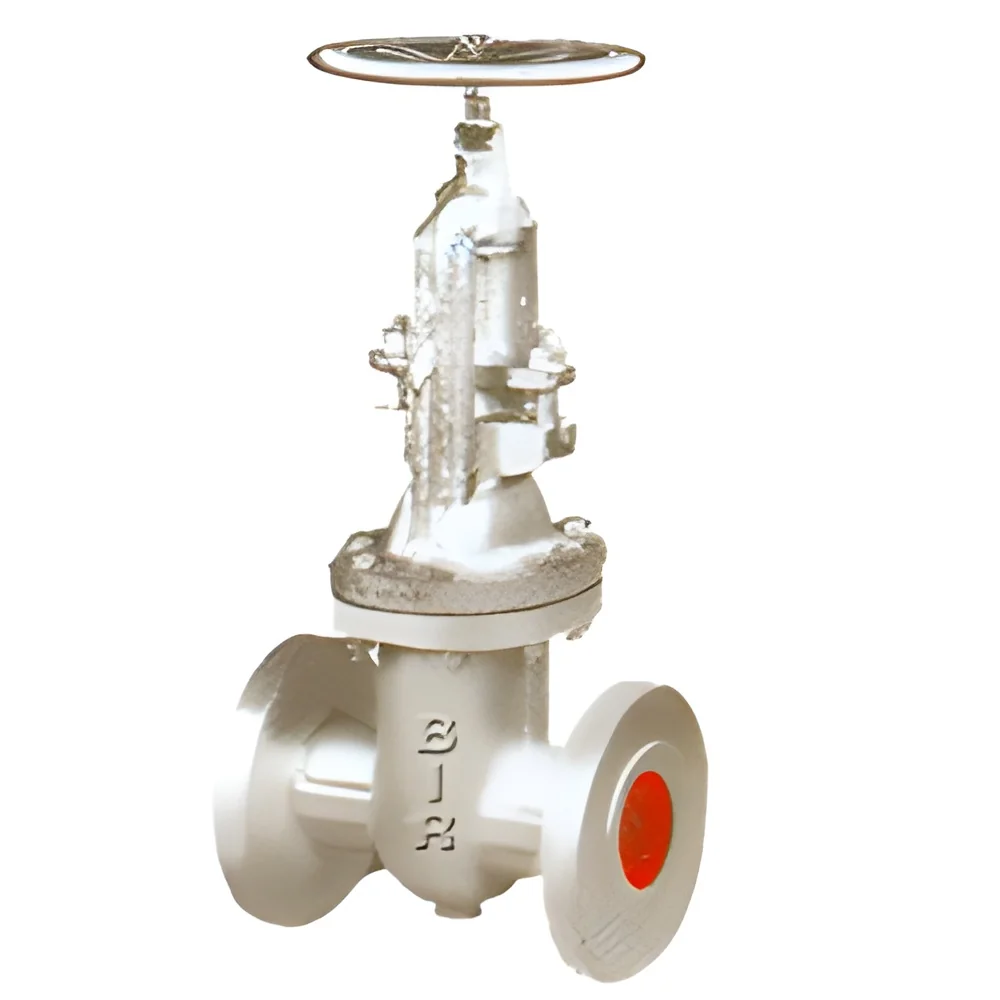
Industrial motorized sluice valves represent advanced flow control technology engineered specifically for demanding chemical and process industry applications. Manufactured using high-grade materials and precision engineering, these valves ensure reliable performance in challenging industrial environments. As a leading manufacturer from India, we maintain stringent quality standards throughout production, resulting in products that meet international specifications while exceeding performance expectations. The motorized operation provides seamless remote control capabilities, while the robust construction guarantees longevity and minimal maintenance requirements across various industrial settings and operating conditions.

These motorized sluice valves find extensive application across multiple industries where precise flow control is critical to operational success. In chemical and process industries, they handle aggressive chemicals, solvents, and corrosive media with exceptional res...
Industrial motorized sluice valves represent advanced flow control technology engineered specifically for demanding chemical and process industry applications. Manufactured using high-grade materials and precision engineering, these valves ensure reliable performance in challenging industrial environments. As a leading manufacturer from India, we maintain stringent quality standards throughout production, resulting in products that meet international specifications while exceeding performance expectations. The motorized operation provides seamless remote control capabilities, while the robust construction guarantees longevity and minimal maintenance requirements across various industrial settings and operating conditions.

These motorized sluice valves find extensive application across multiple industries where precise flow control is critical to operational success. In chemical and process industries, they handle aggressive chemicals, solvents, and corrosive media with exceptional resistance to degradation. Water treatment facilities utilize them for main supply lines and distribution networks due to their reliable shut-off capabilities and durability. Manufacturing plants integrate them into process water systems, while power generation facilities depend on them for feedwater and cooling circuit management. The mining sector employs these valves for slurry handling applications, demonstrating their versatility across diverse operational requirements and challenging media conditions.

The value of these motorized sluice valves extends beyond basic functionality to encompass significant operational efficiency and cost-effectiveness benefits. Their proven reliability reduces system downtime and maintenance costs, while the motorized operation enables seamless automation integration for improved process control and operational safety. The precision engineering ensures optimal performance in your specific environment, enhancing system reliability while maintaining project schedules and budgetary requirements. These valves are designed to deliver consistent performance under demanding conditions, providing long-term value through reduced operational costs and enhanced process control capabilities.

Key Features:
- Motorized operation enabling remote control and automation system integration
- High-grade materials construction providing superior corrosion resistance and durability
- Precision engineering ensuring reliable shut-off and precise flow control capabilities
- Robust design suitable for high-pressure and high-temperature applications
- Manufactured according to international quality standards and specifications

Benefits:
- Reduced operational downtime through reliable performance and minimal maintenance
- Enhanced process control with precise flow regulation and remote operation capabilities
- Long service life due to corrosion-resistant materials and robust construction
- Improved safety through reliable shut-off and automated control features
- Cost-effective operation with minimal maintenance requirements and energy efficiency
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial motorized sluice valves deliver precise flow control in demanding chemical processing and industrial environments. These robust valves ensure reliable shut-off and regulation for liquids, slurries, and aggressive chemicals across various pressure conditions. The durable construction guarantees long-term performance in corrosive or high-temperature applications where standard valves would fail, maintaining system integrity and operational safety throughout extended service life.
These motorized valves serve critical functions in chemical plants, water treatment facilities, and industrial manufacturing systems. The automated operation enables remote control and seamless integration with modern industrial automation systems, making them ideal for facilities prioritizing efficiency and safety. They maintain consistent performance in both high-pressure and low-pressure scenarios, ensuring reliable operation across diverse industrial requirements and challenging media handling applications.
- Chemical processing plants for controlling acid, solvent, and chemical flow lines
- Water treatment facilities managing main supply networks and distribution systems
- Industrial manufacturing plants handling process water and cooling circuits
- Power generation facilities for feedwater control and cooling water management
- Mining operations for slurry transport systems and processing applications
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Bir Industries, Punjab
 Punjab, India
Industrial Equipment & Machinery•Manufacturer•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Motorized Sluice Valves For Chemical Process Flow Control
Industrial motorized sluice valves provide reliable chemical process flow control with high-grade materials, precision engineering, and motorized operation for automation integration from India's leading manufacturer.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Bir Industries
 Punjab, India
Industrial Equipment & MachineryManufacturer