IN
₹
Description
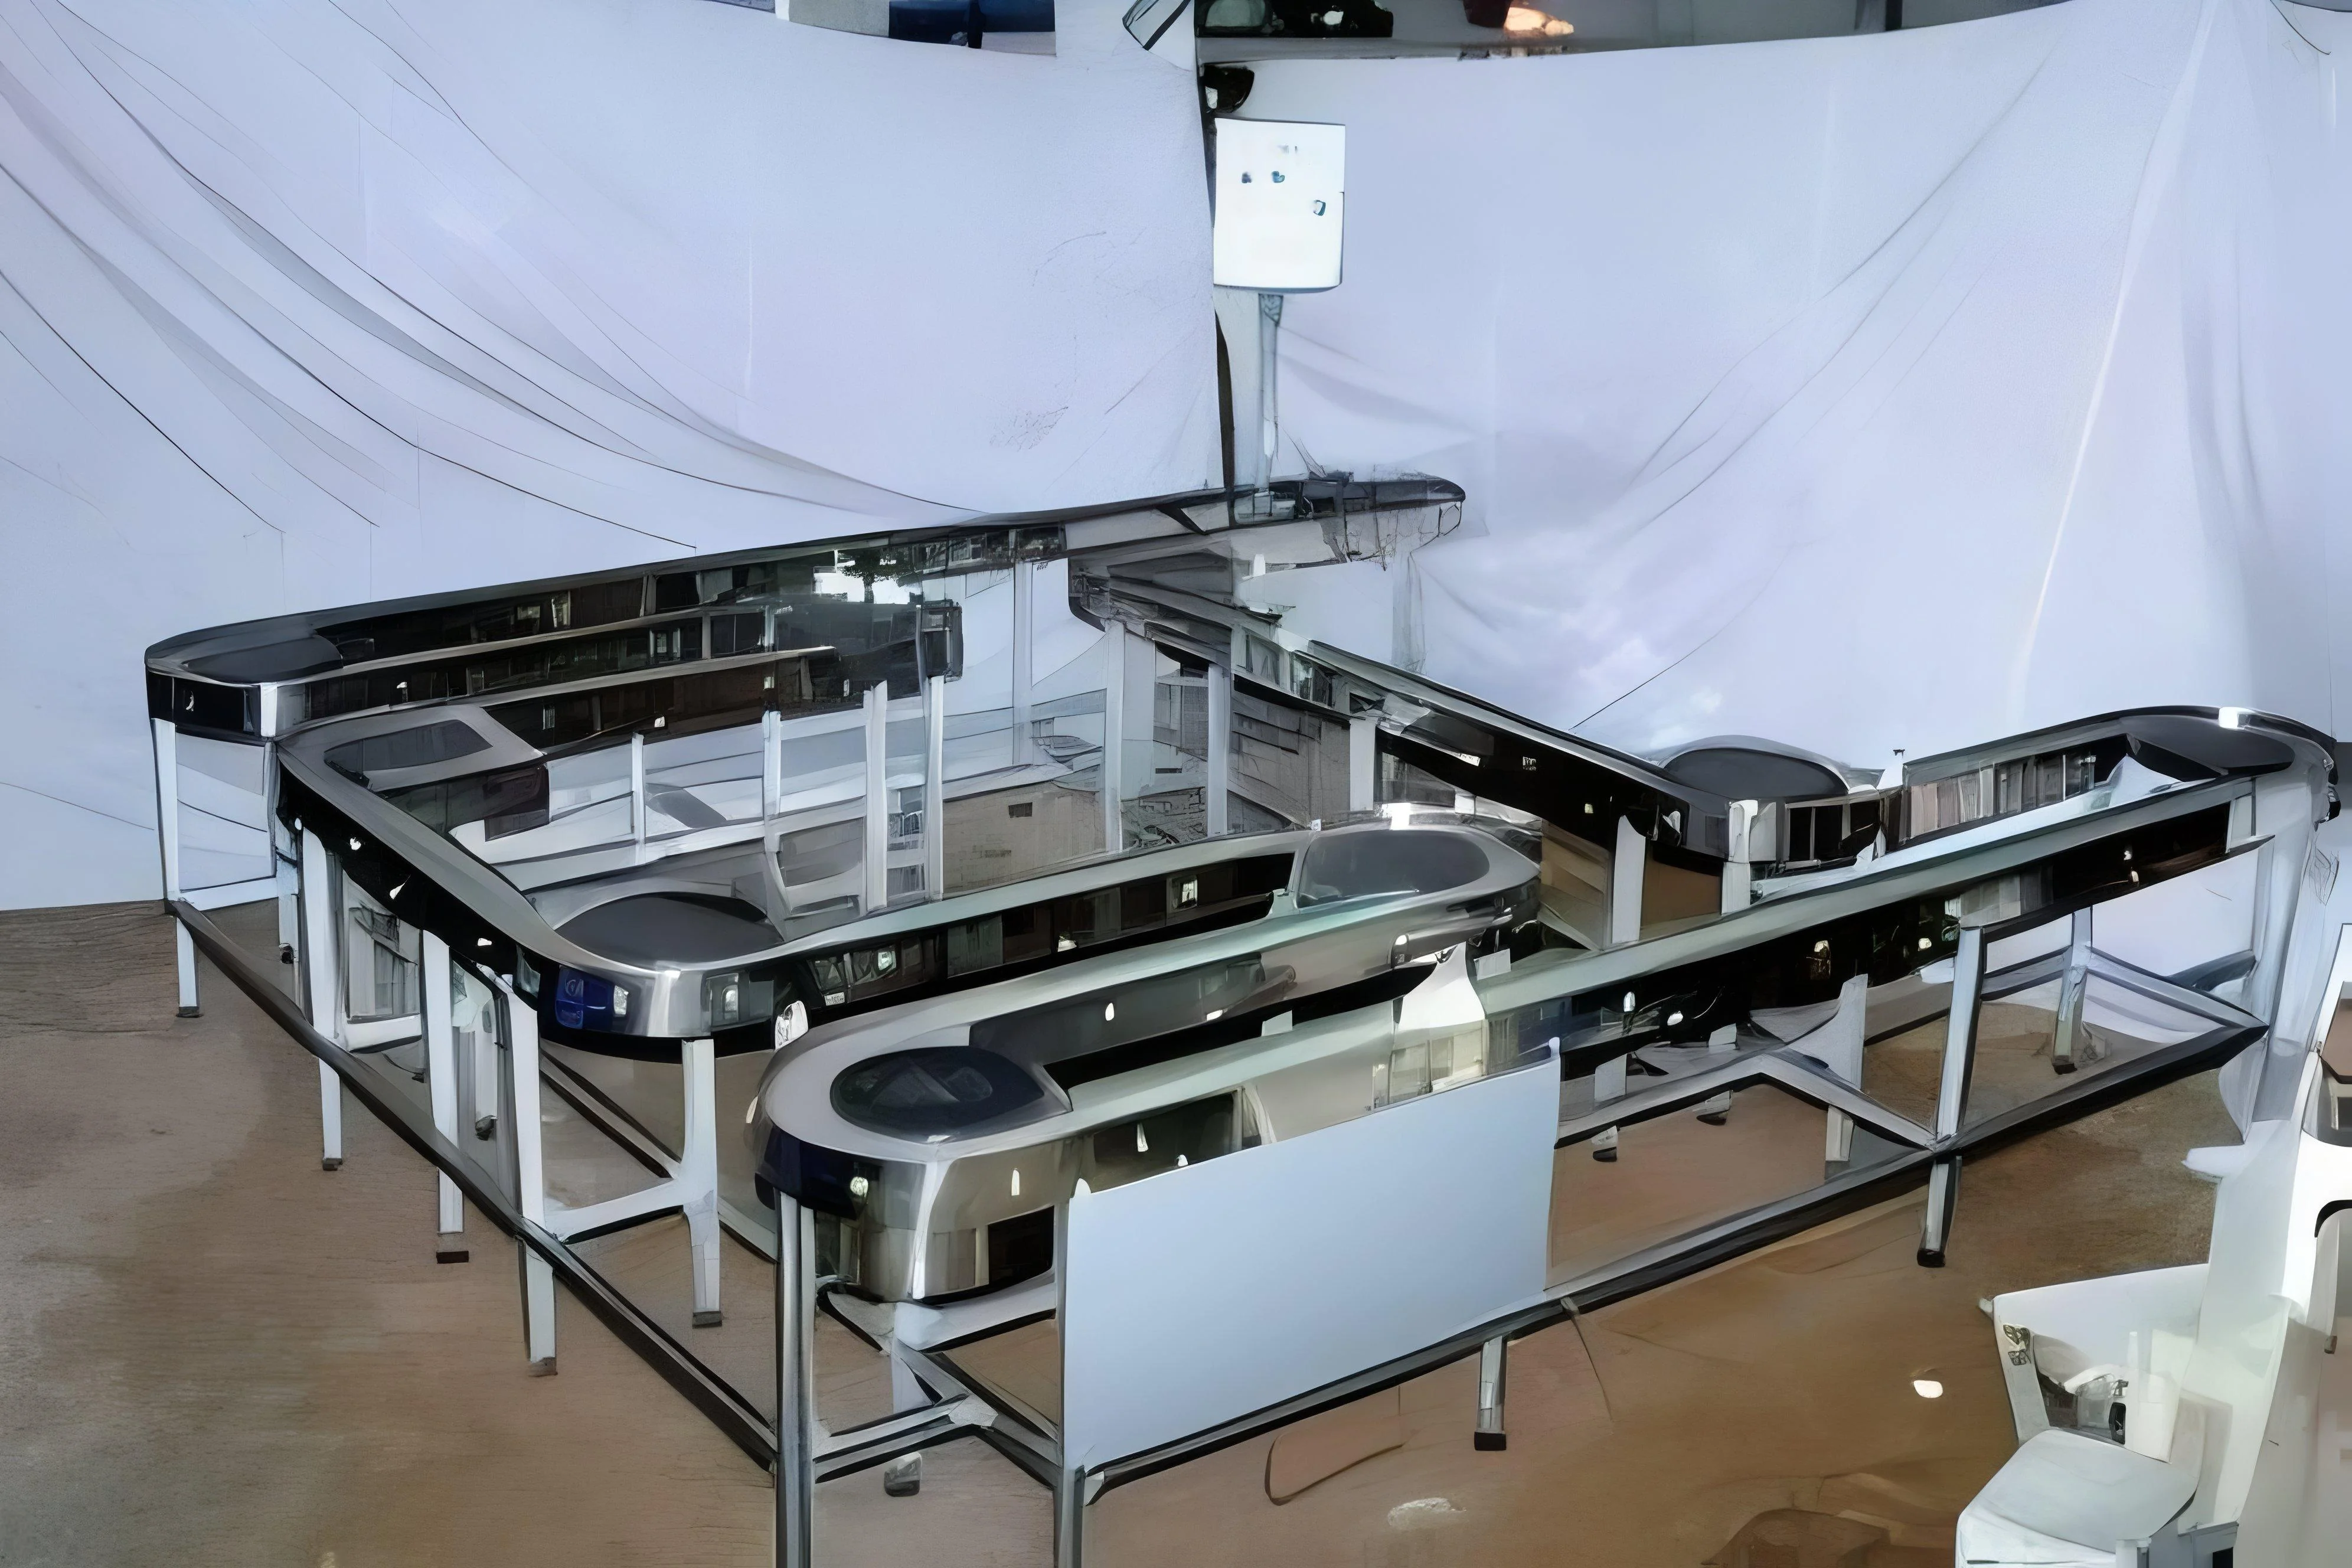
Industrial heavy duty slat chain conveyors represent premium material handling solutions designed for the most demanding industrial applications that require robust performance and exceptional reliability. These conveyors feature rugged construction and high-capacity engineering specifically developed to transport bulky, abrasive, or heavy items with maximum efficiency and minimal operational downtime. The systems ensure perfect adaptation to specific layout requirements, capacity needs, and environmental conditions, making them ideal for various industrial settings. Built with precision engineering and superior quality components, these conveyors offer seamless integration into existing operations while delivering performance that consistently exceeds industry standards for material handling equipment.

These slat chain conveyors serve essential roles across multiple industrial sectors including manufacturing, processing, and logistics operations. In airport facilities, they form the ...
Industrial heavy duty slat chain conveyors represent premium material handling solutions designed for the most demanding industrial applications that require robust performance and exceptional reliability. These conveyors feature rugged construction and high-capacity engineering specifically developed to transport bulky, abrasive, or heavy items with maximum efficiency and minimal operational downtime. The systems ensure perfect adaptation to specific layout requirements, capacity needs, and environmental conditions, making them ideal for various industrial settings. Built with precision engineering and superior quality components, these conveyors offer seamless integration into existing operations while delivering performance that consistently exceeds industry standards for material handling equipment.

These slat chain conveyors serve essential roles across multiple industrial sectors including manufacturing, processing, and logistics operations. In airport facilities, they form the backbone of baggage handling systems, ensuring smooth and reliable passenger luggage transport. Chemical and pharmaceutical plants depend on them for moving raw materials and finished products through complex processing lines. The automotive industry utilizes these conveyors for assembly line parts handling, while glass and ceramic manufacturers rely on them for transporting fragile yet heavy materials. Food and beverage operations benefit from their efficient packaging handling capabilities, making them versatile solutions for diverse industrial applications that demand reliable material movement.

The operational value of these slat chain conveyors lies in their ability to significantly improve processing efficiency while reducing handling costs and manual labor requirements. Their reliable performance in harsh industrial environments ensures continuous operation, minimizing production interruptions and maintenance needs. The engineering allows businesses to optimize the systems for their specific operational requirements, ensuring optimal space utilization and workflow integration. With durable construction that guarantees extended service life and minimal downtime, these conveyors represent a strategic investment that delivers consistent returns through improved productivity, reduced operational costs, and enhanced material handling capabilities that support operational excellence.

Key Features:
- Rugged steel construction for heavy-duty applications and extended operational lifespan
- High capacity design capable of handling bulky and abrasive materials efficiently
- Simplified maintenance system that reduces downtime and service requirements
- Adaptable configurations to accommodate specific space and layout requirements
- Compatibility with various chain types and drive systems for operational flexibility

Benefits:
- Enhanced operational efficiency through reliable continuous material transport
- Reduced labor costs by minimizing manual handling requirements
- Lower maintenance costs with durable construction and simplified service access
- Improved workflow integration through adaptable design configurations
- Long-term reliability ensuring consistent performance in demanding environments
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial heavy duty slat chain conveyors are engineered for moving heavy, abrasive, or oversized materials through demanding operational environments. They deliver consistent material flow that supports continuous production processes while significantly reducing manual handling requirements. These conveyor systems excel where maximum durability and reliability are essential for operational success and long-term performance sustainability across various industrial settings.
These robust conveyor systems serve critical functions across multiple sectors, handling diverse materials from luggage and chemicals to automotive parts and packaged goods. Their consistent performance and minimal maintenance requirements make them ideal for continuous operation environments where downtime must be minimized. The conveyors adapt to various industrial layouts and material types, ensuring smooth transportation through different processing stages while maintaining operational efficiency and reliability.
- Airport baggage handling and cargo transport systems for efficient luggage movement
- Chemical and pharmaceutical processing lines handling raw materials and products
- Glass, ceramic, and building material manufacturing transporting heavy fragile items
- Automotive assembly plants moving components through production lines
- Food and beverage packaging operations for efficient product handling
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
M S International Corporation, Haryana
 Haryana, India
Industrial Equipment & Machinery•Manufacturer•Trading Company
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
South Asia
Industrial Heavy Duty Slat Chain Conveyors For Material Handling
Industrial heavy duty slat chain conveyors from leading manufacturers provide robust material handling for demanding environments, featuring high-capacity transport of heavy bulky items with exceptional durability and reliability across manufacturing and processing facilities.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
M S International Corporation
 Haryana, India
Industrial Equipment & MachineryManufacturer