IN
₹
Apparel & Fashion
Description
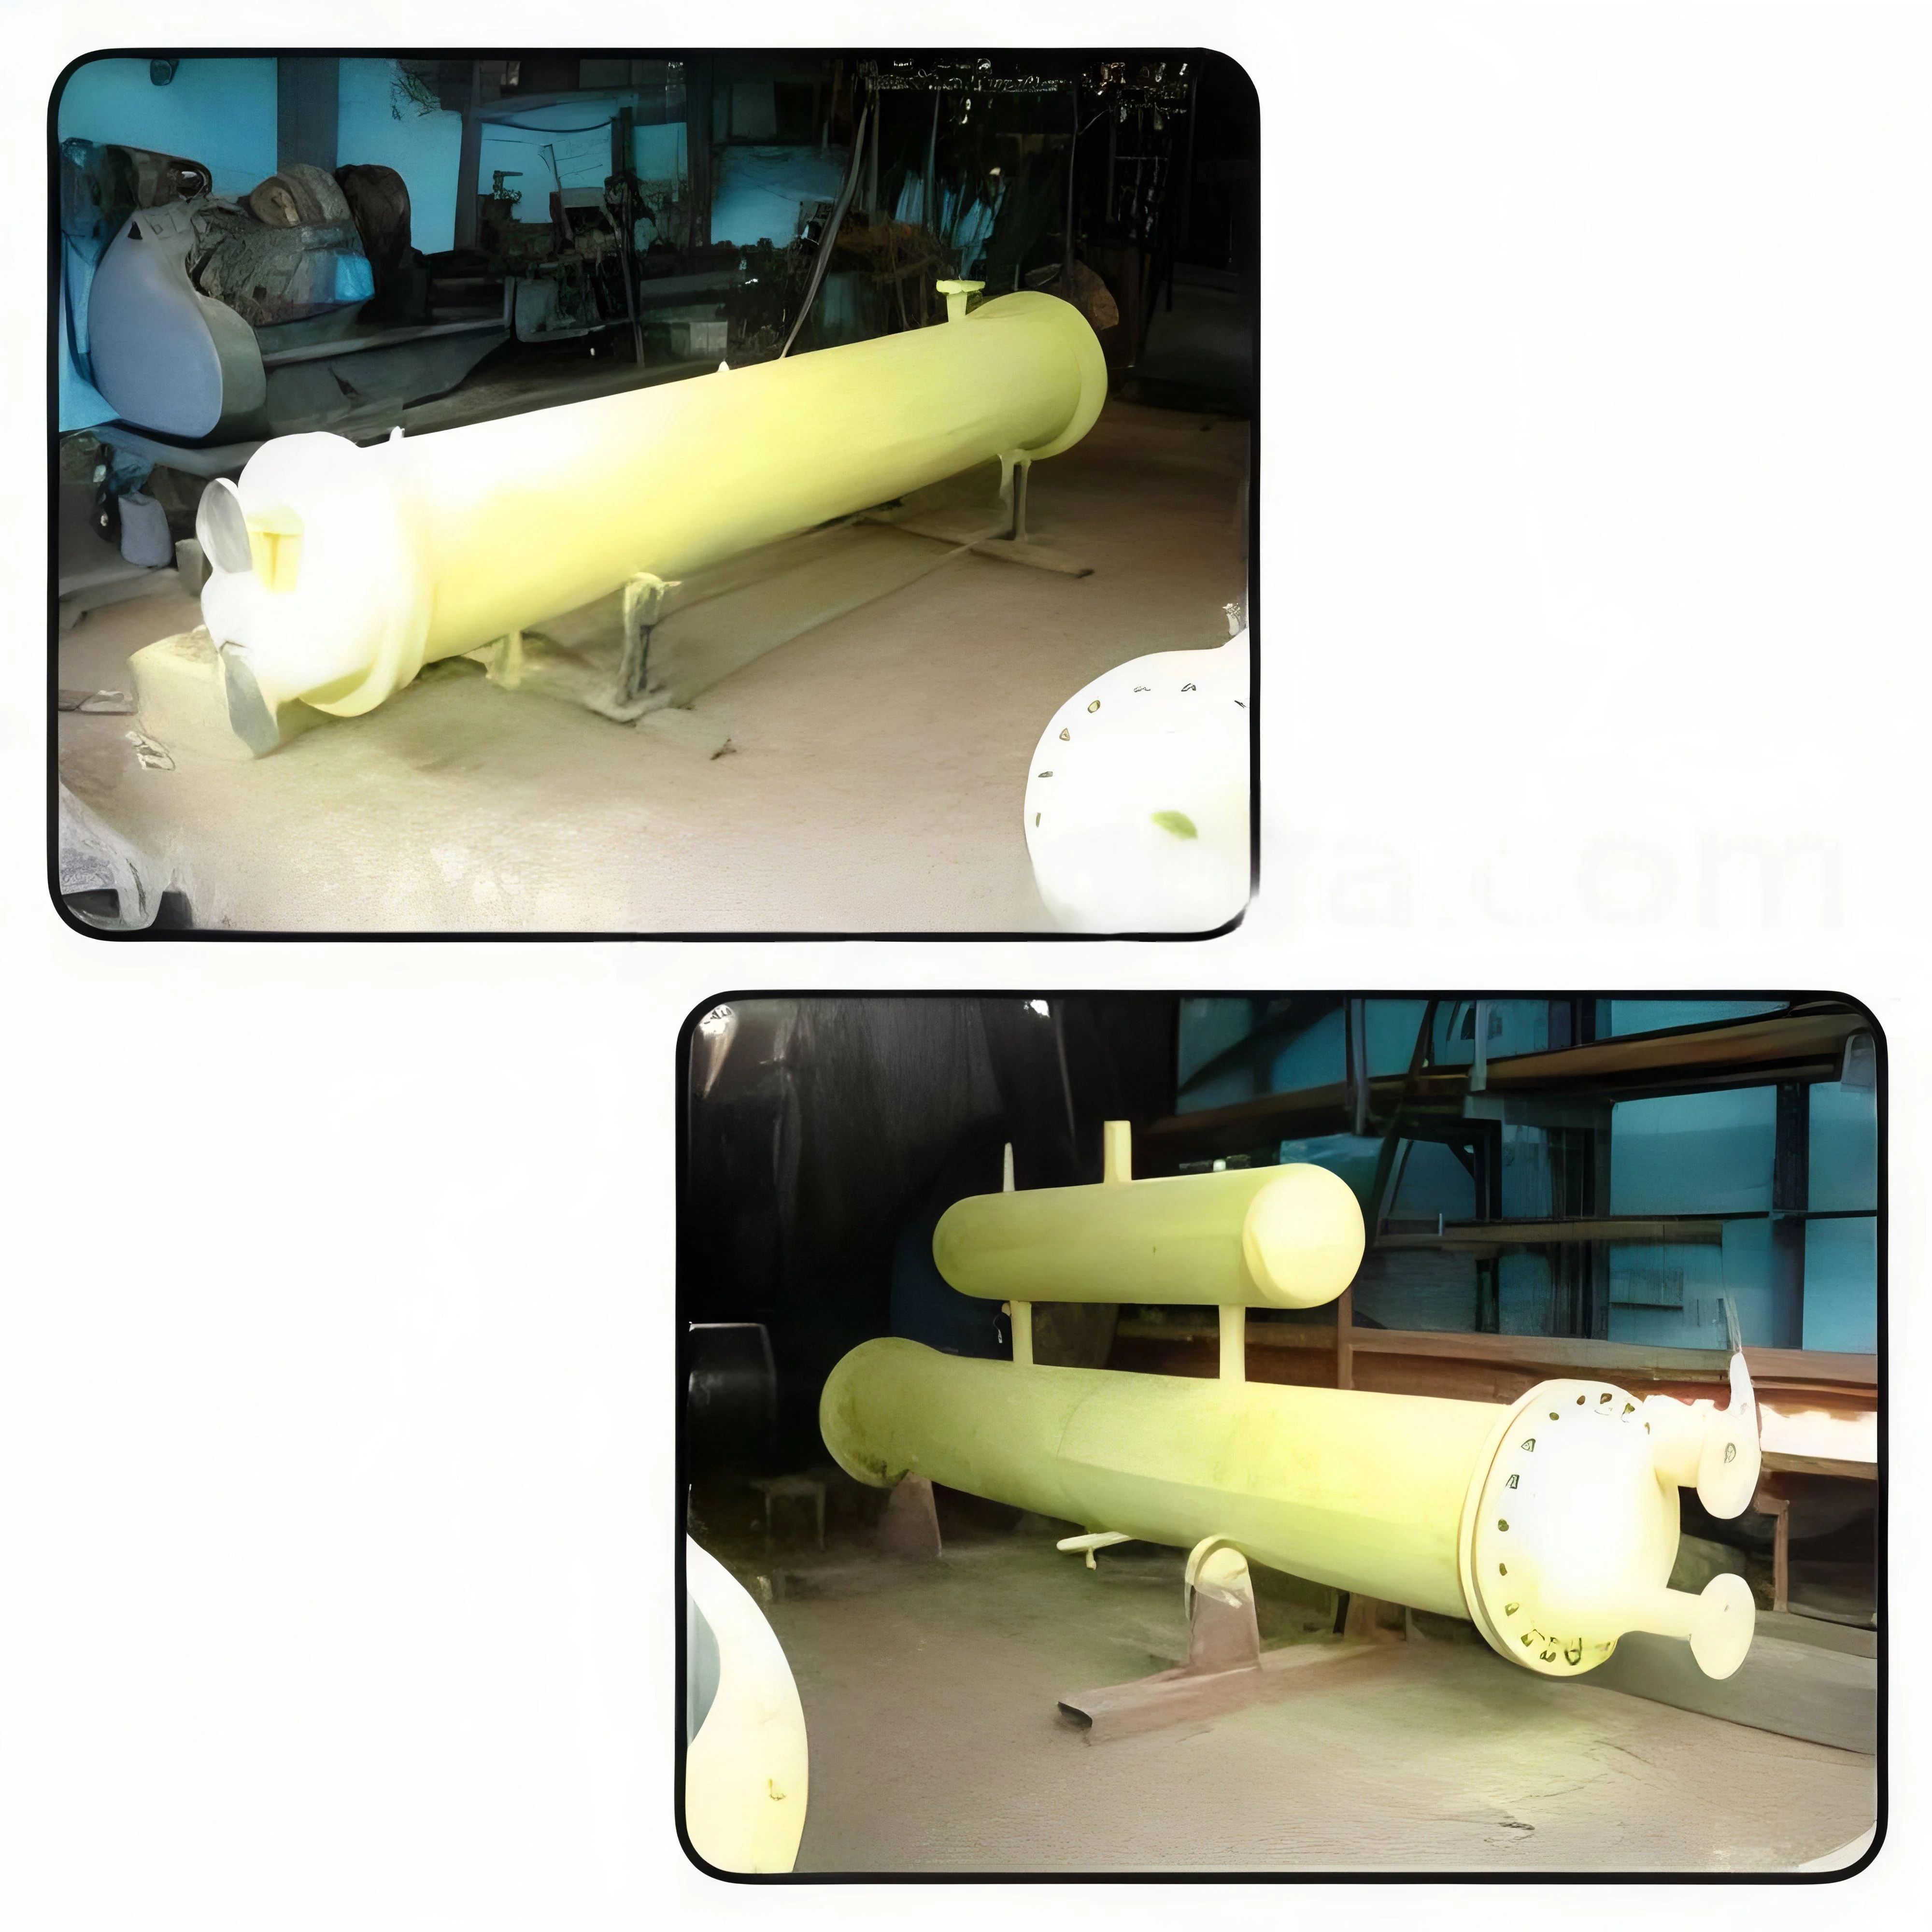
Industrial shell and tube condensers represent advanced thermal management solutions engineered for superior heat transfer efficiency in demanding industrial environments. These units feature precision engineering to match specific operational requirements, ensuring optimal performance under varying pressure and temperature conditions. Constructed with advanced fabrication techniques and high-quality materials, they deliver reliable thermal management for critical cooling applications across multiple industries, providing consistent results and long-term operational stability while maintaining energy efficiency throughout their service life. The robust design ensures dependable performance even in the most challenging industrial settings, making them a trusted choice for professionals seeking reliable cooling solutions.

These condensers find extensive application across diverse industrial sectors including HVAC systems for large commercial spaces, refrigeration plants in food processi...
Industrial shell and tube condensers represent advanced thermal management solutions engineered for superior heat transfer efficiency in demanding industrial environments. These units feature precision engineering to match specific operational requirements, ensuring optimal performance under varying pressure and temperature conditions. Constructed with advanced fabrication techniques and high-quality materials, they deliver reliable thermal management for critical cooling applications across multiple industries, providing consistent results and long-term operational stability while maintaining energy efficiency throughout their service life. The robust design ensures dependable performance even in the most challenging industrial settings, making them a trusted choice for professionals seeking reliable cooling solutions.

These condensers find extensive application across diverse industrial sectors including HVAC systems for large commercial spaces, refrigeration plants in food processing and preservation, chemical manufacturing facilities requiring precise temperature control, power generation stations for steam condensation, and oil and gas processing units handling hydrocarbon fluids. Their versatile design makes them ideal for applications requiring efficient heat exchange, reliable condensation performance, and durable operation in challenging industrial environments where temperature management and process efficiency are crucial for successful operations and regulatory compliance. Each sector benefits from tailored performance characteristics that address specific thermal management needs.

The business value of our shell and tube condensers lies in their exceptional reliability, reduced maintenance requirements, and engineered configurations that ensure perfect system integration. These units offer excellent return on investment through enhanced energy efficiency, minimal operational downtime, and extended service life, making them a smart choice for businesses seeking quality thermal solutions without compromising on performance or durability. Their proven track record in demanding applications provides peace of mind for operators who require consistent performance and long-term value from their industrial equipment investments, ensuring operational continuity and cost-effective thermal management solutions.

Key Features:
- High-efficiency heat transfer design for optimal thermal performance
- Robust construction using quality materials for durability and longevity
- Capability to handle high pressure and temperature operating conditions
- Advanced fabrication techniques ensuring reliability and consistent performance
- Precision engineering to meet specific operational requirements and system specifications

Benefits:
- Enhanced energy efficiency reducing operational costs
- Minimal maintenance requirements and extended service life
- Reliable performance under demanding industrial conditions
- Reduced operational downtime ensuring continuous production
- Optimal heat transfer efficiency improving overall system performance
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial shell and tube condensers serve as essential heat exchange components in demanding processes, efficiently transferring thermal energy between fluids while maintaining system integrity under high pressure and temperature conditions. They provide reliable condensation and thermal management, ensuring operational stability across applications where consistent cooling is vital for process efficiency and safety compliance in various industrial environments.
These condensers are extensively utilized in HVAC systems for large commercial buildings, refrigeration plants in food processing facilities, chemical manufacturing operations, power generation stations, and oil and gas processing units. Their durable construction handles challenging operational conditions, making them suitable for heavy-duty applications where maintaining precise temperature control and condensation efficiency directly impacts productivity and operational reliability.
- HVAC systems for large commercial buildings and industrial facilities requiring efficient heat rejection
- Refrigeration units in food processing plants and cold storage warehouses for condensation duties
- Chemical manufacturing plants for process cooling and vapor condensation applications
- Power generation facilities for steam turbine exhaust condensation in thermal plants
- Oil refineries and gas processing units for hydrocarbon condensation and cooling operations
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Gurdev Icecans Refrigeration Industries, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Shell And Tube Condensers For High Efficiency Cooling
Industrial shell and tube condensers provide high-efficiency cooling for industrial processes with reliable performance and custom specifications from leading manufacturers for thermal management applications.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Gurdev Icecans Refrigeration Industries
 Maharashtra, India
Industrial Equipment & MachineryManufacturer