
 IN
₹
Description
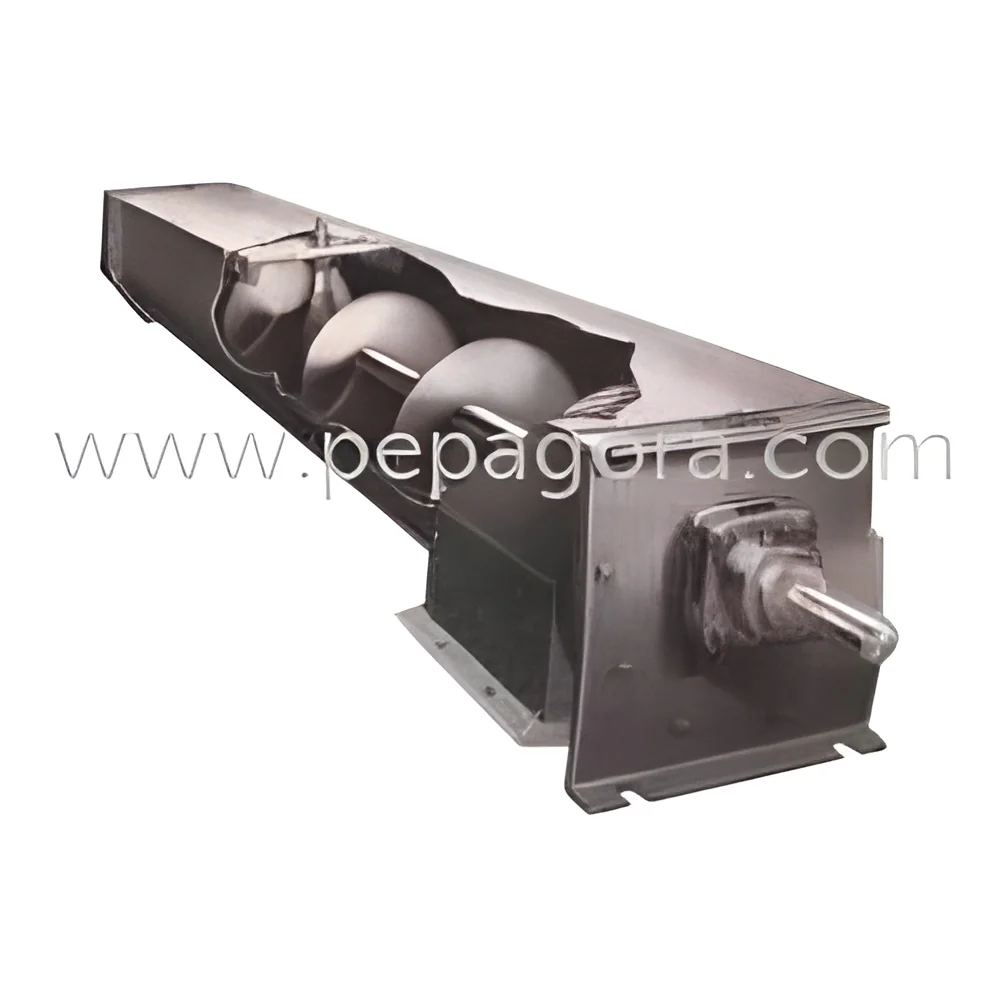
Our industrial screw conveyors deliver efficient horizontal or inclined transportation of semi-solid materials for demanding industrial operations. Engineered with precision design, these systems provide high-capacity performance without requiring excessive rotational speeds, reducing energy consumption and component wear. The robust construction ensures reliable operation in challenging environments while maintaining material integrity throughout the transfer process. Each conveyor is built to industry standards using quality materials that withstand continuous operation and various material types. The design emphasizes simplicity and efficiency, resulting in systems that require minimal maintenance while delivering maximum throughput for material handling needs.

These conveyors serve numerous industries requiring efficient bulk material handling solutions. They are particularly valuable in agricultural processing for moving grains, feed, and harvested products between processing sta...
Our industrial screw conveyors deliver efficient horizontal or inclined transportation of semi-solid materials for demanding industrial operations. Engineered with precision design, these systems provide high-capacity performance without requiring excessive rotational speeds, reducing energy consumption and component wear. The robust construction ensures reliable operation in challenging environments while maintaining material integrity throughout the transfer process. Each conveyor is built to industry standards using quality materials that withstand continuous operation and various material types. The design emphasizes simplicity and efficiency, resulting in systems that require minimal maintenance while delivering maximum throughput for material handling needs.

These conveyors serve numerous industries requiring efficient bulk material handling solutions. They are particularly valuable in agricultural processing for moving grains, feed, and harvested products between processing stages. Construction operations utilize them for handling cement, aggregates, and other building materials, while manufacturing facilities employ them for transporting production materials between processes. The food industry relies on these conveyors for hygienic transfer of ingredients and products, and chemical plants depend on their contained design for safe handling of powders and compounds. Mining operations use heavy-duty versions for moving ores and minerals, and wastewater treatment facilities employ them for sludge conveyance. This versatility makes them suitable for both new installations and retrofitting existing operations across multiple sectors.

The operational value of our screw conveyors lies in their ability to streamline material handling processes, reduce labor requirements, and minimize material loss during transfer. Their reliability ensures uninterrupted production flow, while the robust construction translates to reduced maintenance costs and longer service life, providing excellent return on investment. These systems contribute to workplace safety by enclosing moving parts and containing materials, reducing potential hazards. The energy-efficient design lowers operational expenses while maintaining high throughput capacity. Operations benefit from the flexibility to handle various semi-solid materials without needing multiple transfer systems, optimizing both space and resource utilization.

Key Features:
- Precision-engineered screw design for optimal material flow and reduced energy consumption
- Robust construction using industrial-grade materials for durability in demanding environments
- Enclosed design preventing contamination, spillage, and dust generation during operation
- Customizable lengths and configurations to fit specific operational layouts and requirements
- Simple maintenance design ensuring long service life and reliable continuous performance

Benefits:
- Efficient material handling reduces operational costs and improves production throughput
- Reliable performance minimizes downtime and ensures consistent operational continuity
- Enclosed design enhances workplace safety and prevents material contamination
- Durable construction lowers maintenance requirements and extends equipment lifespan
- Versatile application across multiple industries provides flexible material handling solutions
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial screw conveyors provide efficient, contained transfer of semi-solid materials across various processing environments. Their horizontal or inclined operation ensures consistent material flow without spillage or contamination, making them ideal for bulk handling where material integrity is crucial. The robust construction withstands demanding conditions while maintaining reliable performance in both indoor and outdoor applications.
Customizable configurations allow seamless integration into existing production lines or new facility designs. These systems transport materials over moderate distances efficiently, reducing manual handling and operational downtime. The simple design translates to minimal maintenance requirements and extended service life, providing dependable performance for continuous operations. Their versatility makes them suitable for numerous industries where efficient, contained material transfer is essential for productivity.
- Agricultural processing for moving grains, animal feed, and harvested products between storage and processing units
- Chemical manufacturing plants for safe, enclosed transfer of powdered chemicals and granular compounds
- Food production facilities for hygienic transportation of ingredients, mixes, and finished food products
- Construction material handling for cement, sand, aggregates, and other bulk building materials
- Mining and mineral processing operations for efficient movement of ores, extracted minerals, and processing materials
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Canara Engineers Pvt Ltd, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Screw Conveyors For Semi Solid Material Handling
Industrial screw conveyors efficiently handle semi-solid materials like grains, powders, and aggregates. Built for reliability in demanding industrial operations with high-capacity performance and market-leading value.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Canara Engineers Pvt Ltd
 Maharashtra, India
Industrial Equipment & MachineryManufacturer


