IN
₹
Apparel & Fashion
Description
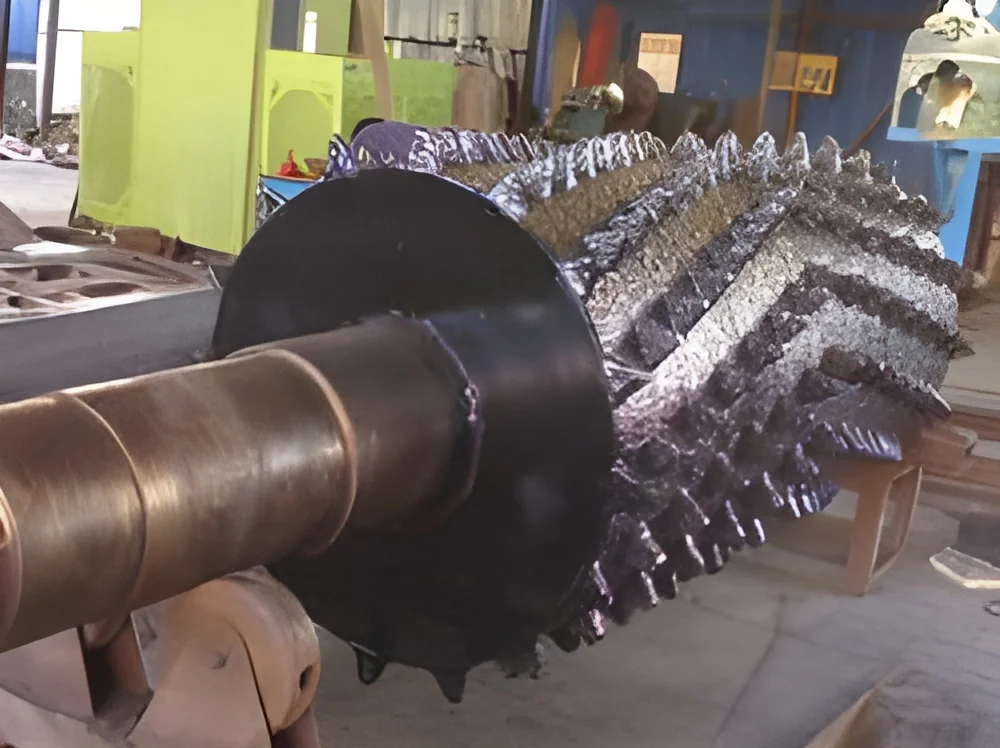
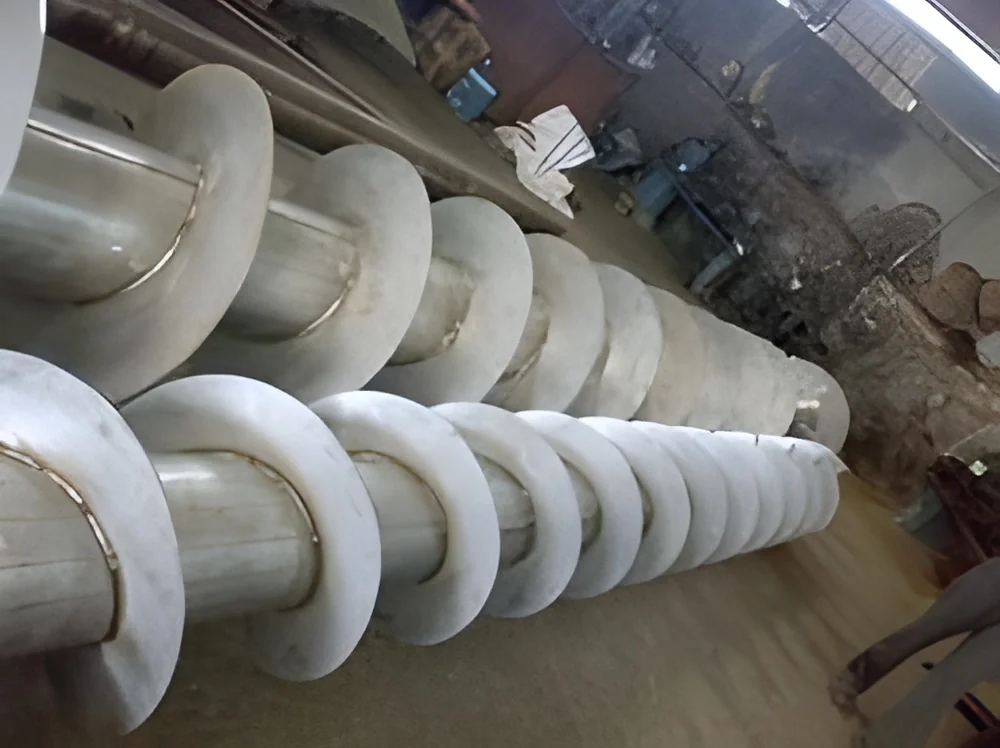
Our premium screw conveyor systems represent specialized engineering solutions designed specifically for the rigorous demands of sugar industry material handling. These robust systems utilize rotating helical screws within sealed troughs to efficiently transport bulk materials like sugar crystals, bagasse, and granular products throughout processing facilities. Manufactured with durability and reliability as primary considerations, these conveyors handle everything from fine powdered sugar to coarse bagasse with consistent performance. The precision engineering ensures optimal material flow rates while preventing contamination and product degradation, making them essential components for modern sugar processing operations where hygiene and efficiency are paramount.

These screw conveyors serve critical functions throughout sugar production facilities, from initial cane processing to final packaging operations. They efficiently transport bagasse from milling stations to boilers for ener...
Our premium screw conveyor systems represent specialized engineering solutions designed specifically for the rigorous demands of sugar industry material handling. These robust systems utilize rotating helical screws within sealed troughs to efficiently transport bulk materials like sugar crystals, bagasse, and granular products throughout processing facilities. Manufactured with durability and reliability as primary considerations, these conveyors handle everything from fine powdered sugar to coarse bagasse with consistent performance. The precision engineering ensures optimal material flow rates while preventing contamination and product degradation, making them essential components for modern sugar processing operations where hygiene and efficiency are paramount.

These screw conveyors serve critical functions throughout sugar production facilities, from initial cane processing to final packaging operations. They efficiently transport bagasse from milling stations to boilers for energy generation, move raw sugar crystals between washing and refining stages, and handle intermediate products throughout the production chain. Beyond core sugar processing, adjacent operations benefit from their reliable performance, including by-product handling, waste management systems, and materials transfer between different facility sections. The versatility of these systems makes them indispensable for any sugar processing operation requiring controlled, continuous movement of bulk materials with minimal maintenance requirements.

The operational value of our screw conveyors extends beyond basic material transport to deliver tangible efficiency improvements and long-term reliability. These systems significantly reduce manual handling requirements while minimizing product loss and contamination risks associated with alternative transportation methods. Their durable construction ensures extended service life with minimal operational downtime, providing exceptional return on investment through reduced maintenance costs and consistent performance. The engineering focus on sugar industry applications means these conveyors are optimized for the specific material characteristics and environmental conditions found in sugar processing facilities, ensuring reliable operation even in demanding conditions where consistent material handling directly impacts production success.

Key Features:
- Heavy-duty construction with corrosion-resistant materials suitable for sugar industry environments
- Precision-engineered helical screws optimized for sugar crystals and bagasse material characteristics
- Enclosed trough design preventing contamination and dust emission in processing areas
- Customizable length, diameter, and capacity to match specific facility layouts
- Multiple discharge options and configurations for flexible installation in existing plants

Benefits:
- Reliable continuous operation minimizing production interruptions in sugar processing
- Reduced product loss and contamination through enclosed material transport
- Lower maintenance requirements with durable components built for industrial use
- Energy-efficient design reducing operational costs for material handling
- Flexible installation options adapting to existing facility layouts and space constraints
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Screw conveyors provide efficient, enclosed bulk material transport for sugar mills and processing plants, moving sugar crystals, bagasse, and granular products with consistent flow and minimal contamination. Their robust design handles demanding industrial environments where reliable material movement is critical for continuous production and operational efficiency.
These systems offer versatile solutions for various material handling needs with adjustable speeds and configurations. The enclosed trough design prevents dust emission and product loss while ensuring safety and cleanliness in sensitive processing areas. This makes them suitable for facilities requiring precise control over material transfer between different stages of production.
- Transporting sugarcane bagasse from mills to boilers or storage in sugar production facilities
- Moving refined sugar crystals between processing, packaging, and storage areas
- Handling intermediate sugar products like raw crystals and molasses within processing lines
- Conveying filter cake and other by-products in sugar refinery operations
- Transferring granular materials in food processing plants adjacent to sugar facilities
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
A S Pattern & Engineering Works, Uttar Pradesh
 Uttar Pradesh, India
Industrial Equipment & Machinery•Manufacturer•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Premium Screw Conveyor For Sugar Industries Material Handling
Premium screw conveyor for sugar industries material handling offers reliable bulk transport with custom designs for demanding industrial applications, ensuring efficient movement of sugar crystals and bagasse.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
A S Pattern & Engineering Works
 Uttar Pradesh, India
Industrial Equipment & MachineryManufacturer