IN
₹
Description
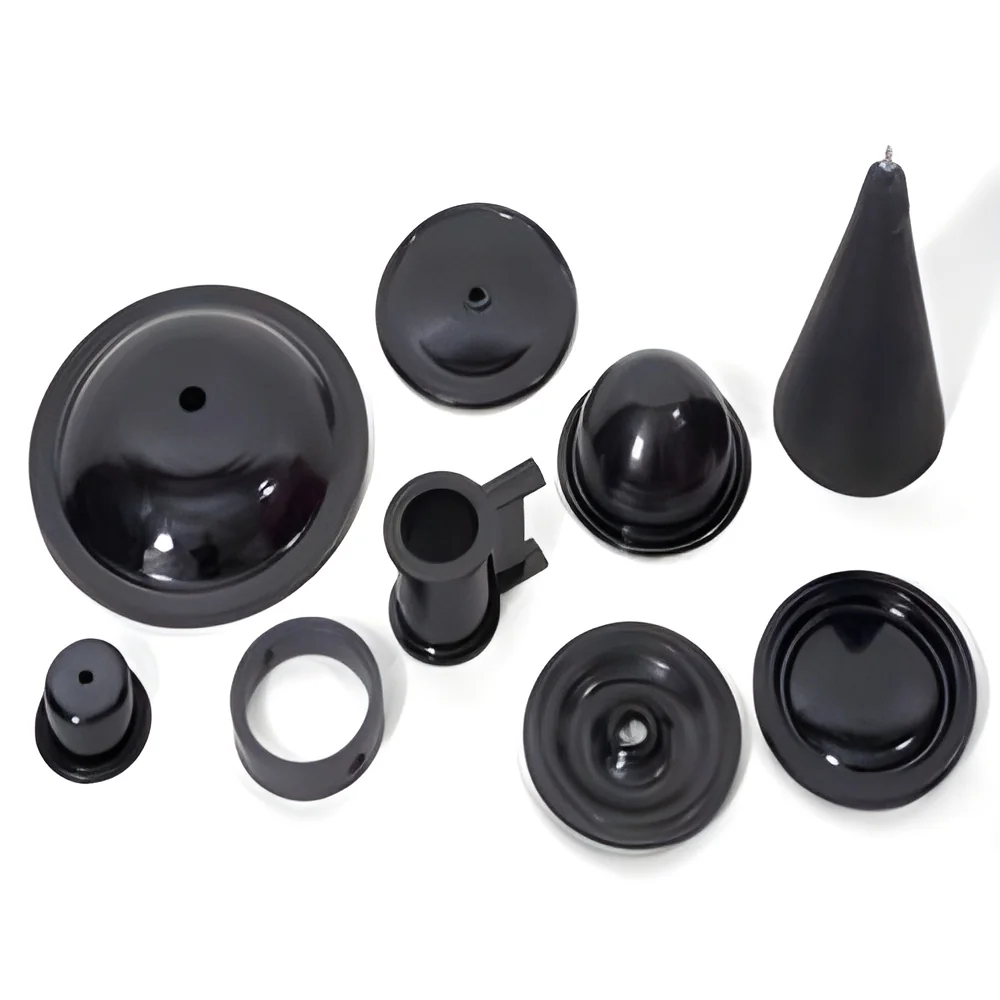
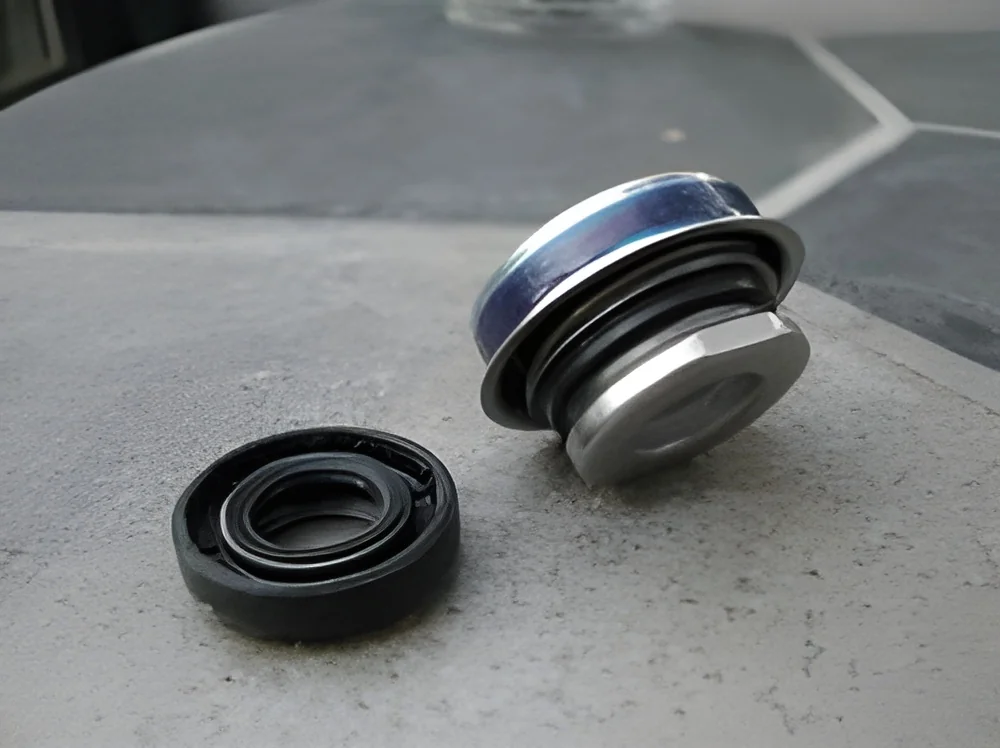
Our premium industrial rubber water seals are precision-engineered for applications requiring reliable leak prevention and durability in challenging environments. Manufactured from high-quality rubber compounds, these seals offer exceptional resistance to wear, abrasion, and various fluids including sewage, muddy water, and light chemicals. They are designed to maintain perfect sealing under demanding conditions, ensuring your machinery operates at peak efficiency without downtime or fluid loss. The precision engineering guarantees exact fitment while the robust material composition provides long-lasting performance even in the most challenging industrial settings, from high-pressure systems to temperature-variable operations.

These water seals serve critical functions across multiple industries including wastewater treatment, agriculture, chemical processing, oil and gas, and power generation. In sewage treatment plants, they prevent leaks in pumps and valves handling abrasive materi...
Our premium industrial rubber water seals are precision-engineered for applications requiring reliable leak prevention and durability in challenging environments. Manufactured from high-quality rubber compounds, these seals offer exceptional resistance to wear, abrasion, and various fluids including sewage, muddy water, and light chemicals. They are designed to maintain perfect sealing under demanding conditions, ensuring your machinery operates at peak efficiency without downtime or fluid loss. The precision engineering guarantees exact fitment while the robust material composition provides long-lasting performance even in the most challenging industrial settings, from high-pressure systems to temperature-variable operations.

These water seals serve critical functions across multiple industries including wastewater treatment, agriculture, chemical processing, oil and gas, and power generation. In sewage treatment plants, they prevent leaks in pumps and valves handling abrasive materials and contaminants. Agricultural machinery relies on them for irrigation systems operating in muddy conditions where standard seals would fail. Chemical processing units utilize their resistance to light chemicals, while oil pumps and generators benefit from their pressure and temperature tolerance. Marine equipment and water infrastructure projects also depend on these seals for reliable performance in wet environments where corrosion and wear are constant challenges.

For importers, distributors, and wholesalers, these rubber water seals represent exceptional value through reduced maintenance costs, extended equipment lifespan, and minimized operational downtime. Their reliability ensures consistent performance that protects machinery investments and maintains production efficiency. The quality construction and precision engineering provide tailored solutions that meet specific application requirements, delivering proven performance that meets the highest standards of durability. Trusted by global industrial suppliers, these seals offer peace of mind through their consistent performance in demanding applications where failure is not an option.

Key Features:
- High-quality rubber compounds for superior durability and longevity in harsh conditions
- Precision engineering ensures exact fit and optimal sealing performance for machinery
- Exceptional resistance to abrasion, wear, and exposure to various industrial fluids
- Designed to withstand high-pressure conditions and temperature variations
- Reliable performance in sewage, muddy water, light chemicals, and oil applications

Benefits:
- Reduces maintenance costs and extends equipment lifespan through durable construction
- Minimizes operational downtime with reliable leak-proof performance
- Protects machinery investments by preventing fluid leaks and contamination
- Ensures consistent performance in demanding industrial environments
- Provides peace of mind with proven reliability across multiple applications
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
These industrial-grade rubber water seals provide essential sealing solutions for machinery operating in extreme environments. They prevent fluid leaks, protect equipment from contaminants, and ensure operational continuity in systems exposed to water, chemicals, and abrasive materials. Their robust construction makes them indispensable for industries where equipment failure is not an option, maintaining integrity under pressure, temperature variations, and harsh chemical exposure.
Designed for consistent performance in pumps, generators, and fluid handling systems, these seals deliver reliable operation across multiple sectors. They withstand exposure to sewage, muddy water, light chemicals, and oils while maintaining perfect sealing capabilities. Trusted by engineers and maintenance professionals globally for their durability and precision fit in demanding industrial applications.
- Sewage treatment plants and wastewater management systems handling abrasive materials
- Agricultural machinery and irrigation equipment operating in muddy water conditions
- Light chemical processing units and industrial fluid transfer systems
- Oil pumps, hydraulic systems, and power generation equipment
- Marine applications and water supply infrastructure projects
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
E V Engineering, Tamil Nadu
 Tamil Nadu, India
Industrial Equipment & Machinery•Manufacturer
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
South Asia
Industrial Rubber Water Seals For Sewage Muddy Water Chemical Oil Pumps
Industrial rubber water seals for sewage, muddy water, chemical, and oil pumps. Engineered for leak-proof performance in demanding machinery applications with reliable sealing under harsh conditions.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
E V Engineering
 Tamil Nadu, India
Industrial Equipment & MachineryManufacturer