IN
₹
Apparel & Fashion
Description
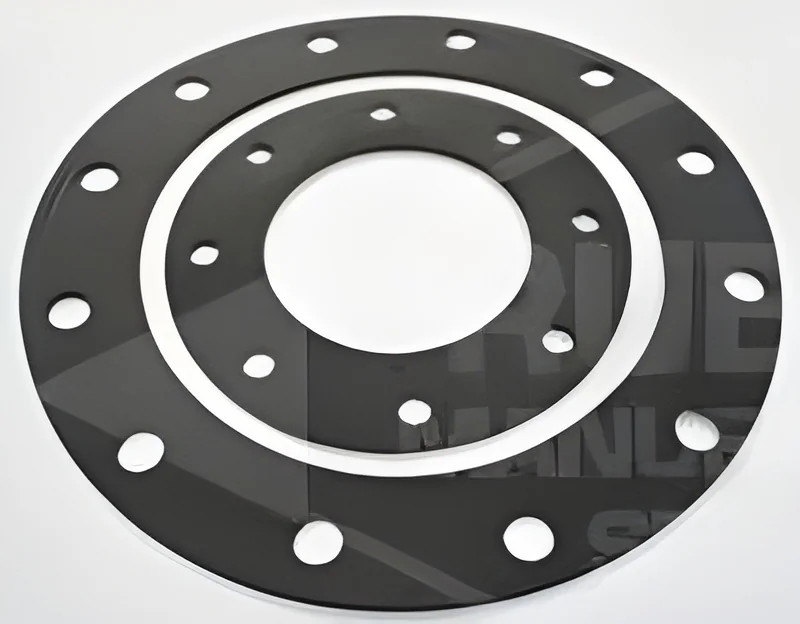
Industrial rubber gaskets represent precision-engineered sealing solutions designed for demanding industrial applications where reliability and durability are essential. Manufactured from premium elastomers including EPDM, Nitrile, Silicone, and Neoprene, these gaskets provide exceptional compression set resistance for long-term performance under extreme conditions. Each material formulation is carefully selected for specific environmental and chemical exposure requirements, ensuring optimal performance characteristics. Supported by comprehensive quality control processes, these gaskets deliver dependable, scalable sealing components that integrate seamlessly into existing systems while minimizing maintenance requirements and operational disruptions.

These sealing solutions serve critical functions across diverse industrial sectors including automotive manufacturing, oil and gas operations, water treatment facilities, pharmaceutical production, food processing, and HVAC systems. In au...
Industrial rubber gaskets represent precision-engineered sealing solutions designed for demanding industrial applications where reliability and durability are essential. Manufactured from premium elastomers including EPDM, Nitrile, Silicone, and Neoprene, these gaskets provide exceptional compression set resistance for long-term performance under extreme conditions. Each material formulation is carefully selected for specific environmental and chemical exposure requirements, ensuring optimal performance characteristics. Supported by comprehensive quality control processes, these gaskets deliver dependable, scalable sealing components that integrate seamlessly into existing systems while minimizing maintenance requirements and operational disruptions.

These sealing solutions serve critical functions across diverse industrial sectors including automotive manufacturing, oil and gas operations, water treatment facilities, pharmaceutical production, food processing, and HVAC systems. In automotive applications, they provide reliable sealing for engines, transmissions, and fluid systems while withstanding high temperatures and lubricants. Water treatment facilities depend on them for leak-proof performance in pipes and valves, ensuring operational safety and regulatory compliance. Pharmaceutical and food industries utilize approved gasket variants to maintain hygiene standards and prevent contamination, while HVAC systems employ them for effective thermal insulation and air sealing to enhance energy efficiency.

The strategic implementation of industrial rubber gaskets delivers substantial business value through enhanced operational reliability, reduced leakage-related losses, and minimized maintenance expenditures. Their robust construction significantly decreases the risk of system failures, ensuring continuous production processes and avoiding costly downtime. The availability of specialized formulations enables businesses to address unique operational challenges, improving overall system efficiency and safety parameters. Supported by consistent quality standards and reliable supply chain management, these gaskets help establish long-term partner confidence while supporting compliance with industry regulations and standards. Their cost-effectiveness and extended service life provide strong return on investment, making them an intelligent choice for organizations prioritizing performance excellence and sustainable value.

Key Features:
- Manufactured from premium elastomers including EPDM, Nitrile, Silicone, and Neoprene
- Available in various sizes and material compounds to meet specific operational requirements
- Excellent resistance to compression set for maintaining long-term sealing integrity
- Suitable for high-pressure, high-temperature, and chemical exposure environments
- Comprehensive quality control and testing procedures ensure consistent performance

Benefits:
- Enhanced operational reliability through dependable sealing performance
- Reduced maintenance requirements and associated operational costs
- Minimized risk of system failures and production downtime
- Improved safety compliance and environmental protection
- Long service life and cost-effectiveness for better return on investment
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial rubber gaskets deliver critical sealing performance across multiple sectors, ensuring leak-proof operation in high-pressure and temperature environments. Engineered to resist chemicals, oils, and weathering, they maintain integrity where failure is not an option. These gaskets withstand demanding applications while providing consistent sealing reliability for industrial operations.
These sealing components serve essential functions in automotive manufacturing, water treatment facilities, chemical processing plants, and HVAC systems. They perform reliably in pumps, valves, flanges, and machinery assemblies, preventing fluid or gas leaks while maintaining system safety. Their versatility supports both static and dynamic sealing configurations, enabling efficient and secure industrial processes across various operational conditions.
- Sealing pipe flanges in water treatment plants to prevent leaks and ensure environmental compliance
- Engine and transmission gasketing in automotive applications for high-temperature and oil resistance
- Thermal and air seals in HVAC systems for improved energy efficiency and performance
- Chemical-resistant seals for pharmaceutical and chemical processing equipment
- Machinery sealing solutions for food processing operations meeting safety standards
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Ashok Malik & Company, Punjab
 Punjab, India
Industrial Equipment & Machinery•Trading Company•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Rubber Gaskets For Sealing Applications In OEM MRO
Industrial rubber gaskets provide reliable sealing solutions for OEM and MRO applications. These durable gaskets feature customizable sizes and materials for superior performance in demanding fluid systems and industrial environments.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Ashok Malik & Company
 Punjab, India
Industrial Equipment & MachineryTrading Company