IN
₹
Apparel & Fashion
Description
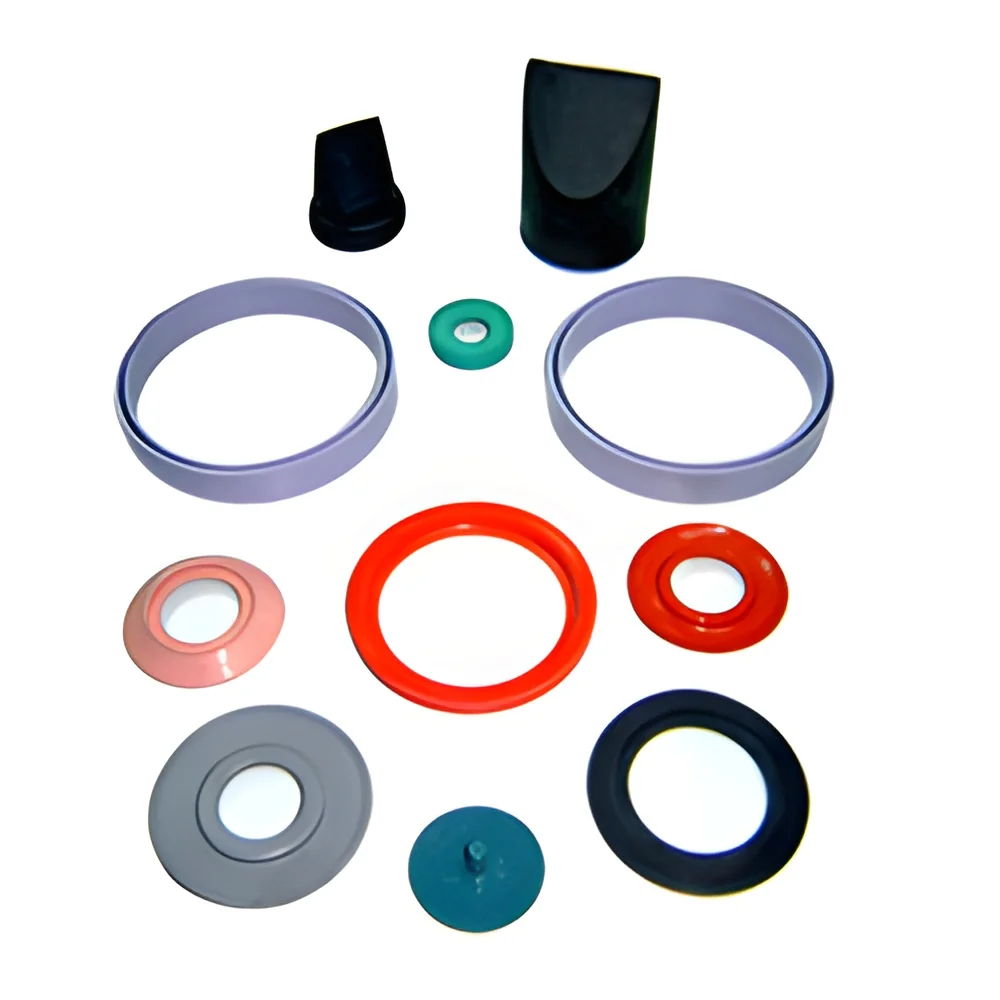
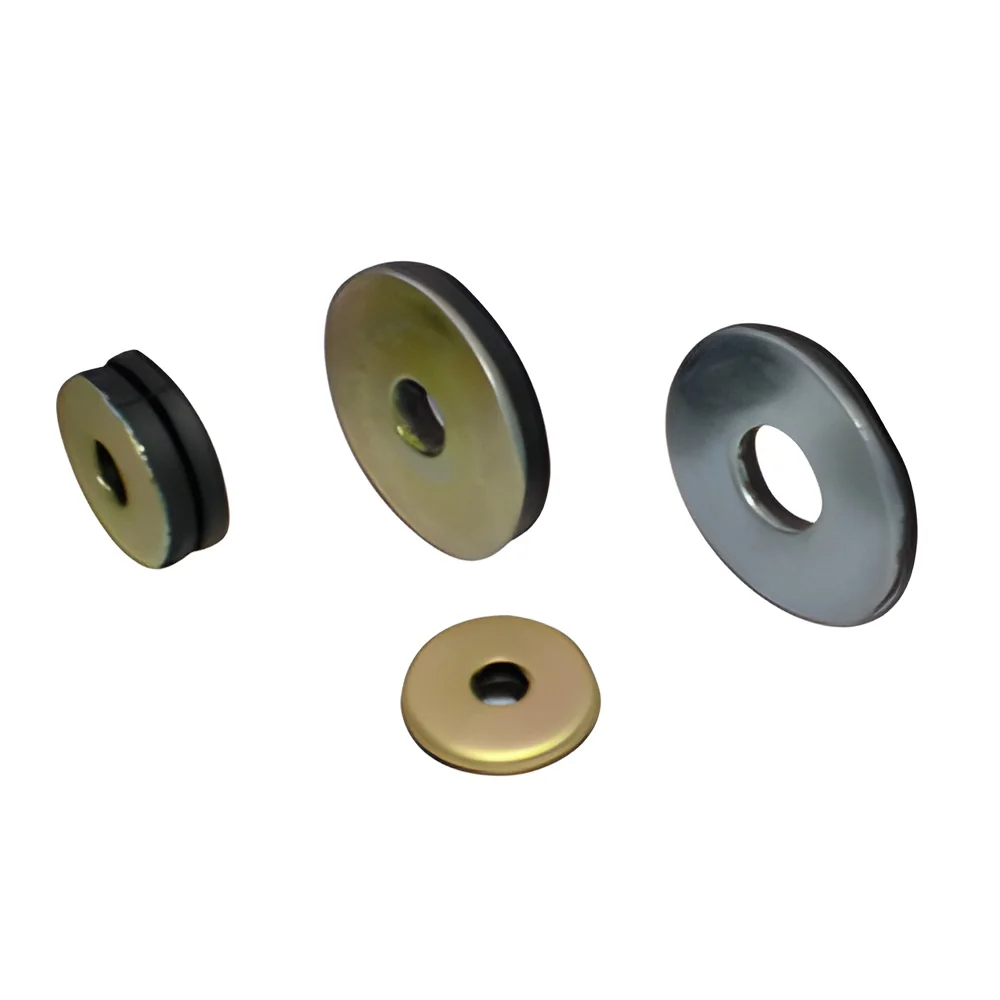
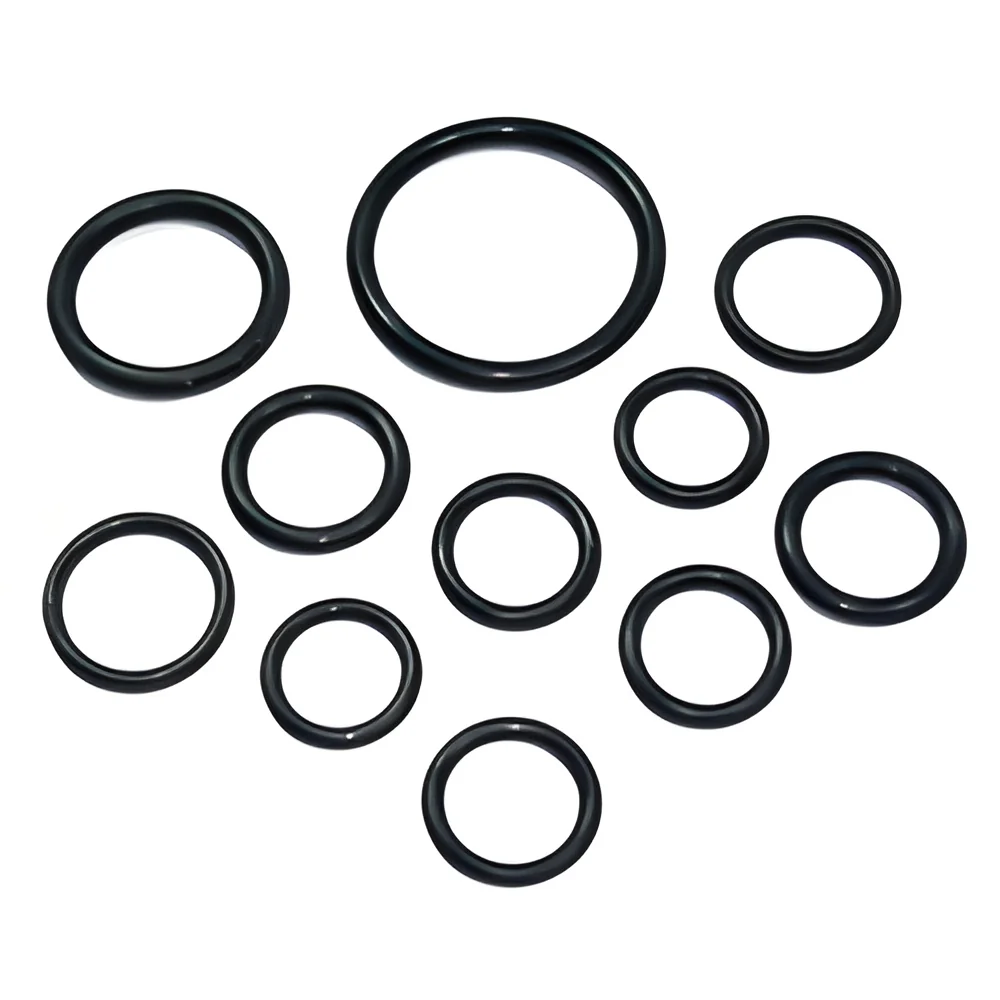
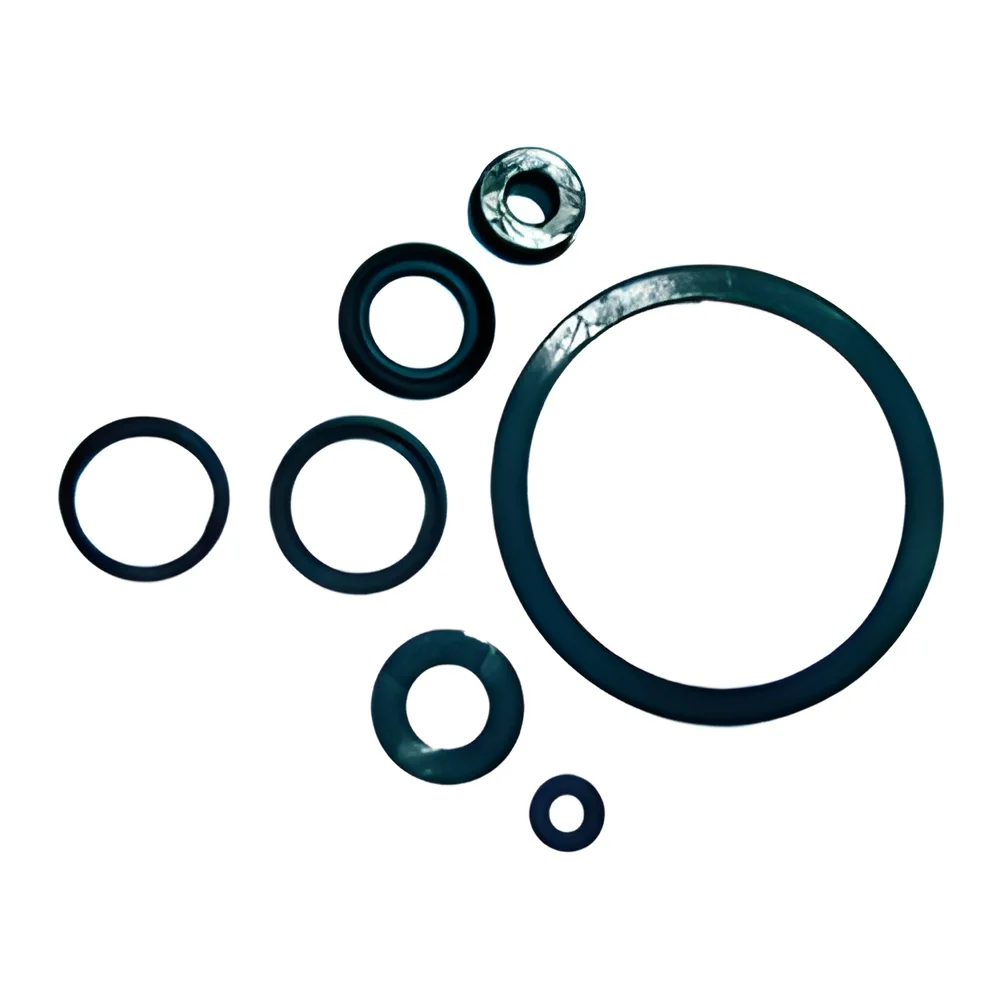
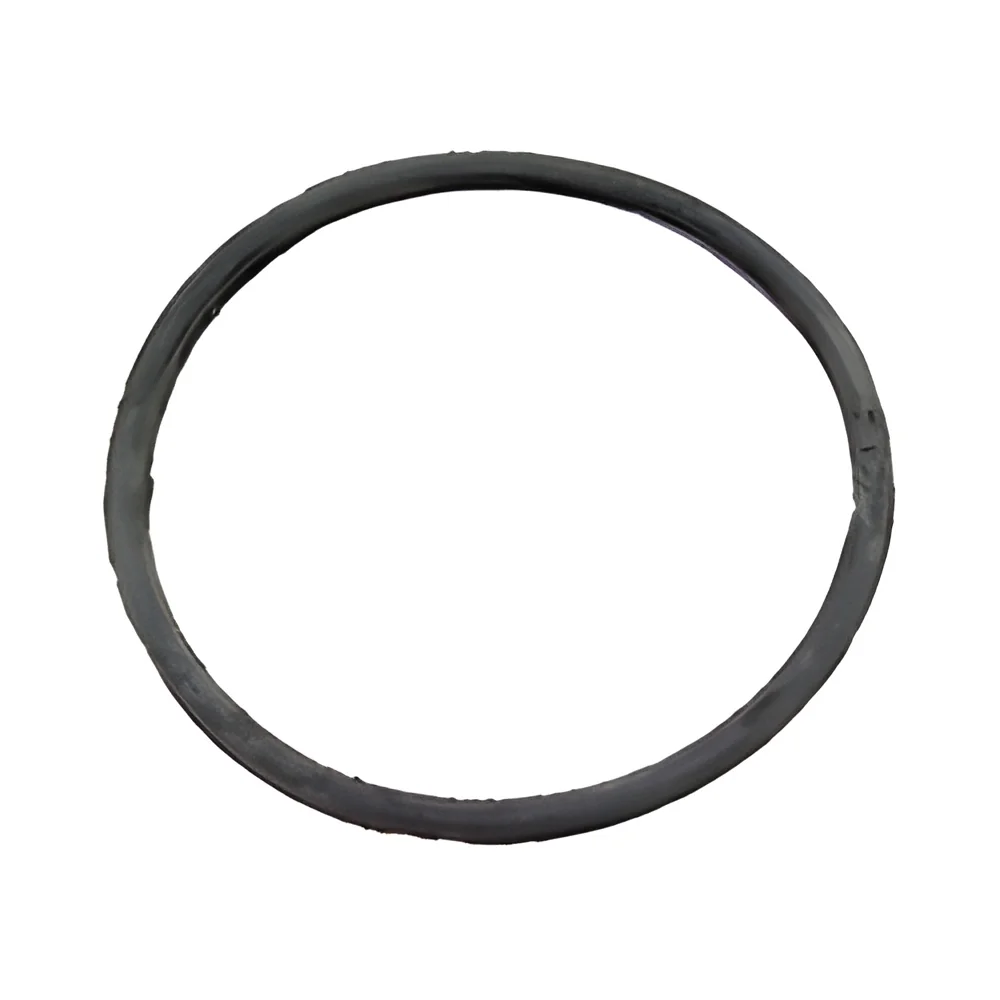
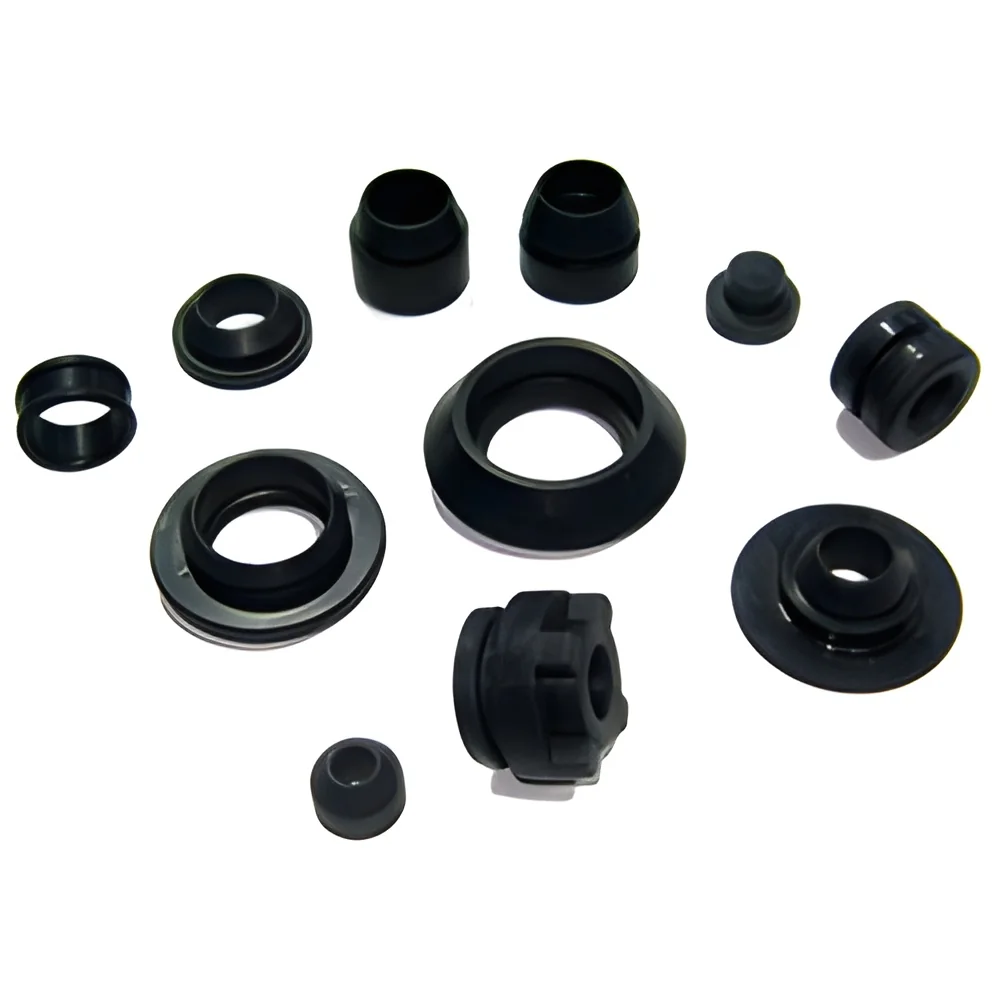
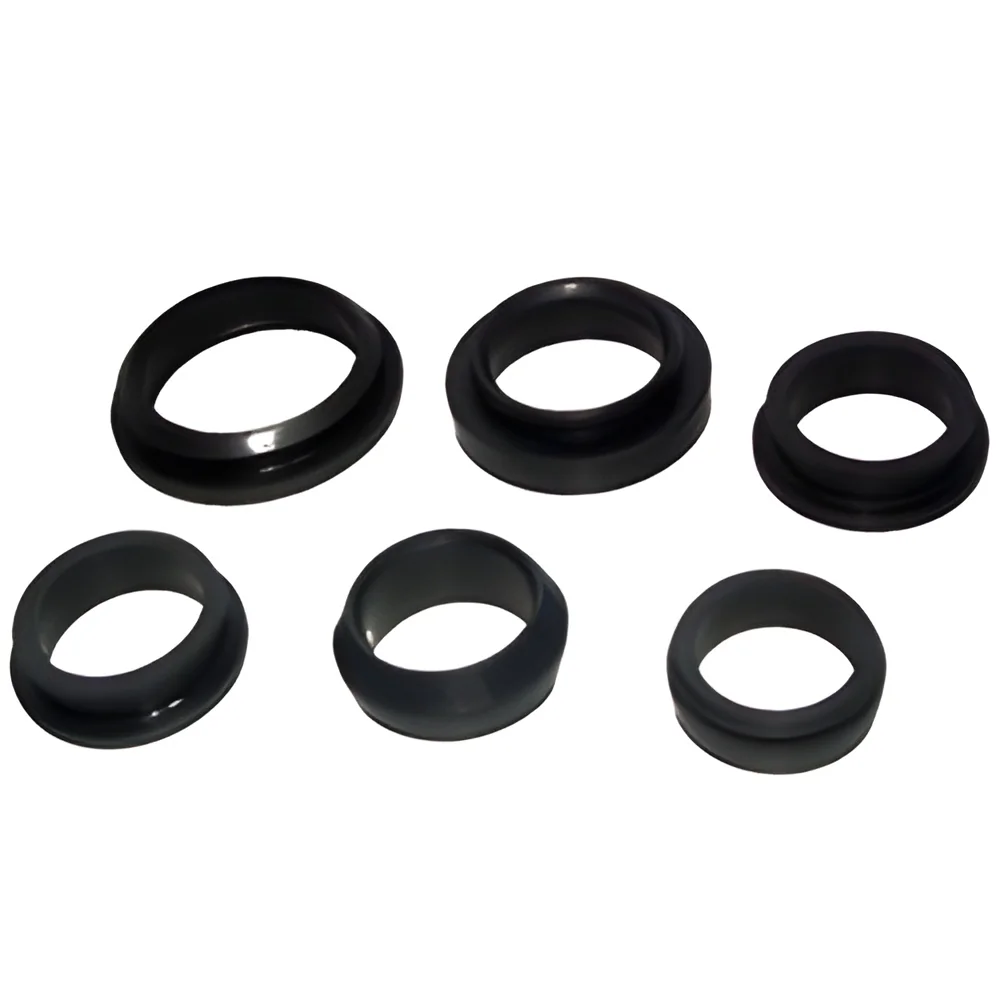
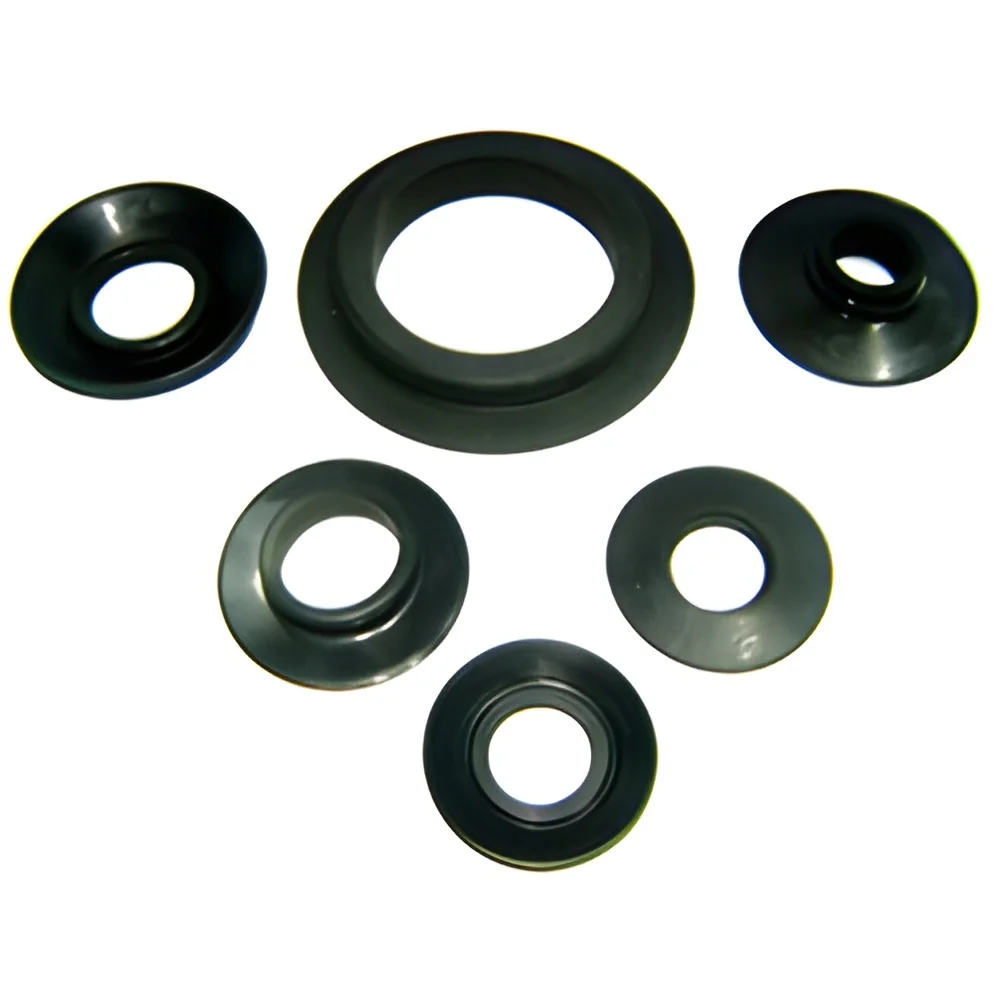
Our industrial rubber check valves represent superior engineering in fluid control technology, designed to deliver reliable backflow prevention across demanding industrial environments. Manufactured from premium, tested rubber compounds, these valves maintain their structural integrity and performance characteristics even under challenging operational conditions. Available in multiple configurations including flanged, insertable, and slip-on designs, they provide versatile solutions for various piping systems. The flexible rubber construction enables automatic operation, opening seamlessly with forward flow pressure and sealing tightly against reverse flow. Built for durability and long service life, these valves offer industrial buyers dependable fluid control solutions that stand up to rigorous daily use.

These rubber check valves find extensive application across numerous industrial sectors due to their adaptable performance and reliability. Water treatment facilities utilize them ...
Our industrial rubber check valves represent superior engineering in fluid control technology, designed to deliver reliable backflow prevention across demanding industrial environments. Manufactured from premium, tested rubber compounds, these valves maintain their structural integrity and performance characteristics even under challenging operational conditions. Available in multiple configurations including flanged, insertable, and slip-on designs, they provide versatile solutions for various piping systems. The flexible rubber construction enables automatic operation, opening seamlessly with forward flow pressure and sealing tightly against reverse flow. Built for durability and long service life, these valves offer industrial buyers dependable fluid control solutions that stand up to rigorous daily use.

These rubber check valves find extensive application across numerous industrial sectors due to their adaptable performance and reliability. Water treatment facilities utilize them to prevent backflow contamination in filtration and distribution systems, ensuring water quality and safety. Chemical processing plants depend on these valves for handling corrosive fluids and protecting expensive pumping equipment from reverse flow damage. The automotive industry incorporates them in cooling systems and fluid transfer operations, while mining operations rely on their robust construction for abrasive slurry handling. HVAC systems integrate rubber check valves for controlling refrigerant and water flow, and marine applications benefit from their corrosion-resistant properties in saltwater environments, making them essential components across diverse industrial landscapes.

Businesses select our rubber check valves for their exceptional reliability and significant operational value. The quality-tested rubber construction ensures consistent performance over time, reducing maintenance expenses and minimizing operational downtime. These valves provide crucial protection against backflow damage, safeguarding expensive equipment and preventing production interruptions that can impact profitability. Their automatic operation requires no external power sources or complex controls, contributing to energy efficiency and operational simplicity. The availability of multiple configurations allows for seamless system integration, while the durable construction ensures long-term performance. This combination of reliability, versatility, and cost-effectiveness delivers substantial return on investment for industrial operations seeking dependable fluid control solutions.

Key Features:
- Manufactured from premium, tested rubber compounds for enhanced durability
- Available in flanged, insertable, and slip-on configurations for system compatibility
- Automatic operation requiring no external power sources or controls
- Corrosion-resistant construction suitable for harsh industrial environments
- Flexible design ensuring tight sealing against varying pressure conditions

Benefits:
- Reduces maintenance costs and operational downtime through reliable performance
- Protects expensive equipment from backflow damage and system failures
- Requires no external power, contributing to energy efficiency and simplicity
- Adapts to various industrial applications with multiple configuration options
- Provides long service life and consistent performance in demanding conditions
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial rubber check valves serve critical functions across multiple sectors by preventing backflow in fluid handling systems. Their flexible rubber construction ensures tight sealing even with varying pressures and temperatures, making them ideal for water, chemicals, and semi-solid media. These valves automatically open with forward flow and close against reverse flow, protecting pumps and equipment from potential damage while maintaining system integrity.
Available in flanged, insertable, and slip-on designs, these valves adapt to different piping configurations with ease. Industries select rubber check valves for their corrosion resistance, minimal maintenance needs, and ability to handle abrasive substances. The straightforward design guarantees reliable performance without requiring external controls, offering cost-efficient solutions for diverse operational requirements across numerous industrial settings.
- Preventing backflow contamination in water treatment plants and municipal water systems
- Protecting pumping equipment from reverse flow damage in chemical processing facilities
- Controlling fluid direction in HVAC systems and industrial heating applications
- Managing abrasive slurry and particulate-laden media in mining and mineral processing
- Ensuring one-way flow in marine applications, offshore platforms, and shipboard systems
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile

Amar Polymers, Haryana
 Haryana, India
Industrial Equipment & Machinery•Manufacturer•Trading Company•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Rubber Check Valves Flanged Insertable Slip On Backflow Prevention
Industrial rubber check valves provide reliable backflow prevention in flanged, insertable, and slip-on configurations. These durable, leak-proof valves protect fluid systems in water treatment, chemical processing, and industrial applications with automatic operation and corrosion resistance.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Amar Polymers
 Haryana, India
Industrial Equipment & MachineryManufacturer