IN
₹
Apparel & Fashion
Description
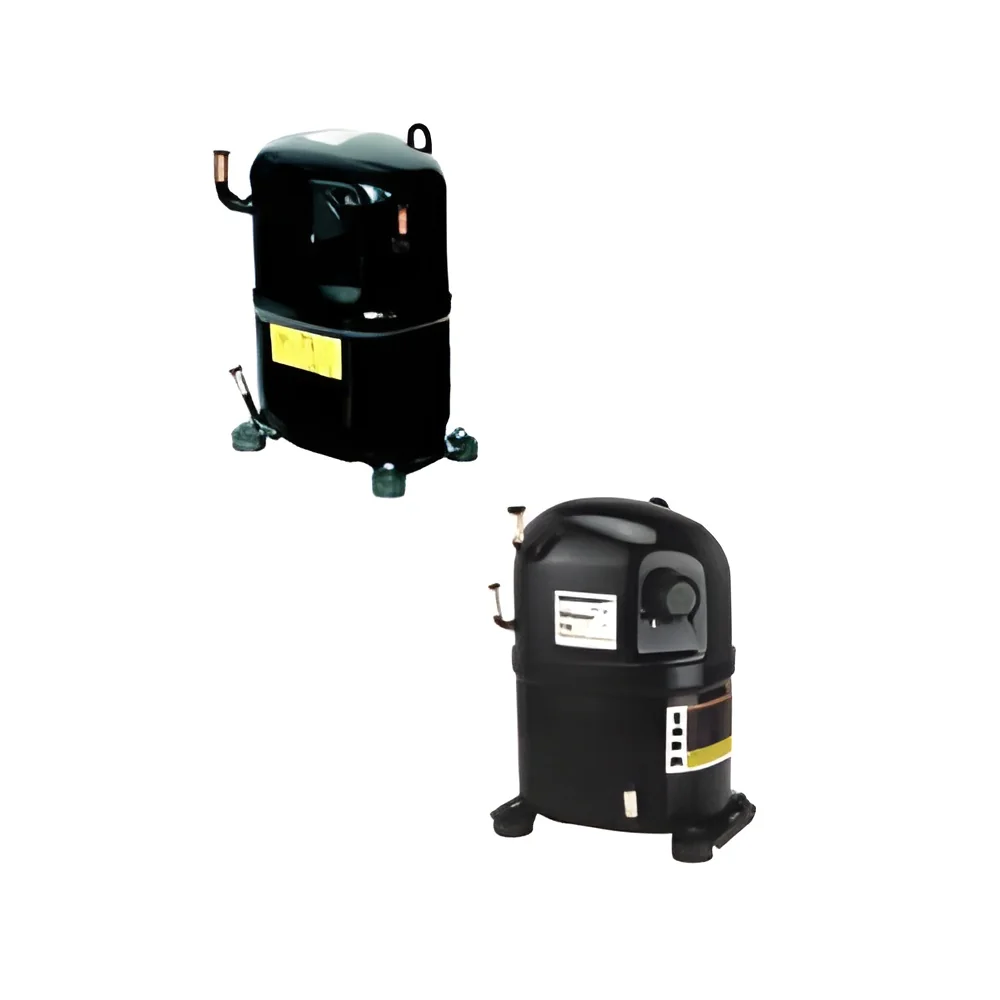
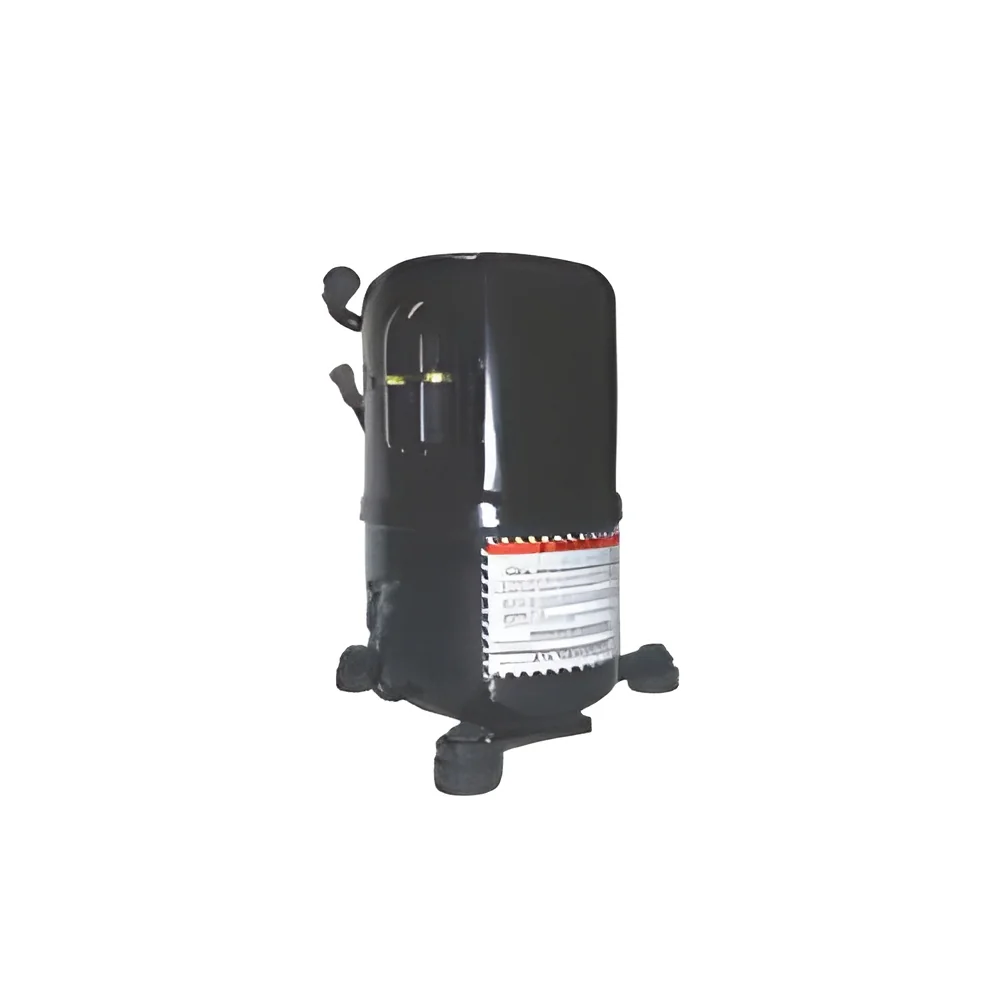
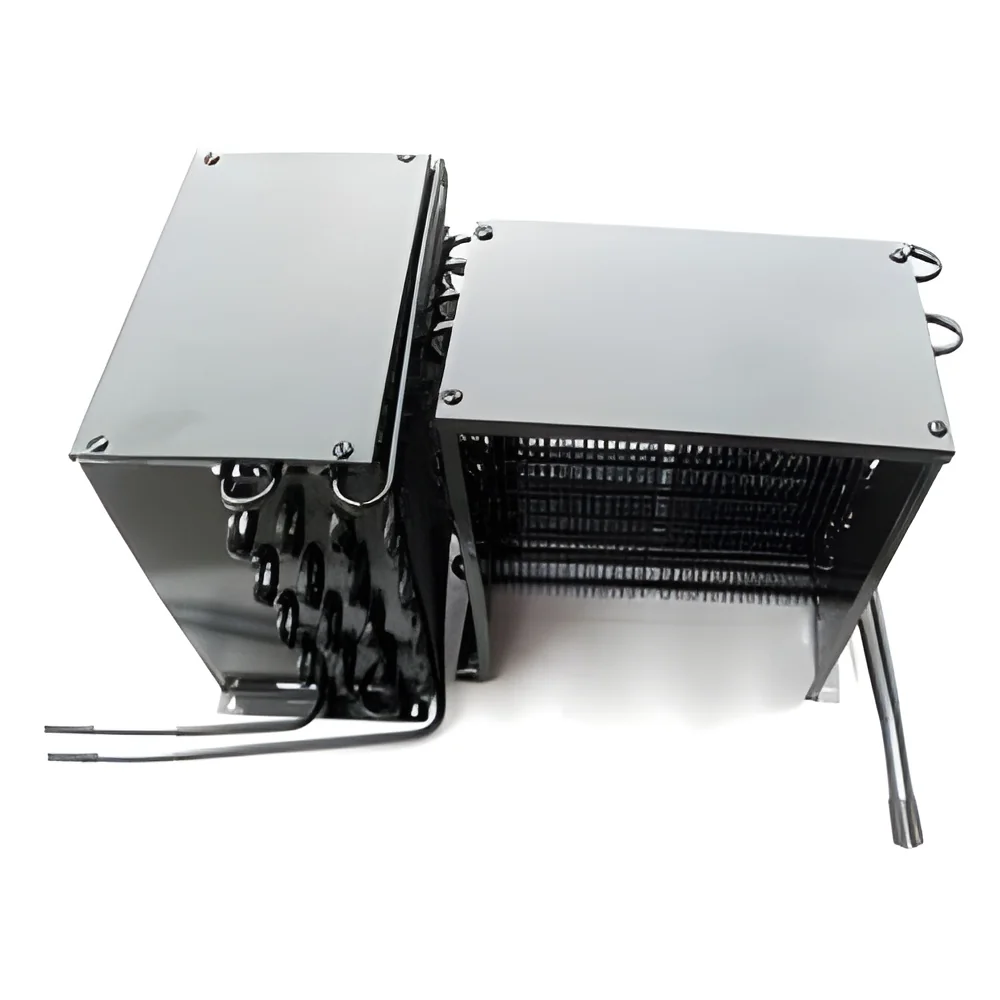
Our premium industrial refrigerator condensers represent advanced cooling technology engineered specifically for commercial and industrial applications. Manufactured using high-grade copper and aluminum materials combined with sophisticated production techniques, these condensers deliver exceptional heat transfer efficiency and long-term operational reliability. Each unit meets rigorous international quality standards, ensuring optimal performance in demanding refrigeration systems while significantly reducing energy consumption and operational expenses. The durable construction withstands continuous operation in challenging environments, maintaining consistent cooling performance throughout extended service life without compromising efficiency or reliability.

These condensers serve critical functions across multiple industries where precise temperature control is essential for operational success. In food processing and cold storage facilities, they maintain exact temperatures to pre...
Our premium industrial refrigerator condensers represent advanced cooling technology engineered specifically for commercial and industrial applications. Manufactured using high-grade copper and aluminum materials combined with sophisticated production techniques, these condensers deliver exceptional heat transfer efficiency and long-term operational reliability. Each unit meets rigorous international quality standards, ensuring optimal performance in demanding refrigeration systems while significantly reducing energy consumption and operational expenses. The durable construction withstands continuous operation in challenging environments, maintaining consistent cooling performance throughout extended service life without compromising efficiency or reliability.

These condensers serve critical functions across multiple industries where precise temperature control is essential for operational success. In food processing and cold storage facilities, they maintain exact temperatures to preserve product quality, safety, and freshness. Pharmaceutical companies depend on them for temperature-sensitive storage solutions that comply with strict regulatory requirements and quality standards. Commercial establishments including supermarkets, restaurants, and hotels utilize these condensers in their refrigeration systems for optimal food preservation and customer service. Industrial manufacturing plants implement them in process cooling applications, while large-scale HVAC systems in commercial buildings rely on their efficient heat dissipation capabilities for effective climate control and occupant comfort.

The business value of our refrigerator condensers extends beyond basic cooling functionality to deliver substantial operational advantages and cost savings. These units provide enhanced energy efficiency that translates to significant reductions in electricity costs over their extended operational lifespan. Their reliable performance minimizes system downtime and maintenance requirements, ensuring continuous productivity in critical cooling applications. The corrosion-resistant construction ensures durability even in demanding environmental conditions, while the compliance with international standards guarantees safety and reliability. This combination of features provides businesses with a dependable cooling solution that protects their investments, maintains operational consistency, and supports long-term business growth through reliable temperature management.

Key Features:
- High-grade copper and aluminum construction for superior thermal conductivity
- Advanced heat transfer technology maximizes cooling efficiency and performance
- Corrosion-resistant design ensures durability in harsh operating environments
- Robust construction withstands continuous heavy-duty operation
- Complies with international quality standards for reliability and safety

Benefits:
- Significant energy efficiency reduces operational costs and electricity consumption
- Reliable performance minimizes downtime and maintenance requirements
- Extended service life provides long-term value and return on investment
- Consistent temperature control ensures product quality and safety
- Durable construction withstands demanding environmental conditions
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our industrial refrigerator condensers provide optimal heat dissipation for commercial and industrial refrigeration systems, ensuring consistent temperature control and energy-efficient operation across various sectors. These units maintain peak efficiency during continuous heavy-duty use while reducing operational costs and enhancing system reliability in challenging conditions.
Engineered for demanding environments, these condensers deliver precise temperature management critical for product integrity and operational safety. The robust construction withstands harsh conditions while maintaining consistent cooling performance, making them suitable for applications where reliability and regulatory compliance are essential requirements for successful operations.
- Cold storage warehouses requiring reliable temperature control for perishable goods preservation
- Food processing plants needing efficient cooling for production lines and storage areas
- Pharmaceutical storage facilities demanding precise temperature maintenance for medications
- Supermarket refrigeration systems for display cases and walk-in coolers
- Large commercial HVAC installations in office buildings and healthcare facilities
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Capri Refrigeration, Gujarat
 Gujarat, India
Industrial Equipment & Machinery•Distributor / Wholesaler•Retailer•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
South Asia
Industrial Refrigerator Condensers For Commercial Cooling Systems
Premium industrial refrigerator condensers deliver superior heat transfer and energy efficiency for commercial cooling systems. Built with high-grade materials for reliable performance in demanding environments, ensuring consistent temperature control and reduced operational costs.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Capri Refrigeration
 Gujarat, India
Industrial Equipment & MachineryDistributor / Wholesaler