IN
₹
Apparel & Fashion
Description
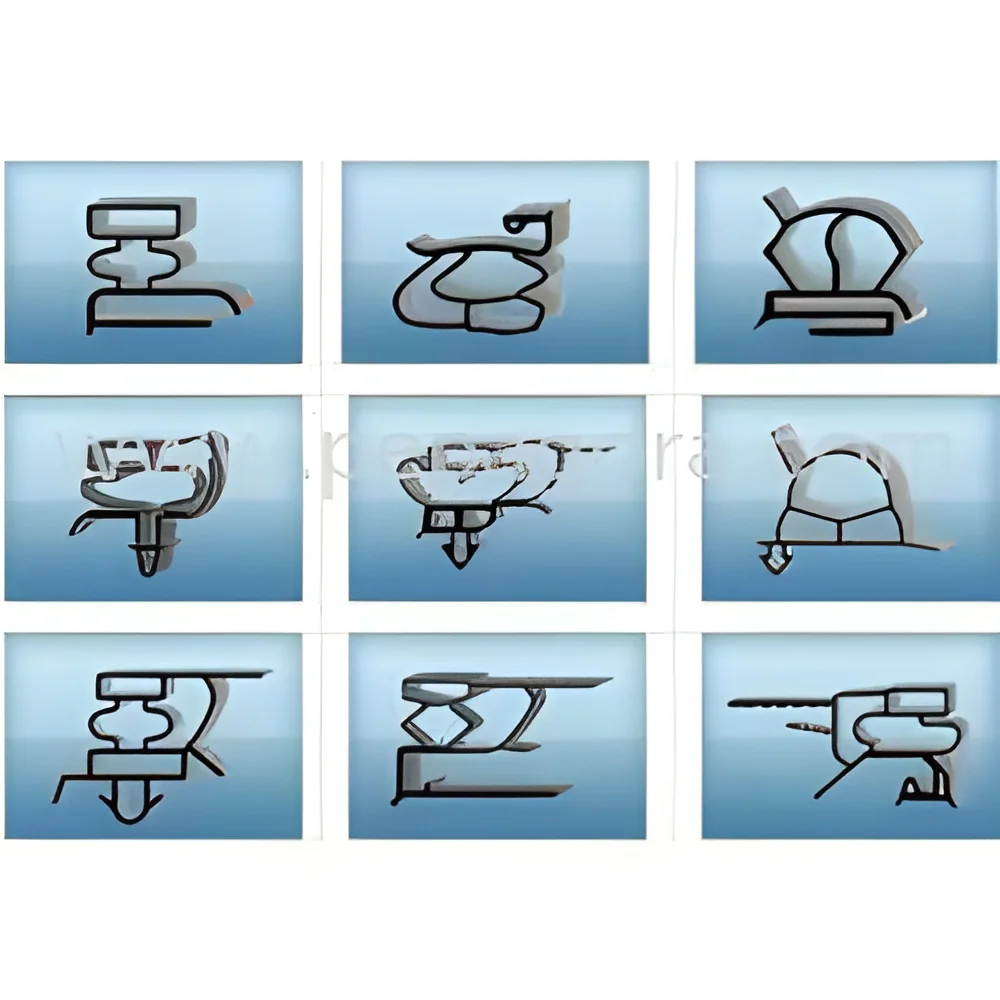
Our premium refrigeration gaskets are engineered to deliver exceptional sealing performance in demanding temperature environments. Manufactured under strict ISO standards with comprehensive quality control protocols, these gaskets ensure reliable operation and extended service life for various commercial and industrial refrigeration applications. We utilize superior raw materials from verified suppliers to guarantee consistent quality, performance, and durability against environmental factors and mechanical wear. Each gasket undergoes rigorous testing for compression set, temperature resistance, and longevity to meet exacting industry standards.

These refrigeration gaskets serve critical functions across multiple industries where temperature control is paramount. In food service and hospitality, they maintain proper sealing for commercial refrigerators, freezers, and walk-in coolers. Pharmaceutical and medical facilities rely on them for precise temperature maintenance in drug storage...
Our premium refrigeration gaskets are engineered to deliver exceptional sealing performance in demanding temperature environments. Manufactured under strict ISO standards with comprehensive quality control protocols, these gaskets ensure reliable operation and extended service life for various commercial and industrial refrigeration applications. We utilize superior raw materials from verified suppliers to guarantee consistent quality, performance, and durability against environmental factors and mechanical wear. Each gasket undergoes rigorous testing for compression set, temperature resistance, and longevity to meet exacting industry standards.

These refrigeration gaskets serve critical functions across multiple industries where temperature control is paramount. In food service and hospitality, they maintain proper sealing for commercial refrigerators, freezers, and walk-in coolers. Pharmaceutical and medical facilities rely on them for precise temperature maintenance in drug storage and laboratory refrigeration units. Retail supermarkets utilize these gaskets for display cases, while food processing plants and industrial cold storage facilities depend on them for large-scale refrigeration systems operating continuously under heavy use conditions.

The business value of our refrigeration gaskets lies in their reliability, energy efficiency, and cost-effectiveness. By providing superior sealing that prevents cold air leakage, they significantly reduce energy consumption and operational costs. Their durability minimizes maintenance requirements and downtime, extending the lifespan of expensive refrigeration equipment. The availability of both magnetic and non-magnetic options ensures perfect compatibility with various refrigeration systems. This reliability makes them ideal for businesses that cannot afford temperature fluctuations or system failures.

Key Features:
- ISO certified manufacturing process ensuring international quality standards
- Available in both magnetic and non-magnetic variants for different applications
- Premium raw materials from verified vendors for consistent performance
- Rigorous quality control and testing protocols for reliability assurance
- Designed for durability in extreme temperature environments

Benefits:
- Reduces energy consumption by preventing cold air leakage
- Extends equipment lifespan through reliable sealing performance
- Minimizes maintenance requirements and operational downtime
- Ensures consistent temperature control for product safety
- Provides reliable operation in demanding industrial environments
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our ISO-certified refrigeration gaskets deliver critical temperature sealing for commercial refrigeration systems across multiple sectors. They ensure energy efficiency by preventing cold air leakage in walk-in coolers, display cases, and freezer doors while maintaining consistent internal temperatures. These gaskets are essential for both new installations and replacement projects where reliable performance is non-negotiable.
These sealing solutions are widely adopted in food service, pharmaceutical storage, hospitality, and retail sectors. They meet demanding requirements of medical refrigeration, laboratory environments, and food processing facilities where temperature integrity directly impacts product safety and quality. The gaskets maintain sealing properties even under frequent door operations and extreme conditions.
- Commercial refrigerator and freezer door seals in restaurants and hotels
- Walk-in cooler and cold room sealing systems for food storage facilities
- Display case gaskets for supermarkets and retail refrigeration units
- Medical and pharmaceutical refrigeration units requiring precise temperature control
- Industrial cold storage and food processing plant refrigeration systems
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Acme Plastics, Haryana
 Haryana, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Commercial Refrigeration Gaskets Magnetic Non Magnetic ISO Certified
ISO-certified commercial refrigeration gaskets in magnetic and non-magnetic types provide reliable sealing and durability for extreme temperature environments across industrial applications.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Acme Plastics
 Haryana, India
Industrial Equipment & MachineryManufacturer