IN
₹
Apparel & Fashion
Description
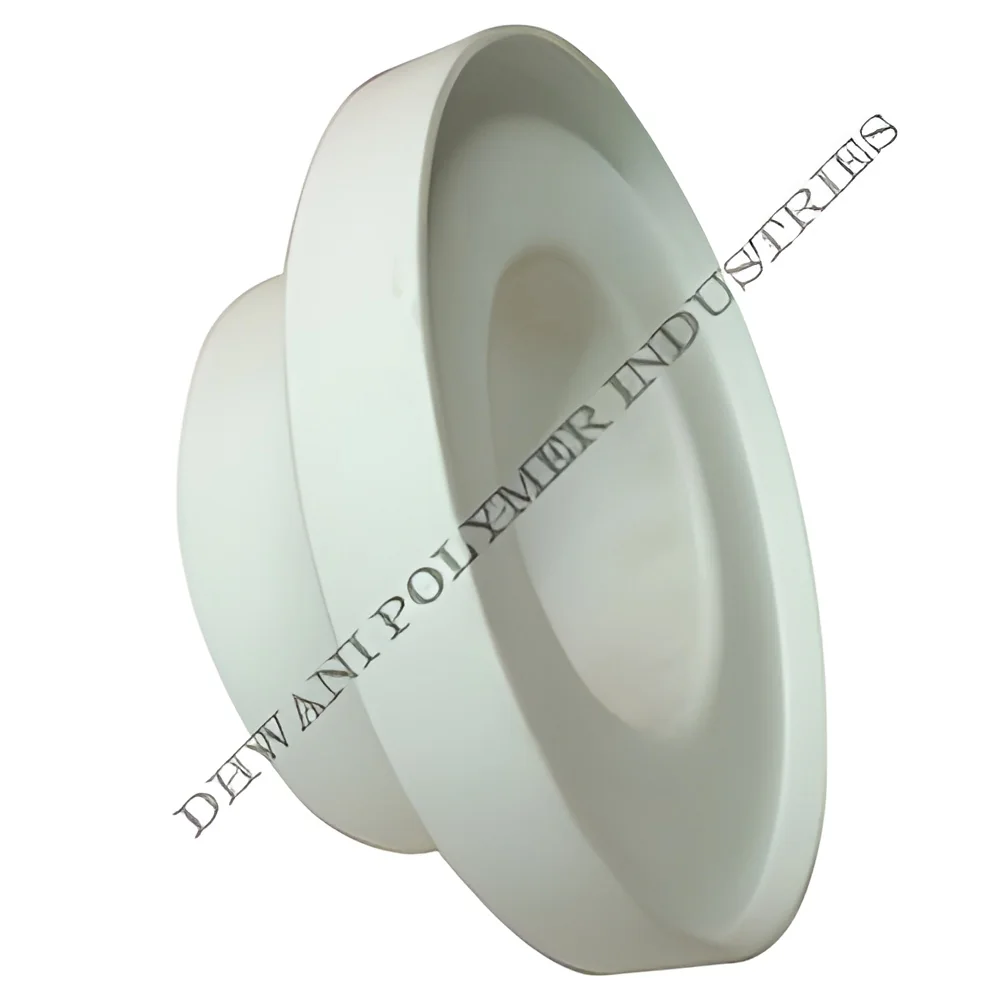
Industrial PTFE V Rings represent advanced sealing solutions engineered for high-performance applications across demanding industrial sectors. Manufactured from premium polytetrafluoroethylene material, these rings provide superior leakage prevention in mechanical systems involving shafts, rotating equipment, and fluid handling components. The distinctive V-shaped design ensures optimal sealing contact with mating surfaces, creating reliable barriers against fluid and gas escape while accommodating various operational movements. These components maintain structural integrity under extreme pressure conditions while offering exceptional chemical resistance against aggressive media including acids, solvents, and corrosive substances. The thermal stability range from -100°C to 260°C ensures consistent performance across temperature variations commonly encountered in industrial processes.

These sealing rings serve essential functions across multiple industrial sectors including chemical pr...
Industrial PTFE V Rings represent advanced sealing solutions engineered for high-performance applications across demanding industrial sectors. Manufactured from premium polytetrafluoroethylene material, these rings provide superior leakage prevention in mechanical systems involving shafts, rotating equipment, and fluid handling components. The distinctive V-shaped design ensures optimal sealing contact with mating surfaces, creating reliable barriers against fluid and gas escape while accommodating various operational movements. These components maintain structural integrity under extreme pressure conditions while offering exceptional chemical resistance against aggressive media including acids, solvents, and corrosive substances. The thermal stability range from -100°C to 260°C ensures consistent performance across temperature variations commonly encountered in industrial processes.

These sealing rings serve essential functions across multiple industrial sectors including chemical processing, oil and gas exploration, pharmaceutical manufacturing, water treatment facilities, and food processing operations. In chemical plants, they effectively seal pumps and valves handling aggressive acids, alkalis, and solvents where conventional seals would rapidly deteriorate. The oil and gas industry relies on them for drilling equipment, pipeline systems, and refinery applications where they withstand high pressures and corrosive media. Pharmaceutical manufacturers value their non-contaminating properties in processing equipment requiring sterile conditions, while water treatment plants utilize their durability in pumps and filtration systems handling various water qualities. Food processing applications benefit from their compliance with food safety standards and clean operation characteristics.

The operational value of PTFE V Rings lies in their reliability and cost-effectiveness through reduced maintenance requirements and extended equipment service life. These rings significantly minimize operational downtime by providing consistent sealing performance in challenging conditions, directly enhancing production efficiency and system reliability. Their exceptional wear resistance and low friction properties translate to longer replacement intervals, reducing inventory costs and maintenance overhead. The availability in multiple standard sizes ensures compatibility with various equipment specifications, while the material's non-stick characteristics prevent material buildup and ensure consistent performance throughout the product lifecycle. Manufacturers benefit from improved system integrity and reduced leakage-related losses, contributing to overall operational excellence and cost management.

Key Features:
- Premium PTFE material providing superior chemical resistance against aggressive media
- V-shaped design ensuring optimal sealing contact and pressure distribution
- Exceptional thermal stability maintaining performance from -100°C to 260°C
- Low friction coefficient reducing wear on mating surfaces and components
- Multiple standard sizes available for various shaft and equipment requirements

Benefits:
- Extended service life reducing replacement frequency and maintenance costs
- Reliable leakage prevention enhancing operational safety and efficiency
- Chemical compatibility with diverse media including acids and solvents
- Consistent performance across temperature variations and pressure conditions
- Non-contaminating properties suitable for sensitive processing applications
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
PTFE V Rings deliver exceptional sealing performance in challenging industrial environments where chemical resistance and thermal stability are critical. These rings maintain integrity when exposed to aggressive chemicals, extreme temperatures, and high-pressure conditions, outperforming conventional sealing materials. Their durable construction ensures long service life while preventing fluid and gas leakage in rotating equipment and mechanical systems.
These sealing solutions are engineered for diverse industrial applications requiring reliable performance under demanding operational conditions. The V-ring design provides effective sealing contact while accommodating various shaft sizes and movement types. Industries utilize these components for their non-contaminating properties, low friction operation, and ability to withstand harsh processing environments without degradation or performance loss.
- Hydraulic and pneumatic systems requiring reliable shaft sealing under pressure
- Chemical processing equipment handling corrosive acids and solvents
- Oil and gas industry valves, pumps, and drilling equipment
- Pharmaceutical manufacturing machinery needing sterile, non-contaminating seals
- Water treatment plants and irrigation systems with rotating components
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Dhwani Polymer Industries, Gujarat
 Gujarat, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial PTFE V Rings For High Performance Sealing Applications
Industrial PTFE V Rings provide high-performance sealing for shafts and mechanical systems. These durable PTFE seals prevent leakage in demanding applications across multiple industries with reliable chemical resistance and thermal stability from -100°C to 260°C.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Dhwani Polymer Industries
 Gujarat, India
Industrial Equipment & MachineryManufacturer