IN
₹
Apparel & Fashion
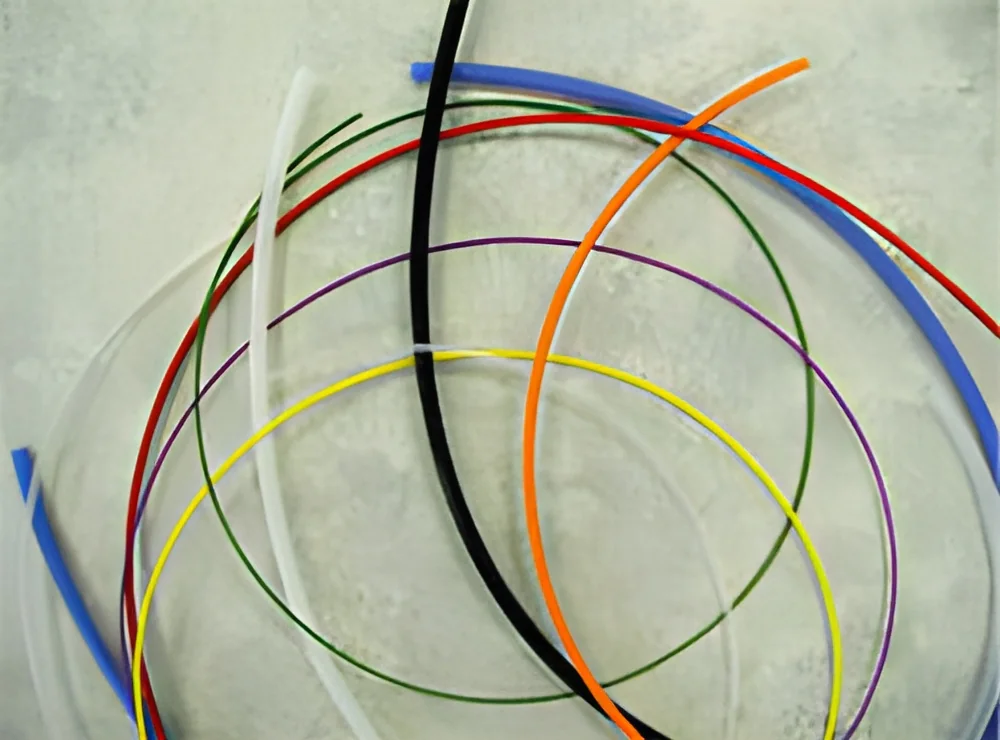
Description
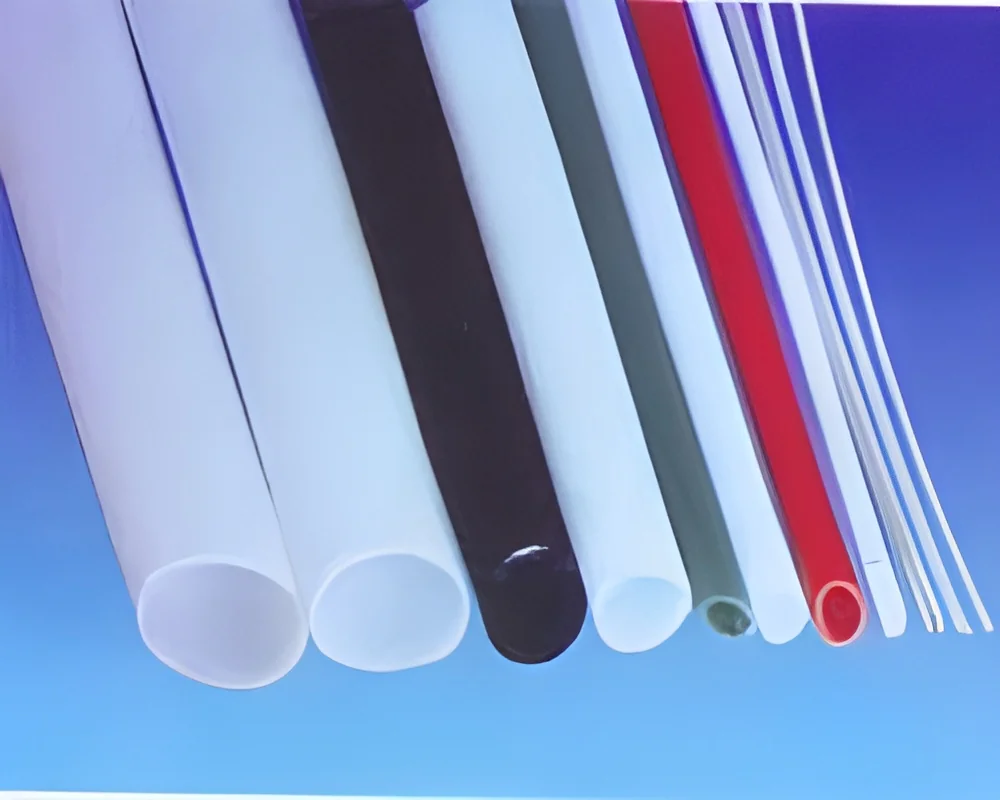
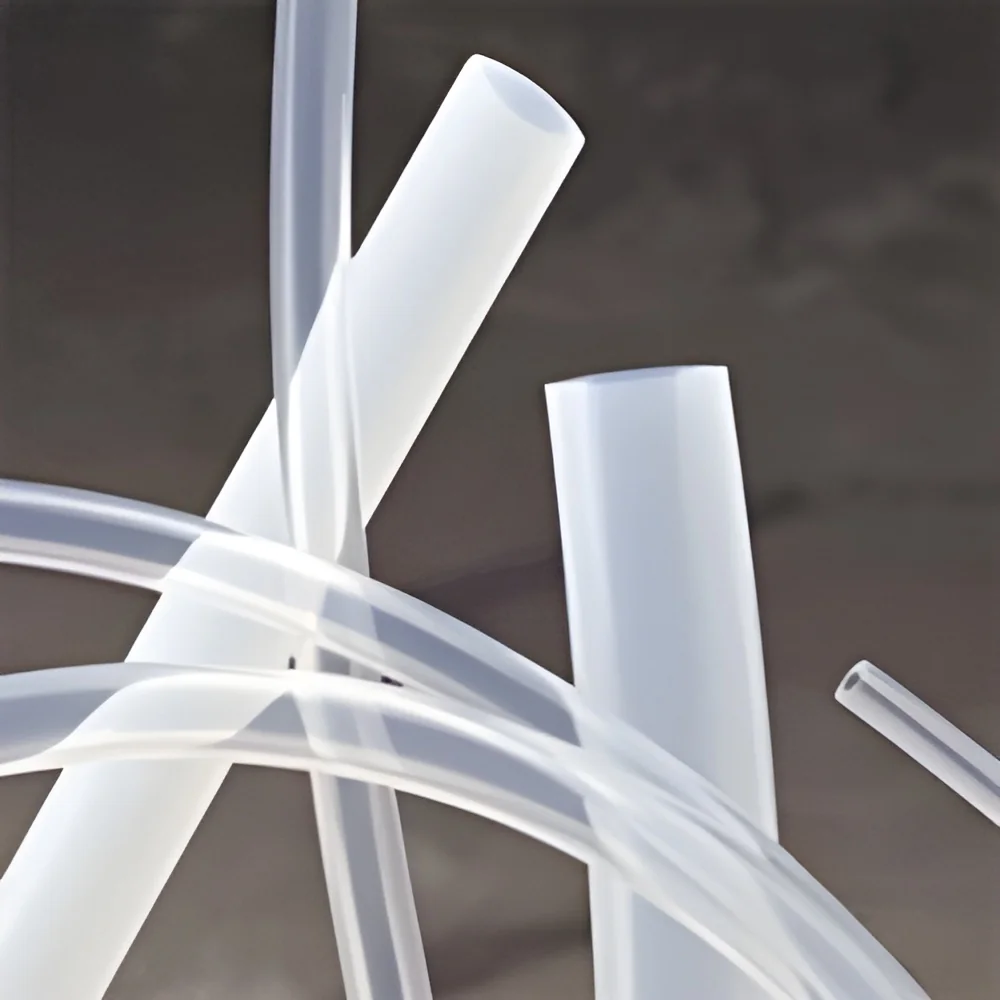
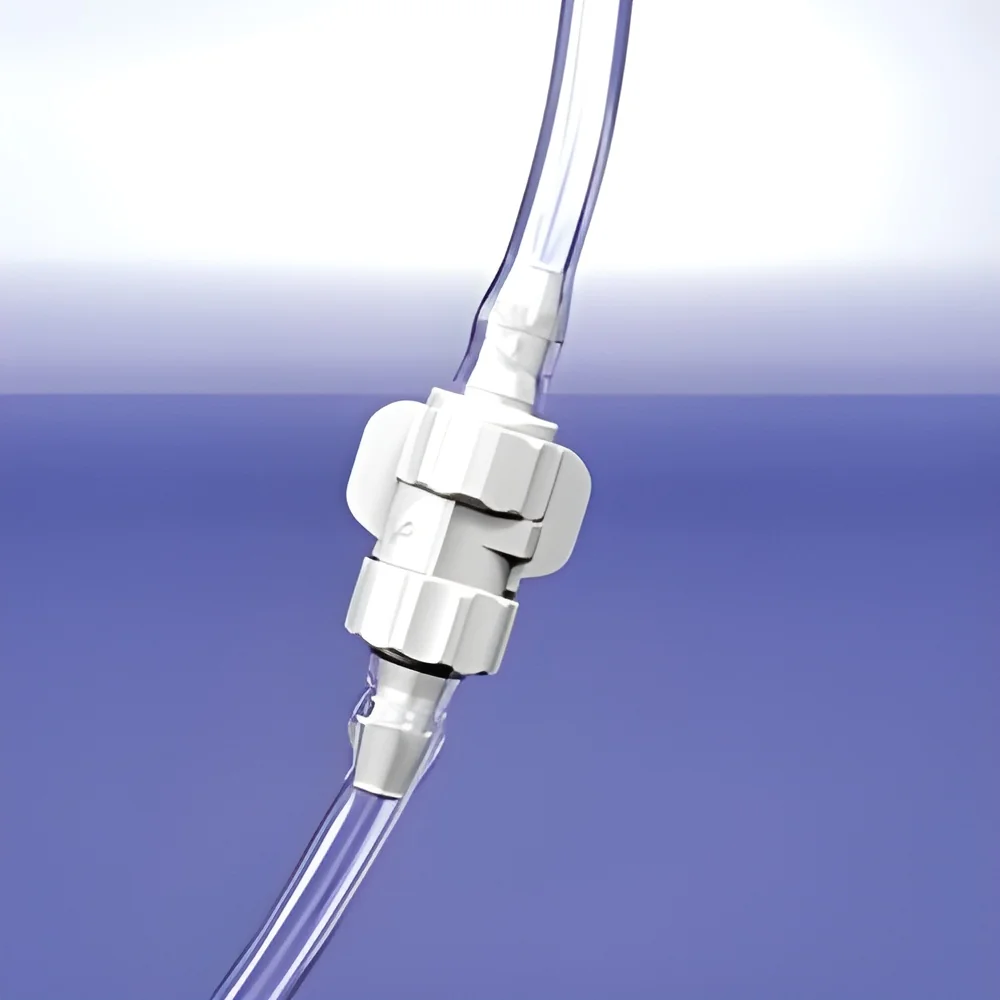
Industrial PTFE tubing sets the standard for reliability in demanding fluid transfer applications. Manufactured from premium polytetrafluoroethylene, this tubing offers unmatched chemical resistance against virtually all aggressive chemicals, acids, and solvents. The smooth, non-stick interior surface minimizes friction loss and prevents material buildup, ensuring consistent flow performance over extended operational periods. Its exceptional thermal stability maintains structural integrity across extreme temperature ranges from cryogenic conditions to high-heat processes, outperforming alternative tubing materials in challenging industrial environments.

Numerous industries depend on PTFE tubing for critical operations where failure is not an option. Chemical processing facilities utilize it for safely transferring corrosive substances between reactors and storage vessels. Automotive manufacturers incorporate it in fuel and brake systems where reliability is essential. Pharmaceutical a...
Industrial PTFE tubing sets the standard for reliability in demanding fluid transfer applications. Manufactured from premium polytetrafluoroethylene, this tubing offers unmatched chemical resistance against virtually all aggressive chemicals, acids, and solvents. The smooth, non-stick interior surface minimizes friction loss and prevents material buildup, ensuring consistent flow performance over extended operational periods. Its exceptional thermal stability maintains structural integrity across extreme temperature ranges from cryogenic conditions to high-heat processes, outperforming alternative tubing materials in challenging industrial environments.

Numerous industries depend on PTFE tubing for critical operations where failure is not an option. Chemical processing facilities utilize it for safely transferring corrosive substances between reactors and storage vessels. Automotive manufacturers incorporate it in fuel and brake systems where reliability is essential. Pharmaceutical and food processing operations value its compliant, non-contaminating properties for maintaining product purity. Electrical sectors employ it as high-temperature insulation for wiring and components, while semiconductor manufacturers use it in ultra-pure fluid handling systems where microscopic contamination must be eliminated.

Organizations select PTFE tubing for its proven reliability and long-term cost effectiveness despite higher initial investment. The material's exceptional durability translates to reduced downtime and maintenance expenses, delivering superior return on investment compared to conventional tubing solutions. Consistent quality assurance and technical support ensure every length of tubing meets rigorous industry standards and performance expectations. The tubing's versatility allows for seamless integration into existing systems, providing reliable performance across diverse industrial applications.

Key Features:
- Exceptional chemical resistance against acids, solvents, and aggressive chemicals
- Wide temperature range from -200°C to +260°C for versatile applications
- Non-stick interior surface prevents material buildup and maintains flow efficiency
- FDA compliant material suitable for food and pharmaceutical industries
- Available in various diameters and wall thicknesses for specific needs

Benefits:
- Reduced maintenance costs through exceptional durability and chemical resistance
- Versatile application across extreme temperature environments
- Consistent flow performance with minimal friction loss
- Compliance with purity standards for sensitive industries
- Reliable performance in demanding industrial conditions
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
PTFE tubing delivers exceptional performance in challenging environments due to its outstanding chemical resistance and thermal stability. This tubing maintains integrity across extreme temperatures from -200°C to +260°C, making it suitable for both high-heat processes and cryogenic applications. The non-stick surface prevents material accumulation, ensuring consistent flow rates and reducing maintenance requirements in processing systems.
Multiple sectors utilize PTFE tubing for transferring aggressive chemicals, high-purity fluids, and gases safely. The material meets FDA standards, making it appropriate for applications where contamination must be prevented. Manufacturers value the tubing's flexibility and durability for specific operational needs, with options available in various diameters and wall thicknesses to match system requirements.
- Chemical plants transfer corrosive acids and solvents through PTFE tubing systems
- Automotive manufacturers use it in fuel lines and brake systems for reliability
- Pharmaceutical companies employ it in sterile fluid transfer applications
- Food processing facilities convey ingredients without contamination risk
- Electrical industries utilize it as insulation for high-temperature wiring
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Arizona Tech- Zeal, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Trading Company•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial PTFE Tubing High Temperature Chemical Resistance Electrical Insulation
Industrial PTFE tubing provides high temperature resistance, excellent chemical compatibility, and superior electrical insulation for demanding applications across chemical processing, automotive, and pharmaceutical industries. This reliable tubing withstands extreme conditions while maintaining performance.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Arizona Tech- Zeal
 Maharashtra, India
Industrial Equipment & MachineryTrading Company