IN
₹
Description
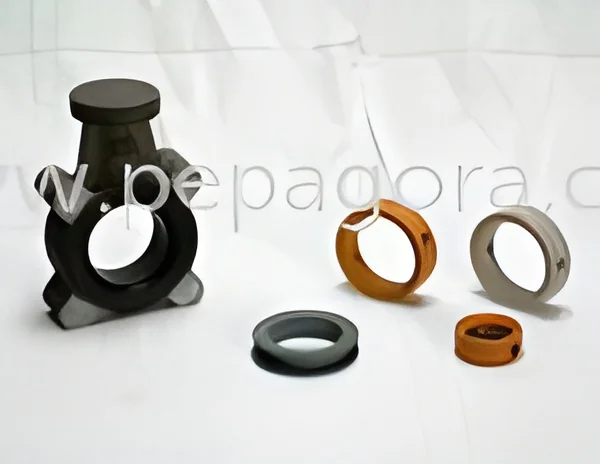
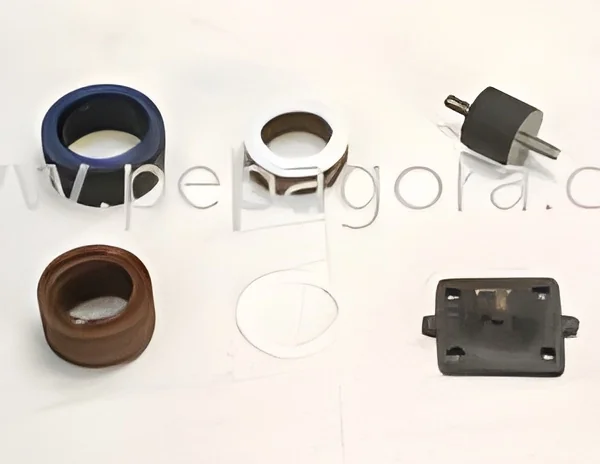
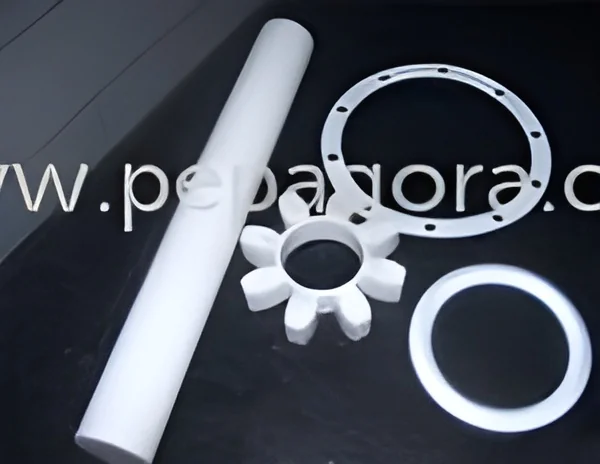
Our premium PTFE industrial products are engineered to deliver exceptional performance in the most demanding operational environments. These materials provide outstanding chemical resistance, low friction characteristics, and thermal stability that remains consistent across extreme temperature ranges. Manufactured to precise specifications, our PTFE solutions ensure reliable performance for industrial buyers, importers, and distributors who require dependable components for their critical machinery and processes. The material's inherent properties make it suitable for applications where failure is not an option, providing consistent performance day after day in challenging conditions.

PTFE serves critical functions across multiple industrial sectors including chemical processing, automotive manufacturing, food production, pharmaceuticals, and electronics. In chemical plants, PTFE components handle aggressive acids, bases, and solvents without degradation. Automotive applications benef...
Our premium PTFE industrial products are engineered to deliver exceptional performance in the most demanding operational environments. These materials provide outstanding chemical resistance, low friction characteristics, and thermal stability that remains consistent across extreme temperature ranges. Manufactured to precise specifications, our PTFE solutions ensure reliable performance for industrial buyers, importers, and distributors who require dependable components for their critical machinery and processes. The material's inherent properties make it suitable for applications where failure is not an option, providing consistent performance day after day in challenging conditions.

PTFE serves critical functions across multiple industrial sectors including chemical processing, automotive manufacturing, food production, pharmaceuticals, and electronics. In chemical plants, PTFE components handle aggressive acids, bases, and solvents without degradation. Automotive applications benefit from low-friction bearings and seals that withstand high operating temperatures and harsh conditions. Food processing facilities rely on PTFE for non-stick surfaces that meet strict hygiene standards while pharmaceutical operations utilize biocompatible PTFE components in manufacturing processes and medical devices. This broad industry adoption demonstrates the material's versatility and essential role in modern industrial operations.

The business value of our PTFE products lies in their ability to enhance operational efficiency, reduce maintenance costs, and extend equipment lifespan. Their exceptional durability translates to fewer replacements and less downtime, providing substantial return on investment over time. Supported by rigorous quality control measures, these products ensure compliance with relevant industry standards and regulatory requirements. This reliability makes them a trusted choice for industries where component failure could lead to significant operational disruptions, safety concerns, or compliance issues, giving businesses confidence in their critical operations.

Key Features:
- Exceptional chemical resistance to acids, bases, solvents, and corrosive substances
- Wide operating temperature range from -200°C to +260°C for extreme environments
- Very low coefficient of friction providing superior non-stick properties
- High dielectric strength suitable for electrical insulation applications
- Consistent performance and dimensional stability under varying conditions

Benefits:
- Reduced maintenance costs and extended equipment lifespan through superior durability
- Enhanced operational safety in hazardous chemical and high-temperature environments
- Improved process efficiency with reliable non-stick and low-friction performance
- Compliance with industry standards for food, pharmaceutical, and chemical applications
- Long-term cost savings through reduced replacement frequency and downtime
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
PTFE products are engineered for extreme industrial environments where chemical inertness, thermal stability, and low friction are essential. They maintain performance in corrosive settings, high-temperature operations, and applications requiring minimal friction, ensuring long-term durability and safety across critical processes. These versatile materials are indispensable for components facing aggressive chemicals, extreme temperatures, or strict hygiene requirements. From chemical seals to food-grade linings and high-performance bearings, PTFE solutions enhance efficiency, reduce maintenance, and support compliance in regulated environments where reliability is paramount.
Real-world applications:
- Seals and gaskets in chemical processing equipment handling corrosive acids and solvents
- Non-stick coatings for food processing machinery to prevent sticking and simplify cleaning
- High-temperature electrical insulation components in electronics and power distribution systems
- Low-friction bearings and sliding parts in automotive and aerospace assemblies
- Biocompatible tubing and components for pharmaceutical manufacturing and medical devices
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Pravin Rubber & Engg Works, Gujarat
 Gujarat, India
Industrial Equipment & Machinery•Manufacturer
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial PTFE Products Chemical Resistance Low Friction Thermal Stability
Premium PTFE industrial products deliver unmatched chemical resistance, low friction, and thermal stability for demanding applications in chemical processing, automotive, food, and pharmaceutical industries.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Pravin Rubber & Engg Works
 Gujarat, India
Industrial Equipment & MachineryManufacturer