IN
₹
Description
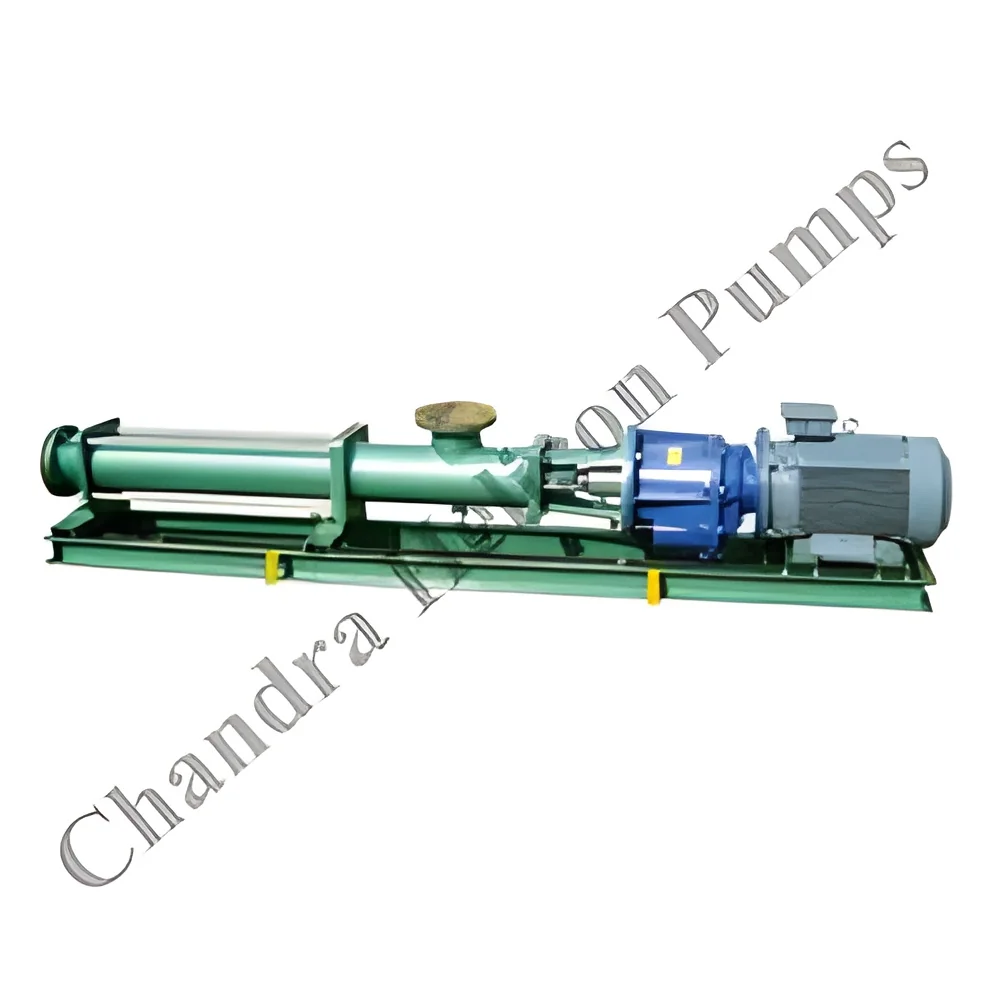
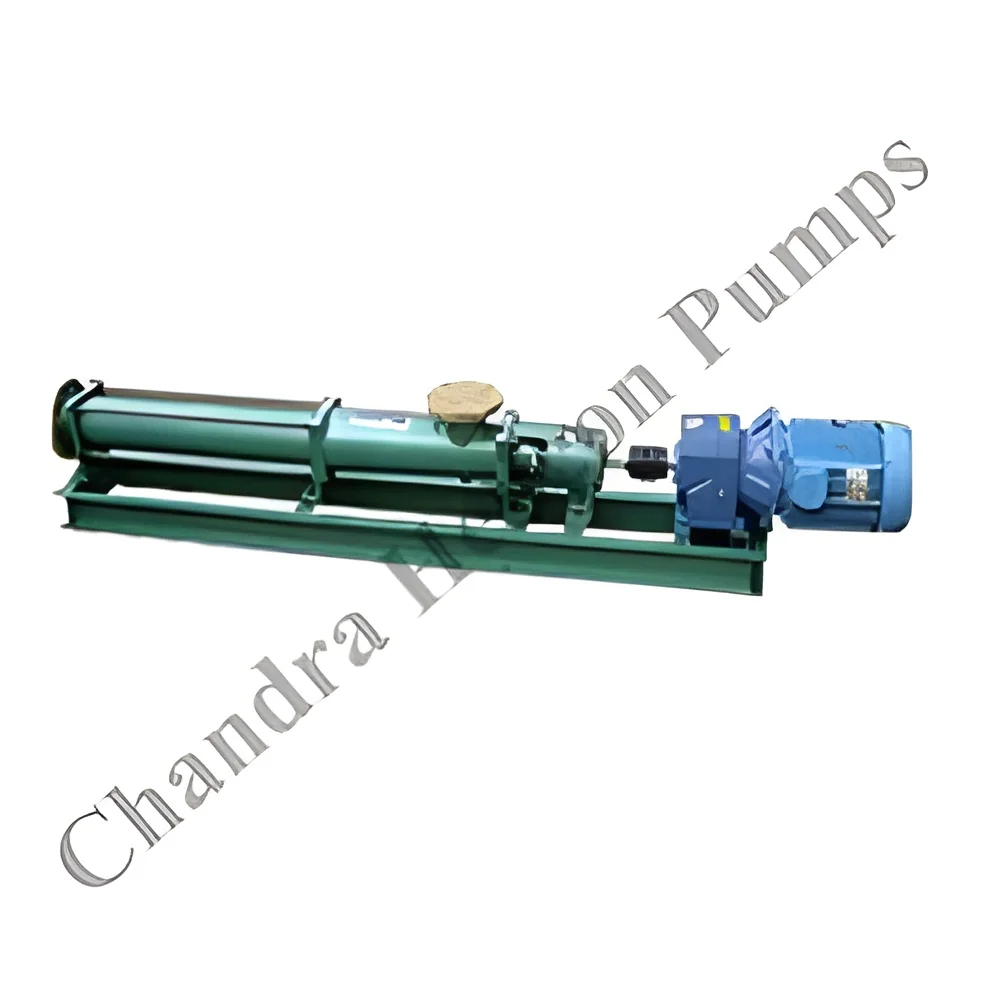
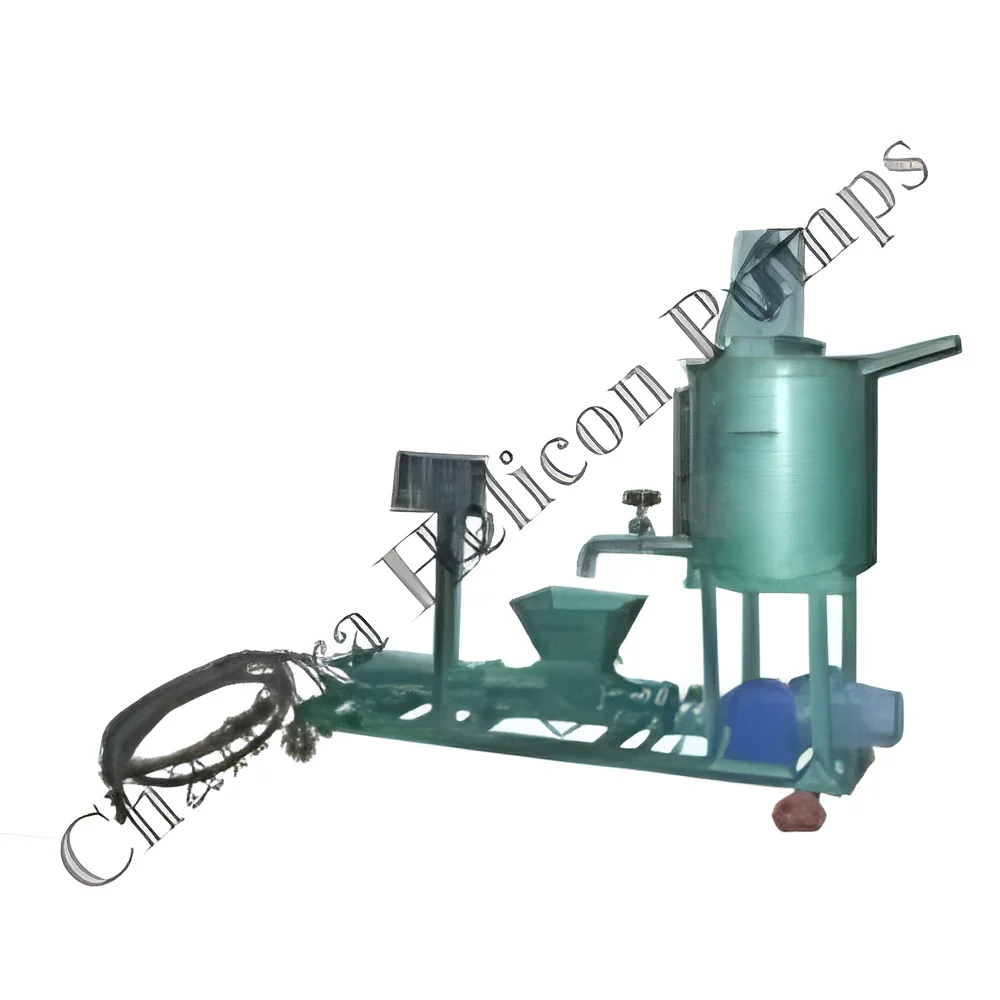
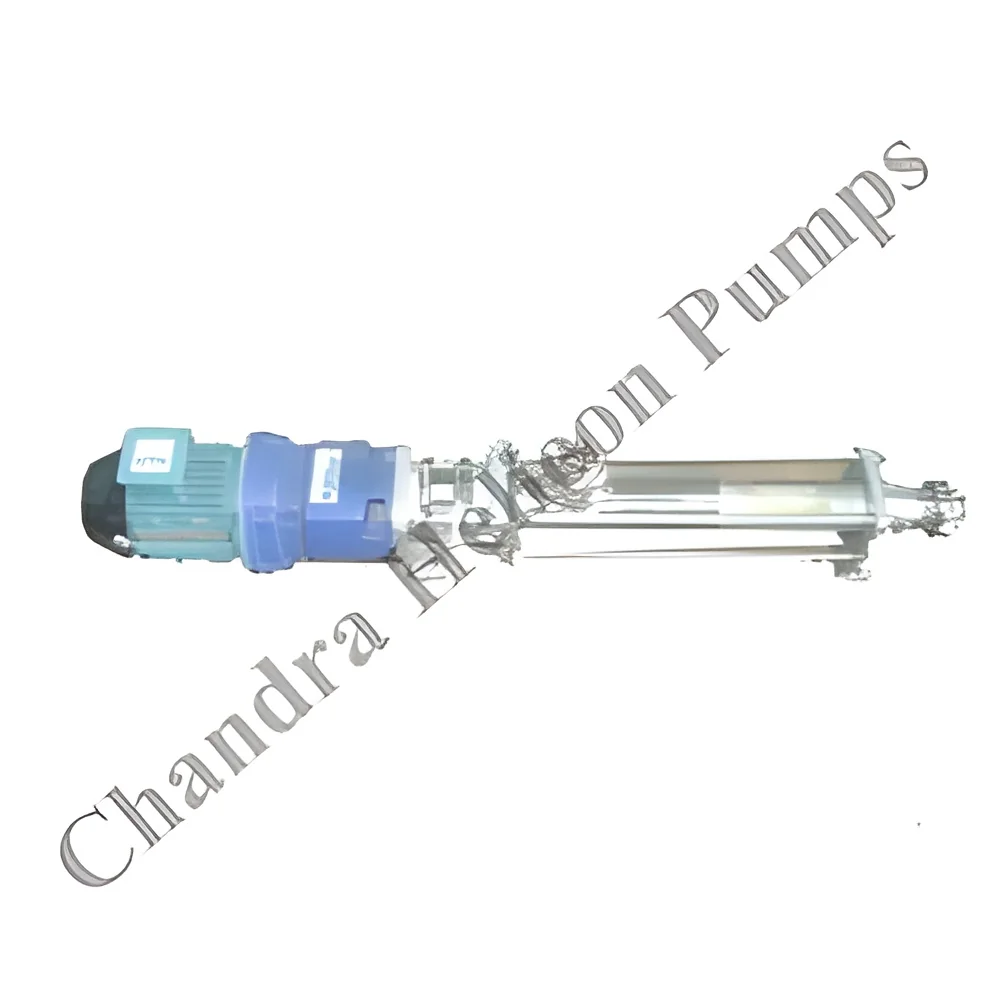
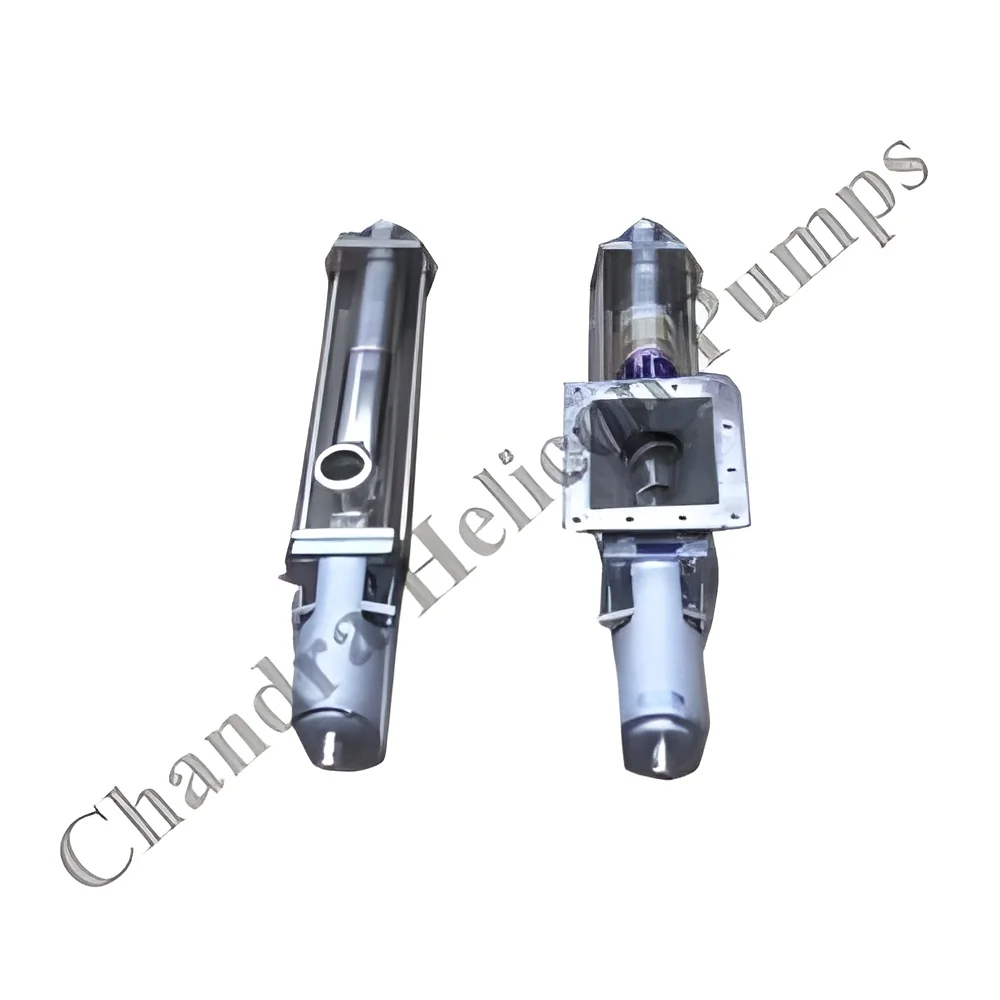
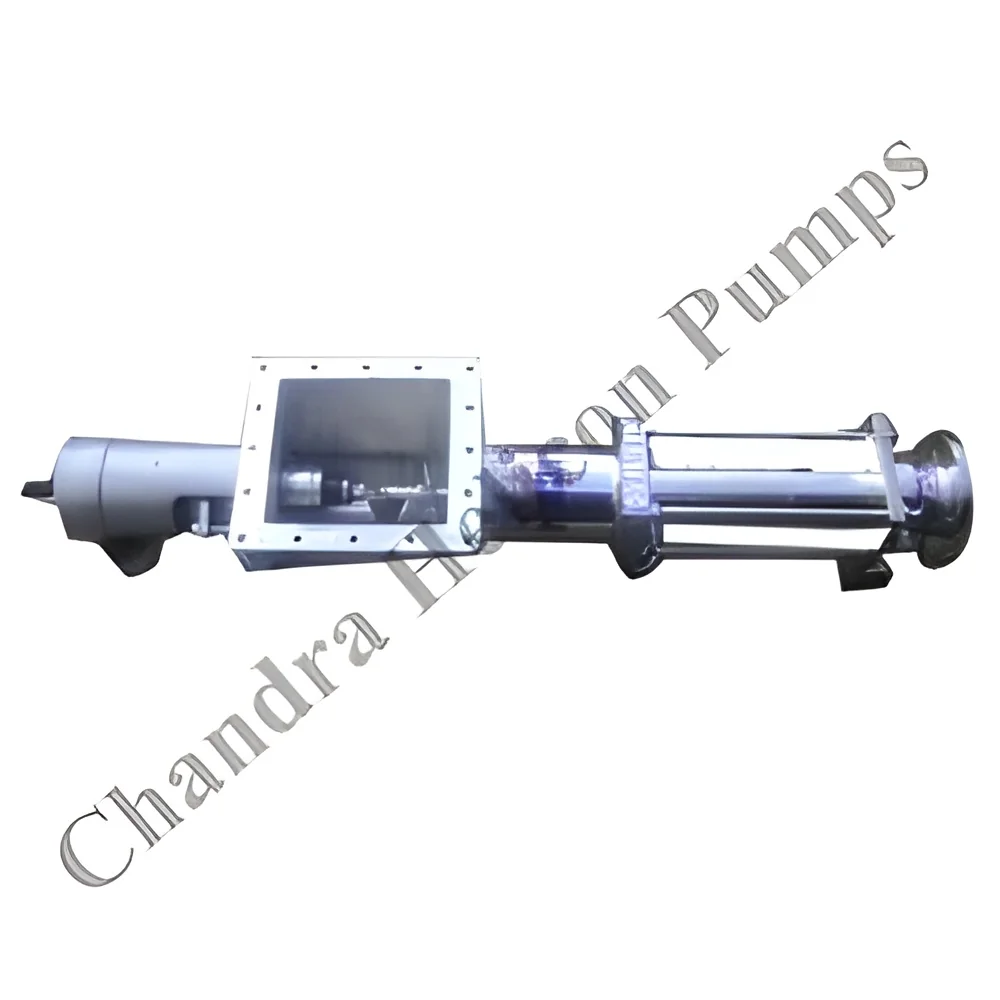
Our industrial progressive cavity pumps are precision-engineered for the demanding task of transferring viscous, abrasive, and corrosive fluids. Manufactured from premium materials like stainless steel and specially treated alloy components, these pumps are built to withstand harsh industrial environments. The core single-helical rotor and double-helical stator design ensures a smooth, non-pulsating flow that protects sensitive products from shear damage. Every unit undergoes stringent quality assurance, delivering a reliable pumping solution that minimizes downtime and maximizes process efficiency for critical operations.

These pumps serve as workhorses in numerous industrial sectors. In chemical and pharmaceutical plants, they reliably handle aggressive acids, alkalis, and abrasive slurries. The food and beverage industry utilizes them for pumping everything from delicate sauces and dairy products to thick pastes and molasses, maintaining strict hygiene and product integrity. Enviro...
Our industrial progressive cavity pumps are precision-engineered for the demanding task of transferring viscous, abrasive, and corrosive fluids. Manufactured from premium materials like stainless steel and specially treated alloy components, these pumps are built to withstand harsh industrial environments. The core single-helical rotor and double-helical stator design ensures a smooth, non-pulsating flow that protects sensitive products from shear damage. Every unit undergoes stringent quality assurance, delivering a reliable pumping solution that minimizes downtime and maximizes process efficiency for critical operations.

These pumps serve as workhorses in numerous industrial sectors. In chemical and pharmaceutical plants, they reliably handle aggressive acids, alkalis, and abrasive slurries. The food and beverage industry utilizes them for pumping everything from delicate sauces and dairy products to thick pastes and molasses, maintaining strict hygiene and product integrity. Environmental and municipal applications depend on their robust, non-clogging design for wastewater treatment and sludge transfer. Additionally, they are indispensable in mining for mineral slurries, in oil and gas for multiphase fluids, and in manufacturing for paints, adhesives, and ceramic glazes.

The business value of these pumps is rooted in their exceptional reliability, durability, and low total cost of ownership. Their robust construction reduces maintenance frequency and withstands punishing conditions, leading to extended service life and less production downtime. The energy-efficient, positive displacement operation ensures consistent performance regardless of viscosity or pressure changes, optimizing process control. This operational reliability translates directly into improved productivity, reduced operational costs, and enhanced safety for handling hazardous or valuable fluids, making them a sound long-term investment for your fluid management needs.

Key Features:
- Constructed with high-grade materials including stainless steel, cast iron, and wear-resistant alloy steel for longevity.
- Positive displacement design delivers consistent, pulse-free flow rates for precise metering of difficult fluids.
- Self-priming capability and excellent suction lift for versatile installation and operation.
- Non-clogging rotor-stator design efficiently handles fluids with high solid content and abrasive particles.
- Hard chrome-plated rotor and resilient stator materials provide enhanced resistance to wear and corrosion.

Benefits:
- Ensures reliable and uninterrupted transfer of challenging fluids, minimizing process downtime.
- Protects product integrity with gentle, low-shear pumping action suitable for sensitive materials.
- Reduces maintenance costs and extends service intervals through durable, wear-resistant construction.
- Offers energy-efficient operation with consistent performance across varying viscosity and pressure conditions.
- Provides versatile application across multiple industries with a single, robust pumping solution.
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Progressive cavity pumps are engineered to master the most challenging fluid transfer tasks. Their positive displacement design guarantees a consistent, pulse-free flow, even with high-viscosity liquids, abrasive slurries, or shear-sensitive products. This makes them a critical component where other pumps fail, ensuring precision and operational reliability in processes that cannot tolerate interruptions or product damage.
These versatile pumps are fundamental across heavy industries, providing dependable solutions for moving difficult materials. They are extensively used in chemical processing for aggressive fluids, in food production for delicate ingredients, and in wastewater management for solids-laden sludge. Their non-clogging operation and ability to handle everything from corrosive acids to viscous oils make them the preferred choice for engineers seeking efficient and trouble-free transfer systems.
- Safely transferring corrosive chemical solutions and abrasive mineral slurries in processing plants.
- Handling viscous food-grade products like syrups, molasses, and dairy formulations without degradation.
- Managing industrial wastewater, sewage sludge, and effluents containing high solid content.
- Pumping petroleum products, lubricants, and viscous oils in refinery and storage operations.
- Transferring ceramic glazes, paper pulp, and other abrasive suspensions in manufacturing settings.
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Chandra Helicon Pumps Pvt Ltd, Uttar Pradesh
 Uttar Pradesh, India
Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
South Asia
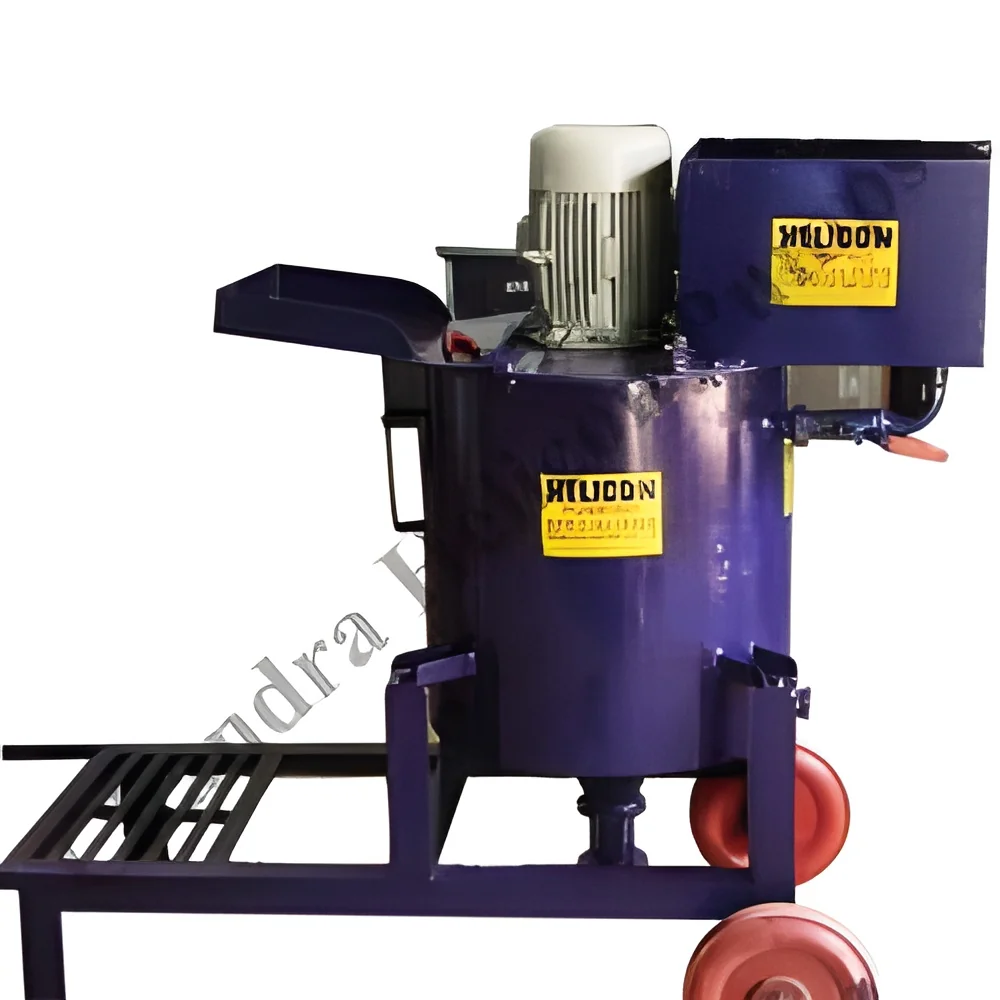
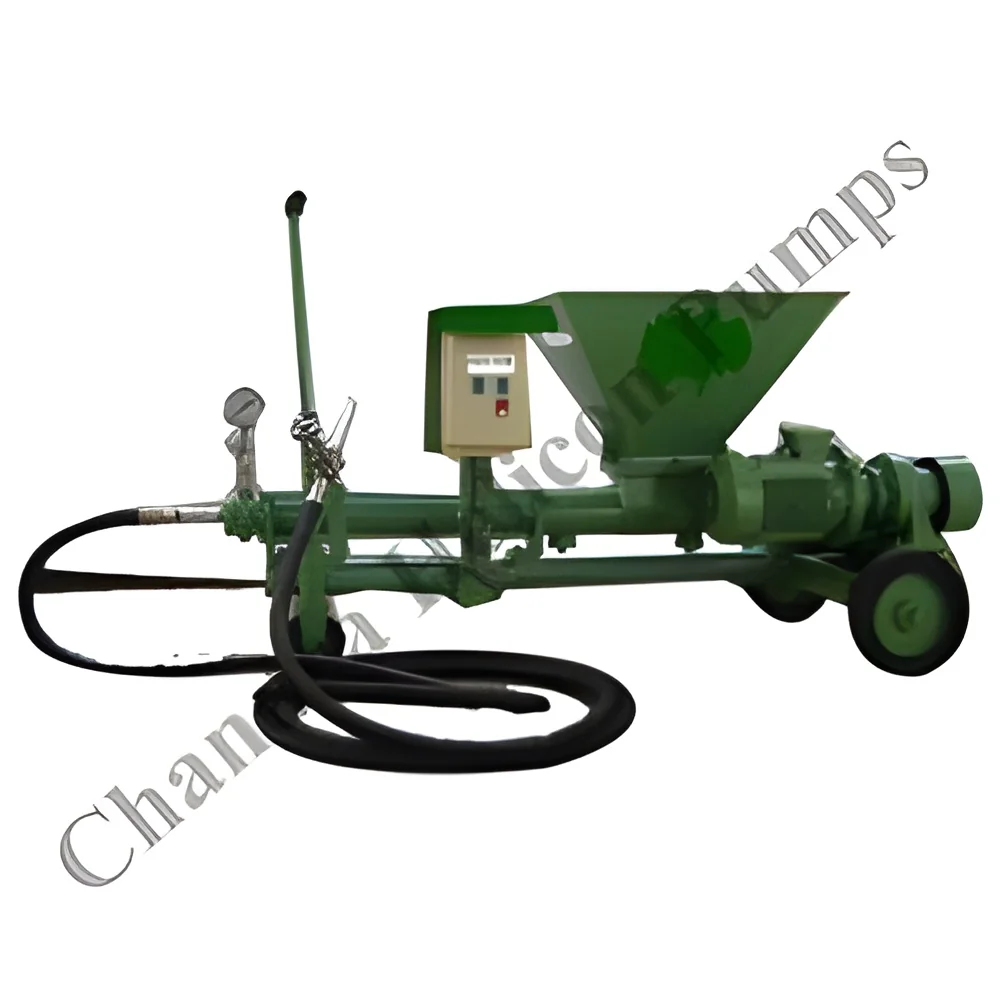
Industrial Progressive Cavity Pumps For Viscous Abrasive Corrosive Fluids
Industrial progressive cavity pumps efficiently transfer viscous, abrasive, and corrosive fluids. Built with robust stainless steel and alloy steel for reliable performance in demanding chemical, food processing, and wastewater applications.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Chandra Helicon Pumps Pvt Ltd
 Uttar Pradesh, India
Manufacturer