IN
₹
Apparel & Fashion
Description
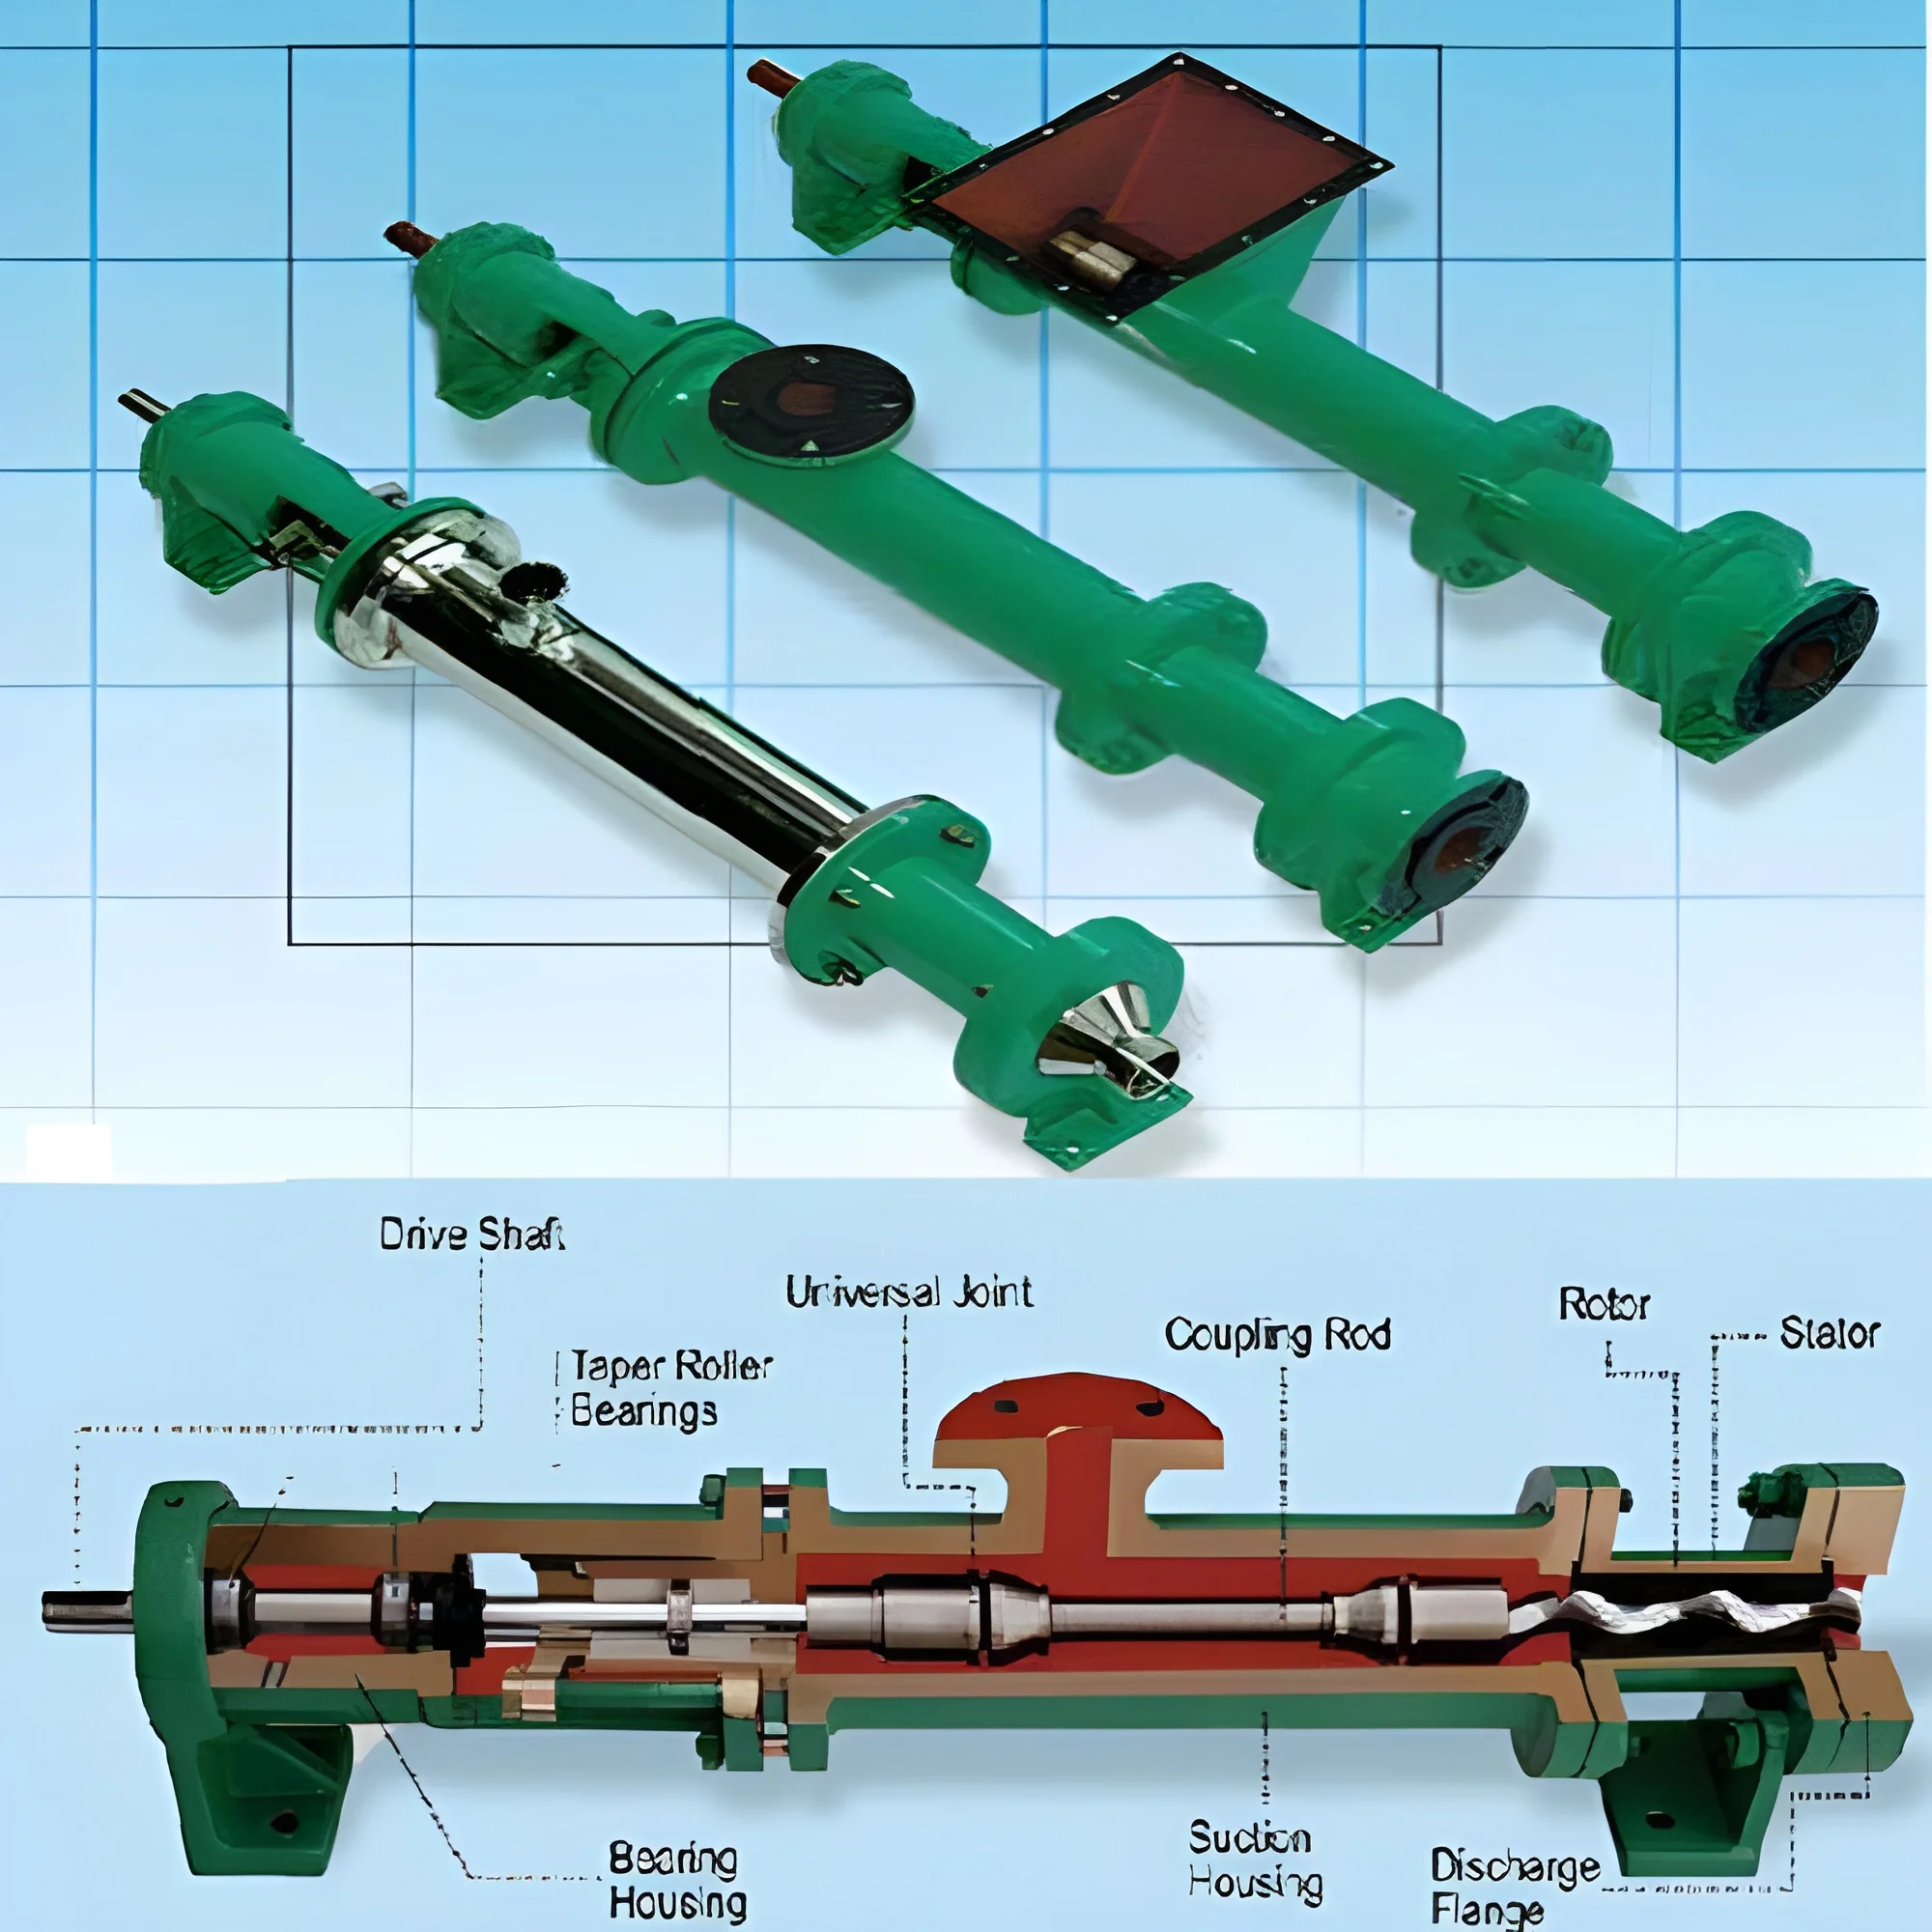
Our industrial process pumps represent the pinnacle of engineering excellence for handling demanding slurry and massecuite applications. These premium pumps are specifically designed to manage abrasive solids, corrosive fluids, and high-viscosity materials with exceptional efficiency and minimal wear. Built to withstand the toughest industrial conditions, they deliver consistent performance while reducing maintenance requirements and operational costs. The robust construction ensures reliable operation in environments where equipment failure can result in significant production losses. Each pump undergoes rigorous quality control to meet the highest industry standards, providing peace of mind for operations managers and plant engineers who depend on uninterrupted performance.

These versatile pumps serve critical functions across multiple industrial sectors with specialized requirements. In mining and mineral processing, they handle abrasive slurries and tailings with remarkable durabi...
Our industrial process pumps represent the pinnacle of engineering excellence for handling demanding slurry and massecuite applications. These premium pumps are specifically designed to manage abrasive solids, corrosive fluids, and high-viscosity materials with exceptional efficiency and minimal wear. Built to withstand the toughest industrial conditions, they deliver consistent performance while reducing maintenance requirements and operational costs. The robust construction ensures reliable operation in environments where equipment failure can result in significant production losses. Each pump undergoes rigorous quality control to meet the highest industry standards, providing peace of mind for operations managers and plant engineers who depend on uninterrupted performance.

These versatile pumps serve critical functions across multiple industrial sectors with specialized requirements. In mining and mineral processing, they handle abrasive slurries and tailings with remarkable durability. The sugar industry relies on our massecuite pumps for gentle transfer of high-viscosity sugar products while maintaining crystal integrity. Chemical processing plants utilize these pumps for moving aggressive chemicals and corrosive mixtures safely. Additional applications include wastewater treatment plants, cement manufacturing facilities, power generation stations, and steel production plants. Each pump configuration is optimized for its specific industrial environment, ensuring peak performance and compatibility with existing systems.

Businesses choose our pumps for their proven reliability, reduced operational downtime, and significant long-term cost savings. The premium materials and advanced engineering translate to extended service life even under the most punishing conditions. The efficient design contributes to reduced energy consumption while maintaining high throughput rates. Comprehensive technical support and maintenance services provide additional value, ensuring optimal performance throughout the equipment lifecycle. These pumps represent a strategic investment that delivers returns through improved operational efficiency, minimized maintenance costs, and enhanced production reliability. The commitment to quality and performance makes them the preferred choice for industrial operations worldwide.

Key Features:
- Engineered for handling abrasive solids and high-viscosity fluids with maximum efficiency
- Constructed from premium wear-resistant materials for extended service life
- Customizable configurations to meet specific operational requirements and system integration needs
- Designed for easy maintenance and quick component replacement to minimize downtime
- Robust sealing systems that prevent leaks and ensure safe operation in demanding environments

Benefits:
- Reduced operational downtime through reliable performance in demanding conditions
- Extended equipment lifespan with premium wear-resistant construction materials
- Lower maintenance costs with easy-access design and quick component replacement
- Enhanced safety with robust sealing systems that prevent leaks and spills
- Improved operational efficiency with energy-optimized performance and high throughput
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our industrial process pumps deliver reliable performance in the most demanding environments where equipment failure is not an option. These robust pumps efficiently transfer abrasive slurries, viscous fluids, and aggressive chemical solutions while maintaining consistent operation under extreme conditions. The advanced engineering ensures minimal downtime and maximum productivity for continuous industrial processes across various sectors.
Specifically designed massecuite pumps provide gentle handling of high-viscosity sugar products while preserving crystal integrity throughout transfer operations. The slurry pump variants offer enhanced wear resistance for mining and mineral processing applications, efficiently moving solid-laden mixtures while withstanding punishing abrasive conditions. These pumps maintain optimal performance in challenging industrial settings where reliability is critical.
- Transferring abrasive mineral slurries and tailings in mining operations
- Handling high-viscosity massecuite in sugar mills without damaging sugar crystals
- Moving chemical slurries and aggressive process fluids in chemical plants
- Dewatering and slurry transfer in wastewater treatment facilities
- Handling abrasive mixtures in cement production and power generation plants
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Kg Corporation, Gujarat
 Gujarat, India
Raw Materials & Chemicals•Trading Company•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
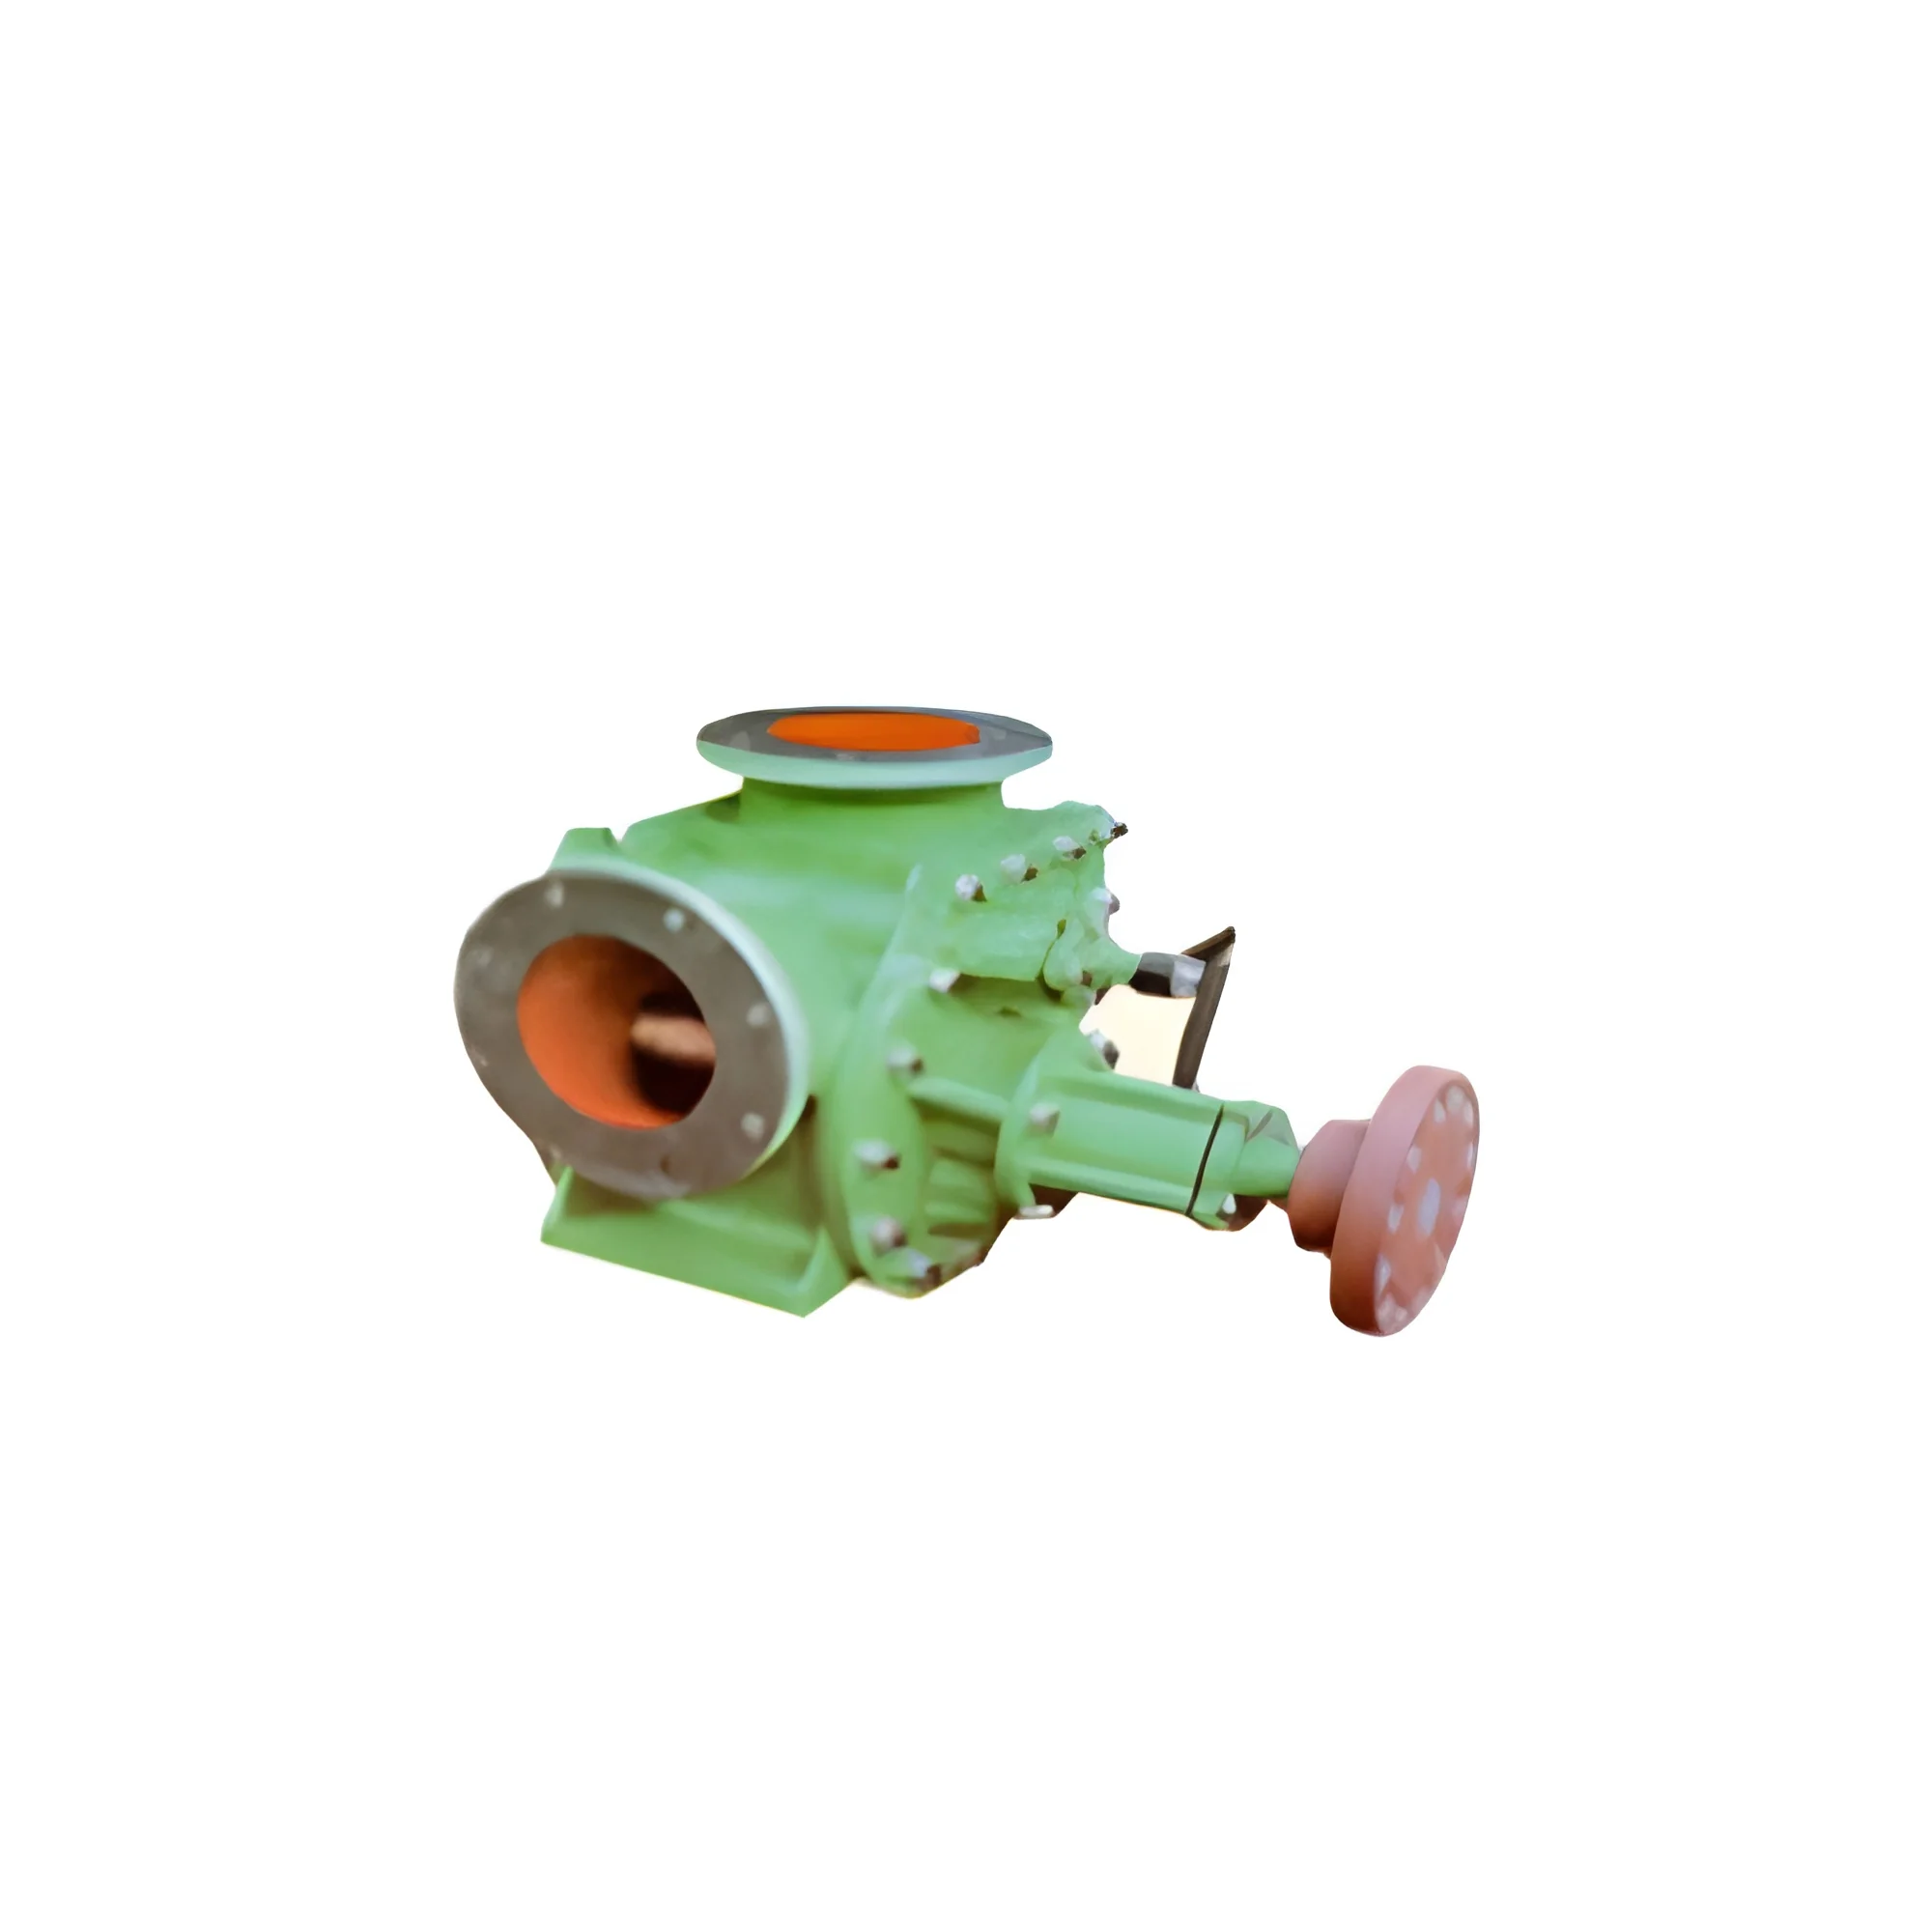
Industrial Process Pumps For Slurry And Massecuite Applications
Industrial process pumps for slurry and massecuite applications handle abrasive solids and high-viscosity fluids with exceptional reliability. Trusted by mining, sugar, and processing industries for demanding operations.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Kg Corporation
 Gujarat, India
Raw Materials & ChemicalsTrading Company