IN
₹
Apparel & Fashion

Description
Our pharmaceutical raw materials represent the foundation of safe and effective medicinal products, manufactured to meet the highest standards of purity and global regulatory compliance. These essential components include active pharmaceutical ingredients (APIs), excipients, and intermediates that undergo rigorous testing protocols to ensure they adhere to international pharmacopeia standards such as USP, EP, and IP. This unwavering commitment to quality assurance makes our materials a trusted choice for manufacturers seeking to deliver consistent therapeutic outcomes while maintaining compliance across diverse international markets. Each batch is carefully monitored and documented to provide complete traceability and quality verification.

These high-purity materials serve critical functions across multiple healthcare sectors, with generic drug manufacturers utilizing them for cost-effective production of off-patent medicines. Nutraceutical companies incorporate these ingredients into...
Our pharmaceutical raw materials represent the foundation of safe and effective medicinal products, manufactured to meet the highest standards of purity and global regulatory compliance. These essential components include active pharmaceutical ingredients (APIs), excipients, and intermediates that undergo rigorous testing protocols to ensure they adhere to international pharmacopeia standards such as USP, EP, and IP. This unwavering commitment to quality assurance makes our materials a trusted choice for manufacturers seeking to deliver consistent therapeutic outcomes while maintaining compliance across diverse international markets. Each batch is carefully monitored and documented to provide complete traceability and quality verification.

These high-purity materials serve critical functions across multiple healthcare sectors, with generic drug manufacturers utilizing them for cost-effective production of off-patent medicines. Nutraceutical companies incorporate these ingredients into dietary supplements and functional health products, while veterinary pharmaceutical producers rely on them for animal health solutions. Research laboratories and clinical trial facilities use these materials for experimental formulations and development projects. The adaptability of these ingredients supports a wide spectrum of applications, from oral solid dosages like tablets and capsules to liquid formulations including syrups, suspensions, and sterile injectables, ensuring comprehensive industry relevance.

Manufacturing partners benefit from enhanced operational reliability and reduced production risks through our consistent supply chain management and comprehensive quality control systems. The materials support compliance with stringent regulatory requirements across global markets, minimizing batch failures and accelerating product development timelines. By utilizing these high-purity components, companies achieve improved production efficiency and superior end-product performance, translating into significant long-term cost savings. This reliability builds strong customer trust and sustains market credibility through consistent delivery of quality medicinal products.

Key Features:
- High-purity materials compliant with USP, EP, and IP pharmacopeial standards
- Comprehensive range of APIs, excipients, and pharmaceutical intermediates
- Rigorous quality testing protocols with complete batch documentation
- Consistent particle size distribution and solubility characteristics
- Scalable quantities supporting both development projects and mass production

Benefits:
- Ensures regulatory compliance across international markets
- Reduces production risks and minimizes batch failures
- Supports consistent therapeutic outcomes in final products
- Accelerates product development and time-to-market
- Provides reliable supply chain for uninterrupted manufacturing
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
These pharmaceutical raw materials serve as essential components in formulating various medicinal products, from tablets and capsules to injectables and topical preparations. They ensure precise dosage delivery and therapeutic effectiveness while meeting strict pharmacopeial standards for purity and safety across different manufacturing environments. Their consistent quality makes them suitable for critical healthcare applications where reliability cannot be compromised.
Multiple industries depend on these high-quality materials for their production needs, including generic drug manufacturing, veterinary medicine, nutraceutical development, and research laboratories. The materials support both large-scale manufacturing operations and specialized compounding requirements, offering versatility across different regulatory frameworks. Businesses benefit from scalable supply chains that maintain uninterrupted production schedules while ensuring product consistency.
- Active Pharmaceutical Ingredient production for both branded and generic medications
- Excipient manufacturing for tablet binding, coating, and disintegration functions
- Formulation of pediatric and geriatric care products like syrups and suspensions
- Production of sterile injectables and ophthalmic solutions requiring highest purity
- Development of nutraceuticals and dietary supplements for health markets
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Ankit Enterprise, Maharashtra
 Maharashtra, India
Raw Materials & Chemicals•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
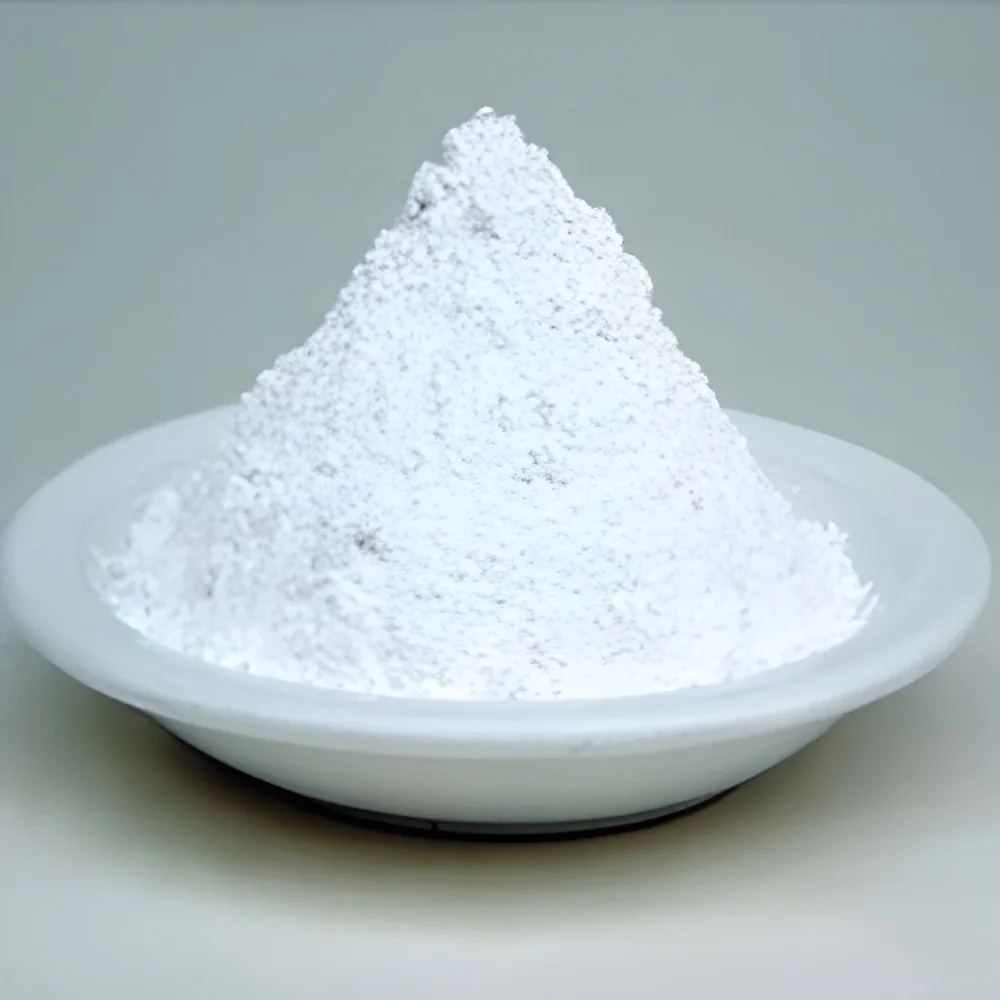
Pharmaceutical Raw Materials High Purity APIs Excipients
High purity pharmaceutical raw materials including APIs and excipients for drug manufacturers, laboratories, and distributors. Trusted quality ensures global compliance and reliable supply for consistent therapeutic outcomes.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Ankit Enterprise
 Maharashtra, India
Raw Materials & ChemicalsDistributor / Wholesaler