IN
₹
Apparel & Fashion
Description
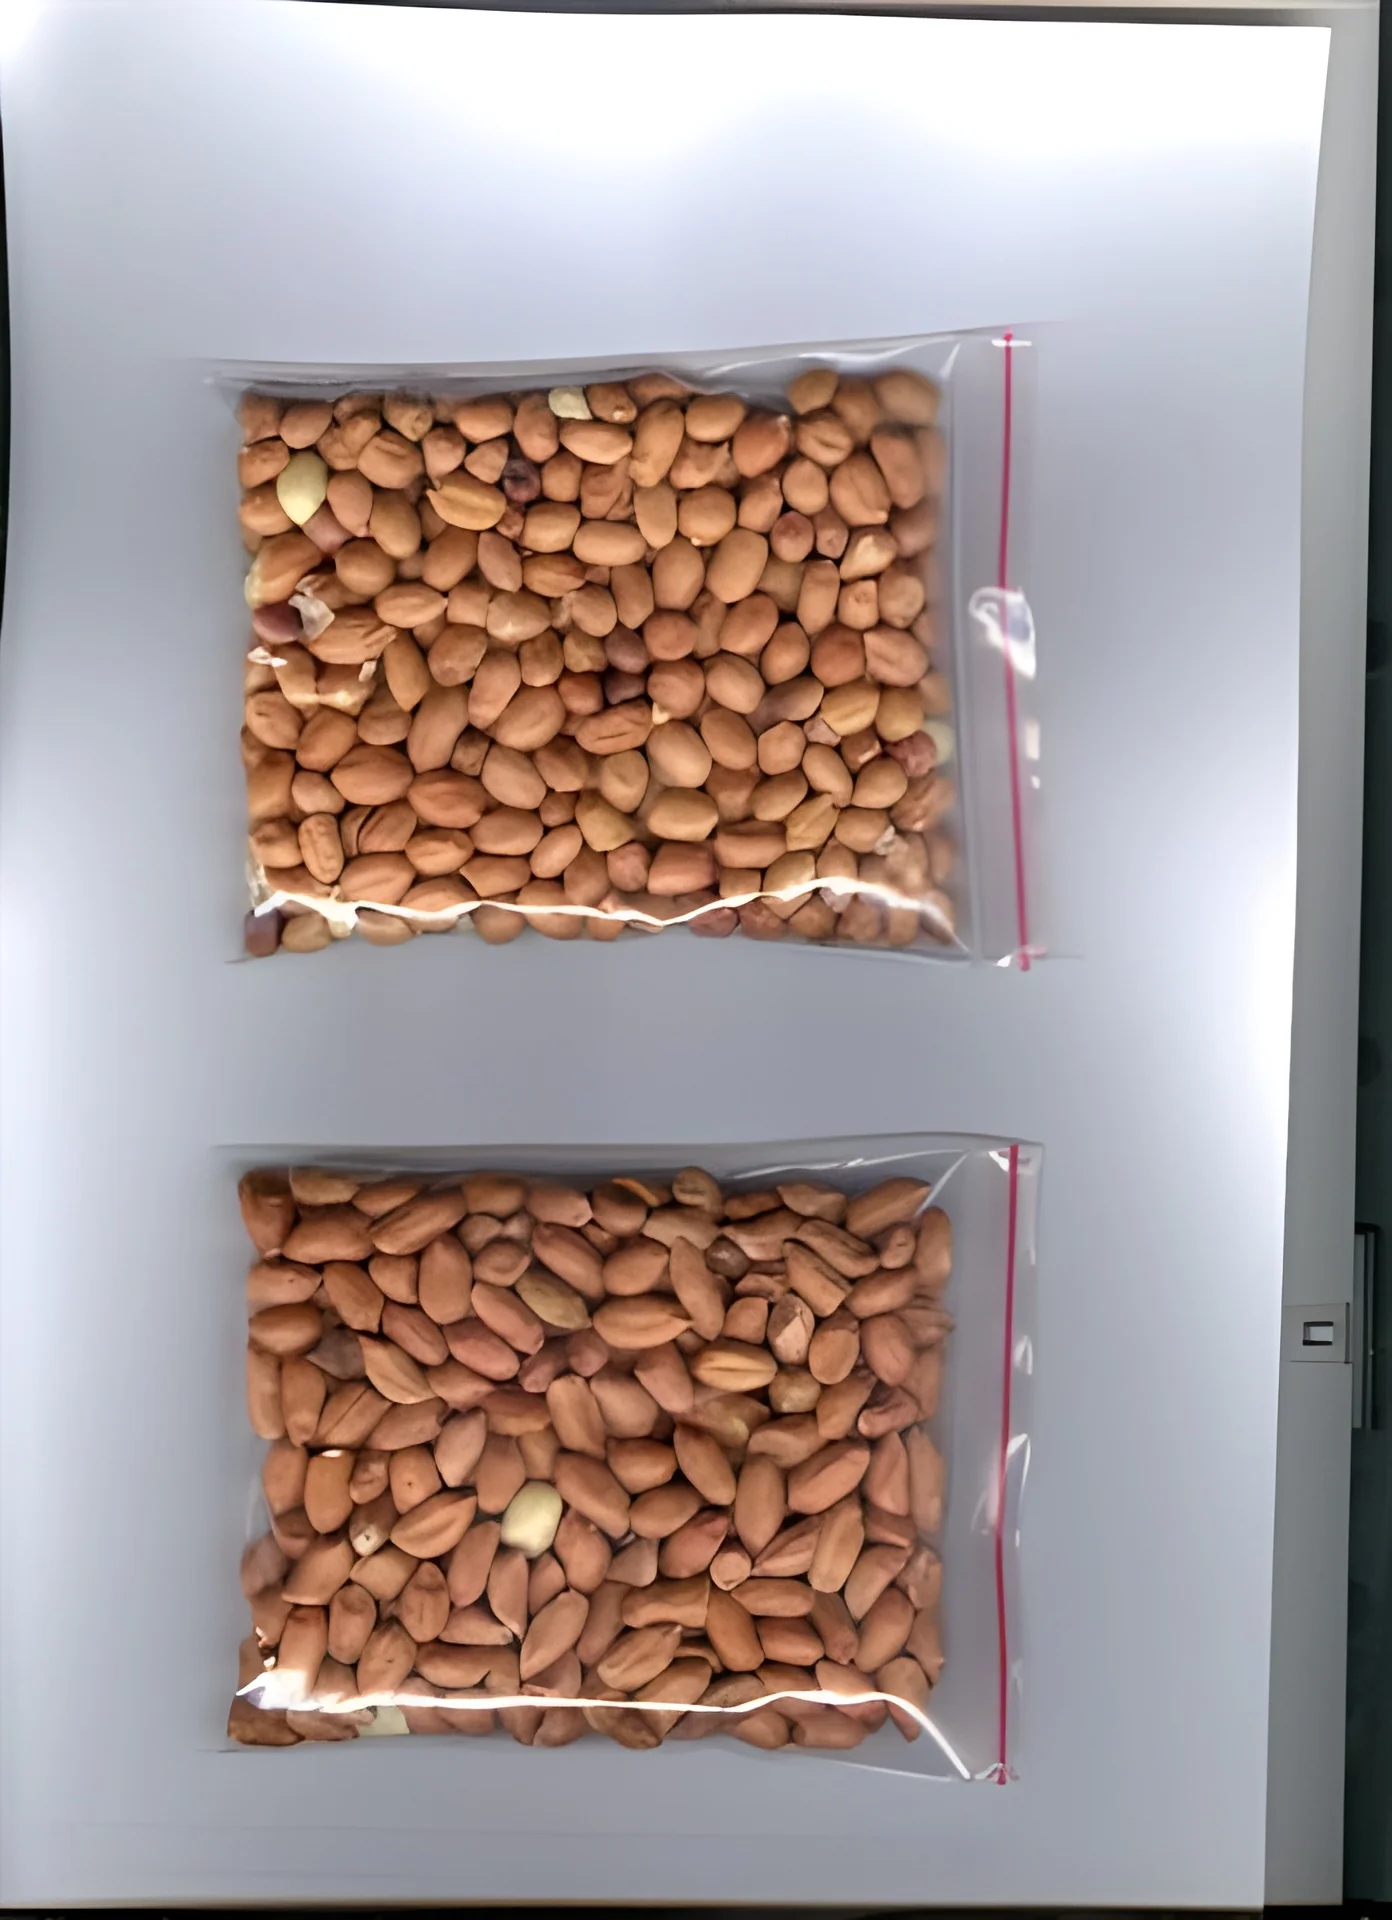
Our premium blanched peanut kernels represent the highest quality standards for industrial food applications. These carefully processed kernels undergo thorough blanching to remove skins, resulting in clean, uniform nuts ready for immediate use in various manufacturing processes. Available in specific size grades including 26/36, these kernels maintain rigorous quality parameters with moisture content limited to 5.5% maximum and foreign matter kept below 0.2%. The product is thoughtfully packaged with oxygen absorbers in either 25kg woven bags or 12.5kg cartons, ensuring extended freshness and optimal shelf life for business customers requiring reliable peanut supplies.

These blanched peanut kernels serve diverse industries including food manufacturing, snack production, confectionery, and culinary services. Food processors consistently choose them for peanut butter manufacturing, where the blanched kernels deliver smooth texture and consistent flavor profiles. Snack manufacturers uti...
Our premium blanched peanut kernels represent the highest quality standards for industrial food applications. These carefully processed kernels undergo thorough blanching to remove skins, resulting in clean, uniform nuts ready for immediate use in various manufacturing processes. Available in specific size grades including 26/36, these kernels maintain rigorous quality parameters with moisture content limited to 5.5% maximum and foreign matter kept below 0.2%. The product is thoughtfully packaged with oxygen absorbers in either 25kg woven bags or 12.5kg cartons, ensuring extended freshness and optimal shelf life for business customers requiring reliable peanut supplies.

These blanched peanut kernels serve diverse industries including food manufacturing, snack production, confectionery, and culinary services. Food processors consistently choose them for peanut butter manufacturing, where the blanched kernels deliver smooth texture and consistent flavor profiles. Snack manufacturers utilize them extensively for roasted peanuts, trail mixes, and coated peanut products. The confectionery industry incorporates them into chocolate bars, bakery products, and various candy formulations. Additionally, restaurants, catering services, and food distributors rely on these kernels for culinary applications, garnishes, and recipe ingredients where consistent quality and reliability are essential for business success.

Business customers select our blanched peanut kernels for their exceptional reliability, consistent quality, and operational efficiency. The product delivers significant business value through reduced processing time and costs since the blanching process is already completed. The innovative oxygen absorber packaging ensures product freshness during storage and transportation, minimizing spoilage and reducing waste. With broken pieces limited to maximum standards, businesses benefit from higher yield and better utilization rates. The multiple packaging options accommodate different business needs, from smaller batch processors to large-scale manufacturing operations, making them suitable for various business scales and production requirements.

Key Features:
- Multiple size grades available including 26/36 for specific applications
- Low moisture content maintained at 5.5% maximum for optimal preservation
- Minimal impurities with admixture limited to 0.2% maximum
- Oxygen absorber packaging technology for extended freshness
- Flexible packaging options including 25kg woven bags and 12.5kg cartons

Benefits:
- Reduced processing time and costs with pre-blanched kernels
- Extended shelf life through advanced packaging with oxygen absorbers
- Higher yield and better utilization with limited broken pieces
- Consistent quality meeting international food safety standards
- Flexible packaging accommodating different business scales and needs
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
These premium blanched peanut kernels serve as essential ingredients for food manufacturers seeking consistent quality and reliable supply. The careful removal of skins ensures a clean, uniform appearance perfect for further processing or direct incorporation into various food products. Their neutral flavor profile and nutritional value make them ideal for businesses requiring dependable peanut inputs that meet strict quality standards.
Food processors across multiple sectors utilize these kernels for their versatility and consistent performance. With moisture content maintained below 5.5% and impurities under 0.2%, they comply with international food safety standards while ensuring processing efficiency. The specific size grading allows manufacturers to select the perfect match for their production requirements and final product specifications, ensuring optimal results in every application.
- Snack manufacturing for roasted peanuts, peanut-based snacks, and mixed trail products
- Peanut butter production ensuring smooth texture and consistent flavor profiles
- Confectionery industry for chocolate coatings, candy bars, and baked goods
- Food service sector for culinary preparations, garnishes, and recipe ingredients
- Export markets requiring quality-assured peanut kernels for various food applications
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Shipping & Logistics
| Port of Dispatch | Delhi |
Company Profile
FENA PVT LTD, New Delhi
 New Delhi, India
Manufacturer•Retailer
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Blanched Peanut Kernels Premium Quality Low Moisture Sizes 26/36 61
Premium blanched peanut kernels in size 26/36 with low moisture content under 5.5% and high purity. Ideal for food manufacturing, snack production, and culinary applications with reliable quality and freshness preserved through oxygen absorber packaging.
Min. Order Quantity: 1 Piece
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
FENA PVT LTD
 New Delhi, India
Manufacturer