IN
₹
Apparel & Fashion
Description
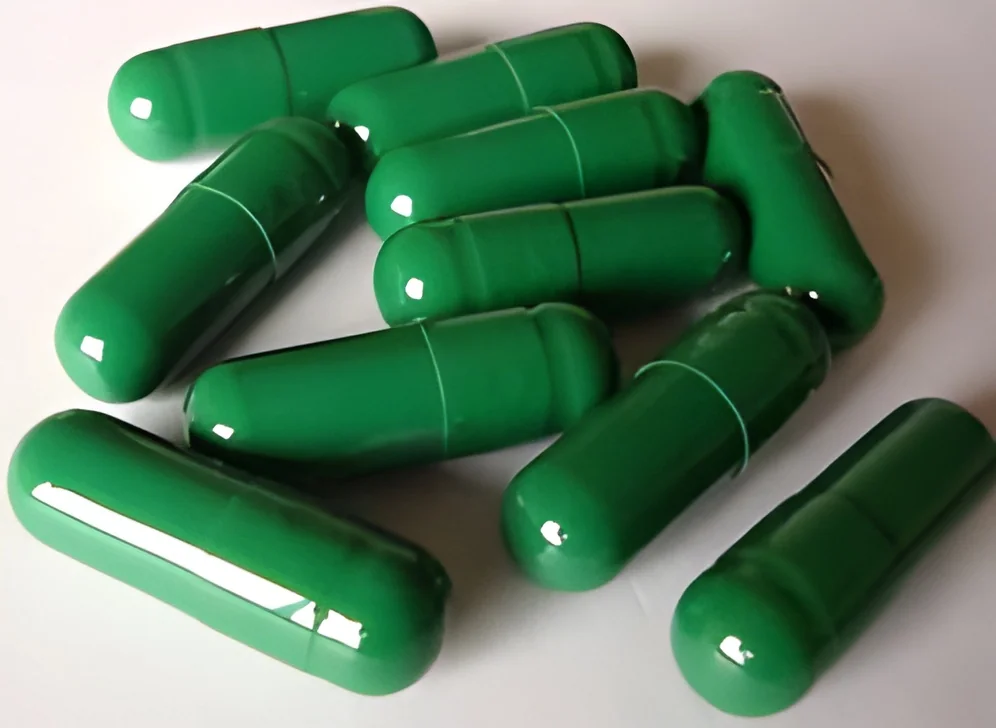
We provide high-quality pharmaceutical packaging materials engineered for critical product protection and regulatory compliance. Our comprehensive range includes aluminum collapsible tubes for semi-solid formulations, specialized aluminum seals for vial containment, amber ampoules for light-sensitive medications, and empty gelatin capsules for powder encapsulation. Each component undergoes strict quality control processes to ensure reliability and performance in demanding pharmaceutical applications. These materials are specifically designed to maintain product integrity, prevent contamination, and extend shelf life while meeting rigorous regulatory requirements for pharmaceutical packaging standards.

These packaging materials serve essential roles across multiple industries including pharmaceutical manufacturing, nutraceutical production, contract packaging services, and laboratory research facilities. Pharmaceutical manufacturers utilize them for both prescription and over-the-count...
We provide high-quality pharmaceutical packaging materials engineered for critical product protection and regulatory compliance. Our comprehensive range includes aluminum collapsible tubes for semi-solid formulations, specialized aluminum seals for vial containment, amber ampoules for light-sensitive medications, and empty gelatin capsules for powder encapsulation. Each component undergoes strict quality control processes to ensure reliability and performance in demanding pharmaceutical applications. These materials are specifically designed to maintain product integrity, prevent contamination, and extend shelf life while meeting rigorous regulatory requirements for pharmaceutical packaging standards.

These packaging materials serve essential roles across multiple industries including pharmaceutical manufacturing, nutraceutical production, contract packaging services, and laboratory research facilities. Pharmaceutical manufacturers utilize them for both prescription and over-the-counter medications, while nutraceutical producers rely on them for dietary supplement packaging. Research laboratories and clinical trial organizations employ these materials for sample storage and investigational product containment. The products are particularly valuable for companies handling sensitive formulations that require protection from environmental factors including light exposure, moisture, oxygen infiltration, and microbial contamination throughout distribution networks.

Our packaging materials deliver significant operational value through enhanced product protection, reduced material waste, and improved end-user safety. The consistent reliability of our aluminum components and glass ampoules ensures smooth performance in automated packaging lines, minimizing production downtime and operational delays. Standardized specifications allow businesses to implement packaging solutions that match specific product requirements, while our quality assurance protocols guarantee batch-to-batch consistency. This operational reliability translates into reduced rejection rates, lower total cost of ownership, and strengthened market reputation through dependable product delivery and customer satisfaction.

Key Features:
- Pharmaceutical-grade aluminum collapsible tubes for creams and ointments
- Precision aluminum seals ensuring vial integrity and tamper evidence
- Light-protective amber ampoules for photosensitive medications
- Empty gelatin capsules suitable for powder and supplement encapsulation
- Standardized sizing and specification options available

Benefits:
- Enhanced product protection against environmental factors and contamination
- Extended shelf life through superior barrier properties and light protection
- Regulatory compliance with pharmaceutical packaging standards and requirements
- Reliable performance in automated packaging and manufacturing processes
- Consistent quality ensuring batch-to-batch uniformity and reduced waste
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our pharmaceutical-grade packaging materials serve critical functions in drug manufacturing and packaging operations. Aluminum collapsible tubes provide secure containment for ointments, creams, and topical medications, while specialized seals ensure vial integrity for injectables and sensitive formulations. These components meet stringent industry standards for product safety and preservation throughout the supply chain.
Amber ampoules offer essential light protection for photosensitive medications, and empty gelatin capsules enable precise dosage encapsulation for powders and supplements. These materials are vital for pharmaceutical companies, nutraceutical manufacturers, and contract packaging organizations requiring reliable, compliant packaging solutions that maintain product stability during distribution and storage.
- Pharmaceutical cream and ointment packaging using aluminum collapsible tubes
- Sterile vial sealing for injectable medications and vaccine containment
- Light-sensitive drug protection utilizing amber glass ampoules
- Powder and supplement encapsulation in gelatin capsules
- Laboratory sample preservation and clinical trial material storage
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Bangalore Fine Chem, Karnataka
 Karnataka, India
Raw Materials & Chemicals•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Pharmaceutical Packaging Materials: Aluminum Tubes, Vial Seals, Ampoules, Gelatin Capsules
Premium pharmaceutical packaging materials including aluminum tubes, vial seals, amber ampoules, and gelatin capsules. Trusted for quality and reliability in sensitive product protection across medical and pharmaceutical industries.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Bangalore Fine Chem
 Karnataka, India
Raw Materials & ChemicalsManufacturer