IN
₹

Description
Fenix N-Rings represent advanced random tower packing technology engineered for superior mass transfer operations in industrial processes. These packings provide optimal surface area for liquid-gas contact while maintaining minimal pressure drop across systems. Manufactured from high-grade materials including various stainless steel grades and specialized alloys, each unit undergoes strict quality control to ensure consistent performance and durability. The unique geometric design enhances liquid distribution and promotes efficient mixing, making these rings a reliable choice for demanding separation and purification applications across multiple industries. This engineering excellence ensures dependable performance in various mass transfer challenges.

These random packings find extensive application across chemical processing, petrochemical refining, pharmaceutical manufacturing, and environmental engineering sectors. In chemical plants, they are deployed in distillation columns for s...
Fenix N-Rings represent advanced random tower packing technology engineered for superior mass transfer operations in industrial processes. These packings provide optimal surface area for liquid-gas contact while maintaining minimal pressure drop across systems. Manufactured from high-grade materials including various stainless steel grades and specialized alloys, each unit undergoes strict quality control to ensure consistent performance and durability. The unique geometric design enhances liquid distribution and promotes efficient mixing, making these rings a reliable choice for demanding separation and purification applications across multiple industries. This engineering excellence ensures dependable performance in various mass transfer challenges.

These random packings find extensive application across chemical processing, petrochemical refining, pharmaceutical manufacturing, and environmental engineering sectors. In chemical plants, they are deployed in distillation columns for separating complex mixtures and in absorption towers for gas treatment processes. The petrochemical industry utilizes them in crude oil fractionation towers and natural gas processing units where reliability under high temperatures and pressures is critical. Pharmaceutical manufacturers employ these rings in purification columns for solvent recovery and API production, while environmental applications include water treatment plants for air stripping volatile contaminants and industrial scrubbers for emission control systems.

The business value of Fenix N-Rings lies in their ability to reduce operational costs while enhancing process efficiency. Their low pressure drop characteristics directly translate to energy savings through reduced pumping requirements and lower utility consumption. The enhanced mass transfer efficiency means smaller equipment footprints can achieve the same separation results, reducing capital investment in new installations. Reliability is built into every ring through material certification from trusted suppliers and rigorous manufacturing standards, ensuring long service life with minimal maintenance needs. These packings offer a cost-effective solution without compromising performance, making them an intelligent choice for operations seeking premium results.

Key Features:
- High-efficiency random packing design for superior mass transfer performance
- Engineered for low pressure drop and minimal energy consumption
- Excellent liquid distribution capabilities for uniform flow patterns
- Constructed from certified stainless steel and alloy materials
- Robust construction suitable for high-temperature and high-pressure operations

Benefits:
- Reduced operational costs through lower energy consumption
- Enhanced process efficiency with improved separation performance
- Extended equipment life with minimal maintenance requirements
- Reliable performance in demanding industrial environments
- Cost-effective solution delivering premium mass transfer results
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Fenix N-Rings are engineered random packings designed to maximize mass transfer efficiency in distillation, absorption, and stripping columns. Their open structure promotes excellent liquid distribution and gas flow, making them ideal for processes requiring high separation efficiency and low energy consumption. These rings perform reliably with corrosive chemicals and high-purity requirements, ensuring consistent operation under demanding conditions across various industrial settings.
These packings serve chemical processing, petrochemical refining, pharmaceuticals, and water treatment industries. Their robust construction from certified materials ensures reliable performance in high-temperature and high-pressure environments. The design minimizes fouling and plugging, reducing maintenance downtime and extending operational life of process towers while maintaining optimal separation efficiency across diverse industrial applications.
- Distillation columns in petrochemical refineries for separating crude oil components
- Gas absorption towers in chemical plants removing contaminants from process streams
- Stripping columns in wastewater treatment facilities for volatile organic compound removal
- Air separation units for cryogenic distillation of nitrogen and oxygen
- Scrubbers in pharmaceutical manufacturing for solvent recovery and purification
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Fenix Process Technologies Pvt Ltd, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Manufacturer•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
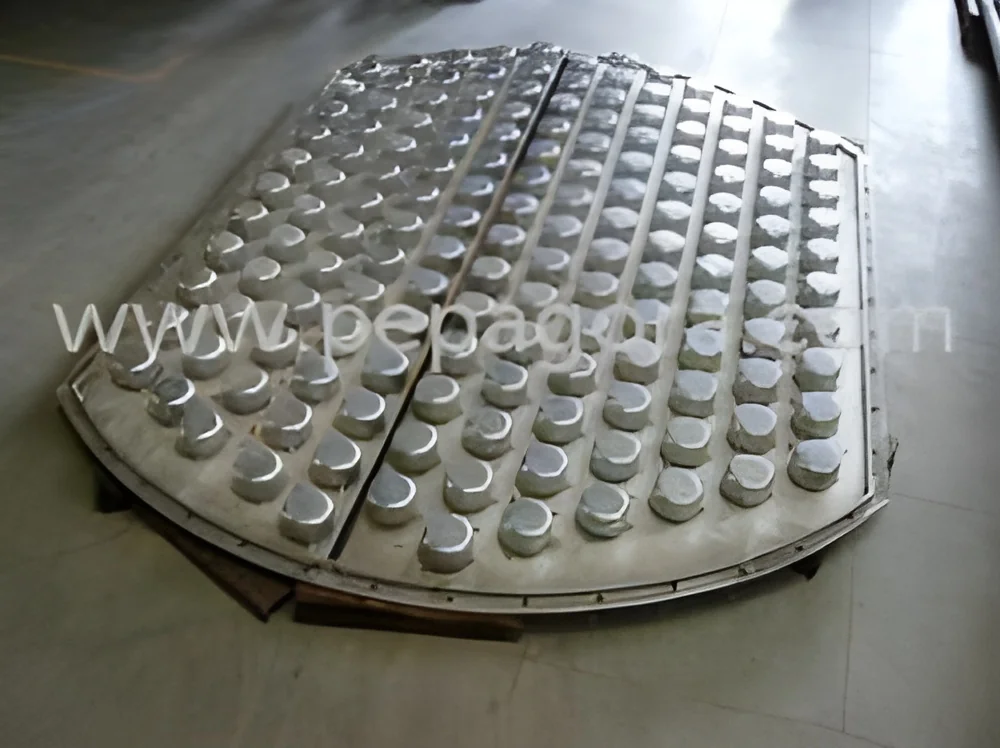
Fenix N Rings High Efficiency Random Tower Packings For Mass Transfer
Fenix N-Rings high-efficiency random tower packings deliver superior mass transfer with low pressure drop and excellent liquid distribution for chemical processing, petrochemical, and environmental applications.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Fenix Process Technologies Pvt Ltd
 Maharashtra, India
Industrial Equipment & MachineryManufacturer