IN
₹
Apparel & Fashion
Description
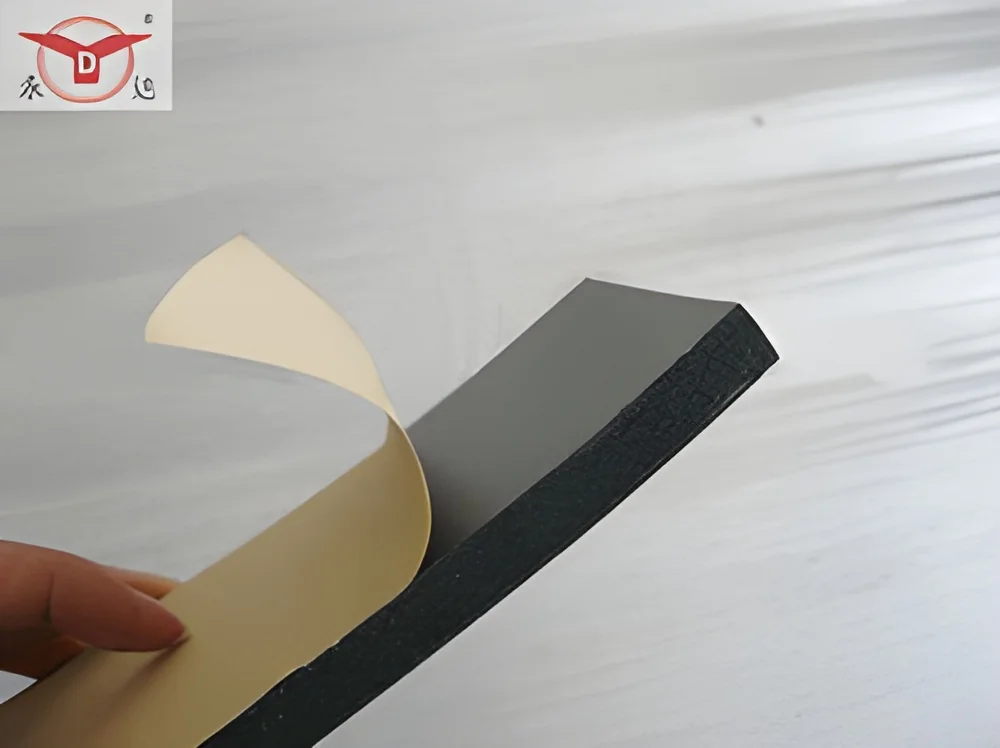
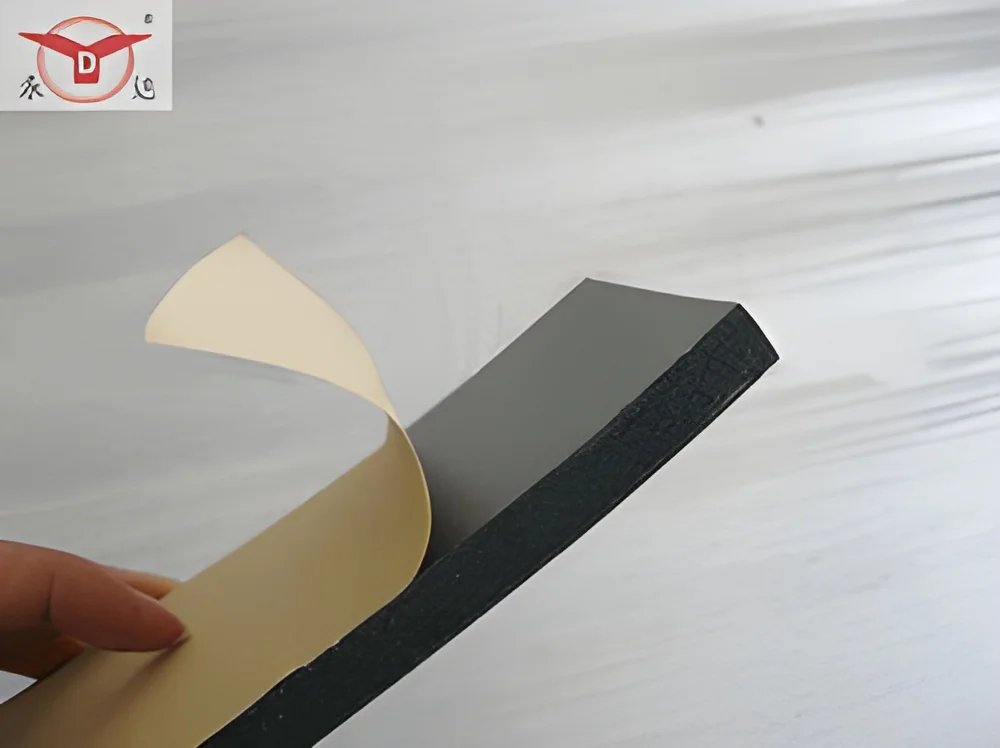
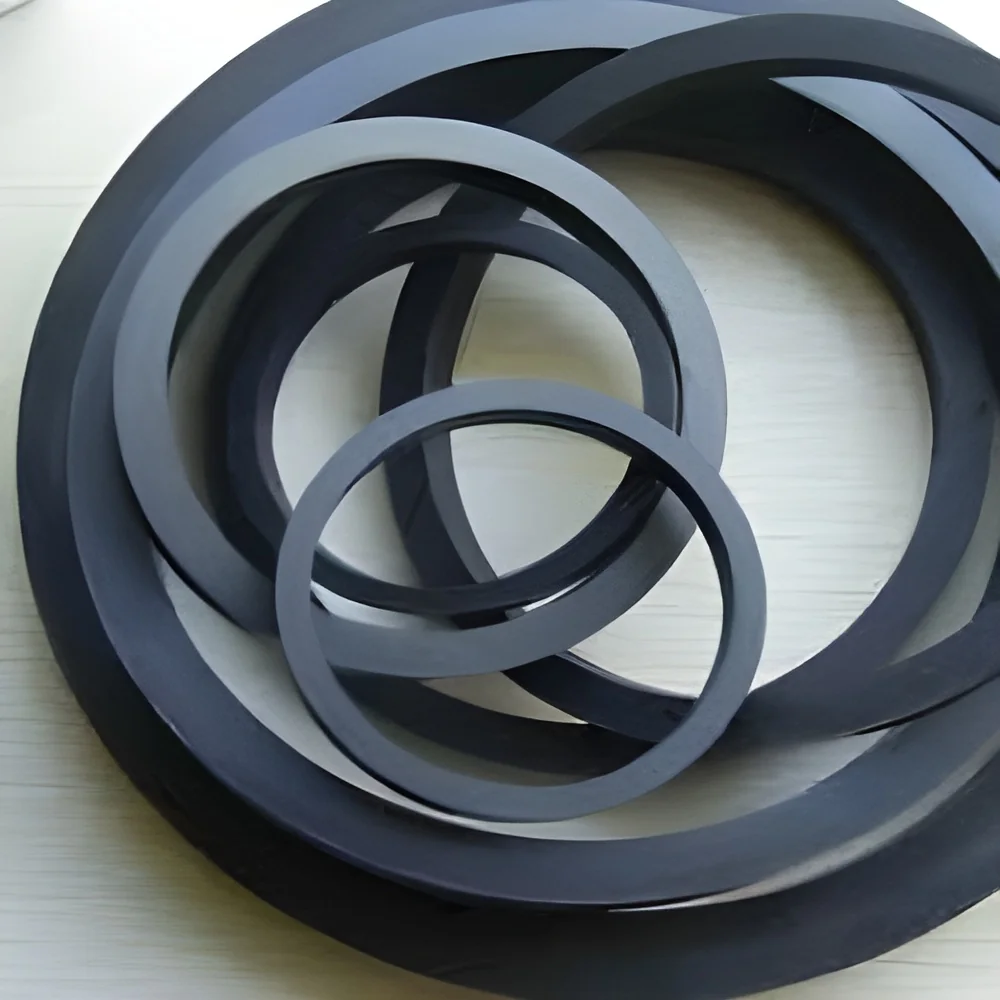
Industrial NBR gaskets represent premium sealing solutions specifically engineered for applications demanding exceptional resistance to oils, fuels, and various chemicals. Manufactured from high-grade nitrile butadiene rubber compounds, these gaskets deliver superior performance in challenging operational environments. The material properties include excellent compression set resistance, reliable abrasion resistance, and consistent sealing capabilities across a broad temperature spectrum from -40°C to 120°C. Available in multiple thicknesses and standard sizes, these gaskets ensure effective fluid containment and environmental protection for diverse equipment and machinery applications. Their consistent quality and dimensional stability guarantee proper fitment and extended service life, significantly reducing the frequency of replacements and maintenance requirements.

These specialized gaskets perform critical functions across numerous industrial sectors including automotive manufact...
Industrial NBR gaskets represent premium sealing solutions specifically engineered for applications demanding exceptional resistance to oils, fuels, and various chemicals. Manufactured from high-grade nitrile butadiene rubber compounds, these gaskets deliver superior performance in challenging operational environments. The material properties include excellent compression set resistance, reliable abrasion resistance, and consistent sealing capabilities across a broad temperature spectrum from -40°C to 120°C. Available in multiple thicknesses and standard sizes, these gaskets ensure effective fluid containment and environmental protection for diverse equipment and machinery applications. Their consistent quality and dimensional stability guarantee proper fitment and extended service life, significantly reducing the frequency of replacements and maintenance requirements.

These specialized gaskets perform critical functions across numerous industrial sectors including automotive manufacturing, oil and gas operations, chemical processing, food and beverage production, pharmaceutical manufacturing, and general industrial applications. In automotive contexts, they effectively seal engine components, transmission systems, and fuel handling mechanisms. The oil and gas industry utilizes them extensively in pipeline flanges, refinery equipment, and drilling machinery where petroleum resistance proves essential. Food processing facilities employ FDA-compliant NBR gaskets for equipment handling oils and fats, while pharmaceutical manufacturers value them for their cleanliness standards and chemical resistance in processing equipment. Industrial manufacturers install them throughout hydraulic systems, pumps, compressors, and valves within their production operations.

The inherent business value of NBR gaskets lies in their proven reliability, cost-effectiveness, and consistent performance delivery. These components substantially reduce operational downtime by providing dependable seals that prevent fluid leaks and contamination issues. Their exceptional oil and chemical resistance translates to significantly longer service life compared to standard rubber gaskets, resulting in reduced replacement costs and lower maintenance expenditures. The consistent quality assurance, reliable delivery schedules, and technical support available help businesses optimize their sealing solutions for specific operational requirements and environmental conditions, ensuring maximum efficiency and productivity.

Key Features:
- Superior resistance to oils, fuels, and various chemicals
- Broad temperature tolerance from -40°C to 120°C
- Excellent compression set and abrasion resistance
- Multiple standard sizes and thickness options
- Consistent quality with dimensional stability

Benefits:
- Extended service life reducing replacement frequency
- Reliable leak prevention minimizing downtime
- Cost-effective maintenance and operational savings
- Versatile compatibility across multiple industries
- Consistent performance in demanding environments
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
NBR gaskets serve as essential sealing components across multiple industries where resistance to oils, fuels, and chemicals is critical. Their superior compression set and durability make them suitable for both static and dynamic applications, ensuring consistent performance under varying temperatures and pressures. These precision-manufactured gaskets provide reliable seals that prevent leaks and minimize maintenance downtime in industrial equipment and machinery.
Various industries rely on NBR gaskets including automotive manufacturing, oil and gas operations, food processing facilities, pharmaceutical production, and industrial machinery. They are specifically engineered to handle petroleum-based fluids, water, and hydraulic fluids, making them versatile solutions for pumps, valves, engines, and pipe flanges. The material's flexibility ensures effective sealing on uneven surfaces while maintaining integrity through compression cycles and environmental exposure.
- Automotive engine gaskets for oil pans, valve covers, and transmission systems
- Hydraulic system seals in construction equipment and manufacturing machinery
- Pipe flange gaskets in chemical processing plants and oil refineries
- Food processing equipment seals requiring FDA-compliant materials
- Pump and compressor gaskets in water treatment facilities and irrigation systems
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Ashwini Enterprises, Karnataka
 Karnataka, India
Raw Materials & Chemicals•Manufacturer•Trading Company•Distributor / Wholesaler
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial NBR Gaskets: Oil Resistant, Durable Sealing Solutions
Industrial NBR gaskets provide durable, oil-resistant sealing solutions for demanding applications in automotive, manufacturing, and hydraulic systems. These high-quality gaskets deliver reliable performance with excellent compression resistance and long-term durability.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Ashwini Enterprises
 Karnataka, India
Raw Materials & ChemicalsManufacturer