IN
₹
Apparel & Fashion
Description
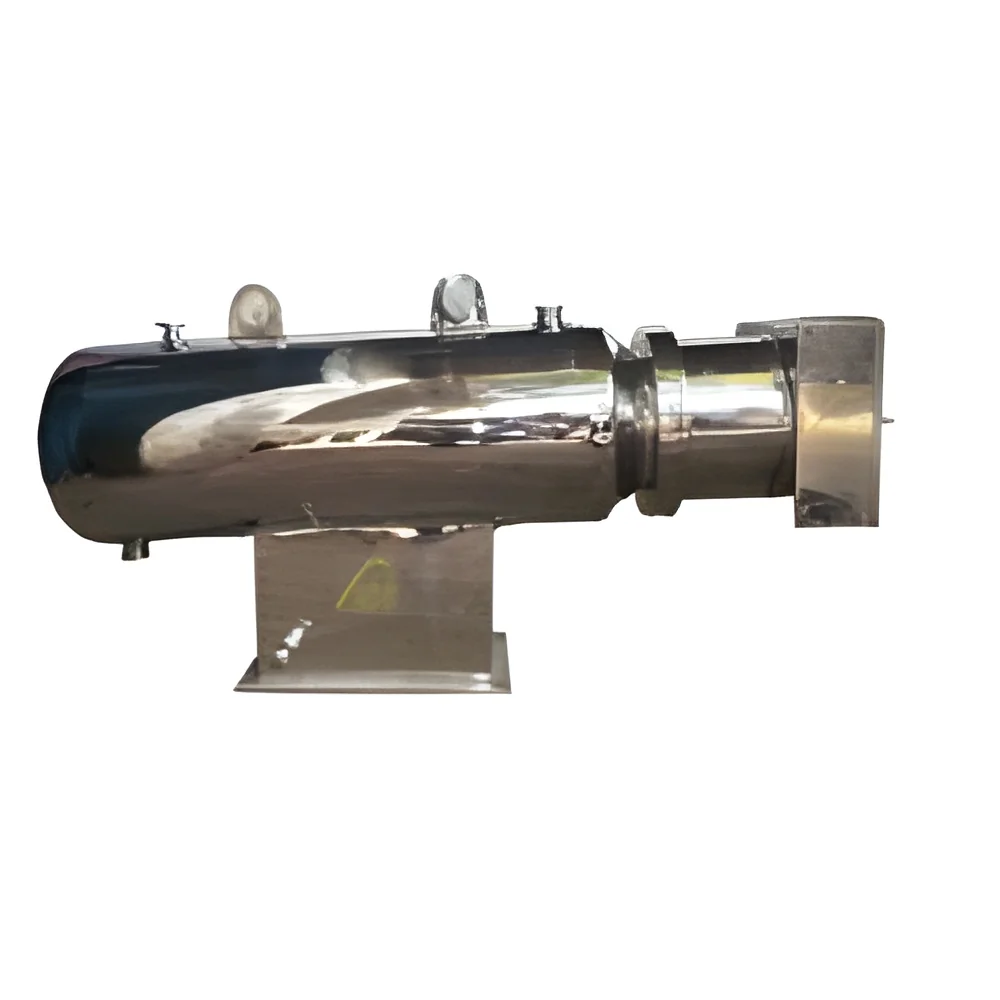
The Industrial 12 KW Multiple Oil Heater delivers reliable thermal fluid heating for demanding industrial applications. Engineered with quality components, this robust heating unit ensures consistent performance through precision temperature control and efficient heat transfer capabilities. Designed specifically for industrial environments, it features advanced safety mechanisms and durable construction that withstands continuous operation. The heater accommodates various industrial oil types and operates effectively across diverse settings, providing dependable heating solutions that maintain process stability and operational efficiency. Its straightforward design prioritizes functionality and longevity, making it a practical choice for facilities requiring uninterrupted thermal management.

This heating solution serves essential functions across numerous industrial sectors. Manufacturing facilities utilize it to maintain precise temperatures in hydraulic systems, production machinery...
The Industrial 12 KW Multiple Oil Heater delivers reliable thermal fluid heating for demanding industrial applications. Engineered with quality components, this robust heating unit ensures consistent performance through precision temperature control and efficient heat transfer capabilities. Designed specifically for industrial environments, it features advanced safety mechanisms and durable construction that withstands continuous operation. The heater accommodates various industrial oil types and operates effectively across diverse settings, providing dependable heating solutions that maintain process stability and operational efficiency. Its straightforward design prioritizes functionality and longevity, making it a practical choice for facilities requiring uninterrupted thermal management.

This heating solution serves essential functions across numerous industrial sectors. Manufacturing facilities utilize it to maintain precise temperatures in hydraulic systems, production machinery, and assembly lines where consistent heat is critical. Chemical and pharmaceutical plants rely on its stable heating capabilities for reactors, mixers, and processing equipment that require controlled thermal conditions. The food production industry employs these heaters for thermal fluid applications in cooking, pasteurization, and packaging operations. Additionally, metalworking, automotive, and plastics industries use them for pre-heating applications, mold temperature control, and maintaining optimal viscosity in lubrication and cutting systems, ensuring smooth production workflows.

Businesses gain significant value through reduced operational costs and enhanced process reliability. The heater's energy-efficient design minimizes electricity consumption while delivering consistent heating performance, lowering utility expenses. Its durable construction ensures extended service life with minimal maintenance requirements, reducing downtime and repair costs. Companies benefit from improved product quality and process consistency through precise temperature control, which minimizes material waste and production errors. The unit's adaptability to various industrial environments and oil types makes it a versatile investment, while its reliable operation supports continuous production schedules and helps meet demanding output targets without thermal interruptions.

Key Features:
- 12 kilowatt heating capacity suitable for industrial-scale thermal requirements
- Compatibility with multiple oil types including hydraulic, thermal transfer, and lubricating fluids
- Robust construction featuring corrosion-resistant components and industrial-grade materials
- Precision digital temperature control with integrated safety cutoff and overload protection
- Compact industrial design with easy installation and straightforward maintenance access

Benefits:
- Consistent and reliable heating performance for uninterrupted industrial processes
- Energy-efficient operation that reduces power consumption and lowers operating costs
- Durable construction ensures long service life with minimal maintenance requirements
- Precise temperature control improves product quality and process consistency
- Versatile application across multiple industries and various thermal fluid systems
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
The 12 KW multiple oil heater provides dependable thermal fluid heating for industrial processes requiring precise temperature management. Its robust design ensures continuous operation in challenging environments, handling various oil types including hydraulic and thermal fluids. The unit delivers consistent heat transfer for applications where temperature stability directly impacts production quality and operational efficiency.
This industrial heating solution serves critical functions across multiple sectors, from manufacturing plants to processing facilities. Its versatility makes it suitable for systems requiring maintained oil viscosity or specific process temperatures. Companies benefit from reduced energy consumption and minimal maintenance needs, supporting uninterrupted production cycles and cost-effective operations.
- Maintaining optimal operating temperatures for hydraulic systems in injection molding and plastic processing machinery.
- Heating thermal transfer fluids in chemical reactors and distillation columns for consistent process control.
- Providing precise heat for food processing lines, including fryers, cookers, and packaging equipment sterilization.
- Pre-heating lubricants and cutting oils in metalworking CNC machines and automotive production lines.
- Supporting temperature regulation in industrial ovens, dryers, and curing systems within manufacturing facilities.
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Amod Engineering Works, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
South Asia
Industrial 12 KW Multiple Oil Heater For Thermal Fluid Heating
Industrial 12 KW multiple oil heater for efficient thermal fluid heating. Built with durable components for reliable performance in demanding industrial environments. Ideal for manufacturing, chemical processing, and production facilities requiring consistent temperature control.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Amod Engineering Works
 Maharashtra, India
Industrial Equipment & MachineryManufacturer