IN
₹
Description
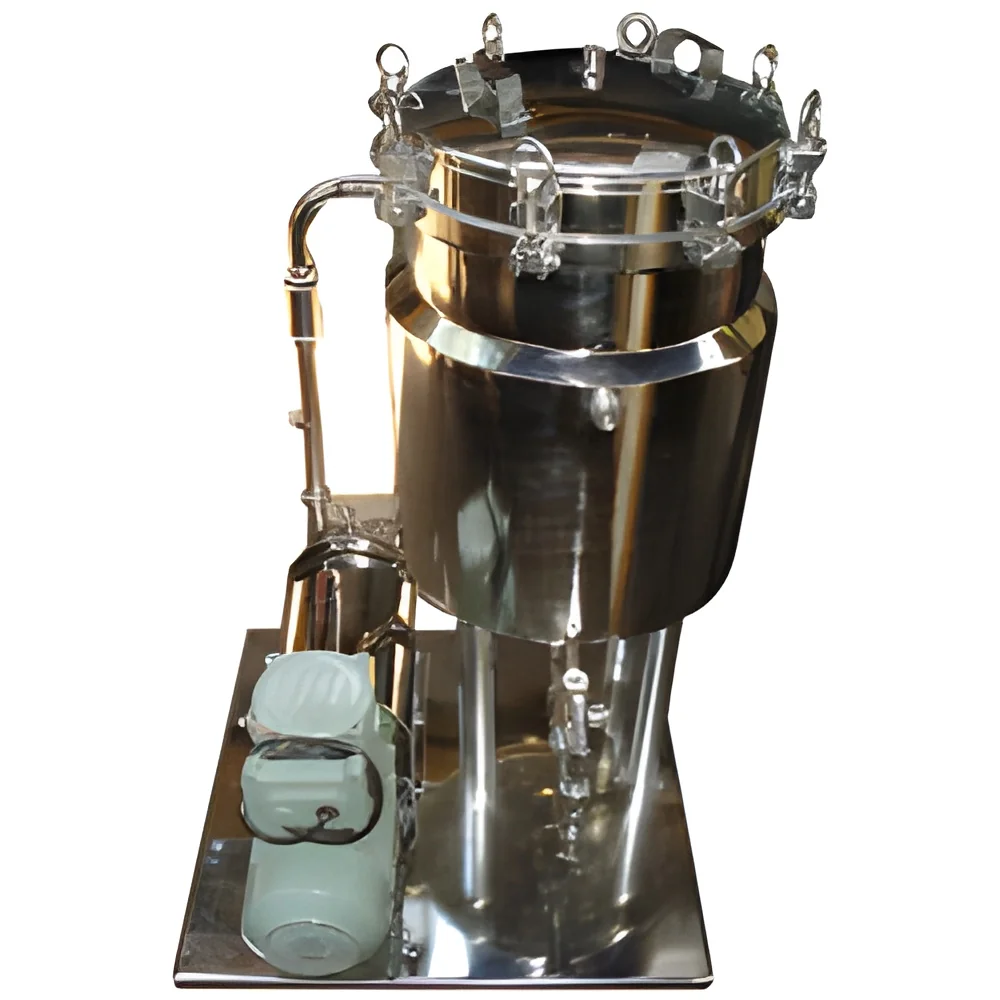
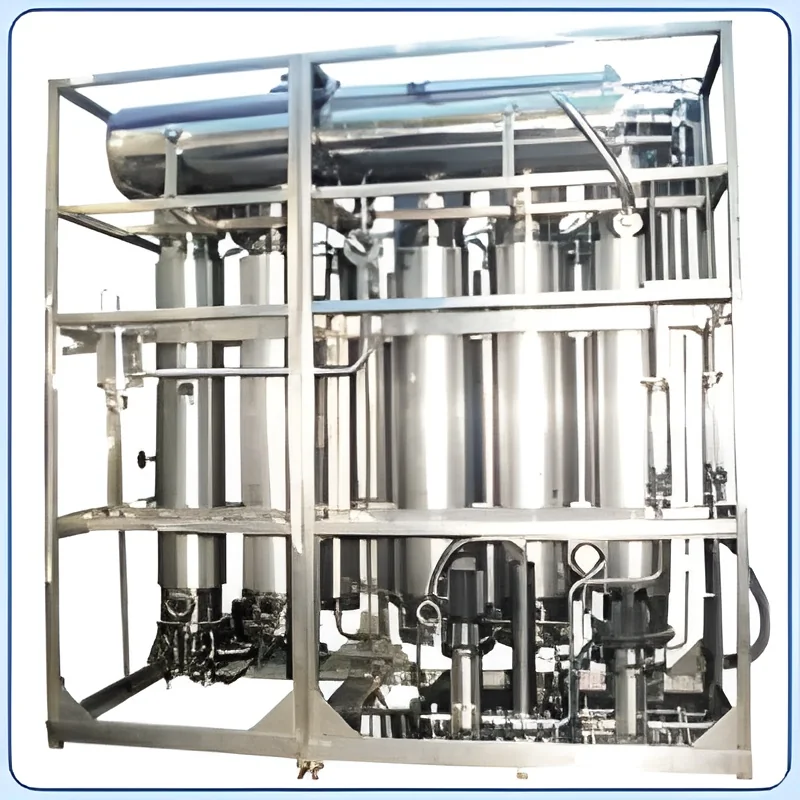
The Multi Column Distillation Plant represents advanced separation technology engineered for industrial-scale purification processes. This integrated system combines multiple distillation columns in a compact design that achieves remarkable 75% energy savings while maintaining exceptional output quality. The specialized spiral baffle system and centrifugal force development ensure efficient pyrogen removal and precise separation of complex mixtures. With no moving parts and a robust multi-stage horizontal pump, the plant delivers reliable performance while minimizing maintenance requirements and operational costs. The integrated control panel provides comprehensive monitoring and adjustment capabilities for optimal process control across various industrial applications.

This distillation system serves critical functions in pharmaceutical manufacturing, chemical processing, and essential oil production industries. Pharmaceutical companies utilize it for producing pyrogen-free water and...
The Multi Column Distillation Plant represents advanced separation technology engineered for industrial-scale purification processes. This integrated system combines multiple distillation columns in a compact design that achieves remarkable 75% energy savings while maintaining exceptional output quality. The specialized spiral baffle system and centrifugal force development ensure efficient pyrogen removal and precise separation of complex mixtures. With no moving parts and a robust multi-stage horizontal pump, the plant delivers reliable performance while minimizing maintenance requirements and operational costs. The integrated control panel provides comprehensive monitoring and adjustment capabilities for optimal process control across various industrial applications.

This distillation system serves critical functions in pharmaceutical manufacturing, chemical processing, and essential oil production industries. Pharmaceutical companies utilize it for producing pyrogen-free water and purifying solvents for drug manufacturing processes. Chemical plants employ the system for separating high-purity compounds and specialty chemicals that require precise temperature control and consistent results. The essential oil industry benefits from its ability to maintain delicate molecular structures during extraction and purification processes. Additionally, alcohol production facilities and environmental management operations use these plants for purification and solvent recovery applications where reliability and consistency are essential for operational success.

The business value of this Multi Column Distillation Plant lies in its significant 75% energy reduction compared to conventional systems, substantially lowering operational expenses while maintaining production quality. Its reliability stems from a simplified design with no moving parts, ensuring minimal downtime and reduced maintenance costs over the system's lifespan. The compact footprint saves valuable floor space while the integrated control system enables precise process management. These advantages make it an excellent long-term investment for businesses seeking to enhance production efficiency, reduce environmental impact, and maintain consistent product quality in competitive industrial markets.

Key Features:
- Compact integrated design with easy maintenance and operational accessibility
- 75% total energy saving with optimized heating and cooling requirements
- Advanced pyrogen removal through centrifugal force and spiral baffle design
- No moving parts configuration for minimal maintenance and reliable performance
- Multi-stage horizontal pump with trouble-free operation and compact control panel

Benefits:
- Significant reduction in operational costs through 75% energy efficiency
- Enhanced reliability with minimal maintenance requirements and reduced downtime
- Consistent high-purity separation results across various industrial applications
- Space-saving compact design optimized for industrial facility integration
- Trouble-free performance with precise process control capabilities
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
This Multi Column Distillation Plant handles complex separation processes requiring precise temperature and pressure control. Its compact design with advanced baffle system ensures continuous operation in demanding environments where purity and energy efficiency are critical for production consistency and quality output across various industrial applications.
The robust construction and minimal maintenance requirements make this system ideal for sterile processing and chemical purification. With no moving parts and reliable multi-stage horizontal pump, it reduces downtime while delivering consistent results in large-scale production environments. This trouble-free performance ensures operational efficiency across multiple processing industries.
- Pharmaceutical manufacturing for solvent purification and pyrogen-free water production
- Essential oil extraction and refinement for fragrance and flavor industries
- Chemical processing for high-purity compound separation and specialty chemicals
- Alcohol production and purification for beverage and industrial applications
- Environmental management for waste treatment and solvent recovery operations
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Anmol Pharma Equipments, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Multi Column Distillation Plant For High Purity Separation With 75% Energy Savings
Multi Column Distillation Plant delivers 75% energy savings for high-purity separation in pharmaceutical, chemical, and essential oil industries. Compact design ensures easy maintenance and reliable pyrogen removal for consistent performance.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Anmol Pharma Equipments
 Maharashtra, India
Industrial Equipment & MachineryManufacturer