IN
₹
Apparel & Fashion
Description
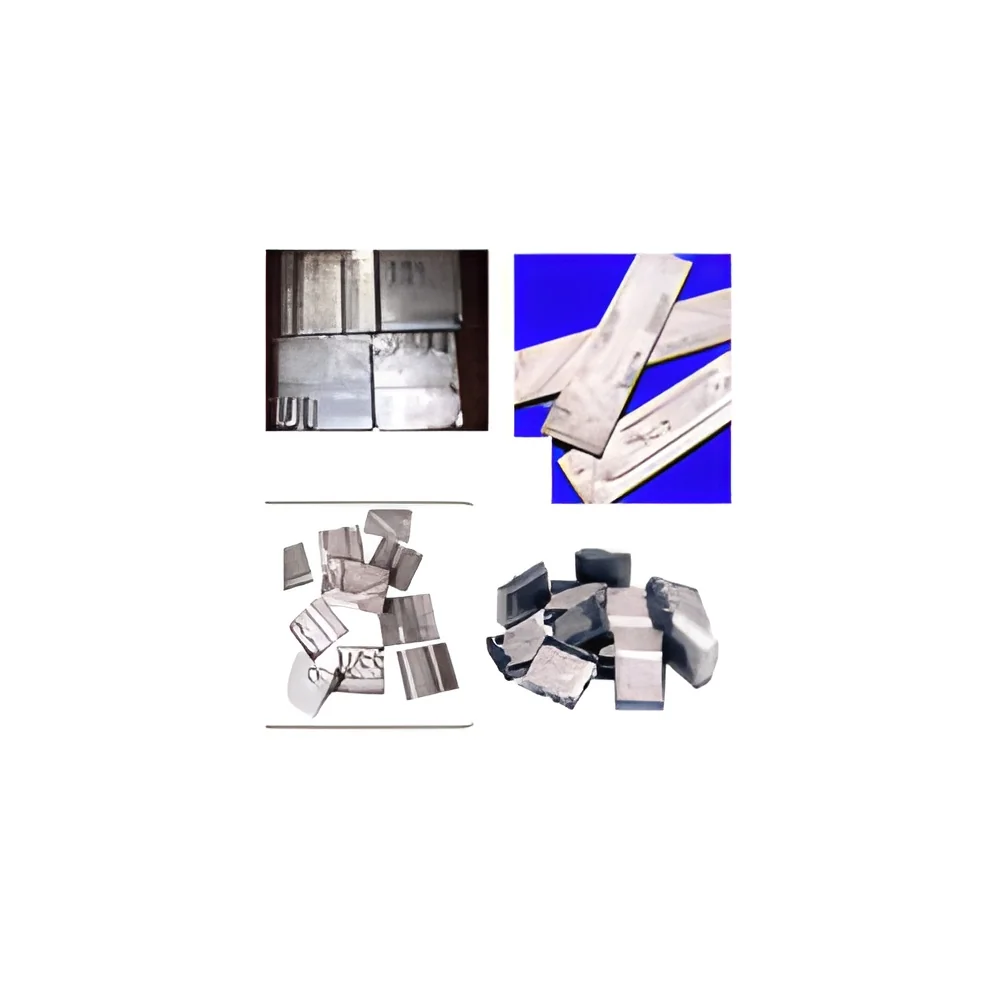
Our premium menthol crystals represent the gold standard in purity and reliability for pharmaceutical and industrial applications worldwide. Available in multiple pharmacopeial grades including IP, BP, EP, USP, and injectable specifications, these crystals meet the most stringent quality requirements for sensitive formulations. With FDA-approved manufacturing facilities and over five decades of industry expertise since 1971, we guarantee consistent quality, batch-to-batch uniformity, and full compliance with international regulatory standards. Our ready stock availability ensures timely delivery while maintaining the crystalline purity and characteristic cooling properties that define exceptional menthol performance across diverse applications.

Pharmaceutical manufacturers trust our menthol crystals for developing over-the-counter medications, prescription drugs, and therapeutic formulations where purity directly impacts patient outcomes. The chemical processing industry utilizes our ...
Our premium menthol crystals represent the gold standard in purity and reliability for pharmaceutical and industrial applications worldwide. Available in multiple pharmacopeial grades including IP, BP, EP, USP, and injectable specifications, these crystals meet the most stringent quality requirements for sensitive formulations. With FDA-approved manufacturing facilities and over five decades of industry expertise since 1971, we guarantee consistent quality, batch-to-batch uniformity, and full compliance with international regulatory standards. Our ready stock availability ensures timely delivery while maintaining the crystalline purity and characteristic cooling properties that define exceptional menthol performance across diverse applications.

Pharmaceutical manufacturers trust our menthol crystals for developing over-the-counter medications, prescription drugs, and therapeutic formulations where purity directly impacts patient outcomes. The chemical processing industry utilizes our product for fragrance compounding, flavor enhancement, and specialty chemical production requiring precise melting points and solubility characteristics. Additional sectors include tobacco manufacturing, cosmetics production, aromatherapy products, and confectionery manufacturing where menthol serves dual roles as both active ingredient and functional additive. Our clients include formulation scientists, production managers, and procurement specialists who depend on consistent quality for their end products' success and regulatory compliance.

We deliver outstanding value through reliable supply chain management, technical expertise, and consistent product performance tailored to specific application requirements. Our established presence since 1971 demonstrates proven reliability and customer satisfaction across global markets. The company's FDA certification and multiple pharmacopeial compliances provide assurance of quality and safety for sensitive applications requiring traceability and documentation. We differentiate through responsive customer service, flexible operational capabilities, and competitive pricing for bulk quantities without compromising the technical specifications that matter most to discerning buyers in regulated industries.

Key Features:
- Multiple pharmacopeial grades including IP BP EP USP injectable
- FDA-approved manufacturing facility with decades of experience
- Consistent crystalline structure with guaranteed high purity levels
- Ready stock availability for immediate shipment requirements
- Standardized particle size and packaging for manufacturing consistency

Benefits:
- Multiple pharmacopeial compliances ensure global regulatory acceptance
- Established manufacturing track record since 1971 guarantees reliability
- High purity levels deliver consistent performance in formulations
- Immediate availability supports production schedules and urgent needs
- Standardized specifications ensure manufacturing process consistency
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Pharmaceutical manufacturers depend on these premium menthol crystals for developing effective therapeutic formulations where purity cannot be compromised. The crystals serve as active ingredients in cough suppressants, topical analgesics, and respiratory treatments, providing consistent cooling relief while meeting stringent pharmacopeial standards for patient safety and product efficacy across global markets.
Industrial applications leverage these high-purity crystals for flavor enhancement in confectionery products, fragrance development in personal care items, and functional additives in tobacco processing. The consistent quality ensures reliable performance in cosmetics, oral hygiene products, and aromatherapy applications where batch-to-batch uniformity and precise melting characteristics are essential for manufacturing success.
- Pharmaceutical tablets and lozenges for cough and cold symptom relief
- Topical analgesic creams and ointments for muscle pain management
- Flavoring compounds for confectionery, chewing gum, and oral care products
- Fragrance manufacturing for cosmetics, perfumes, and personal care items
- Tobacco processing for consistent mentholation and product enhancement
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
A. S. Joshi & Company, Maharashtra
 Maharashtra, India
Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Premium Menthol Crystals IP BP EP USP Injectable Bulk Supplier
Premium menthol crystals in IP BP EP USP injectable grades from trusted manufacturer since 1971. Ideal for pharmaceutical formulations requiring reliable cooling properties and strict purity standards.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
A. S. Joshi & Company
 Maharashtra, India
Distributor / Wholesaler