IN
₹
Apparel & Fashion
Description
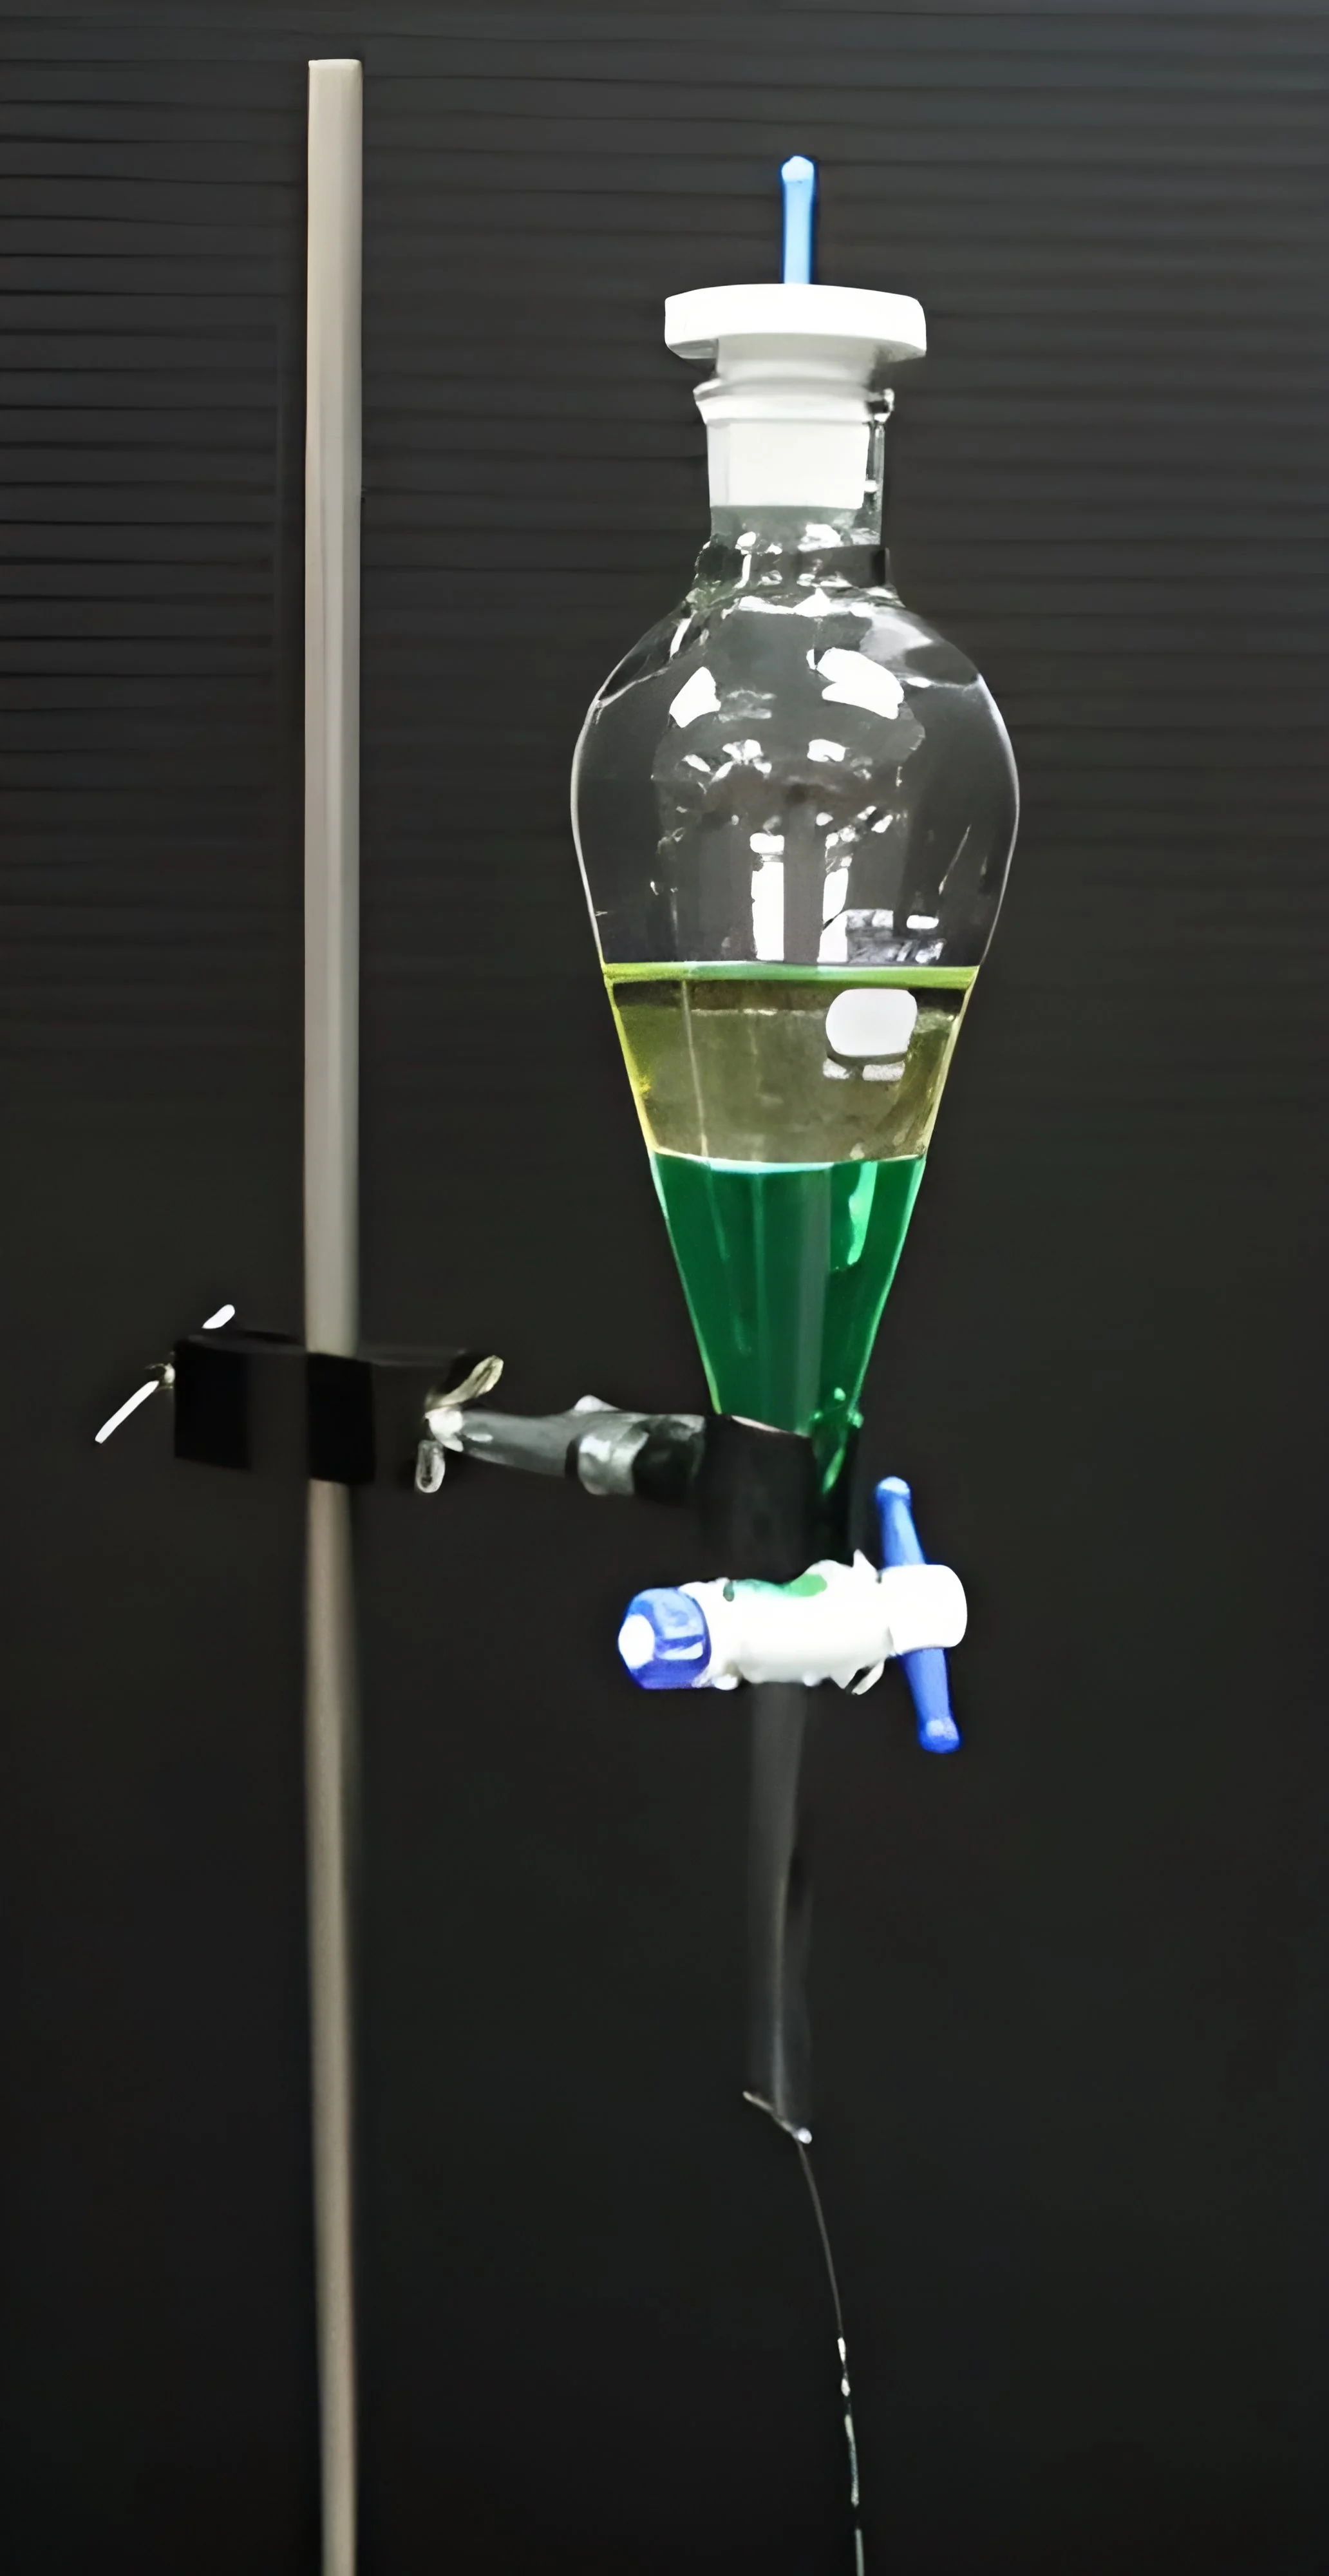
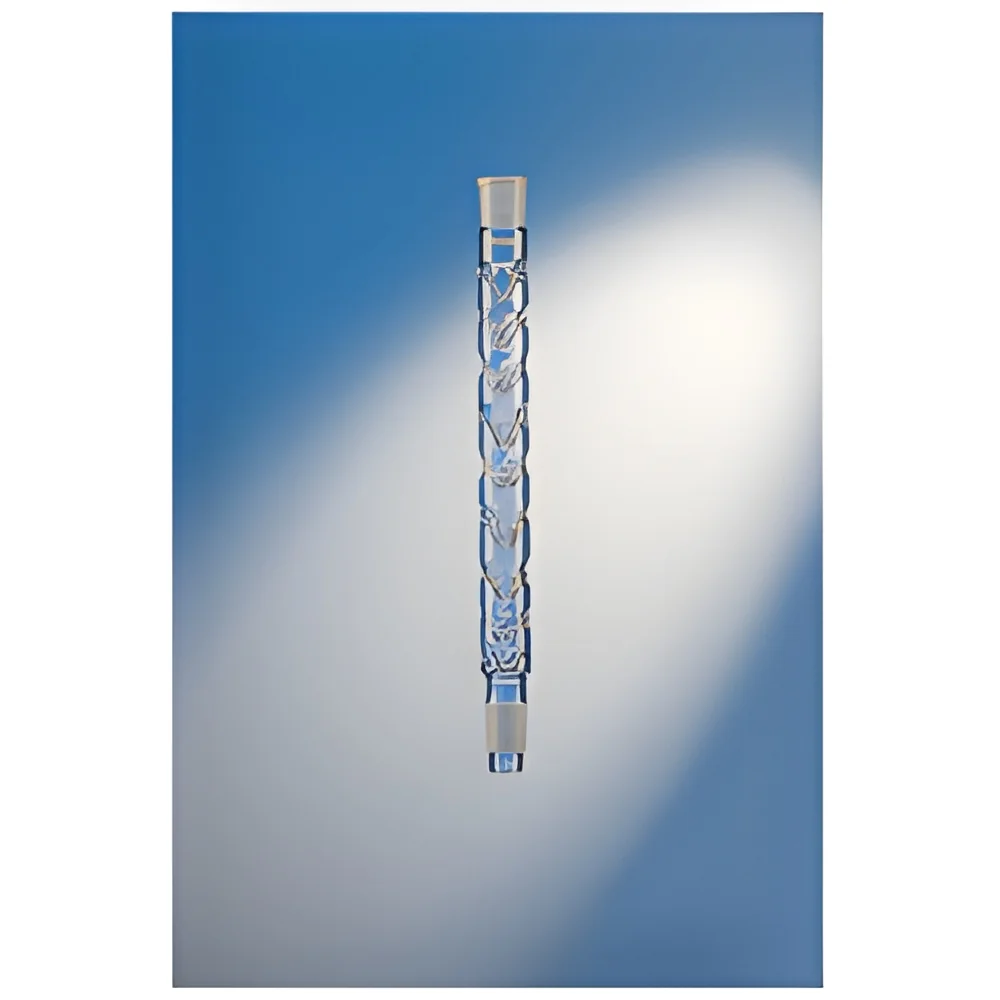
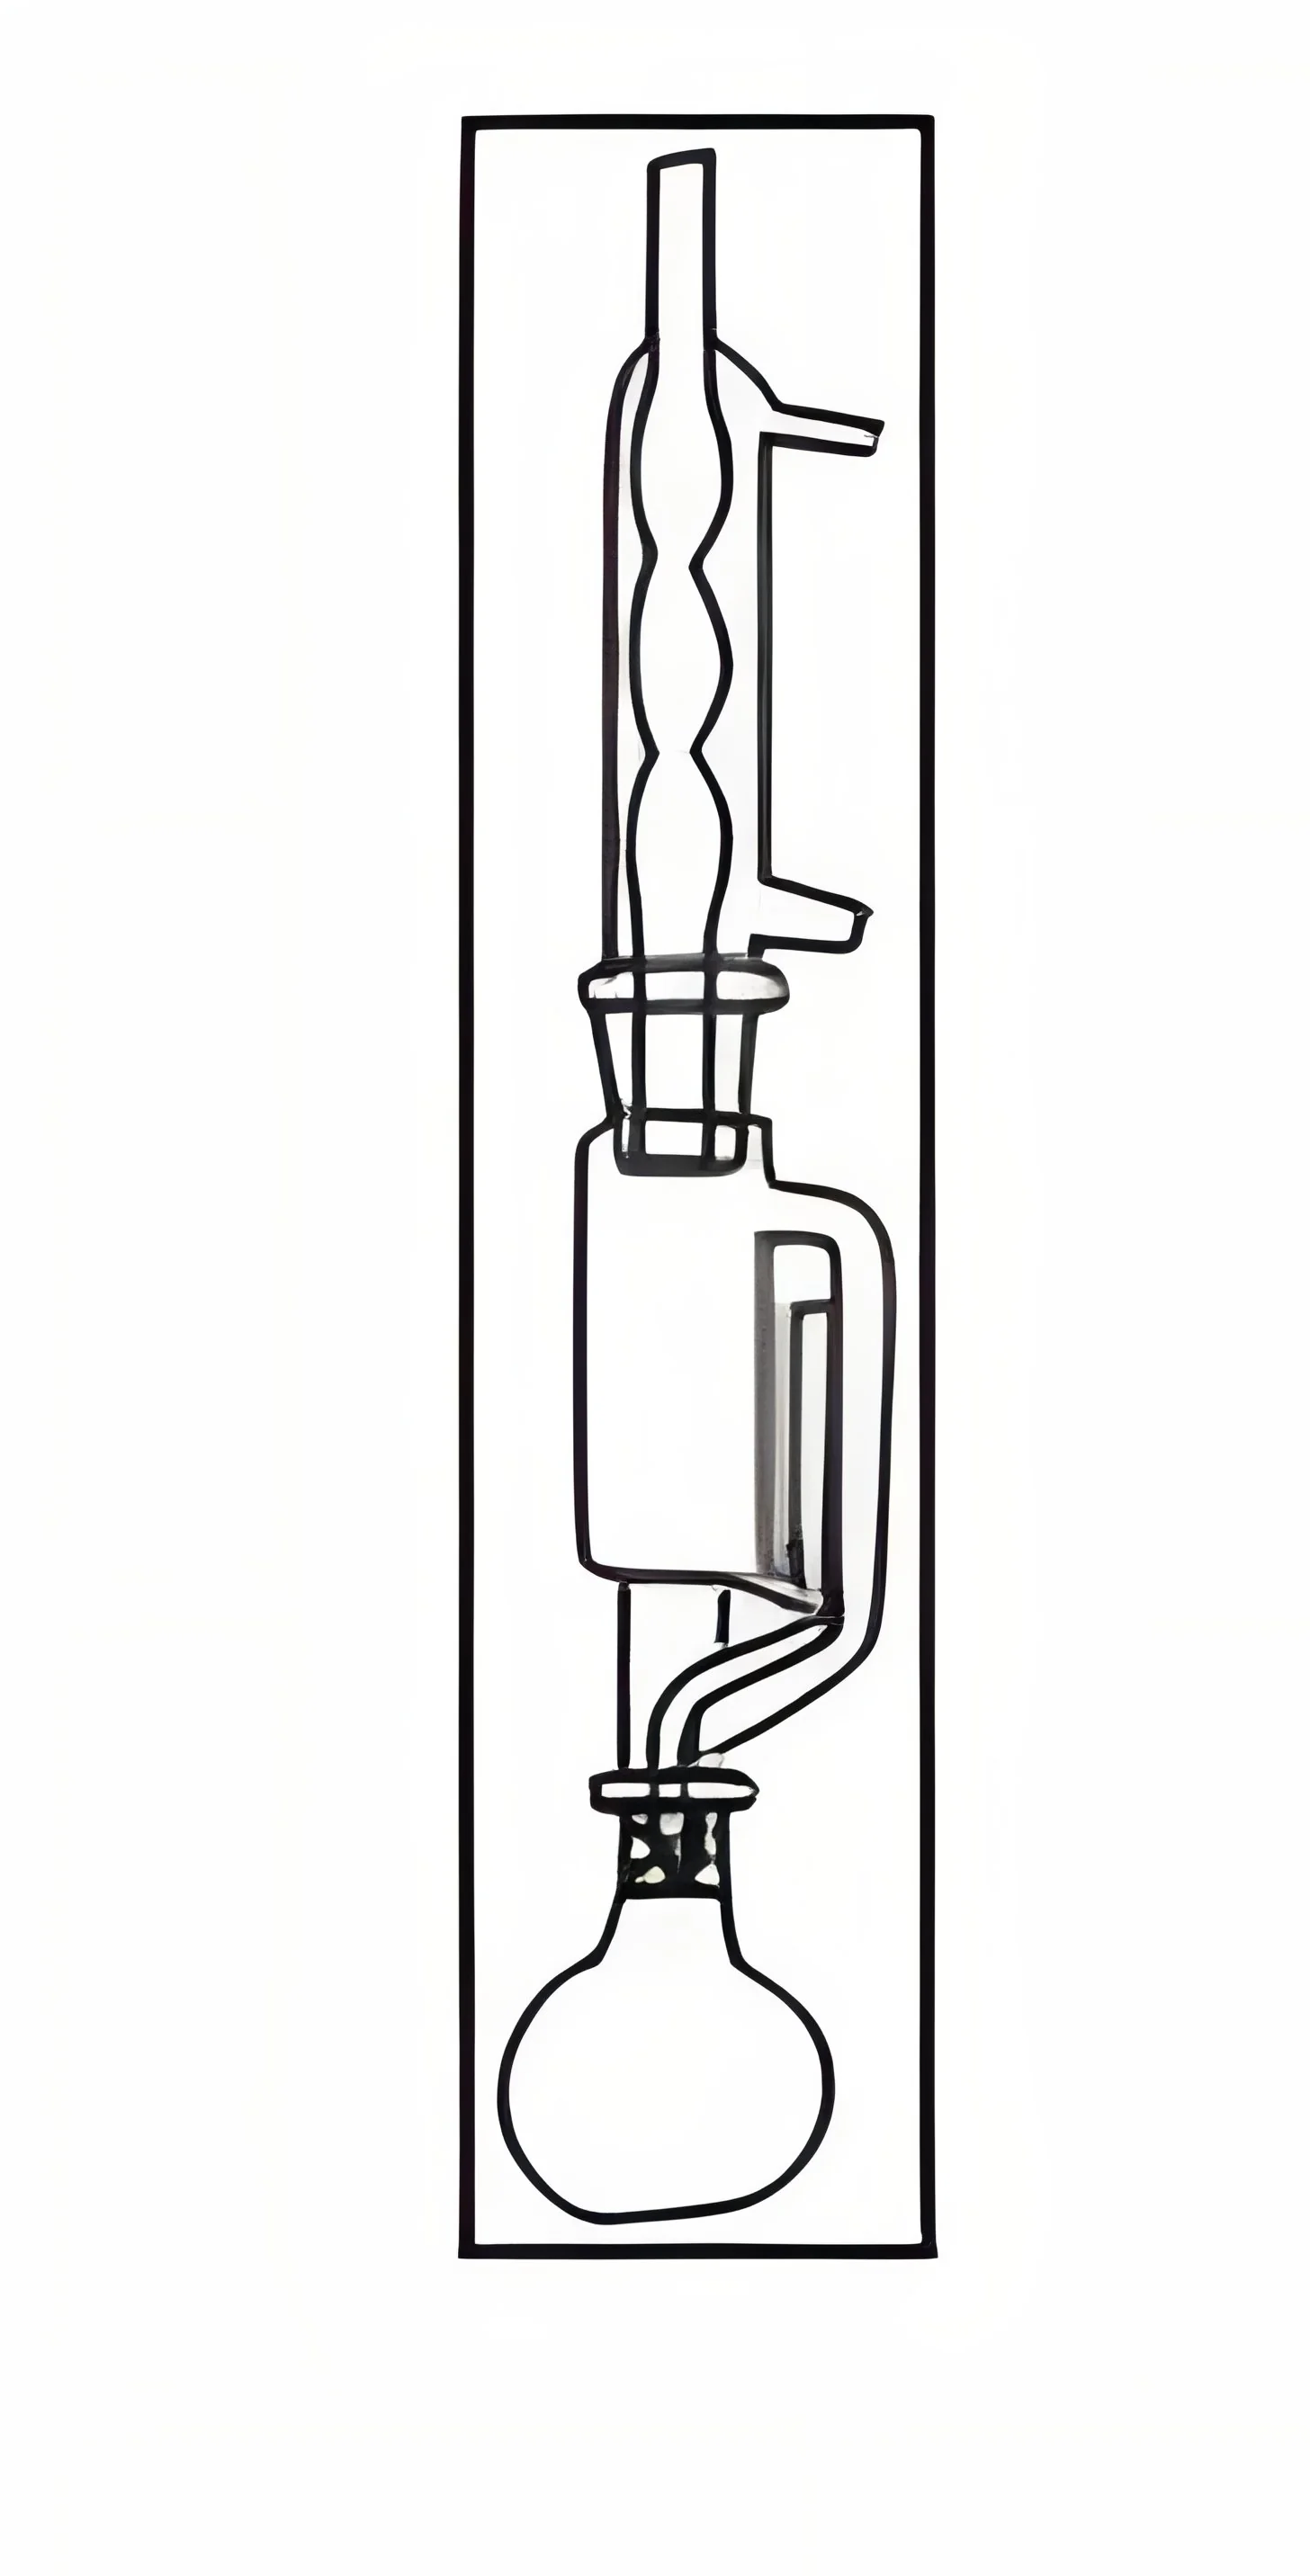
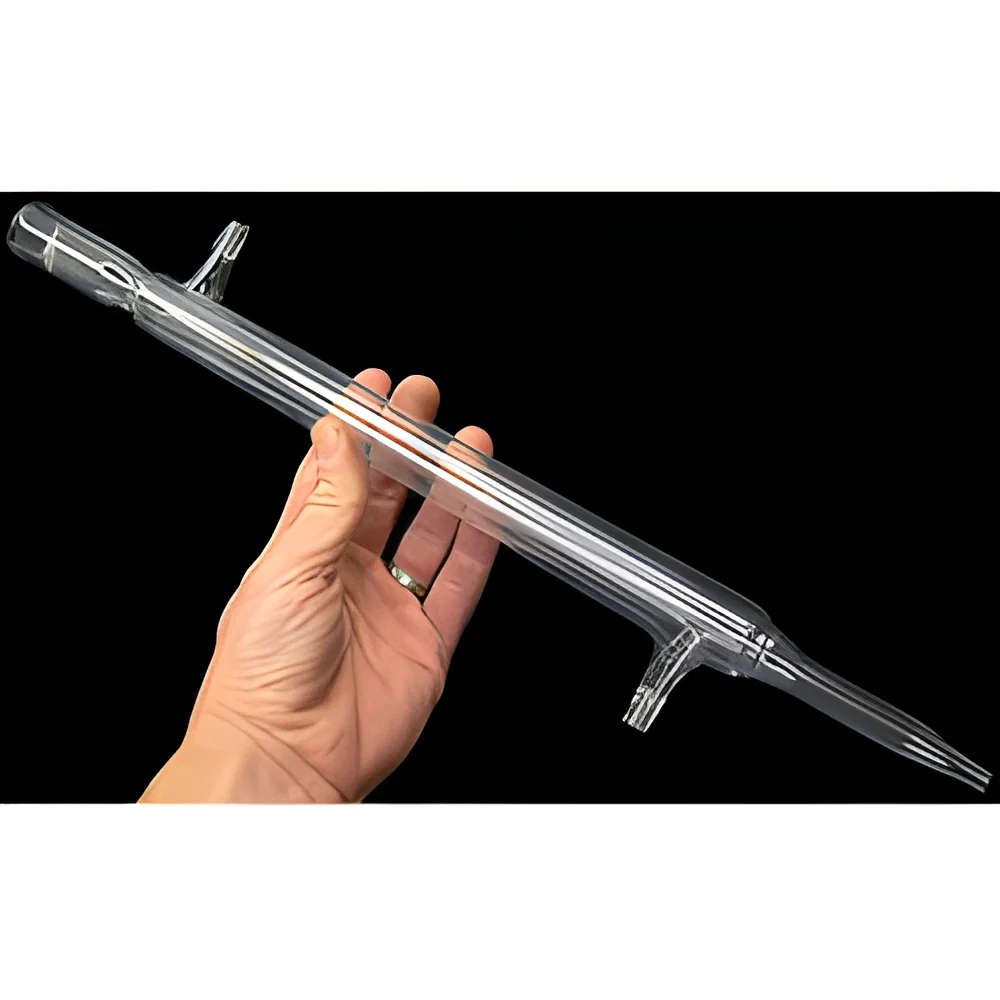
Our premium lab distillators are engineered for exceptional precision and durability in demanding laboratory environments. These advanced systems feature sophisticated temperature control mechanisms and efficient condensation systems that ensure consistent, high-purity results in every distillation process. Built to handle various chemicals and solvents safely, they provide reliable performance for both research and industrial applications while maintaining strict quality standards throughout operation. The robust construction and thoughtful engineering make these units suitable for continuous use in critical laboratory settings where accuracy and reliability are non-negotiable requirements for successful operations.

These distillation systems serve vital roles across multiple industries including pharmaceutical manufacturing, chemical production, research institutions, and quality control laboratories. In pharmaceutical applications, they ensure pure solvent recovery for drug develop...
Our premium lab distillators are engineered for exceptional precision and durability in demanding laboratory environments. These advanced systems feature sophisticated temperature control mechanisms and efficient condensation systems that ensure consistent, high-purity results in every distillation process. Built to handle various chemicals and solvents safely, they provide reliable performance for both research and industrial applications while maintaining strict quality standards throughout operation. The robust construction and thoughtful engineering make these units suitable for continuous use in critical laboratory settings where accuracy and reliability are non-negotiable requirements for successful operations.

These distillation systems serve vital roles across multiple industries including pharmaceutical manufacturing, chemical production, research institutions, and quality control laboratories. In pharmaceutical applications, they ensure pure solvent recovery for drug development and production processes. Chemical laboratories utilize them for precise separation processes and solvent purification tasks. Water treatment facilities rely on these units for producing high-purity water, while essential oil producers use them for extraction and refinement operations. Educational institutions and research centers benefit from their accuracy and reliability in experimental settings and analytical procedures.

The business value of these lab distillators lies in their exceptional reliability, operational efficiency, and long-term cost-effectiveness. They significantly reduce solvent waste through efficient recovery systems, lowering operational costs while supporting environmental sustainability initiatives. The integrated safety features enhance laboratory protection, reducing potential hazards associated with distillation processes. These units support continuous high-volume processing without compromising output quality, ensuring consistent performance that meets industry standards and regulatory requirements. Their extended service life and minimal maintenance requirements provide excellent return on investment for organizations requiring dependable purification solutions.

Key Features:
- Precise temperature control system for accurate distillation processes
- High-quality corrosion-resistant construction materials
- Efficient condensation system for maximum solvent recovery
- Multiple capacity options to suit different laboratory needs
- User-friendly interface with integrated safety features

Benefits:
- Reduced solvent consumption through efficient recovery systems
- Lower operational costs with minimal maintenance requirements
- Enhanced laboratory safety with built-in protection features
- Consistent high-purity output meeting industry standards
- Long service life providing excellent investment value
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Premium lab distillators deliver high-purity solvent recovery and chemical separation for pharmaceutical, chemical, and research laboratories. These robust systems ensure accurate purification for testing, production, and quality control across various industries. Their durable construction supports continuous operation in demanding environments while maintaining consistent performance and output quality standards.
These precision instruments are widely utilized in water purification, essential oil extraction, fuel analysis, and pharmaceutical manufacturing. Laboratories depend on them for reliable separation processes, solvent recycling, and maintaining purity standards in both research and industrial settings. The systems adapt to diverse laboratory configurations and specific application requirements with consistent performance.
- Purification of laboratory solvents and chemicals for reuse
- Essential oil and aromatic compound extraction from botanicals
- High-purity water production for laboratory testing and analysis
- Fuel and lubricant analysis in quality control laboratories
- Pharmaceutical ingredient separation and refinement processes
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Abhishek Scientific Company, Maharashtra
 Maharashtra, India
Electronics & Electrical•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Premium Lab Distillators For Solvent Purification And Recovery
Premium lab distillators for precise solvent purification and recovery in industrial and research labs. Engineered for reliability and efficiency to meet strict quality standards in demanding applications.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Abhishek Scientific Company
 Maharashtra, India
Electronics & ElectricalManufacturer