IN
₹
Apparel & Fashion
Description
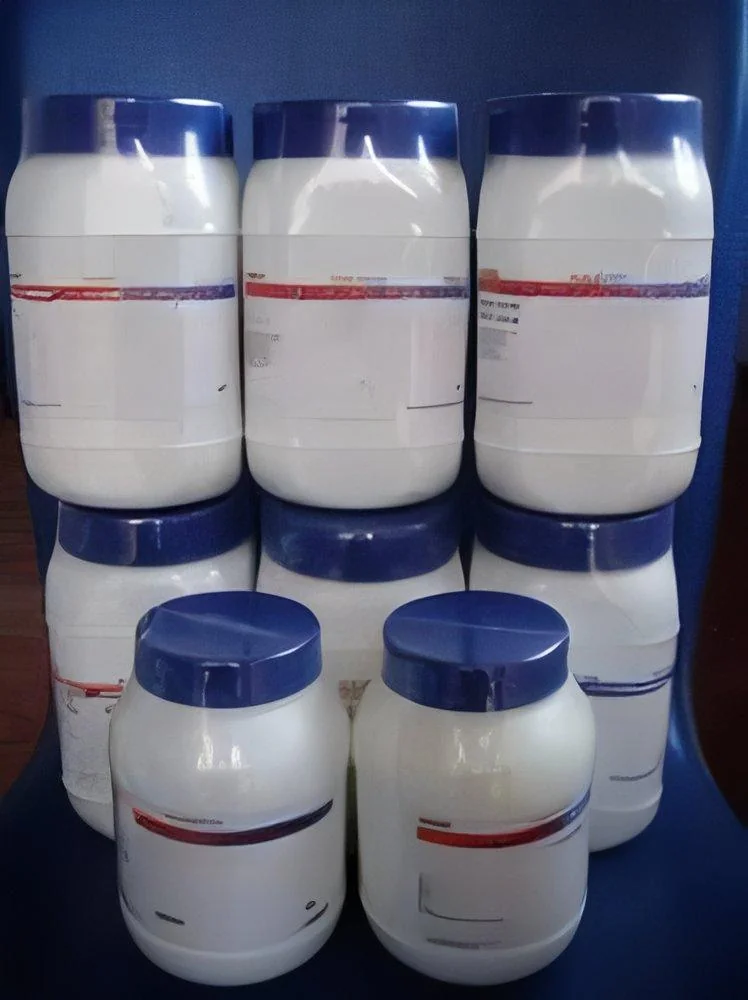
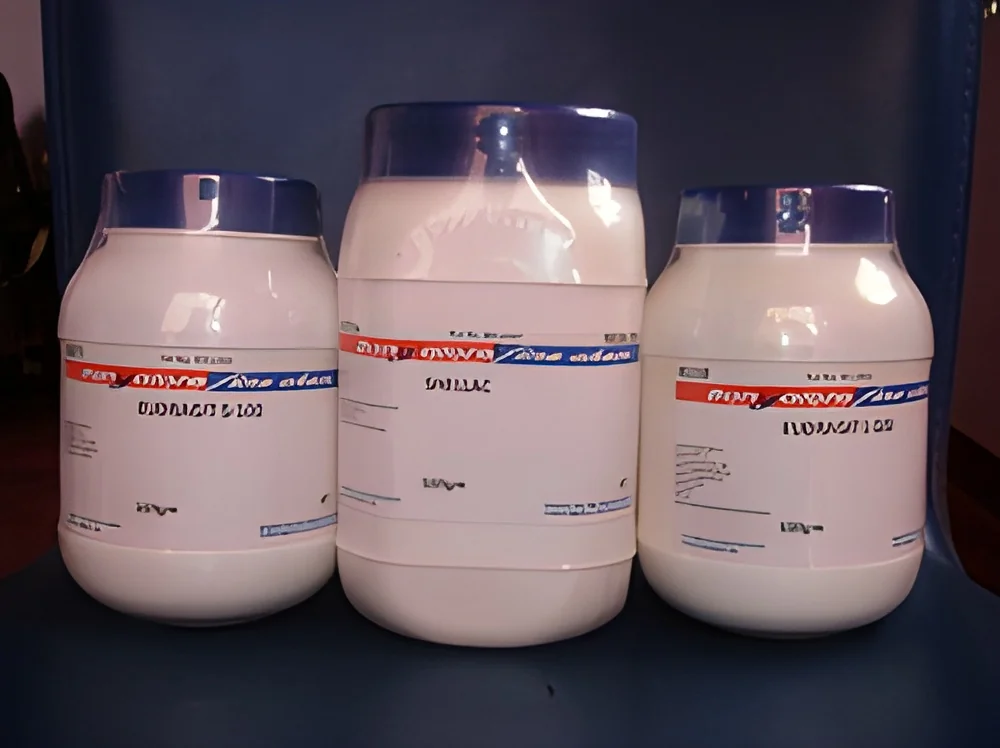
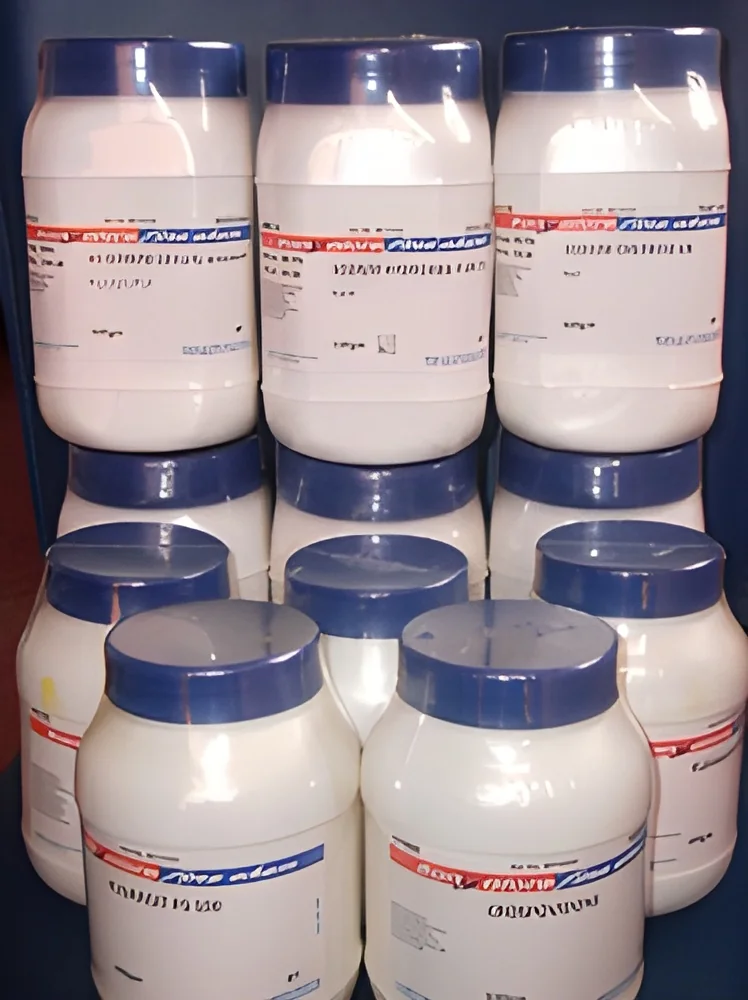
Our premium laboratory chemicals represent the highest standard of purity and reliability for professional industrial and research applications. We supply a comprehensive range of high-purity reagents, solvents, and acids that meet strict quality specifications for demanding environments. Each chemical undergoes rigorous testing and quality assurance protocols to ensure batch-to-batch consistency and performance reliability. Our products are manufactured under controlled conditions and packaged to maintain chemical integrity during storage and transportation. We understand that your processes depend on consistent quality, which is why we prioritize precision in every formulation. These chemicals are specifically designed for analytical testing, research experiments, and production processes where accuracy is non-negotiable. We serve distributors, wholesalers, and large-scale buyers who require dependable chemical solutions for their critical operations and manufacturing requirements.

...
Our premium laboratory chemicals represent the highest standard of purity and reliability for professional industrial and research applications. We supply a comprehensive range of high-purity reagents, solvents, and acids that meet strict quality specifications for demanding environments. Each chemical undergoes rigorous testing and quality assurance protocols to ensure batch-to-batch consistency and performance reliability. Our products are manufactured under controlled conditions and packaged to maintain chemical integrity during storage and transportation. We understand that your processes depend on consistent quality, which is why we prioritize precision in every formulation. These chemicals are specifically designed for analytical testing, research experiments, and production processes where accuracy is non-negotiable. We serve distributors, wholesalers, and large-scale buyers who require dependable chemical solutions for their critical operations and manufacturing requirements.

These laboratory chemicals are essential across multiple industries that rely on precise chemical reactions and analyses for their core operations. The pharmaceutical industry utilizes them extensively for drug development, quality control verification, and manufacturing processes where chemical purity directly impacts product safety and efficacy. Biotechnology companies depend on our chemicals in research laboratories for DNA sequencing, protein purification, and diagnostic test development. Manufacturing sectors incorporate them into quality assurance testing protocols, production processes, and material analysis systems. Educational institutions and research facilities use our products for teaching laboratories and scientific investigations requiring reliable chemical performance. Environmental testing laboratories rely on our chemicals for accurate water and soil analysis, while the food processing industry uses them for safety testing and quality certification processes that ensure regulatory compliance.

Investing in our laboratory chemicals delivers significant business value through enhanced operational reliability and reduced risk exposure. Our high-purity products minimize experimental errors and production defects caused by inconsistent chemical quality, ultimately saving time and valuable resources. The exceptional purity levels ensure accurate test results and reproducible processes, which is crucial for compliance with industry regulations and quality standards. We maintain robust supply chain relationships to ensure consistent availability and timely delivery, preventing operational disruptions that could impact production schedules. Our commitment to quality translates into long-term cost savings by reducing failed experiments, production reworks, and quality issues that arise from inferior chemical supplies. Partnering with us means accessing chemicals you can trust for your most critical applications, providing peace of mind and operational consistency for your business requirements.

Key Features:
- High-purity formulations meeting strict industry standards
- Rigorous quality control procedures and batch consistency testing
- Comprehensive chemical range including reagents, solvents, and acids
- Stable shelf life with specific storage recommendations
- Manufactured under controlled environmental conditions

Benefits:
- Consistent performance across batches and applications
- Reduced risk of experimental errors and production defects
- Compliance with industry regulations and quality standards
- Reliable supply chain ensuring operational continuity
- Long-term cost savings through quality assurance
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our high-purity lab chemicals enable precise analytical testing, quality control procedures, and complex research across scientific and industrial environments. These reagents, solvents, and acids deliver accurate, repeatable results in controlled laboratory settings, supporting critical processes where chemical consistency directly impacts outcomes and reliability. They form the foundation for innovation and quality assurance in professional applications requiring dependable chemical performance and standardized reactions.
These chemical solutions serve fundamental roles across manufacturing, healthcare, and technology sectors. Industries utilize them for product development, safety compliance verification, and scientific discovery initiatives. From large-scale production to specialized research projects, our chemicals provide the essential components for processes that demand purity, accuracy, and consistent performance metrics in various operational environments.
- Pharmaceutical manufacturing for drug formulation and quality testing
- Water treatment facilities for purity analysis and contaminant detection
- Food processing plants for safety compliance and quality verification
- Research institutions for experimental procedures and scientific studies
- Industrial production facilities for process control and material development
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Bangalore Fine Chem, Karnataka
 Karnataka, India
Raw Materials & Chemicals•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Premium Lab Chemicals High Purity Reagents Solvents Acids For Industrial Research
Premium lab chemicals supply high-purity reagents, solvents, and acids for industrial research and manufacturing applications, ensuring strict quality control and reliable performance for pharmaceuticals and biotechnology sectors.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Bangalore Fine Chem
 Karnataka, India
Raw Materials & ChemicalsManufacturer