IN
₹
Apparel & Fashion

Description
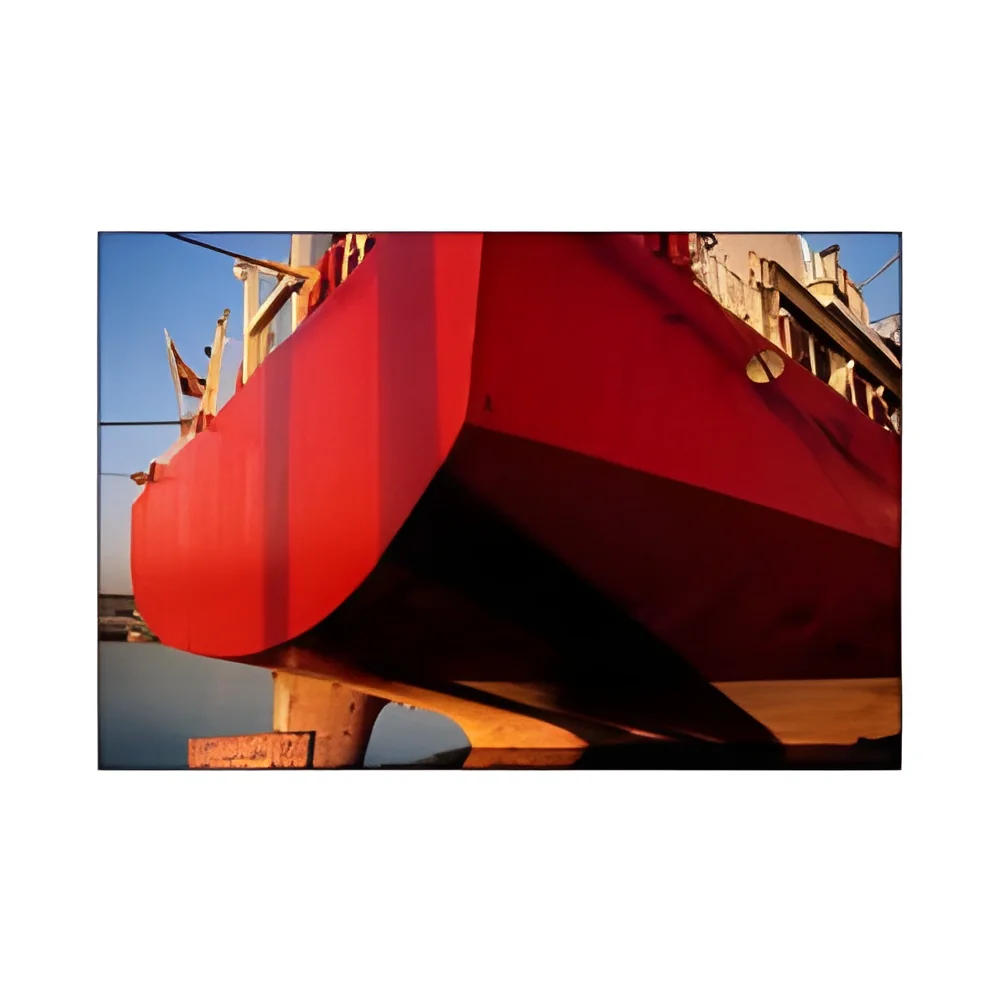
Industrial Protective Coatings represent advanced surface protection technology engineered for extreme environmental conditions. These premium formulations create a robust barrier that shields substrates from aggressive industrial and offshore challenges, significantly extending asset lifespan while reducing maintenance costs. Developed through rigorous research and testing, these coatings provide unmatched protection against heat, chemicals, and corrosion that would compromise standard protective solutions. The trusted quality ensures reliable performance where protection matters most.

These coatings serve critical protection needs across multiple industries including oil and gas infrastructure, chemical processing facilities, marine and offshore platforms, power generation plants, and heavy manufacturing operations. They are specifically designed to meet the demanding requirements of these sectors where equipment failure due to environmental degradation can lead to operational downt...
Industrial Protective Coatings represent advanced surface protection technology engineered for extreme environmental conditions. These premium formulations create a robust barrier that shields substrates from aggressive industrial and offshore challenges, significantly extending asset lifespan while reducing maintenance costs. Developed through rigorous research and testing, these coatings provide unmatched protection against heat, chemicals, and corrosion that would compromise standard protective solutions. The trusted quality ensures reliable performance where protection matters most.

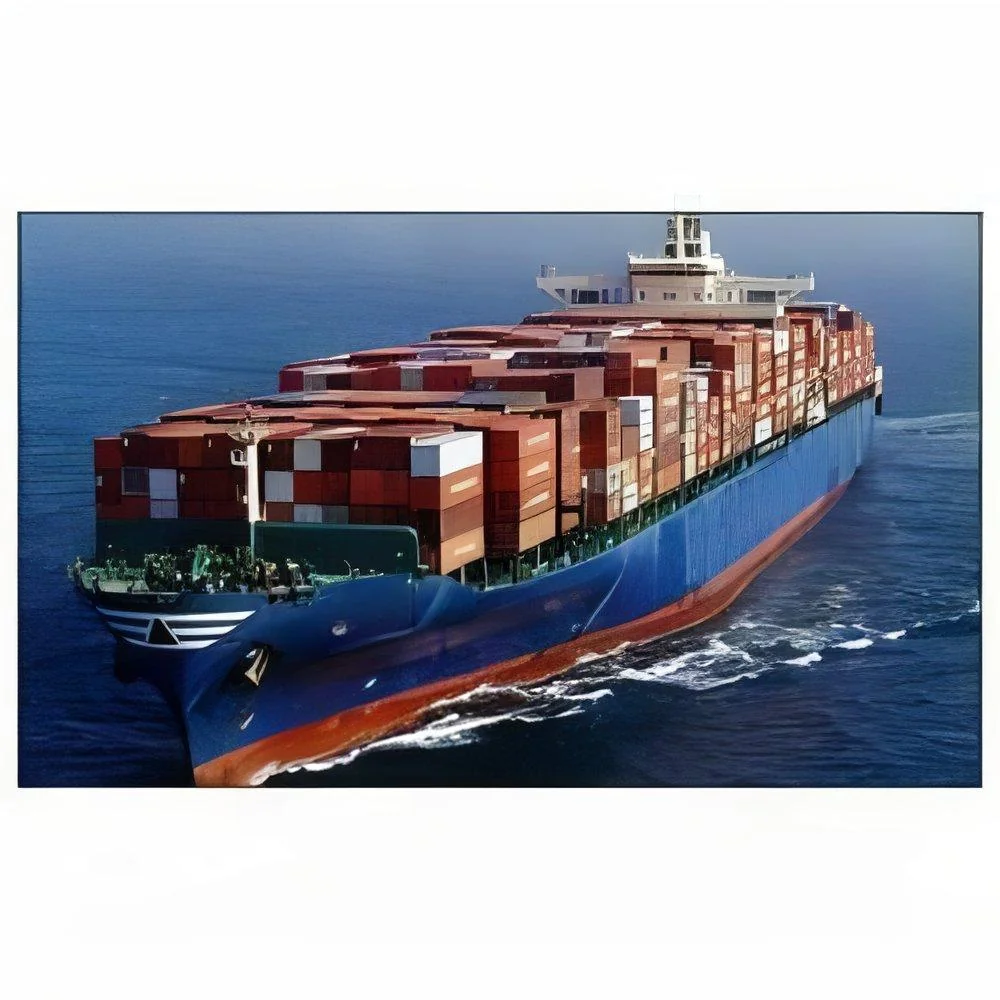
These coatings serve critical protection needs across multiple industries including oil and gas infrastructure, chemical processing facilities, marine and offshore platforms, power generation plants, and heavy manufacturing operations. They are specifically designed to meet the demanding requirements of these sectors where equipment failure due to environmental degradation can lead to operational downtime, safety concerns, and financial losses. The formulations address the unique challenges faced by each industry segment, providing tailored protection for diverse applications.

The business value of these protective coatings lies in their proven reliability and long-term cost-effectiveness. By providing superior protection against environmental degradation, they extend the operational lifespan of critical assets, reduce maintenance frequency, and minimize unexpected downtime. The unique quality and reliability ensure consistent performance, while customization options allow addressing specific operational challenges. This combination delivers tangible value through enhanced asset protection and operational continuity.

Key Features:
- Exceptional heat resistance for high-temperature environments
- Superior chemical resistance against acids, alkalis, and solvents
- Advanced corrosion protection for metal substrates
- Trusted quality with proven reliability in harsh conditions
- Formulated for extreme industrial and offshore applications

Benefits:
- Extends asset lifespan by protecting against environmental degradation
- Reduces maintenance costs and frequency through durable protection
- Minimizes operational downtime by preventing premature failure
- Provides reliable performance in the most challenging conditions
- Ensures long-term surface protection for critical infrastructure
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
These industrial protective coatings are engineered for extreme conditions where standard paints fail, providing a durable shield against aggressive elements to maintain structural integrity and surface protection. The specialized formulations resist extreme temperatures, chemical exposure, and corrosive atmospheres that degrade conventional coatings.
Ideal for demanding sectors including oil and gas facilities, chemical processing plants, marine structures, power generation units, and heavy manufacturing infrastructure. These coatings deliver reliable performance in challenging operational settings, protecting critical assets from degradation and supporting continuous operational efficiency.
- Offshore platforms and marine structures requiring corrosion resistance
- Chemical processing plants and storage tanks needing chemical protection
- Power generation facilities and refineries with high-temperature demands
- Industrial manufacturing plants and equipment facing wear and tear
- Bridges, pipelines, and structural steelwork in harsh environments
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Paladin Paints, Maharashtra
 Maharashtra, India
Raw Materials & Chemicals•Manufacturer•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Industrial Protective Coatings Heat Resistant Chemical Proof Corrosion Defying
Industrial Protective Coatings offer heat-resistant, chemical-proof, and corrosion-defying protection for metal and concrete substrates in harsh industrial and offshore environments. Premium quality ensures long-term asset reliability.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Paladin Paints
 Maharashtra, India
Raw Materials & ChemicalsManufacturer