IN
₹
Apparel & Fashion
Description
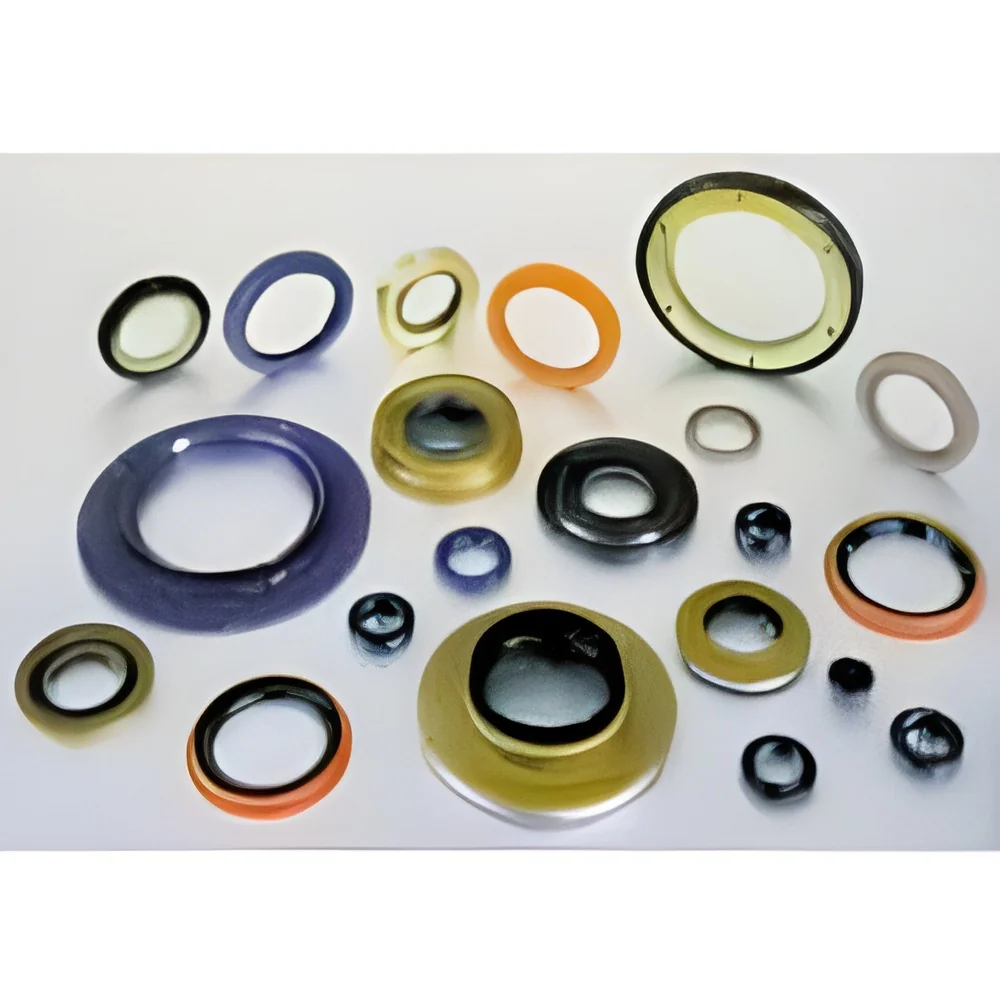
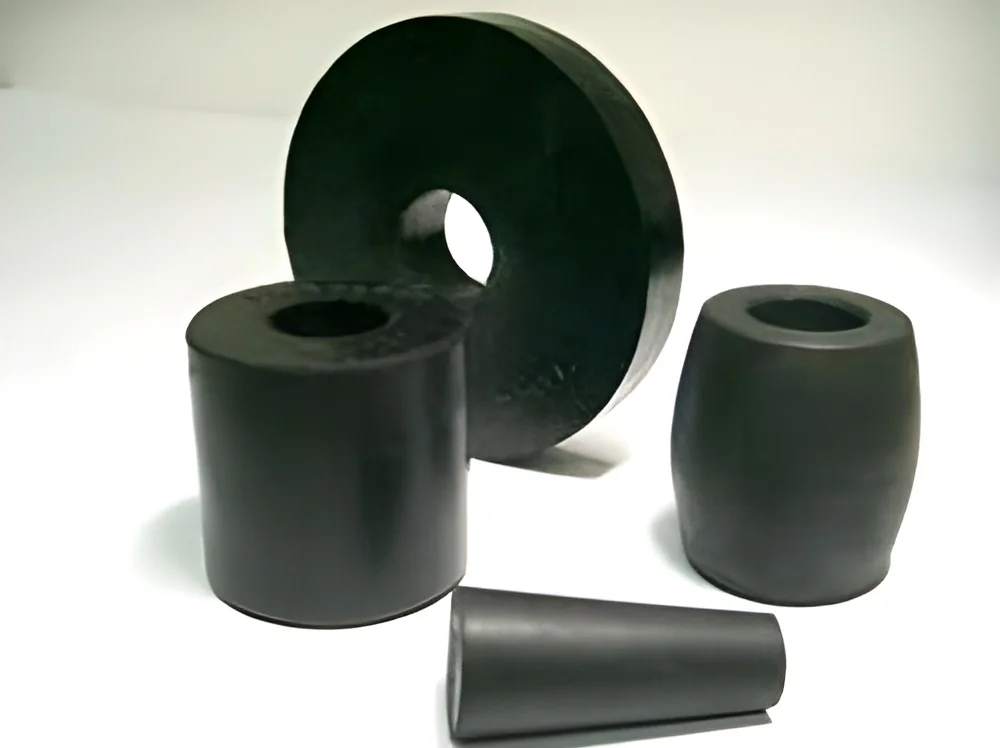
Our industrial rubber rings are engineered for applications where reliability cannot be compromised. Manufactured from premium-grade rubber compounds through strict quality-controlled processes, these rings deliver superior elasticity, exceptional wear resistance, and extended service life even in demanding operational conditions. Each ring undergoes rigorous testing to ensure consistent performance metrics, providing buyers with the assurance of quality that translates to reduced downtime and maintenance costs. The precise engineering ensures they maintain sealing integrity under pressure, temperature variations, and exposure to various industrial fluids and chemicals.

These industrial rubber rings serve critical functions across multiple sectors including manufacturing, automotive, chemical processing, and heavy machinery. In manufacturing plants, they ensure leak-proof connections in hydraulic and pneumatic systems, while automotive applications benefit from their vibration damping...
Our industrial rubber rings are engineered for applications where reliability cannot be compromised. Manufactured from premium-grade rubber compounds through strict quality-controlled processes, these rings deliver superior elasticity, exceptional wear resistance, and extended service life even in demanding operational conditions. Each ring undergoes rigorous testing to ensure consistent performance metrics, providing buyers with the assurance of quality that translates to reduced downtime and maintenance costs. The precise engineering ensures they maintain sealing integrity under pressure, temperature variations, and exposure to various industrial fluids and chemicals.

These industrial rubber rings serve critical functions across multiple sectors including manufacturing, automotive, chemical processing, and heavy machinery. In manufacturing plants, they ensure leak-proof connections in hydraulic and pneumatic systems, while automotive applications benefit from their vibration damping properties in engine and transmission assemblies. Chemical processing facilities rely on their resistance to corrosive substances, and construction equipment manufacturers utilize them for their durability under extreme operational stress. The versatility makes them indispensable components for original equipment manufacturers, maintenance teams, and industrial suppliers across sectors involving mechanical systems and fluid transfer.

For decision-makers, these rubber rings offer tangible value through enhanced operational reliability, reduced maintenance requirements, and long-term cost savings. The investment in premium-quality rings translates to fewer system failures, minimized production interruptions, and improved workplace safety through reliable leak prevention. Their consistent quality maintained through strict manufacturing controls means operations can standardize these components with confidence in their performance and durability, ensuring optimal function without compromise across various applications.

Key Features:
- Premium rubber compounds formulated for maximum durability and flexibility
- Excellent sealing and cushioning properties maintained under pressure
- Superior resistance to abrasion, oils, chemicals, and temperature extremes
- Available in various sizes to match specific application requirements
- Consistent quality assurance through rigorous manufacturing controls and testing

Benefits:
- Enhanced operational reliability with reduced system failures and downtime
- Long-term cost savings through extended service life and minimal maintenance
- Improved workplace safety via reliable leak prevention and vibration control
- Versatile performance across multiple industrial environments and applications
- Consistent quality that allows for standardization across operations
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial rubber rings are essential for preventing leaks and ensuring system integrity across demanding applications. They provide reliable performance in hydraulic systems, pipelines, and mechanical assemblies where pressure resistance and environmental durability are critical for operational safety and efficiency.
These versatile rings serve as effective vibration dampers and insulation components in challenging environments. Their flexibility and resistance to temperature extremes, oils, and chemicals make them suitable for automotive, manufacturing, and processing applications where consistent performance under stress is non-negotiable for smooth operations.
- Hydraulic cylinder seals and fluid power systems in industrial machinery
- Pipeline gaskets and connection seals for water and chemical processing plants
- Automotive engine seals, transmission components, and vibration isolation mounts
- Industrial equipment vibration dampers and noise reduction systems
- Electrical insulation rings and protective covers for electronic assemblies
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Dolphin Rubber Industries, Gujarat
 Gujarat, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
South Asia
Industrial Rubber Rings For Sealing And Vibration Damping
Premium industrial rubber rings for reliable sealing and vibration damping in machinery, pipes, and automotive assemblies. Durable materials and strict quality control ensure long-lasting performance for importers and distributors.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Dolphin Rubber Industries
 Gujarat, India
Industrial Equipment & MachineryManufacturer