IN
₹
Description
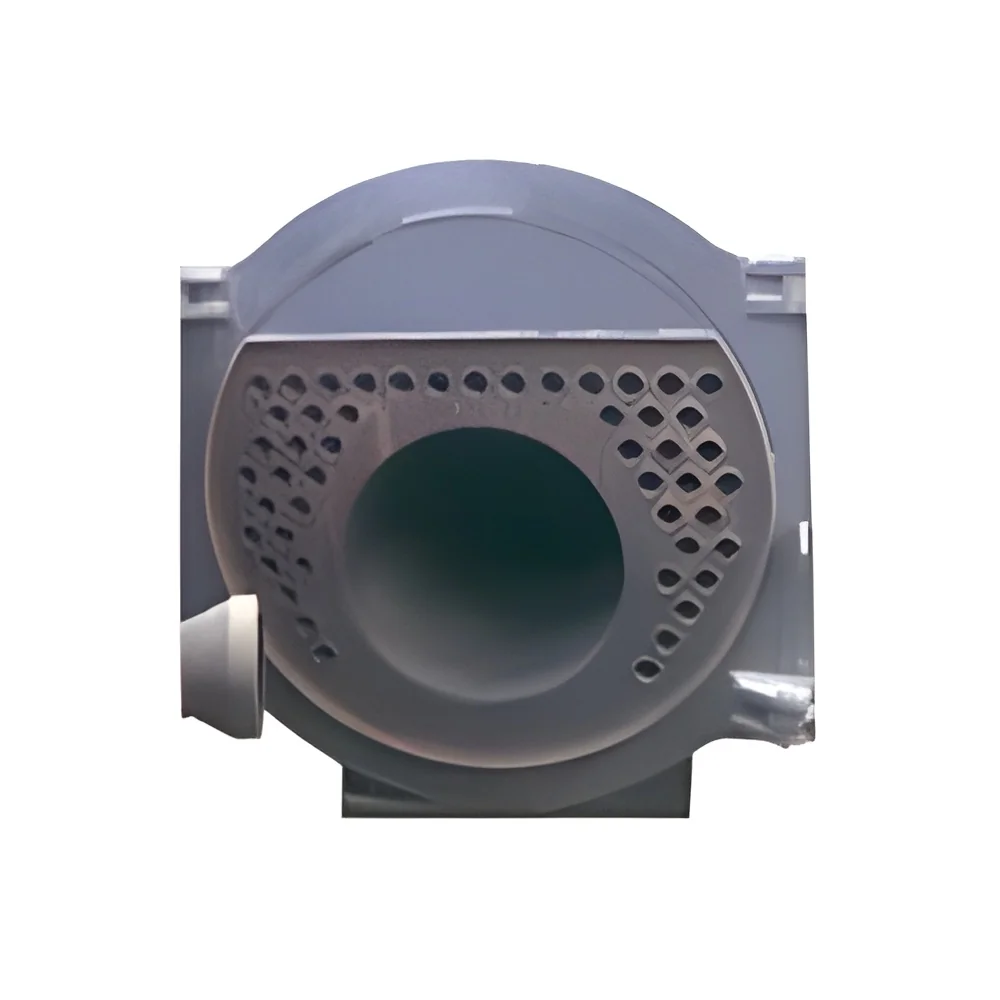
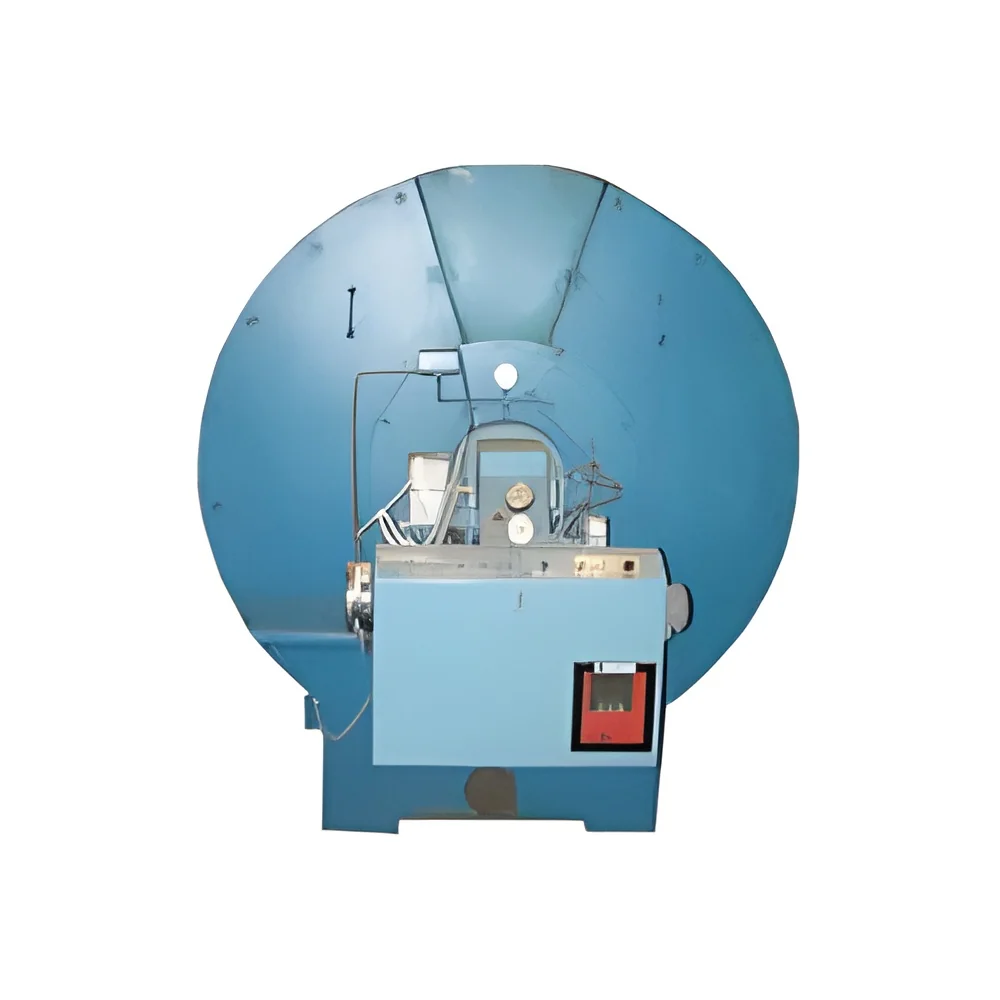
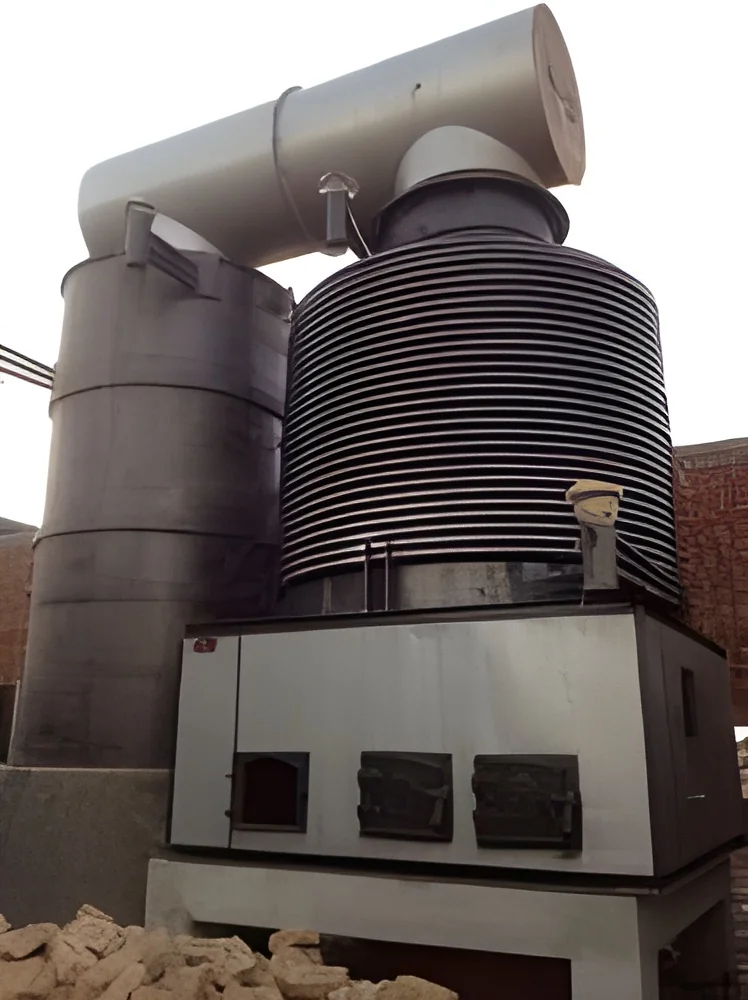
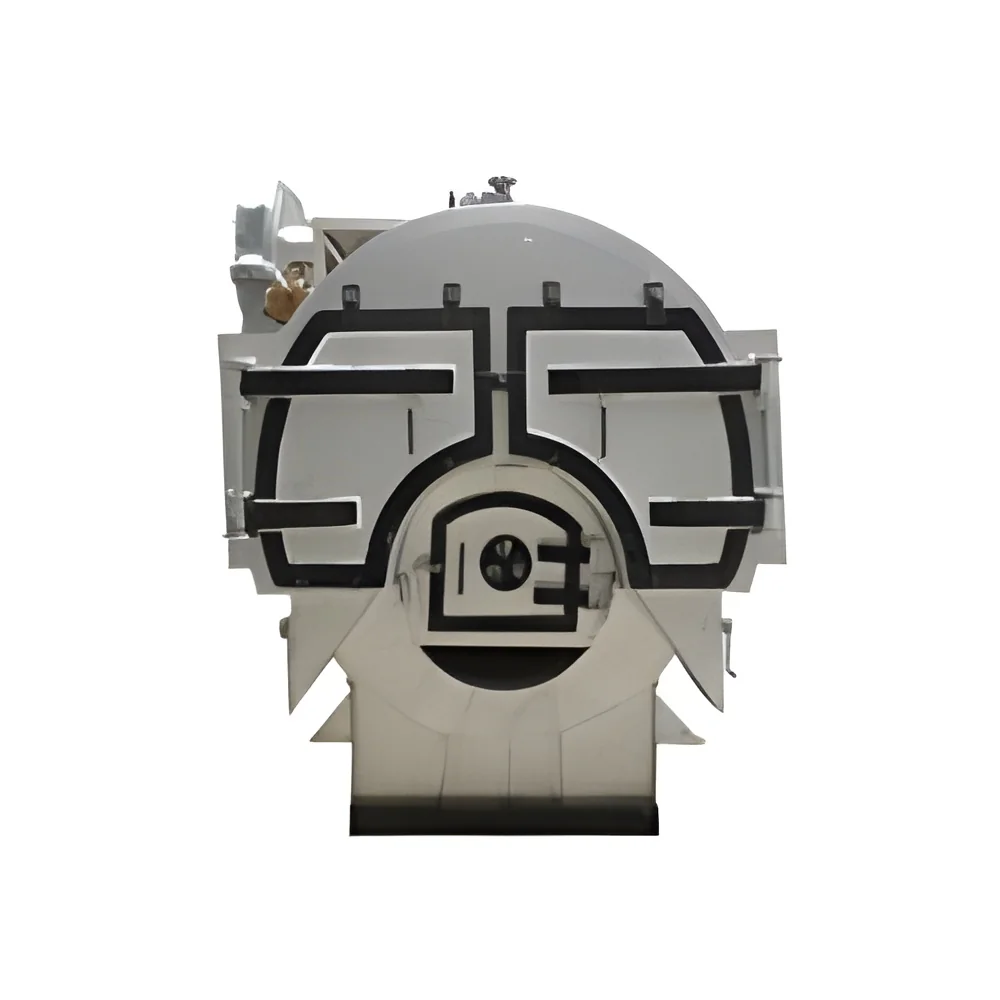
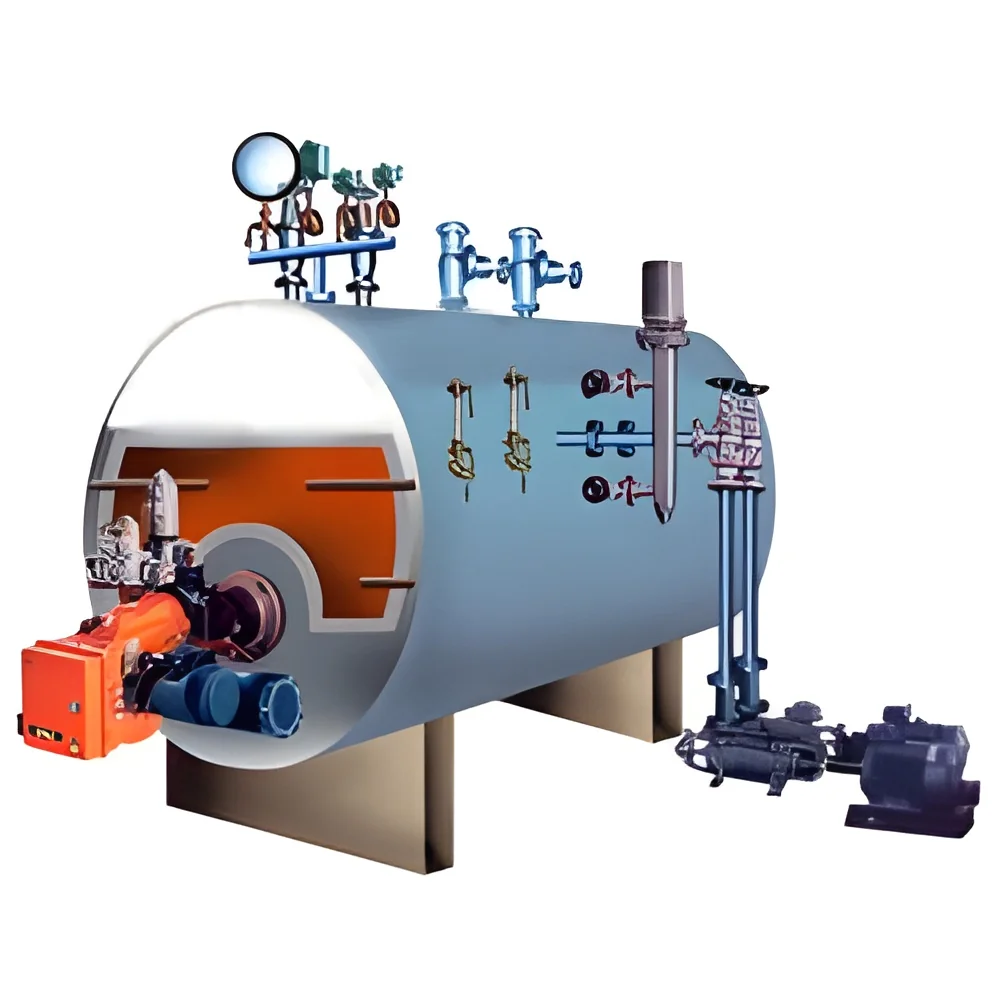
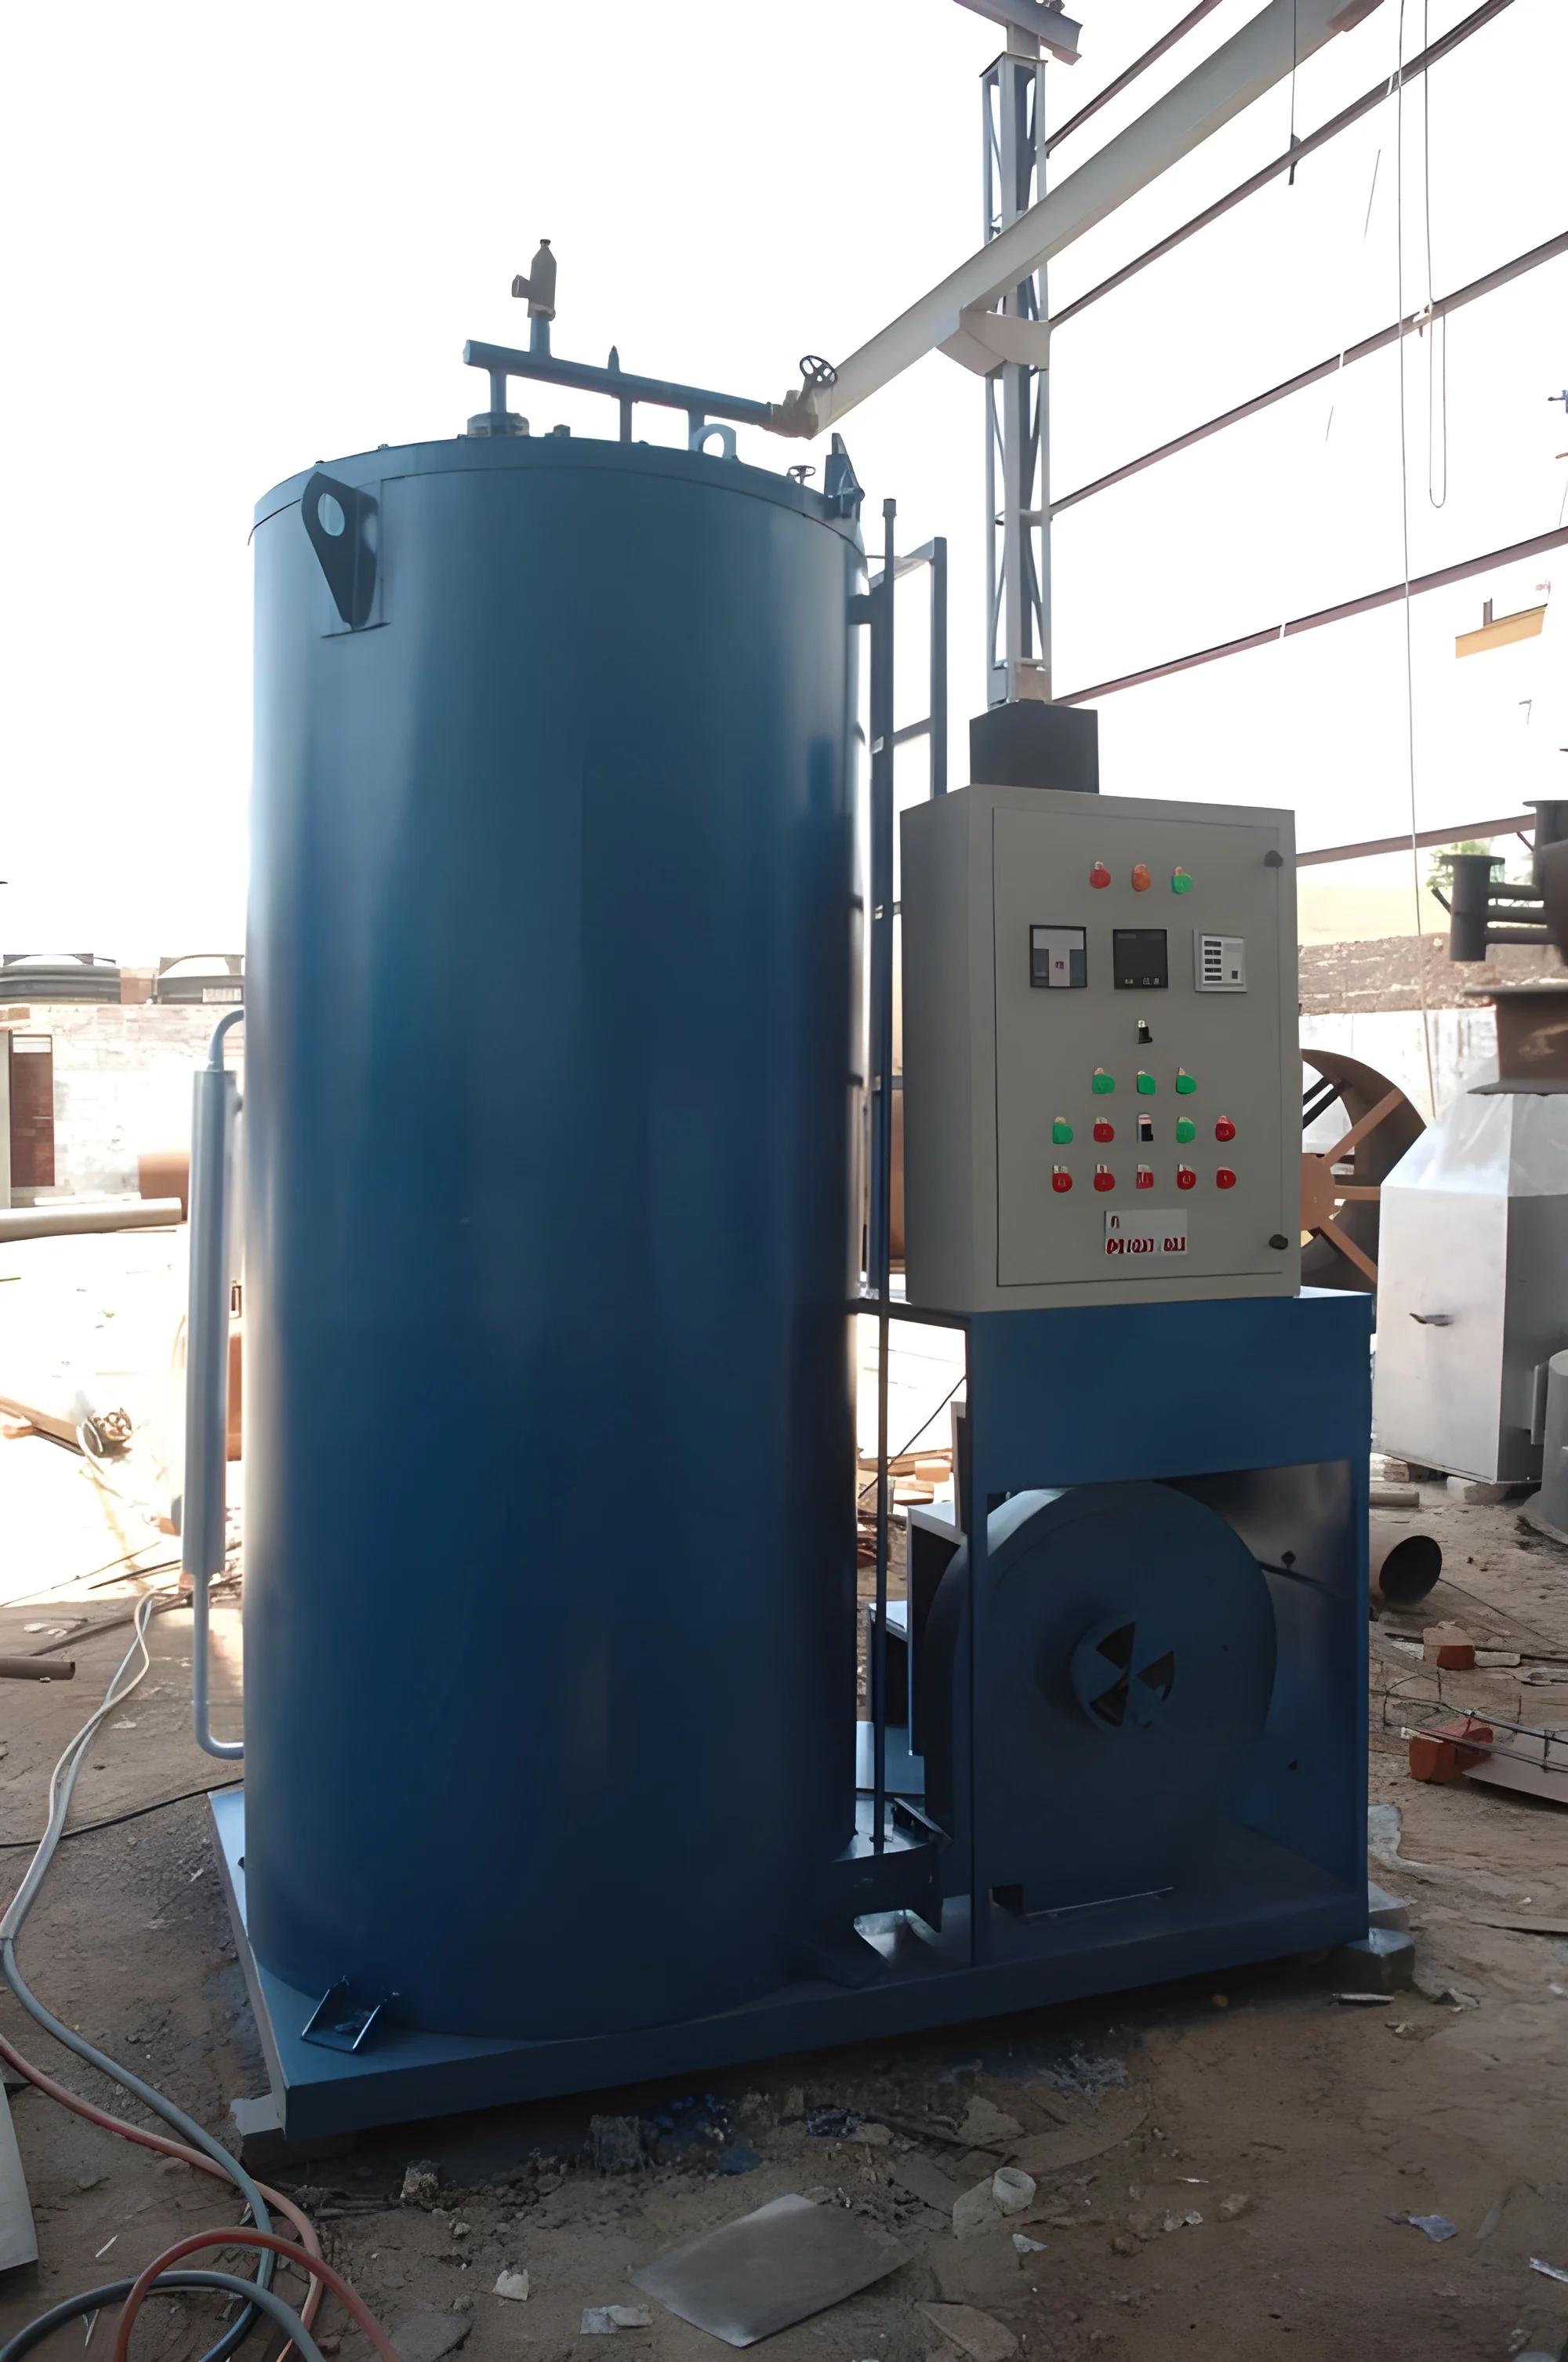
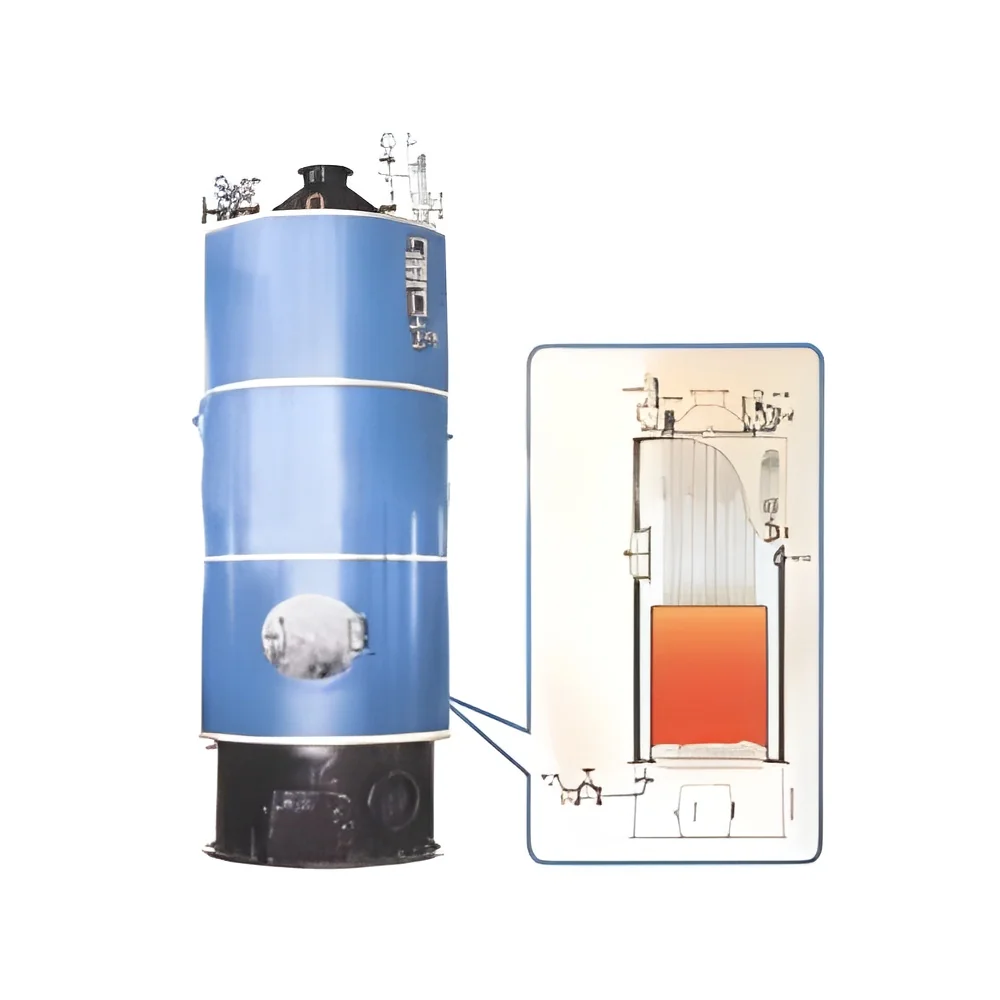
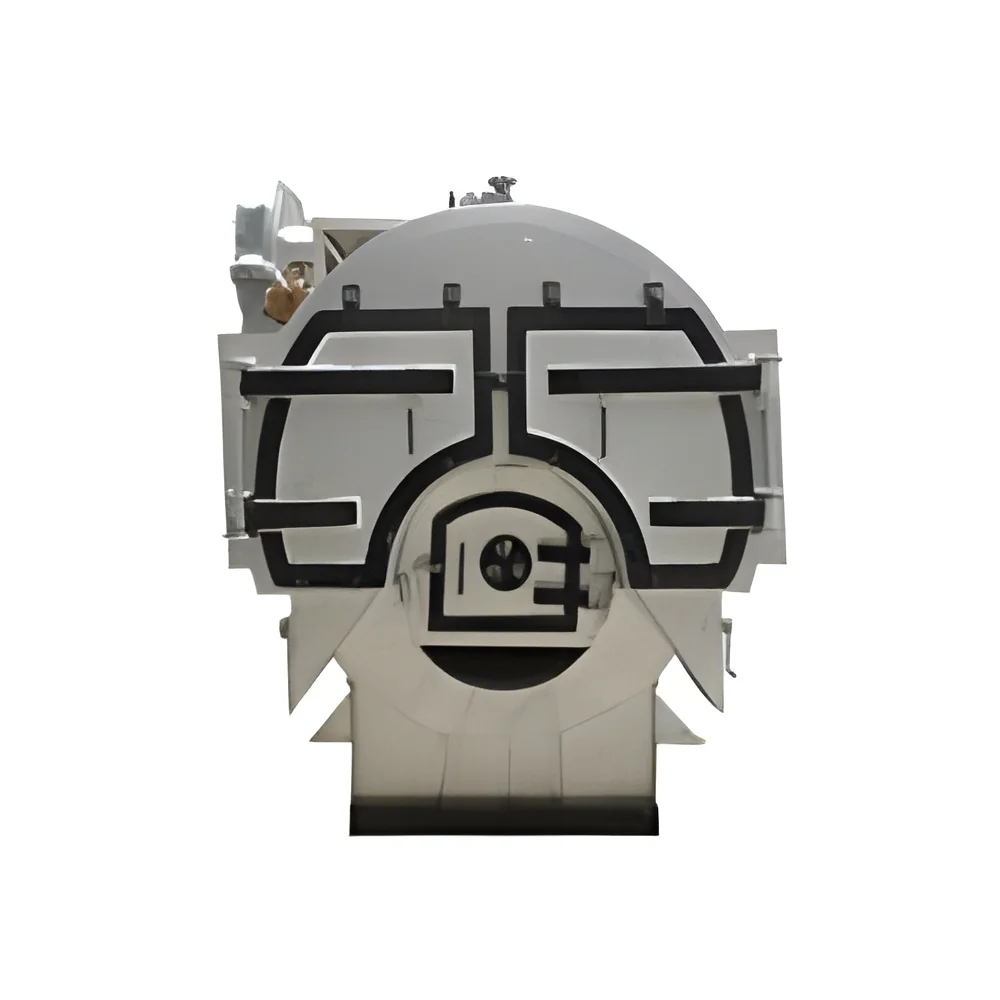
Industrial High Efficiency IBR Steam Boilers represent advanced thermal engineering solutions designed for demanding industrial applications. These boilers are manufactured with premium materials and incorporate sophisticated technology to deliver consistent steam generation while maintaining compliance with Indian Boiler Regulations. The units are engineered for optimal fuel efficiency and reduced maintenance requirements, providing businesses with reliable steam supply for their operational needs. Their construction ensures long-term durability and performance stability even under continuous industrial use conditions.

These steam boilers find extensive application across multiple industrial sectors where thermal energy is critical for production processes. In textile manufacturing, they support dyeing and finishing operations requiring precise temperature control. Food processing facilities utilize them for cooking, pasteurization, and sterilization applications. Chemical plants dep...
Industrial High Efficiency IBR Steam Boilers represent advanced thermal engineering solutions designed for demanding industrial applications. These boilers are manufactured with premium materials and incorporate sophisticated technology to deliver consistent steam generation while maintaining compliance with Indian Boiler Regulations. The units are engineered for optimal fuel efficiency and reduced maintenance requirements, providing businesses with reliable steam supply for their operational needs. Their construction ensures long-term durability and performance stability even under continuous industrial use conditions.

These steam boilers find extensive application across multiple industrial sectors where thermal energy is critical for production processes. In textile manufacturing, they support dyeing and finishing operations requiring precise temperature control. Food processing facilities utilize them for cooking, pasteurization, and sterilization applications. Chemical plants depend on these boilers for reaction heating and distillation, while pharmaceutical manufacturers rely on them for sterile steam requirements in clean room environments and equipment sterilization protocols.

The business value of these IBR Steam Boilers lies in their operational reliability, energy efficiency, and cost-effectiveness over their service life. Their durable construction minimizes downtime and maintenance expenses, while efficient heat transfer surfaces ensure optimal performance. The boilers undergo rigorous quality assurance processes to guarantee consistent operation, making them a trusted choice for industrial clients seeking dependable steam solutions. Their compliance with regulatory standards and robust engineering provide peace of mind for businesses requiring uninterrupted thermal energy for their manufacturing processes.

Key Features:
- Full compliance with Indian Boiler Regulations ensuring safety and standardization
- High-efficiency design for optimal fuel consumption and operational economy
- Premium-grade construction materials providing extended service life
- Advanced heat transfer surfaces for maximum thermal efficiency
- Robust engineering supporting continuous industrial operation

Benefits:
- Reduced operational costs through improved fuel efficiency
- Minimal maintenance requirements lowering total cost of ownership
- Reliable performance ensuring uninterrupted production processes
- Long service life providing excellent return on investment
- Regulatory compliance eliminating safety concerns and certification issues
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Industrial High Efficiency IBR Steam Boilers provide consistent, high-pressure steam essential for various manufacturing processes. Their robust construction and compliance with Indian Boiler Regulations ensure safe operation in demanding industrial environments where reliability and efficiency are paramount for continuous production cycles and thermal operations.
These boilers serve multiple sectors requiring precise steam control and temperature management. From food processing and textile manufacturing to chemical production and pharmaceutical applications, they deliver the thermal energy needed for heating, sterilization, drying, and mechanical drive functions across diverse industrial settings and facility sizes.
- Textile manufacturing for dyeing, finishing, and fabric treatment processes
- Food processing plants for cooking, sterilization, and packaging operations
- Pharmaceutical facilities for equipment sterilization and clean steam applications
- Chemical plants supporting reaction heating and distillation processes
- Manufacturing units for industrial heating and mechanical power generation
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Heat Max Engineering, Gujarat
 Gujarat, India
Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
South Asia
Industrial High Efficiency IBR Steam Boilers For Manufacturing
Industrial High Efficiency IBR Steam Boilers deliver reliable steam generation for manufacturing and processing industries. These durable boilers feature custom specifications and comply with Indian Boiler Regulations for safe, dependable performance.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Heat Max Engineering
 Gujarat, India
Manufacturer