IN
₹
Apparel & Fashion
Description
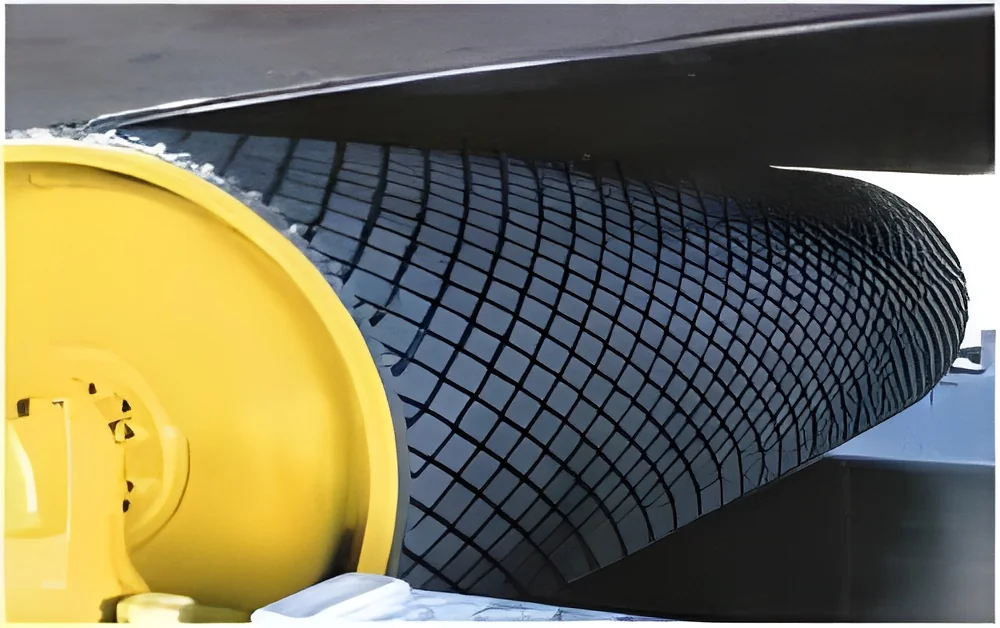
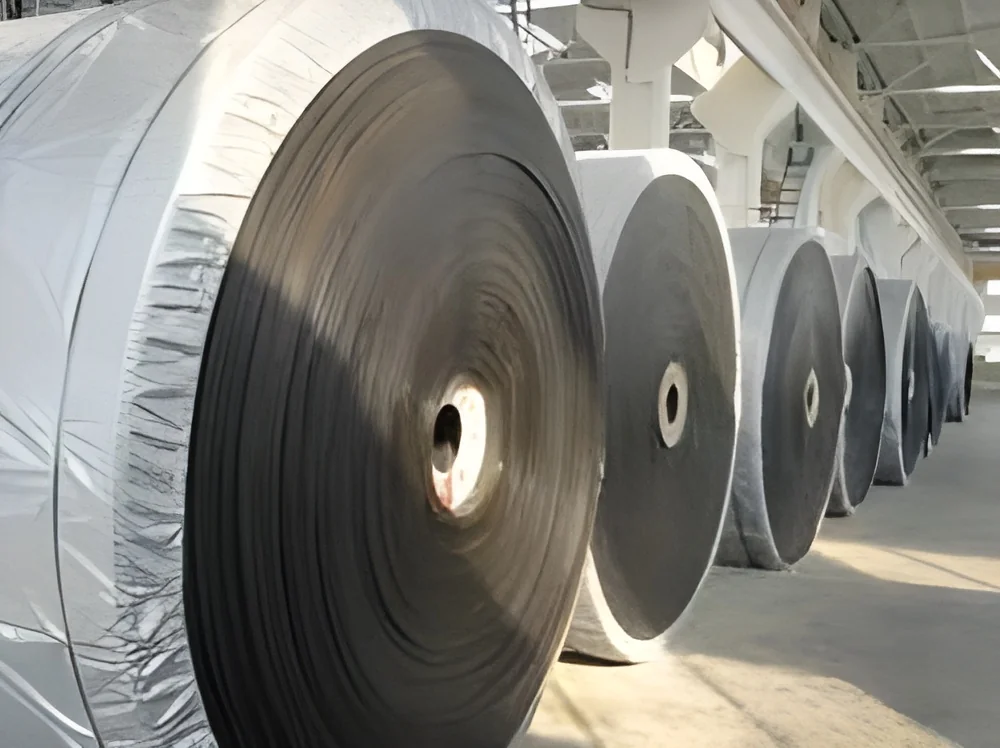
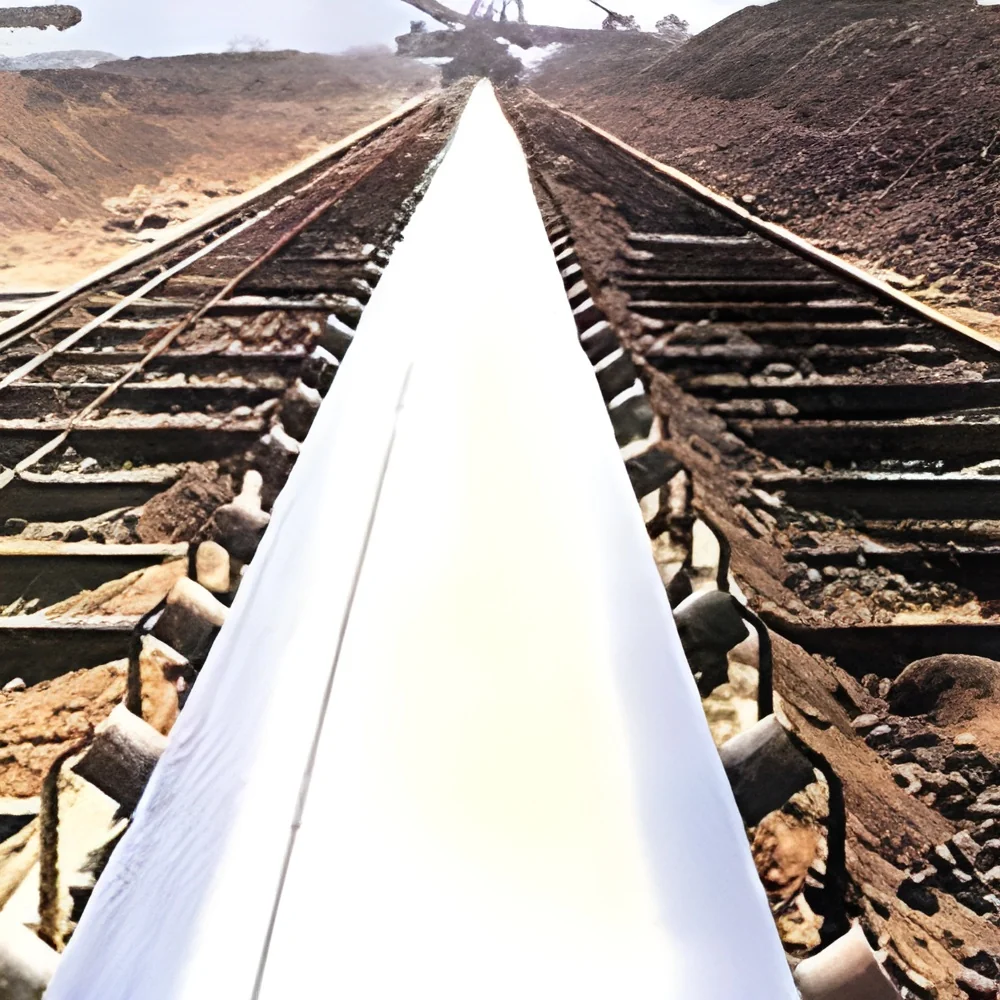
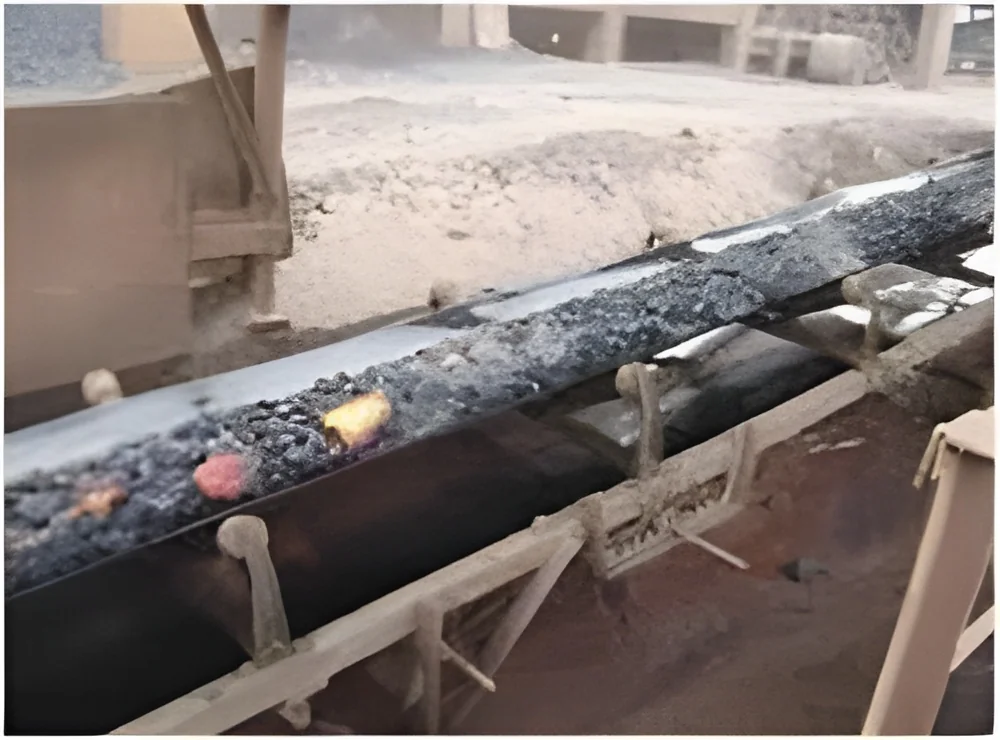
Industrial heat resistant conveyor belts represent advanced material handling solutions engineered specifically for extreme temperature environments. Manufactured using premium materials and sophisticated technologies, these belts maintain structural integrity and operational efficiency even during continuous exposure to high heat conditions. The unique construction incorporates specialized rubber compounds and multiple reinforcement layers that resist thermal degradation, ensuring consistent performance and extended service life. These conveyor belts are precision-engineered to meet international industrial standards, offering superior load-bearing capacity and durability for the most demanding applications across various industrial sectors.

These specialized conveyor belts find essential applications across multiple heavy industries where high-temperature material handling is critical to operations. In cement manufacturing facilities, they efficiently transport hot clinker from rota...
Industrial heat resistant conveyor belts represent advanced material handling solutions engineered specifically for extreme temperature environments. Manufactured using premium materials and sophisticated technologies, these belts maintain structural integrity and operational efficiency even during continuous exposure to high heat conditions. The unique construction incorporates specialized rubber compounds and multiple reinforcement layers that resist thermal degradation, ensuring consistent performance and extended service life. These conveyor belts are precision-engineered to meet international industrial standards, offering superior load-bearing capacity and durability for the most demanding applications across various industrial sectors.

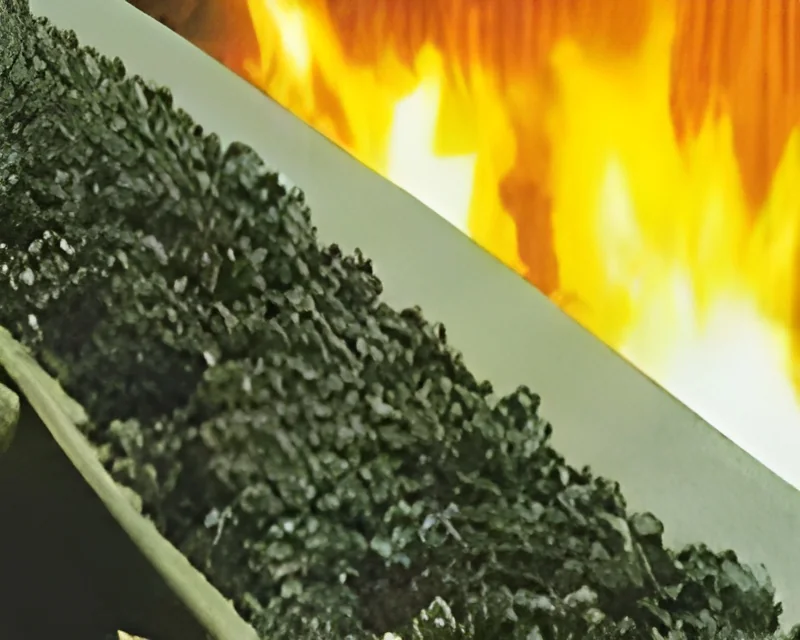
These specialized conveyor belts find essential applications across multiple heavy industries where high-temperature material handling is critical to operations. In cement manufacturing facilities, they efficiently transport hot clinker from rotary kilns to cooling systems without compromising performance. Steel plants utilize them for moving sinter and coke at elevated temperatures throughout production processes, while power generation facilities rely on them for handling hot ashes and slag from combustion systems. The chemical processing industry benefits from their ability to safely convey hot chemical compounds and fertilizers, and metal foundries use them for transferring hot sand and castings during manufacturing operations. Each industry-specific application demands reliable performance under sustained thermal stress, which these belts deliver consistently.

The business value of industrial heat resistant conveyor belts extends beyond technical specifications to encompass operational reliability and significant cost efficiency. By minimizing downtime caused by belt failures in high-temperature environments, these belts substantially reduce maintenance costs while increasing overall productivity. Their exceptional durability translates to longer replacement intervals, providing substantial long-term savings through reduced frequency of belt changes. The quality assurance guarantees consistent performance under demanding conditions, while the reliable construction ensures smooth material flow in critical processes. This combination of reliability and efficiency makes them a strategic investment for businesses seeking to optimize their material handling operations in challenging industrial conditions.

Key Features:
- Engineered with specialized heat-resistant rubber compounds for superior thermal stability
- Reinforced with high-tensile strength fabric or steel cord construction for exceptional durability
- Designed to withstand continuous exposure to temperatures up to 180 degrees Celsius
- Precision manufacturing according to international quality standards for consistent performance
- Multiple reinforcement layers that resist thermal degradation and mechanical abrasion

Benefits:
- Extended service life through superior heat resistance and durable construction
- Reduced maintenance costs and minimized operational downtime in high-temperature environments
- Enhanced productivity through reliable performance in demanding industrial applications
- Long-term cost savings through reduced frequency of belt replacements and repairs
- Consistent material handling efficiency even under sustained thermal stress conditions
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our heat resistant conveyor belts are specifically engineered to maintain structural integrity and performance in extreme temperature conditions. These industrial-grade belts prevent premature wear and ensure continuous operation while handling hot materials, making them ideal for applications where standard belts would fail. The specialized construction combines heat-resistant rubber compounds with reinforced layers to withstand both thermal stress and mechanical abrasion during material transport.
These conveyor belts serve critical functions across multiple heavy industries by enabling safe and efficient transport of high-temperature materials. They are designed to handle demanding applications involving sinter, coke, clinker, and other hot products while maintaining consistent performance. The reliable construction ensures minimal downtime and extended service life, providing dependable operation in the most challenging industrial environments.
- Transporting hot cement clinker from kilns to cooling systems in cement manufacturing
- Moving sintered materials and coke through steel production and metal processing facilities
- Handling hot ashes and slag in power generation plants and waste incineration operations
- Conveying hot fertilizers and chemical compounds in agricultural and chemical processing
- Transferring hot foundry sand and castings in metal casting and forging operations
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile

Belting Enterprises, Madhya Pradesh
 Madhya Pradesh, India
Construction•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
South Asia
Industrial Heat Resistant Conveyor Belts For High Temperature Applications
Industrial heat resistant conveyor belts engineered for high-temperature applications up to 180°C, delivering superior durability and reliable performance in cement, steel, and power industries with exceptional load capacity.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Belting Enterprises
 Madhya Pradesh, India
ConstructionManufacturer