IN
₹
Apparel & Fashion
Description
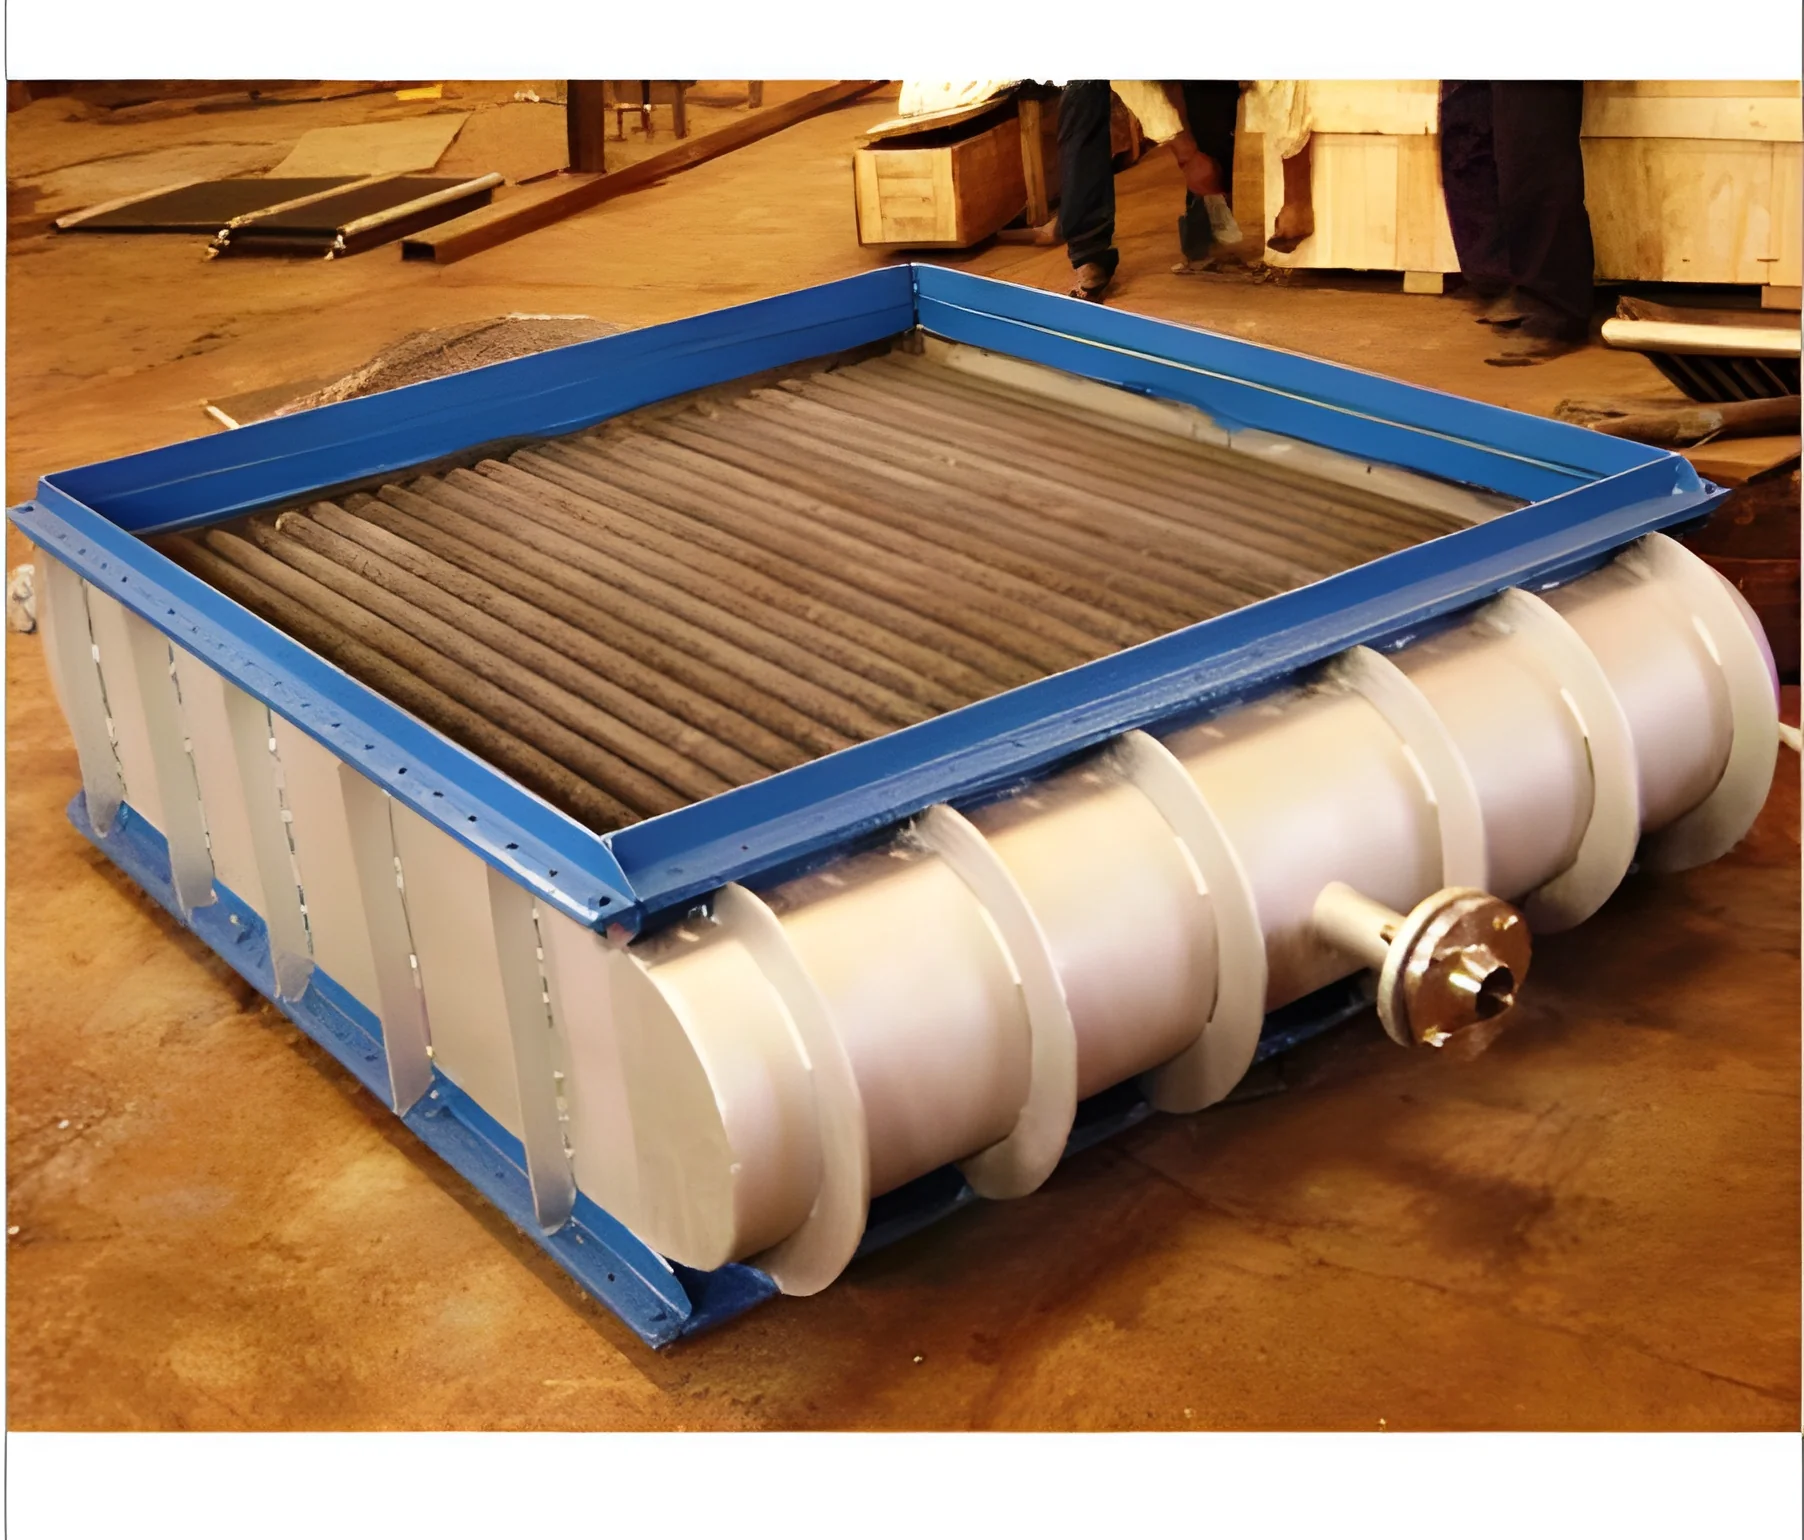
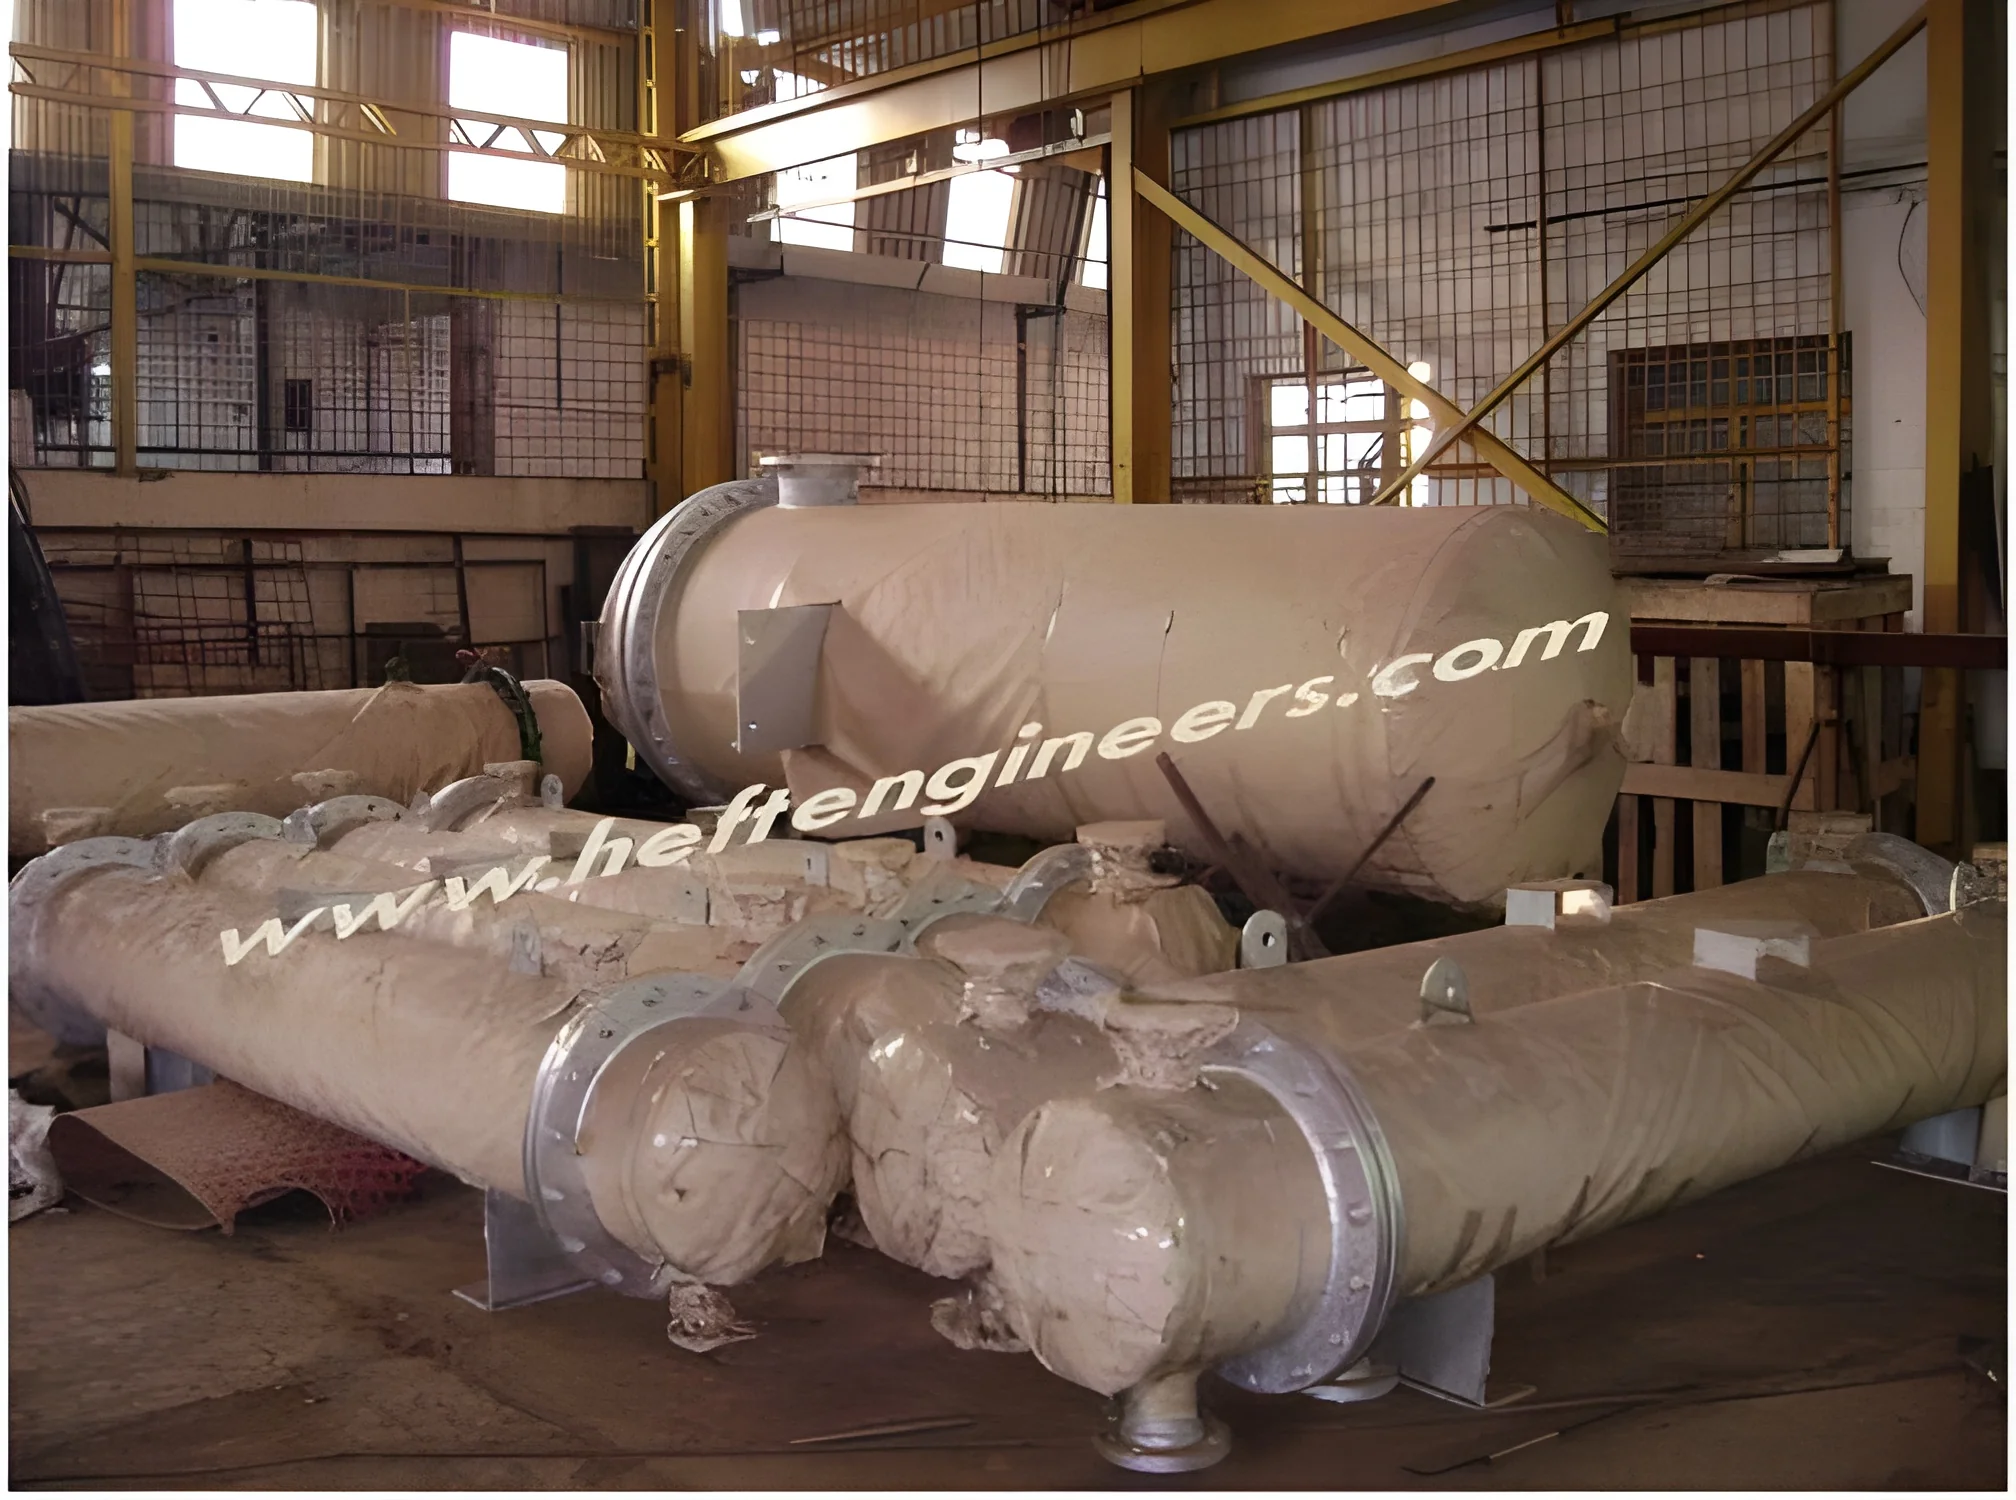
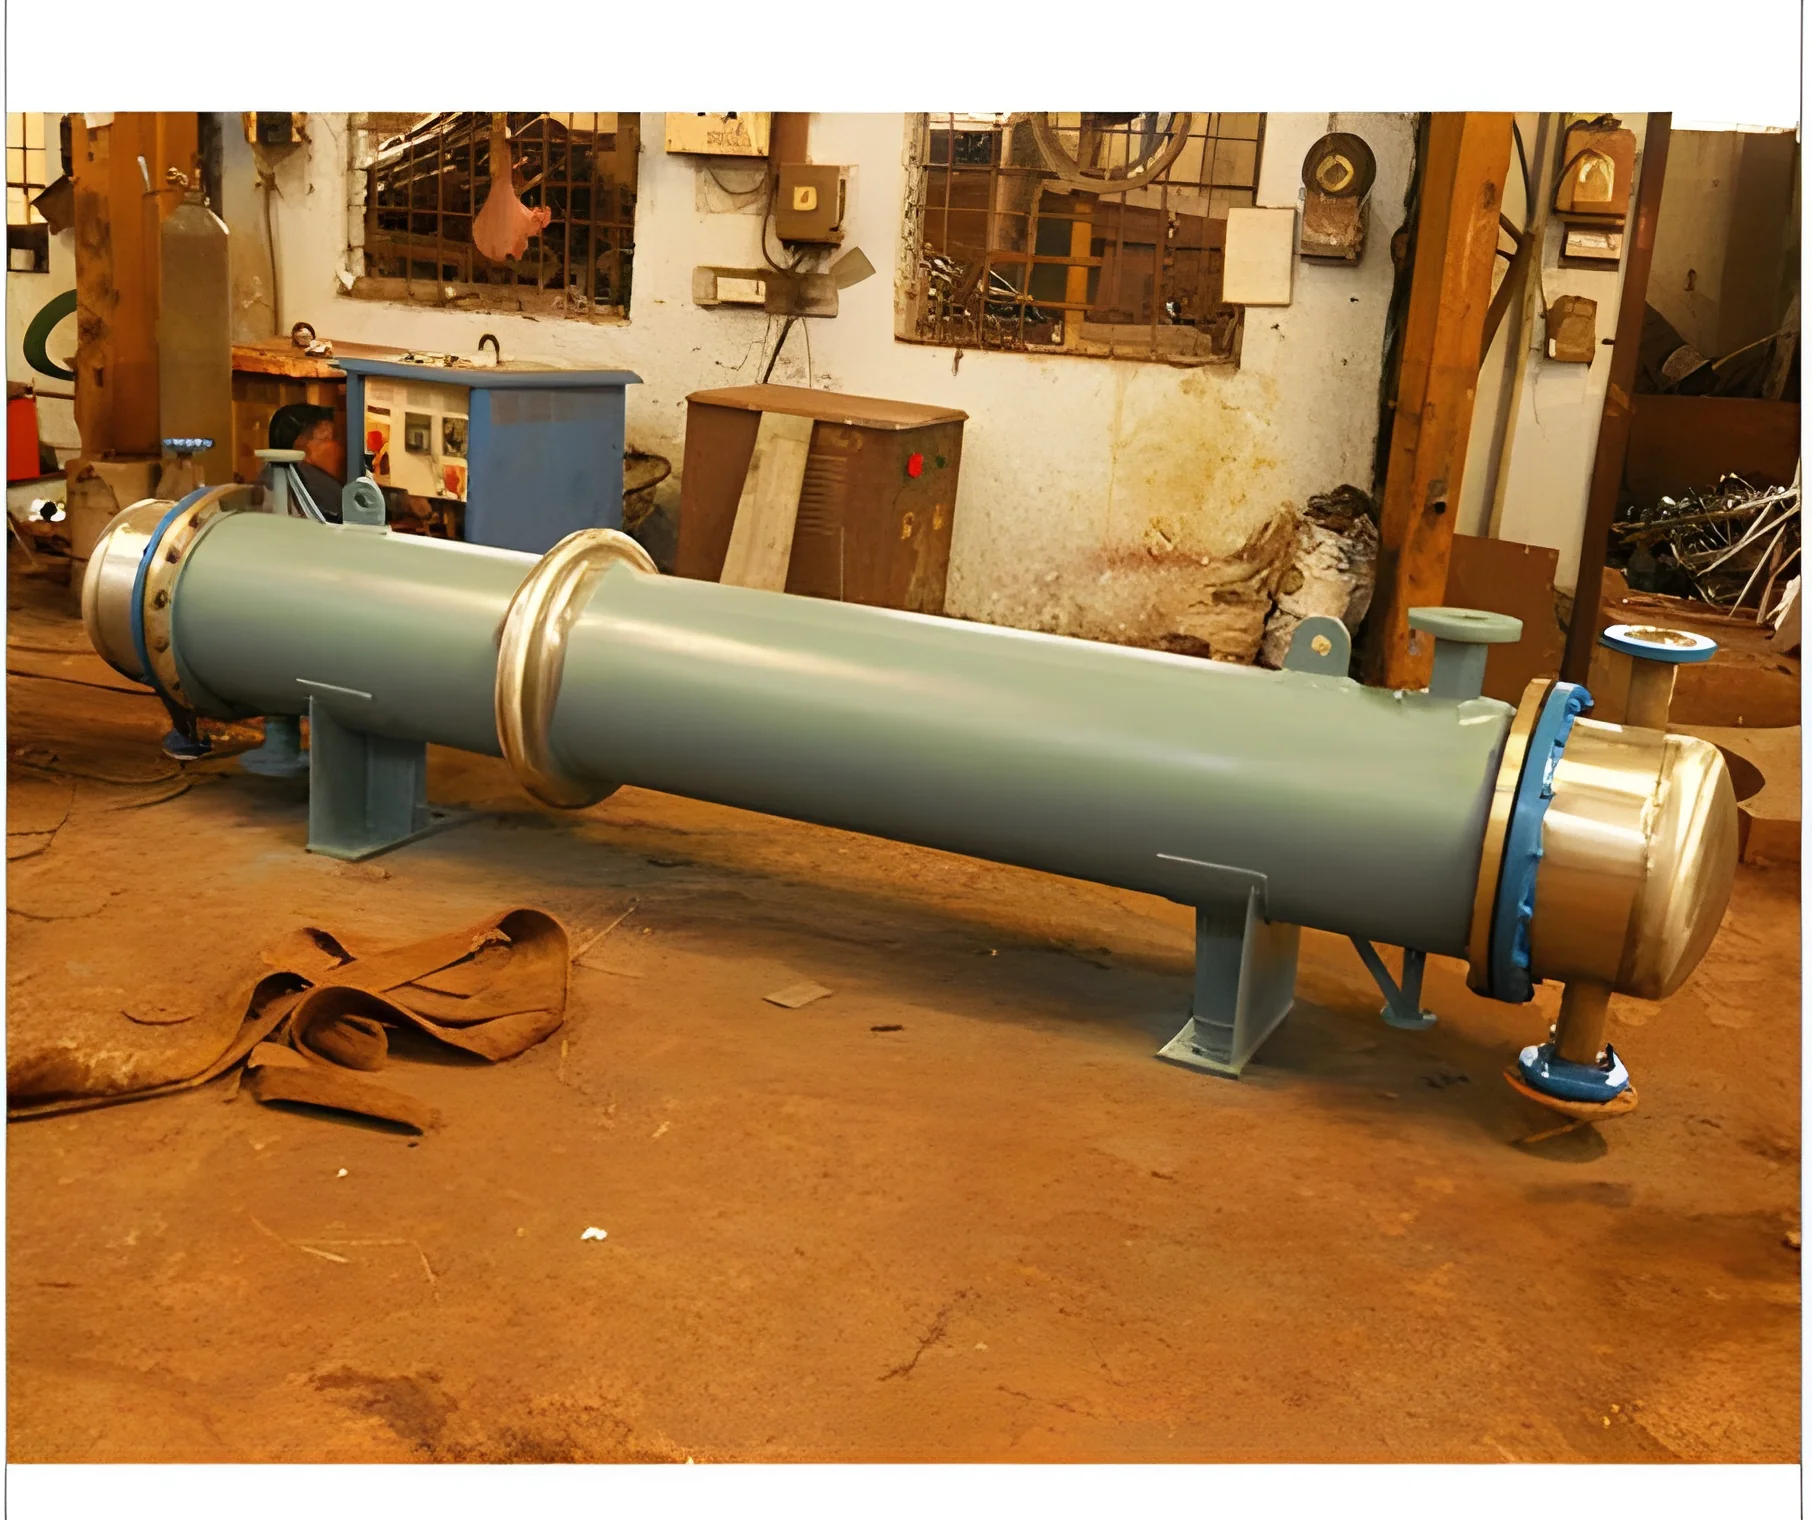
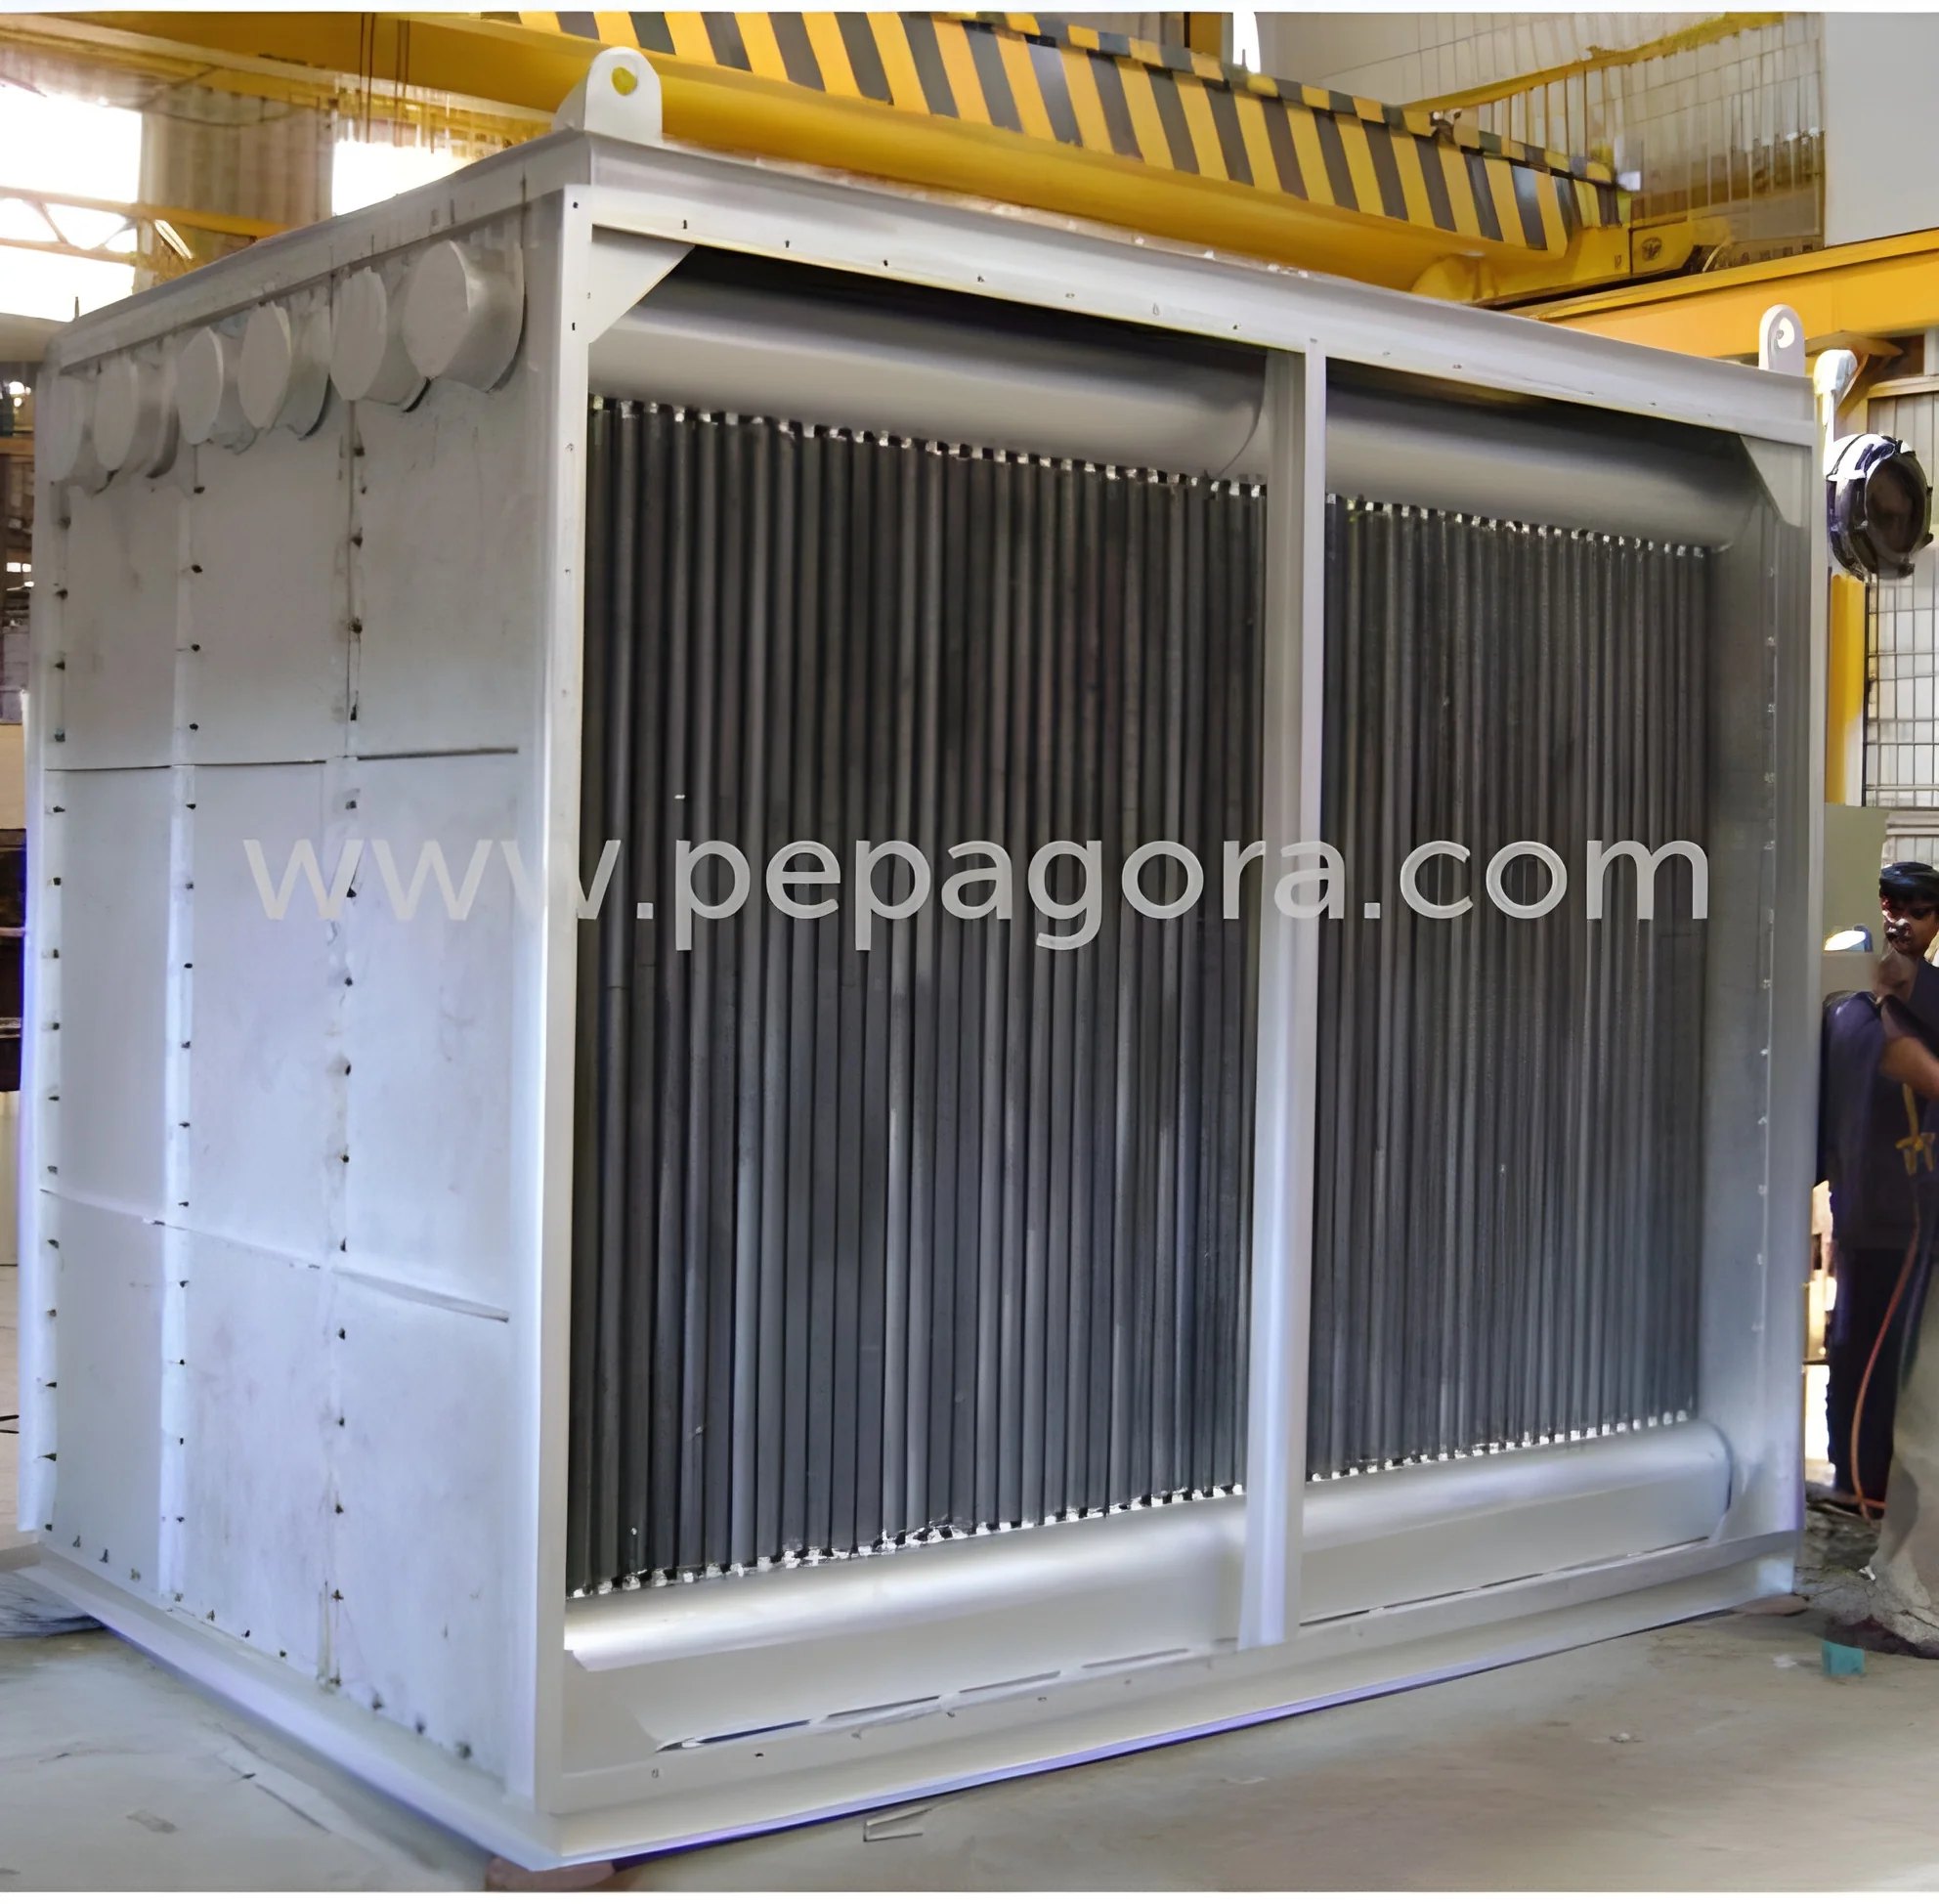
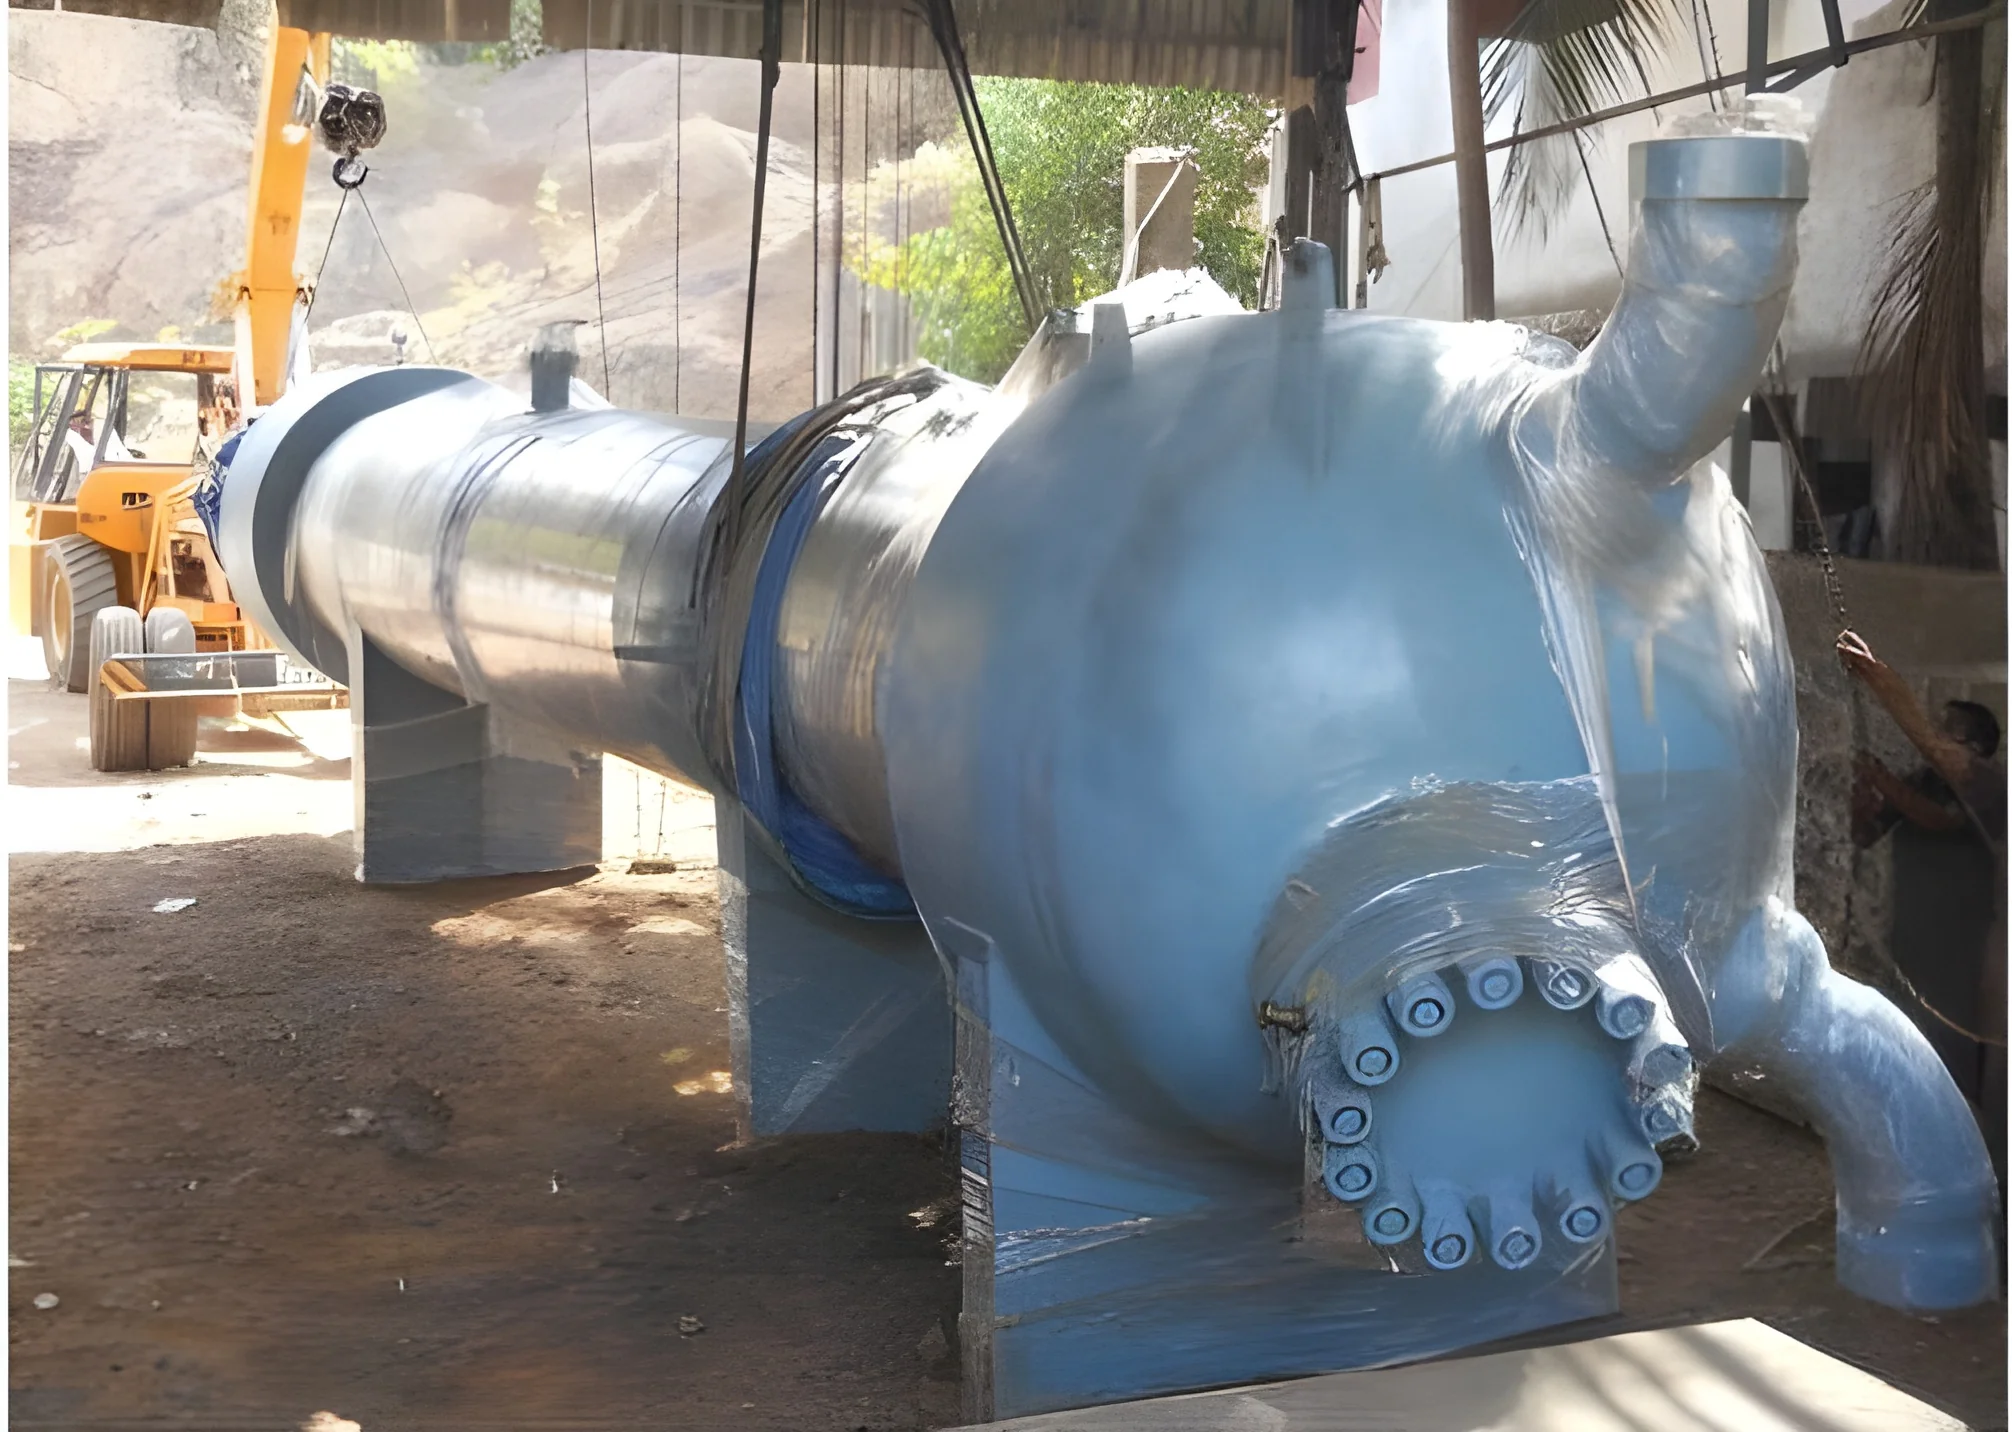
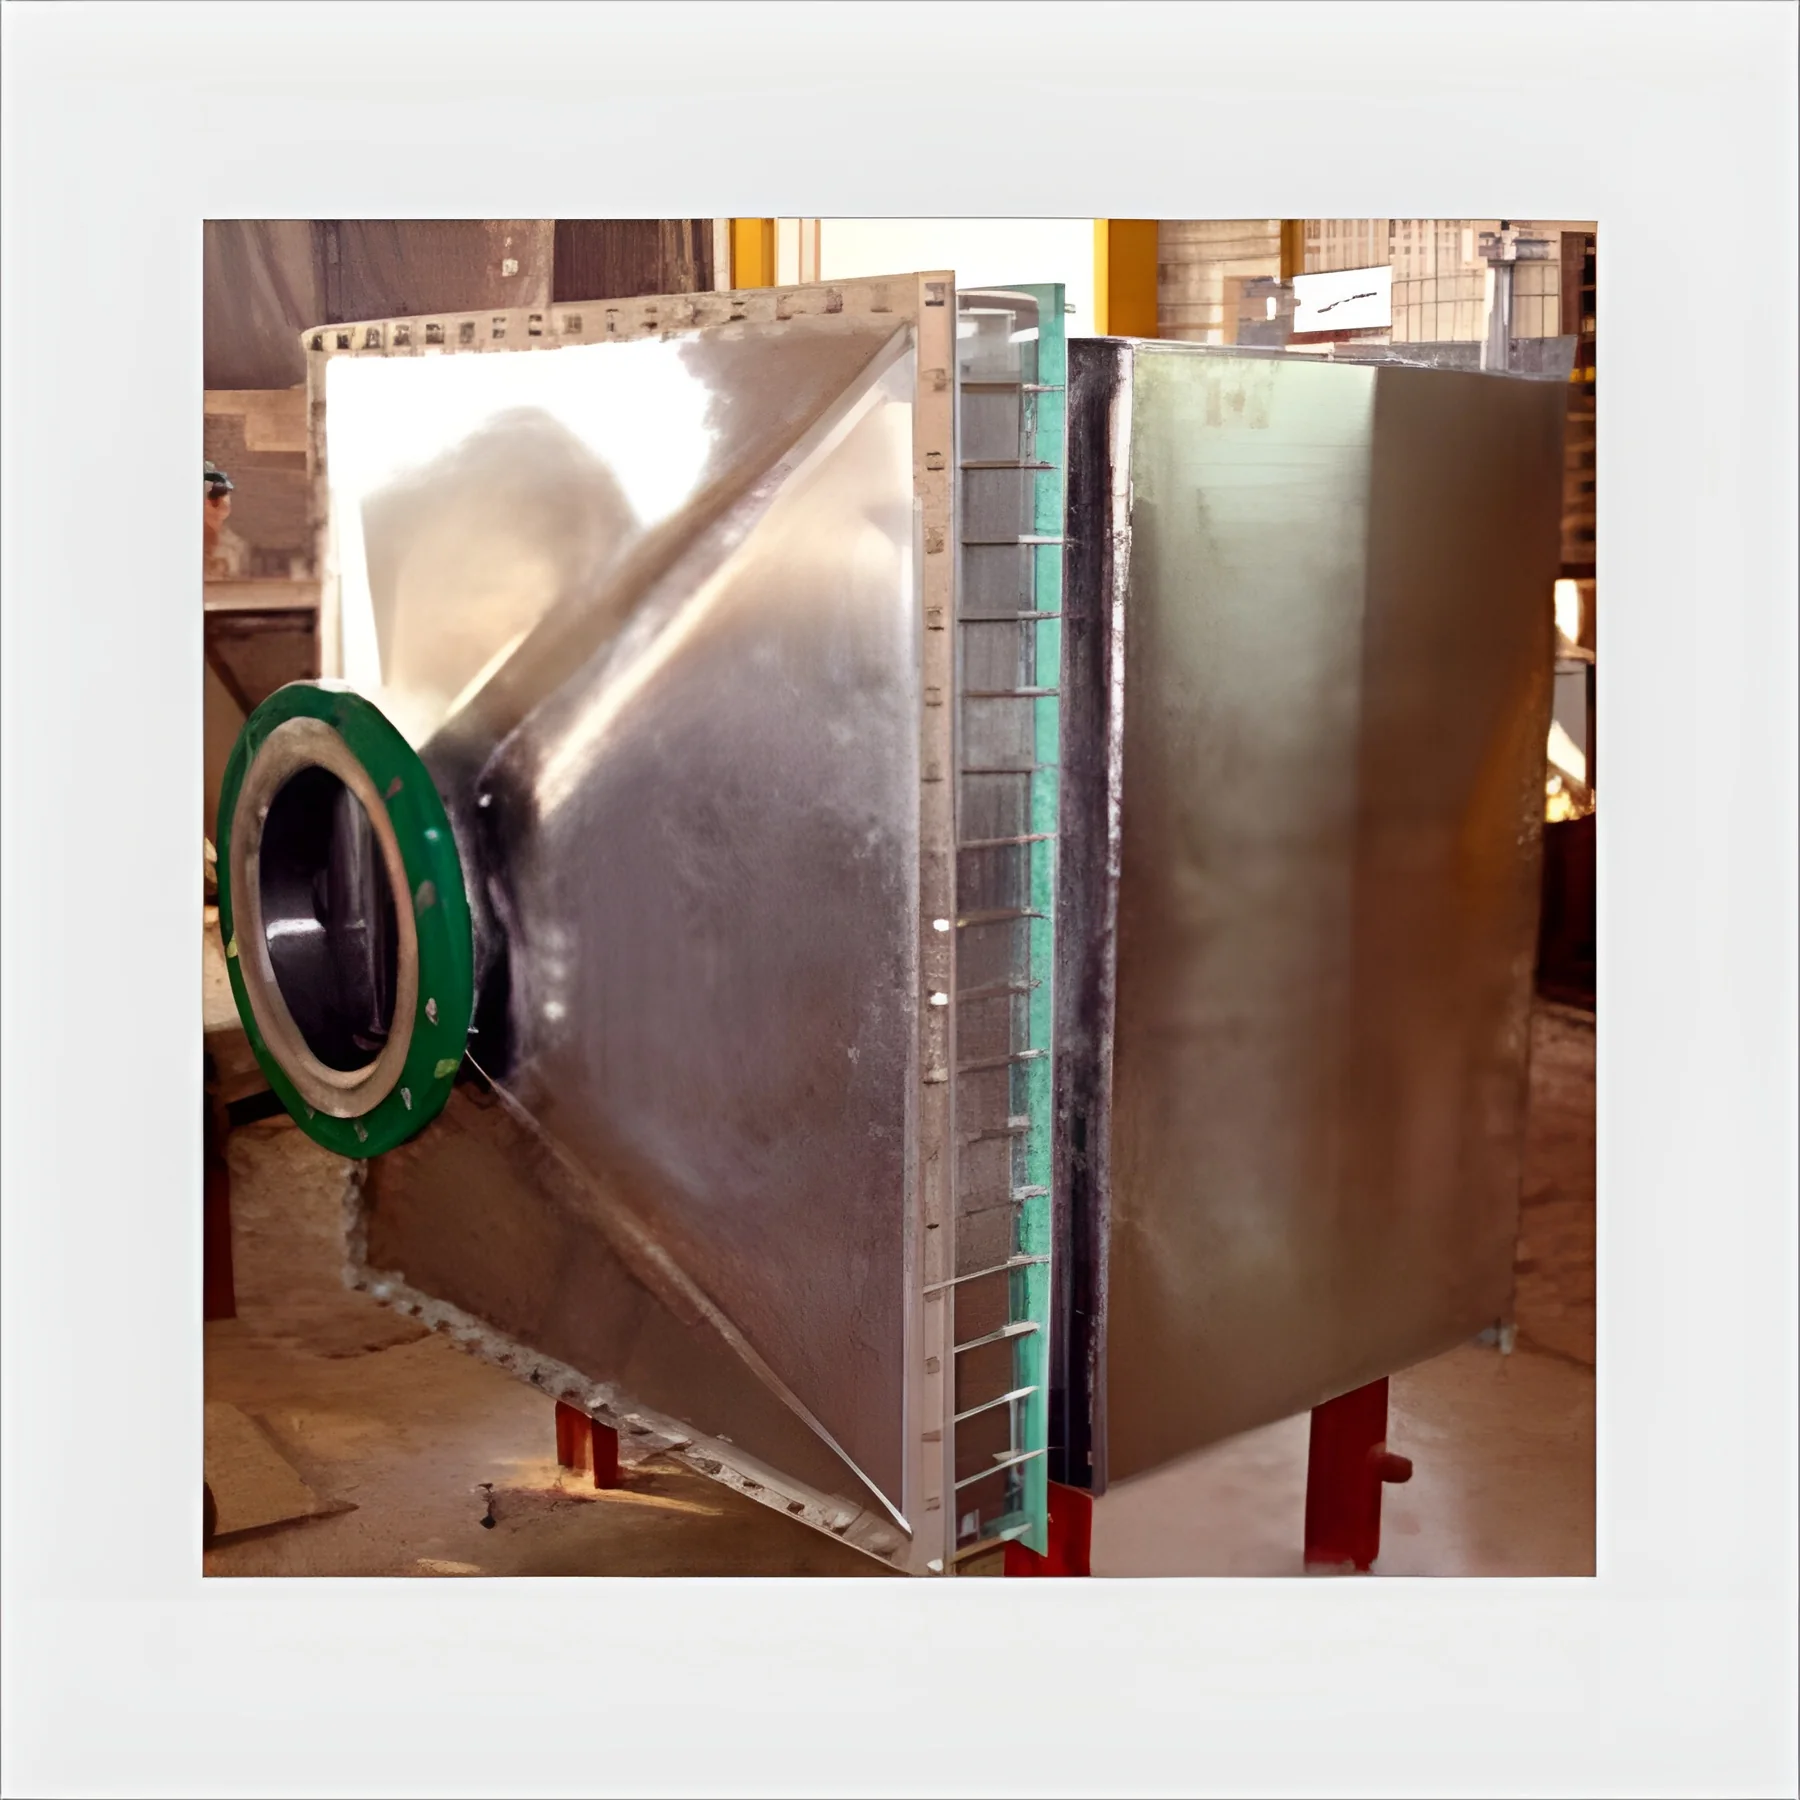
Our industrial air cooled heat exchangers represent engineering excellence in thermal management solutions, specifically designed for applications requiring reliable and efficient heat transfer. Manufactured using proprietary finned tube technology, these units deliver superior performance through increased surface area per square foot while maintaining lower air resistance characteristics. This innovative design ensures optimal heat exchange efficiency while reducing the power required to deliver necessary CFM ratings, making them significantly more effective than conventional alternatives. The lightweight construction and reduced tube count for given BTU transfer rates contribute to overall system efficiency and operational cost savings, providing immediate value to industrial operations.

These heat exchangers find extensive application across multiple industrial sectors where precise temperature control and thermal management are critical to operational success. The chemical proces...
Our industrial air cooled heat exchangers represent engineering excellence in thermal management solutions, specifically designed for applications requiring reliable and efficient heat transfer. Manufactured using proprietary finned tube technology, these units deliver superior performance through increased surface area per square foot while maintaining lower air resistance characteristics. This innovative design ensures optimal heat exchange efficiency while reducing the power required to deliver necessary CFM ratings, making them significantly more effective than conventional alternatives. The lightweight construction and reduced tube count for given BTU transfer rates contribute to overall system efficiency and operational cost savings, providing immediate value to industrial operations.

These heat exchangers find extensive application across multiple industrial sectors where precise temperature control and thermal management are critical to operational success. The chemical processing industry utilizes them for reactor cooling, condenser systems, and process fluid temperature regulation. Power generation facilities deploy these units for turbine oil cooling, transformer cooling, and auxiliary system temperature management. Manufacturing plants integrate them into production machinery cooling systems and process temperature control applications. HVAC systems benefit from their compact design and high efficiency in commercial and industrial climate control applications. The oil and gas sector employs these heat exchangers for compressor cooling, natural gas processing, and various upstream and downstream applications requiring reliable thermal management.

The business value proposition centers on delivering exceptional reliability, operational efficiency, and long-term cost savings. These units are engineered for durability and consistent performance under demanding industrial conditions, ensuring minimal downtime and reduced maintenance requirements. The combination of low friction air losses and high air velocity characteristics enables maximum heat transfer capacity within limited space constraints, providing significant advantages in facility layout and equipment placement. The reduced energy consumption directly translates to lower operational costs and improved environmental compliance through decreased carbon footprint. The robust construction ensures long service life and reliable performance across various industrial environments.

Key Features:
- Proprietary finned tube design for superior thermal efficiency
- Reduced energy consumption with optimal heat transfer performance
- Compact design for optimal space utilization in facility layouts
- Durable construction ensuring reliability under demanding conditions
- Lightweight construction with reduced tube count for efficiency

Benefits:
- Lower operational costs through reduced energy consumption
- Minimal maintenance requirements and reduced downtime
- Optimal performance in space-constrained environments
- Consistent thermal management across various industrial applications
- Long service life with reliable operation under demanding conditions
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our industrial air cooled heat exchangers provide exceptional thermal management across diverse processes where efficient heat transfer is critical. The proprietary finned tube design maximizes surface area while minimizing air resistance, making these units perfect for applications with space constraints and energy efficiency requirements. These robust exchangers serve as essential components in systems needing precise temperature control and consistent performance across multiple operational environments.
Built for durability and reliability, these heat exchangers maintain optimal performance under demanding conditions while reducing maintenance needs and operational costs. Their versatile design adapts to specific industrial needs while delivering unmatched thermal efficiency and long-term value. The units ensure compatibility with various process requirements and industry standards for consistent performance.
- Chemical processing plants utilize our heat exchangers for reactor cooling and condenser applications
- Power generation facilities employ them for turbine oil cooling and auxiliary system temperature control
- HVAC systems integrate these units for commercial building climate management and air handling
- Manufacturing plants use them for machinery cooling and process temperature regulation
- Oil and gas installations deploy them for compressor cooling and process fluid temperature management
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Heft Engineers, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
South Asia
Industrial Air Cooled Heat Exchangers For Superior Thermal Efficiency
Industrial air cooled heat exchangers deliver superior thermal efficiency with reduced energy consumption for reliable industrial heat transfer applications across various sectors requiring optimal space utilization.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Heft Engineers
 Maharashtra, India
Industrial Equipment & MachineryImporter / Exporter