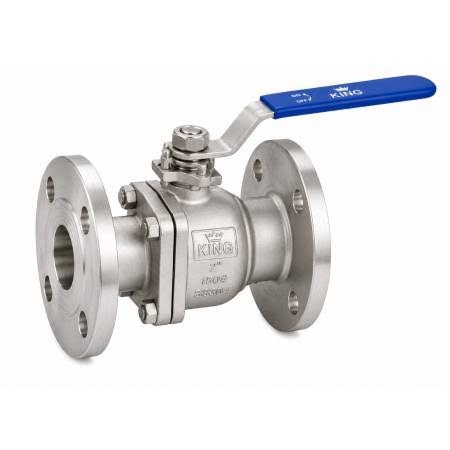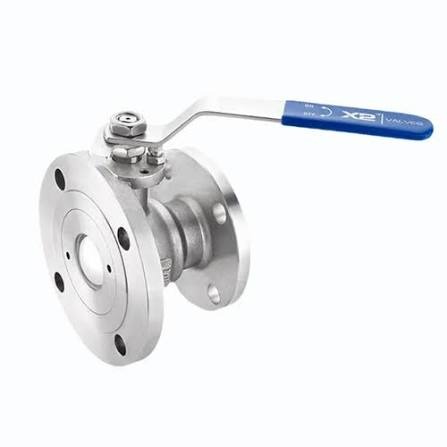
Pharmaceutical synthesis reactors and mixing vessels handling high-purity active pharmaceutical ingredients (APIs), syrups, and liquid excipients.
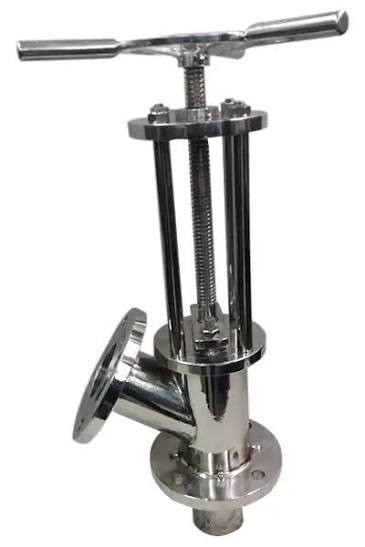
Food and beverage manufacturing plants utilizing sanitary flush valves for dairy products, edible oils, sauces, and beverage concentrates.
Fine chemical and specialty polymer reactors processing reactive slurries, emulsions, and high-viscosity resins.
Cosmetics and personal care formulation tanks handling high-viscosity creams, lotions, and surfactant blends.
Biotech fermentation vessels and sterile media preparation tanks requiring cleanable, zero-dead-leg fluid isolation.