IN
₹
Apparel & Fashion
Description
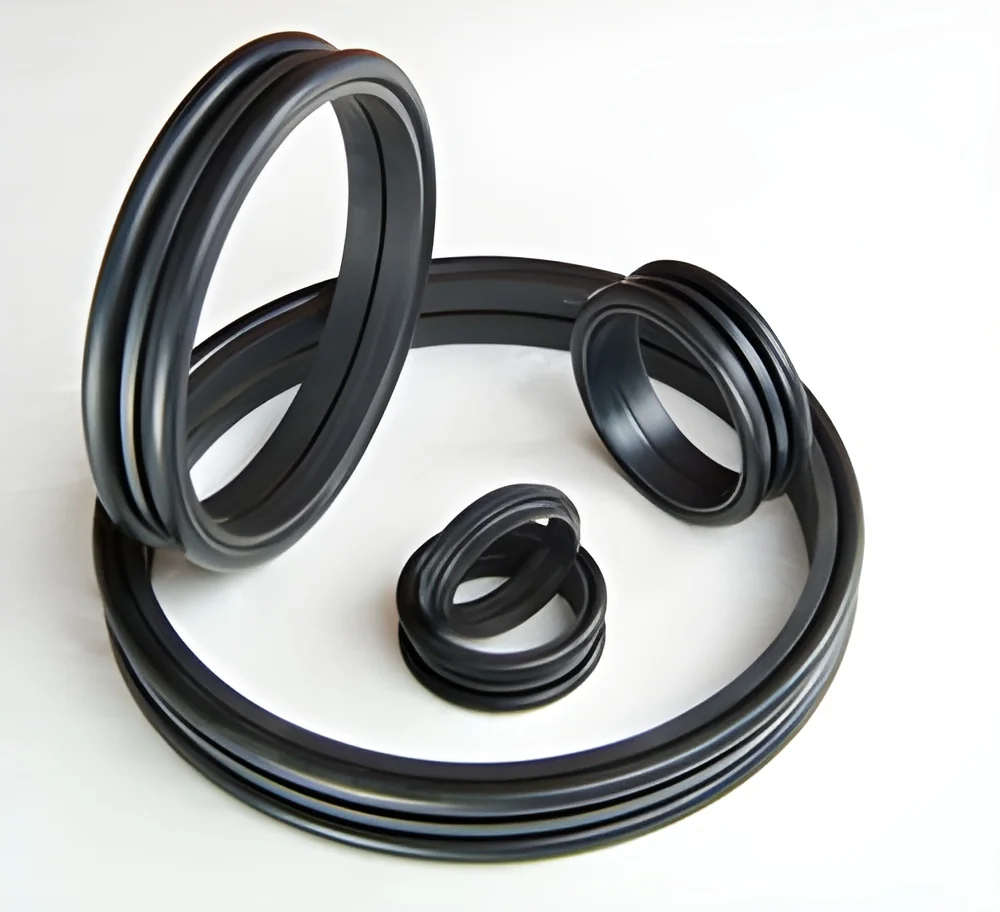
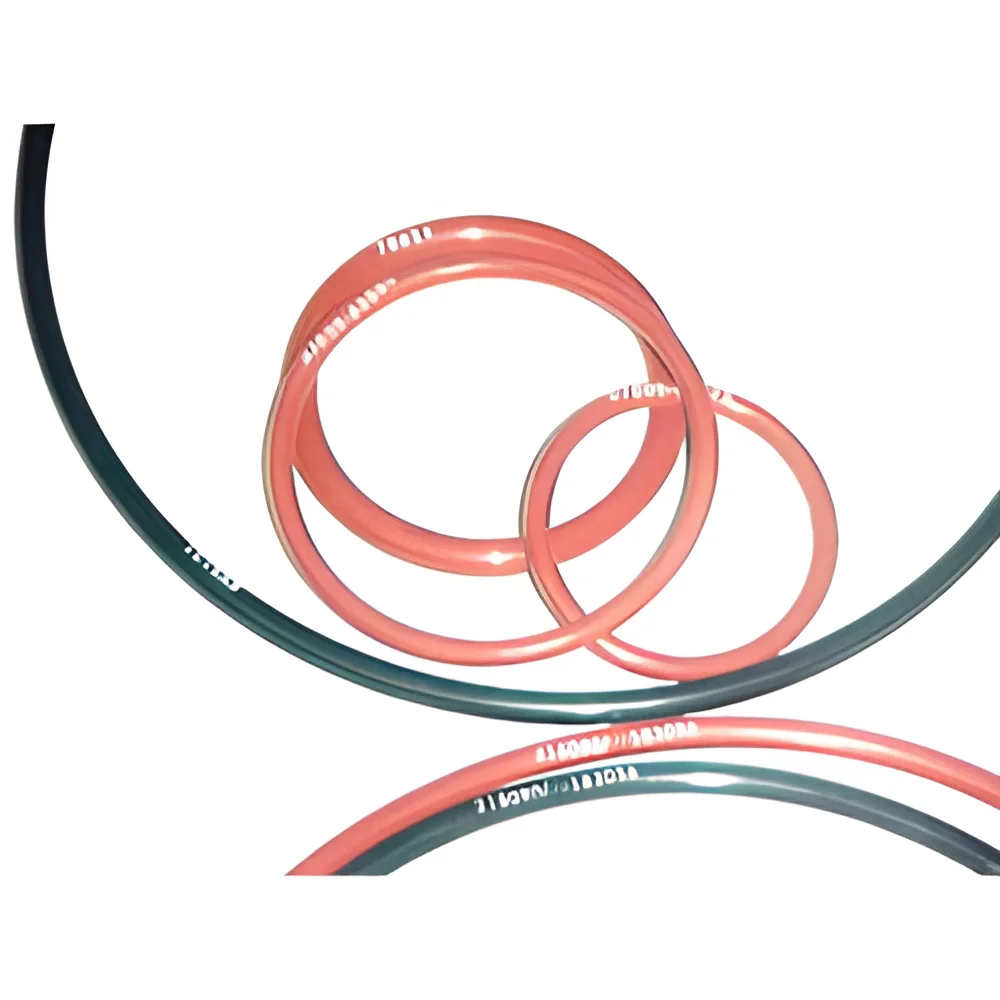
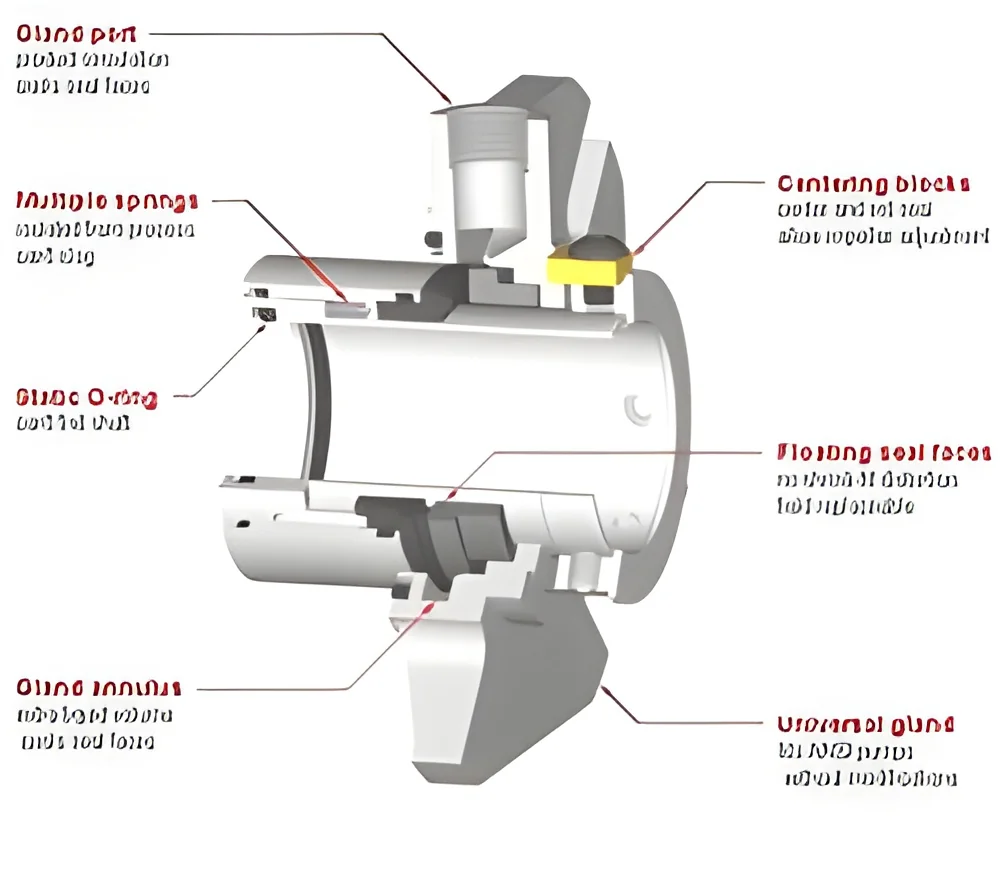
Heavy duty floating seals represent advanced mechanical sealing technology specifically engineered for demanding industrial applications. These precision components consist of two mated metal rings that create an effective seal through axial force, providing superior performance in retaining heavy-duty lubricants while excluding harsh contaminants. Engineered to withstand extreme pressure, shock loads, and significant movement, they outperform traditional sealing solutions in severe-duty scenarios where reliability is paramount. Their robust construction ensures consistent performance in environments filled with dirt, mud, and abrasive materials that would quickly compromise standard seals.

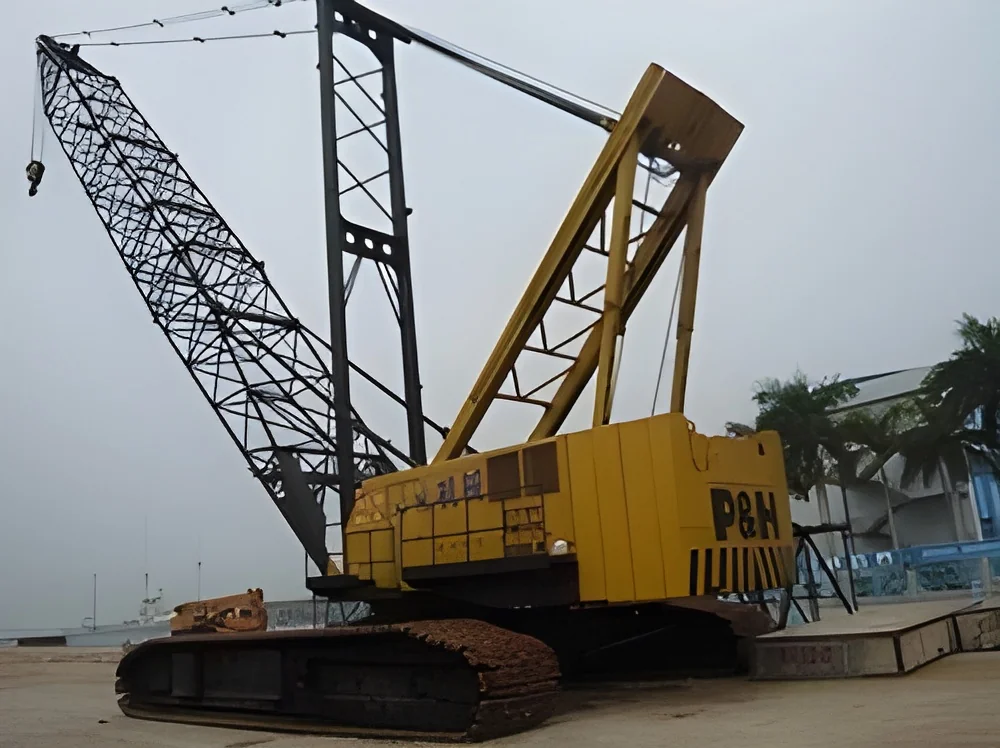
These reliable seals are essential components across multiple industries where equipment operates under challenging conditions. In construction and mining sectors, they protect critical components in bulldozers, excavators, loaders, and compactors. The agricultural industry depends on them for larg...
Heavy duty floating seals represent advanced mechanical sealing technology specifically engineered for demanding industrial applications. These precision components consist of two mated metal rings that create an effective seal through axial force, providing superior performance in retaining heavy-duty lubricants while excluding harsh contaminants. Engineered to withstand extreme pressure, shock loads, and significant movement, they outperform traditional sealing solutions in severe-duty scenarios where reliability is paramount. Their robust construction ensures consistent performance in environments filled with dirt, mud, and abrasive materials that would quickly compromise standard seals.

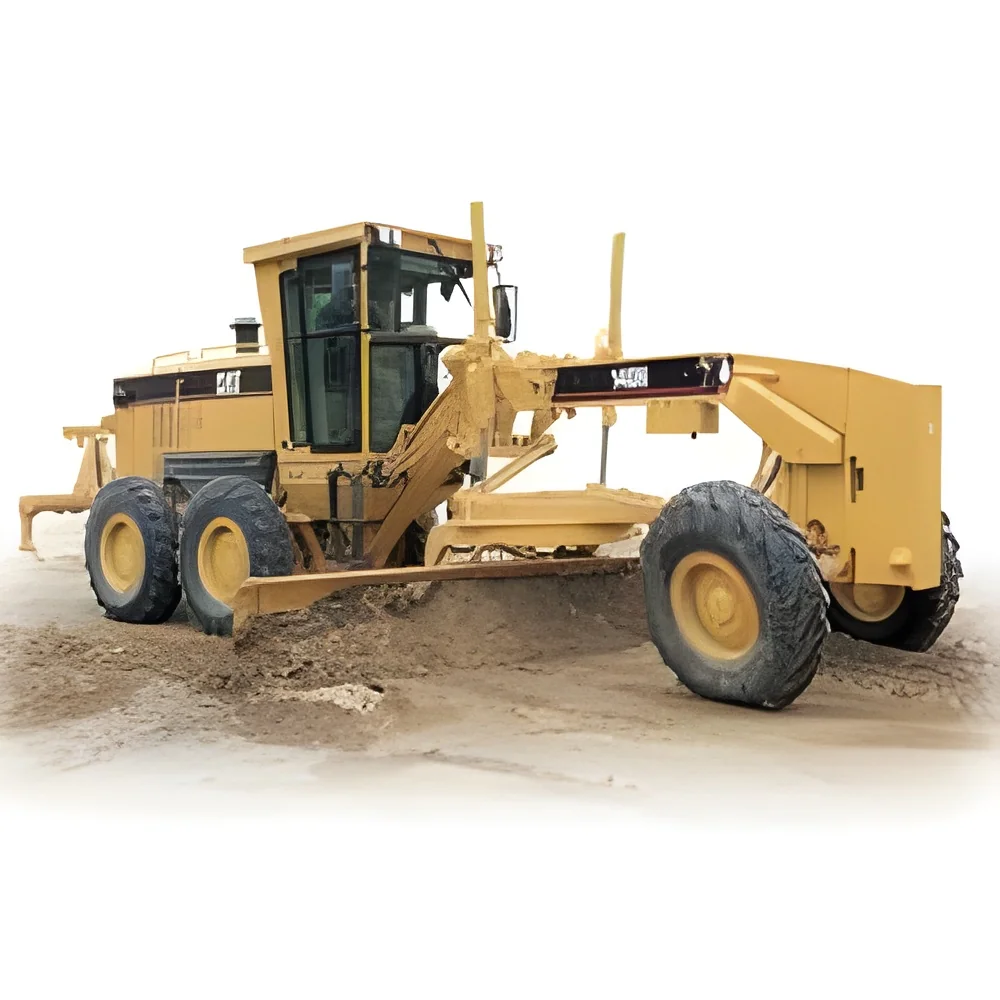
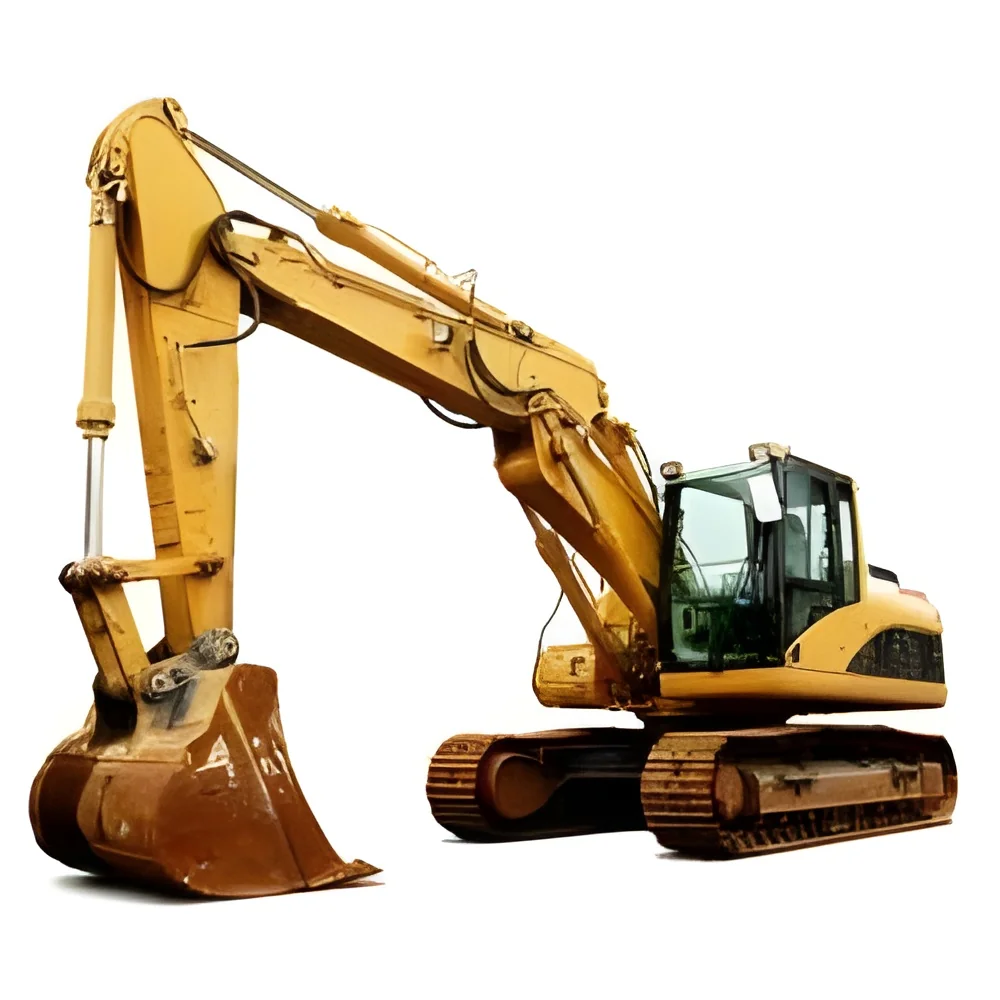
These reliable seals are essential components across multiple industries where equipment operates under challenging conditions. In construction and mining sectors, they protect critical components in bulldozers, excavators, loaders, and compactors. The agricultural industry depends on them for large tractors and harvesting equipment, while material handling operations utilize them in forklifts and industrial stackers. Their proven performance in particulate-filled environments makes them vital for original equipment manufacturers and maintenance operations worldwide, ensuring machinery remains productive despite continuous exposure to extreme working conditions.

For industrial buyers and distributors, heavy duty floating seals deliver significant value through reduced total cost of ownership and enhanced equipment longevity. These components represent a strategic investment in operational reliability, minimizing unplanned downtime and maintenance expenses. Their superior design provides exceptional performance compared to alternative sealing solutions, resulting in fewer replacements and increased machine availability. This reliability translates into predictable equipment performance for end-users, establishing confidence and reinforcing your position as a supplier of high-quality critical components for industrial machinery.

Key Features:
- Manufactured from high-grade wear-resistant materials for maximum durability
- Precision-engineered two-piece metal ring design with mated sealing faces
- Engineered to handle extreme pressure conditions and shock loads
- Optimized for reliable performance in slow-rotation high-load applications
- Built to withstand harsh environments including mud dust and abrasives

Benefits:
- Extended equipment lifespan through superior contaminant exclusion
- Reduced maintenance costs and minimized unplanned downtime
- Consistent performance under extreme pressure and shock conditions
- Enhanced operational reliability in demanding industrial environments
- Improved machinery availability and productivity for end-users
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Heavy duty floating seals provide critical protection for machinery operating under extreme pressure and contamination. Their robust design ensures reliable performance in slow rotation, high load applications where standard seals quickly fail. These seals effectively retain lubricants while excluding harsh contaminants like mud, dust, and abrasive materials, significantly reducing maintenance costs and equipment downtime in demanding industrial environments.
These premium seals serve essential roles across construction, mining, agriculture, and material handling industries. They are the preferred choice for equipment manufacturers and maintenance teams seeking durable, reliable sealing solutions for pivotal rotating assemblies. The seals' ability to perform consistently in the toughest conditions ensures equipment longevity and operational efficiency, making them indispensable components for heavy machinery that faces relentless abuse and challenging working conditions daily.
- Track rollers and final drives in excavators and bulldozers
- Idlers and drive sprockets in construction and mining equipment
- Axles and wheel hubs in agricultural tractors and combines
- Rotating assemblies in material handling forklifts and stackers
- Gearboxes and drivetrains in industrial machinery and off-road vehicles
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Bhailal M. Parikh, Maharashtra
 Maharashtra, India
Industrial Equipment & Machinery•Trading Company•Distributor / Wholesaler•Retailer
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Heavy Duty Floating Seals for Construction and Mining Machinery
Heavy duty floating seals for construction and mining machinery deliver superior sealing in excavators and bulldozers. Engineered to withstand extreme pressure, shock loads, and harsh environments for reliable performance.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Bhailal M. Parikh
 Maharashtra, India
Industrial Equipment & MachineryTrading Company