IN
₹
Apparel & Fashion

Description
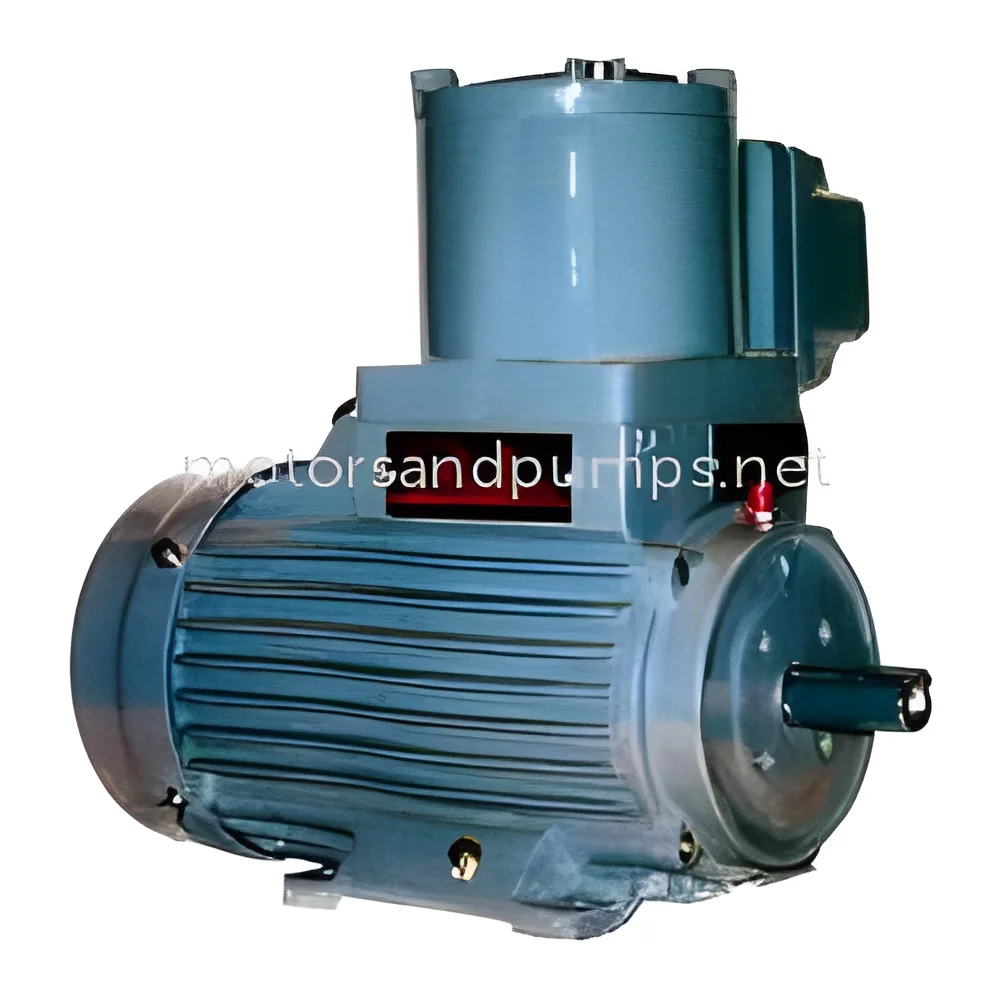
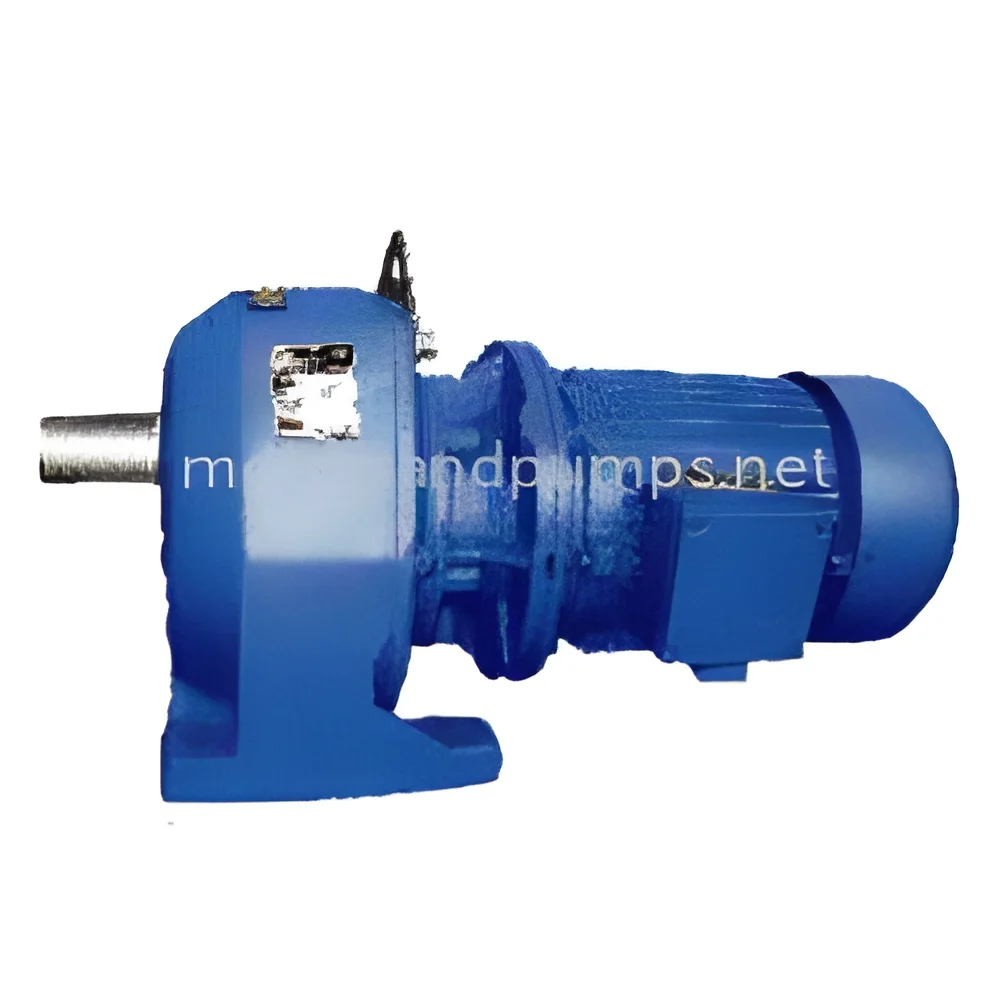
Flame proof motors represent the highest standard of safety engineering for industrial applications in hazardous environments. These explosion-proof motors are specifically designed to operate where flammable gases, vapors, or combustible dust may be present, preventing ignition of surrounding explosive atmospheres. Through specially engineered enclosures that contain any internal explosion, these motors ensure potential ignition sources cannot trigger catastrophic events. Manufactured to comply with international safety standards including ATEX and IECEx, they provide reliable performance in demanding conditions while maintaining operational efficiency and durability.

The application of flame proof motors spans numerous high-risk industries where safety cannot be compromised. In oil and gas operations, they power essential equipment from extraction through refining processes. Chemical processing plants utilize these motors for mixing, pumping, and handling volatile substances. Mining...
Flame proof motors represent the highest standard of safety engineering for industrial applications in hazardous environments. These explosion-proof motors are specifically designed to operate where flammable gases, vapors, or combustible dust may be present, preventing ignition of surrounding explosive atmospheres. Through specially engineered enclosures that contain any internal explosion, these motors ensure potential ignition sources cannot trigger catastrophic events. Manufactured to comply with international safety standards including ATEX and IECEx, they provide reliable performance in demanding conditions while maintaining operational efficiency and durability.

The application of flame proof motors spans numerous high-risk industries where safety cannot be compromised. In oil and gas operations, they power essential equipment from extraction through refining processes. Chemical processing plants utilize these motors for mixing, pumping, and handling volatile substances. Mining operations depend on them for ventilation, conveyance, and processing equipment where combustible dust presents constant danger. Pharmaceutical manufacturers employ them in solvent handling areas, while wastewater treatment facilities rely on their safety features in potentially explosive environments containing methane and other gases.

These motors deliver exceptional business value through enhanced safety protocols, significantly reduced maintenance requirements, and extended service life. They help organizations minimize operational risks while maximizing productivity and uptime in critical applications. The investment in flame proof motors translates to reduced insurance premiums, compliance with stringent regulations, and protection of valuable assets and human resources. Their energy-efficient performance also contributes to lower operational costs over time, making them both a safety necessity and a smart financial decision for businesses operating in hazardous environments.

Key Features:
- Explosion-proof enclosure certified for hazardous area operations
- Corrosion-resistant construction using durable materials for longevity
- Advanced cooling system design for continuous operation capability
- Customizable specifications including mounting styles and protection degrees
- Full compliance with international safety standards ATEX and IECEx

Benefits:
- Enhanced operational safety in explosive environments
- Reduced maintenance requirements and extended service life
- Compliance with international safety standards and regulations
- Energy-efficient performance lowering operational costs
- Protection of personnel and critical infrastructure assets
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Flame proof motors are engineered for industries where flammable gases, vapors, or combustible dust create explosion hazards. These motors prevent ignition sources, ensuring operational safety and reliability in extreme conditions. They meet rigorous international certifications like ATEX and IECEx, providing robust performance where standard motors would fail, protecting both personnel and critical infrastructure from potential disasters.
These durable motors are essential across multiple high-risk sectors, maintaining efficiency while reducing downtime and ensuring regulatory compliance. Their design adapts to specific application needs, delivering optimal performance in diverse industrial processes. Businesses rely on them for continuous operation in challenging environments, prioritizing safety and productivity in equal measure.
- Oil and gas refineries for pumps, compressors, and drilling rigs
- Chemical plants for mixers, agitators, and reactor systems
- Mining operations for conveyor belts and ventilation fans
- Pharmaceutical facilities for solvent extraction areas
- Wastewater treatment plants for aeration and pumping stations
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Petece Enviro Engineers, Tamil Nadu
 Tamil Nadu, India
Electronics & Electrical•Trading Company•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
North America
Northern Europe
Mid East
Southern Europe
Eastern Europe
South Asia
Western Europe
Africa
Domestic
Flame Proof Explosion Proof Motors For Hazardous Environments
Flame proof explosion-proof motors for hazardous environments in oil, gas, chemical, and mining industries. Ensure safety, reliability, and compliance with international standards for high-risk operations.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Petece Enviro Engineers
 Tamil Nadu, India
Electronics & ElectricalTrading Company