IN
₹
Apparel & Fashion
Description
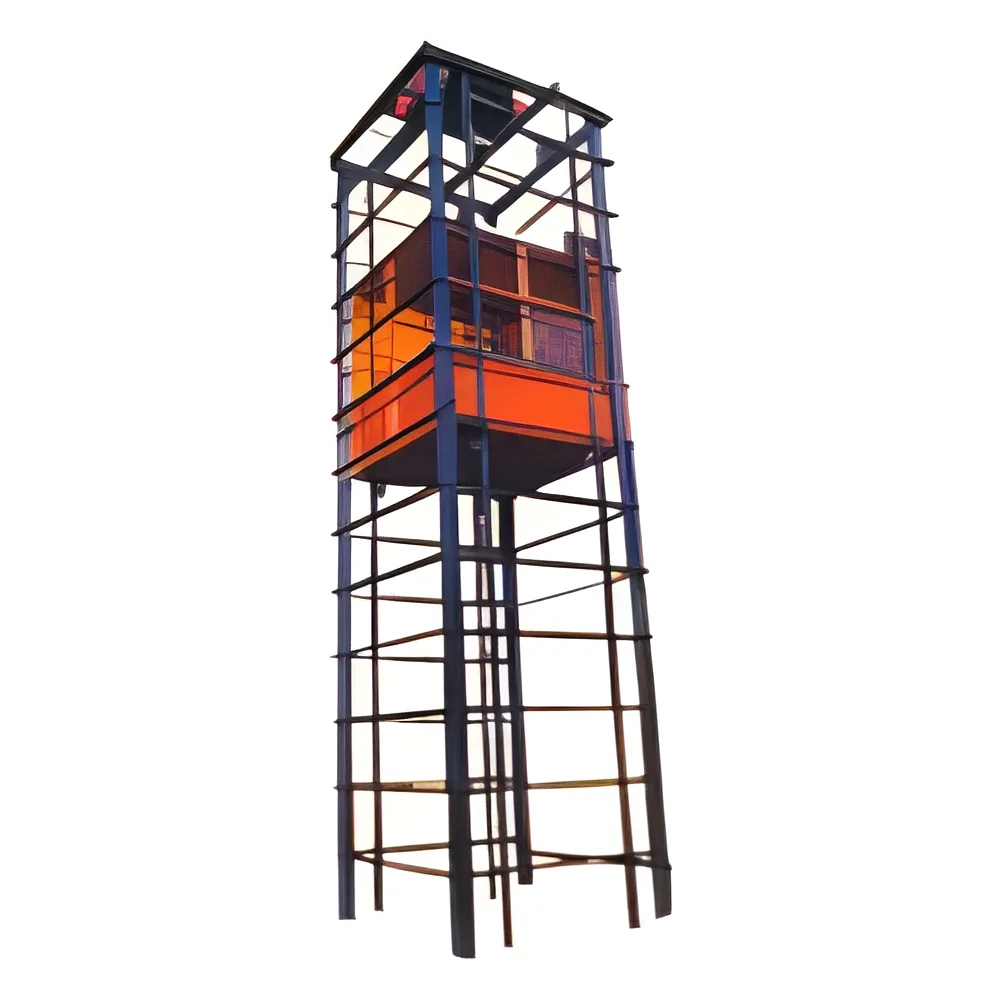
Our flame proof goods lifts are specifically engineered for hazardous environments where explosive atmospheres present constant operational risks. These specialized vertical transportation systems incorporate certified electrical components that prevent ignition of surrounding flammable gases, dust, or vapors, ensuring maximum safety in high-risk industrial operations. Manufactured to comply with stringent IS-2148 specifications, all electrical components carry certification from the Central Mining Research Station in Dhanbad, providing assurance that the equipment meets the highest safety standards for explosive environments. The robust construction focuses on durability and reliability, with attention to every detail that ensures safe operation in volatile conditions.

These flame proof goods lifts serve critical roles across multiple high-risk industries where standard material handling equipment would pose significant safety hazards. In mining operations, they safely transport mate...
Our flame proof goods lifts are specifically engineered for hazardous environments where explosive atmospheres present constant operational risks. These specialized vertical transportation systems incorporate certified electrical components that prevent ignition of surrounding flammable gases, dust, or vapors, ensuring maximum safety in high-risk industrial operations. Manufactured to comply with stringent IS-2148 specifications, all electrical components carry certification from the Central Mining Research Station in Dhanbad, providing assurance that the equipment meets the highest safety standards for explosive environments. The robust construction focuses on durability and reliability, with attention to every detail that ensures safe operation in volatile conditions.

These flame proof goods lifts serve critical roles across multiple high-risk industries where standard material handling equipment would pose significant safety hazards. In mining operations, they safely transport materials through underground tunnels and shafts where methane gas and combustible dust are present. Chemical and pharmaceutical manufacturers rely on them for moving raw materials and finished products through processing areas with volatile vapors. Oil refineries and petrochemical plants utilize these lifts in zones classified for explosive atmospheres, where even a small spark could cause catastrophic incidents. The equipment also proves essential in food processing facilities handling combustible dust and industrial plants with solvent vapors.

The business value of these flame proof goods lifts lies in their ability to maintain operations while ensuring regulatory compliance and worker safety in hazardous environments. They provide reliable performance that reduces downtime and maintenance costs while preventing potentially devastating ignition incidents that could result in facility damage, production halts, or worse. The certification from recognized authorities like the Central Mining Research Station offers peace of mind to facility managers and safety officers, knowing the equipment meets stringent safety standards. This specialized equipment represents a necessary investment for any operation working in classified hazardous areas, providing both operational continuity and comprehensive safety assurance.

Key Features:
- Flame proof electrical components certified for hazardous area operations
- Full compliance with IS-2148 safety standards and specifications
- Central Mining Research Station, Dhanbad certification for explosive atmospheres
- Robust industrial construction for demanding environments and heavy usage
- Engineered for safe operation with flammable gases, vapors, and combustible dust

Benefits:
- Prevents ignition risks in explosive environments for maximum safety
- Ensures regulatory compliance with industry safety standards
- Reduces operational downtime through reliable performance
- Protects personnel and facilities from potential catastrophic incidents
- Maintains productivity in hazardous areas where standard equipment cannot operate
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our IS-2148 certified flame proof goods lifts are engineered for safe vertical transportation where flammable gases, vapors, or combustible dust create explosive atmospheres. These specialized lifts prevent ignition risks through certified electrical components and robust construction, ensuring operational safety and regulatory compliance in high-risk industrial settings. They maintain productivity while eliminating hazards that standard equipment would create in dangerous working environments.
These reliable lifts serve critical material handling needs across multiple hazardous industries where safety cannot be compromised. Designed for consistent performance in challenging conditions, they protect both personnel and facilities from potential ignition incidents while ensuring smooth operations. The equipment meets stringent safety standards for explosive environments, providing peace of mind for facility managers and safety officers responsible for high-risk areas.
- Underground mining operations and tunnel construction sites with methane gas
- Chemical processing plants and pharmaceutical manufacturing facilities with volatile vapors
- Oil refineries, petrochemical complexes, and fuel storage terminals
- Grain silos, flour mills, and food processing plants with combustible dust
- Paint manufacturing facilities and solvent processing areas with flammable atmospheres
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Cranoist Engineers, Gujarat
 Gujarat, India
Industrial Equipment & Machinery•Manufacturer•Distributor / Wholesaler•Importer / Exporter
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Flame Proof Goods Lift For Explosive Environments IS 2148 Certified
IS-2148 certified flame proof goods lift for explosive environments, ideal for mining, chemical, and oil industries. Dhanbad certified for safe hazardous material handling in volatile atmospheres.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Cranoist Engineers
 Gujarat, India
Industrial Equipment & MachineryManufacturer