IN
₹
Apparel & Fashion
Description
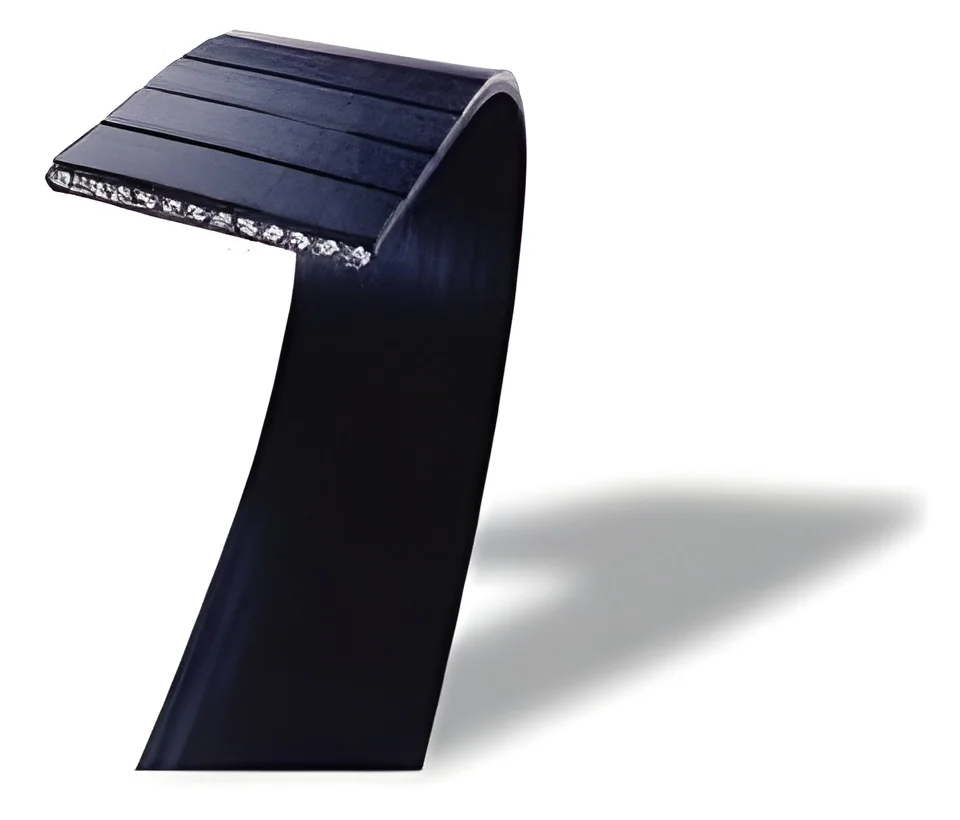
Our industrial heavy duty elevator belts with bucket represent advanced vertical material handling technology engineered for high-capacity industrial applications. These belts feature robust steel cable reinforcement that provides exceptional tensile strength and durability, ensuring reliable performance even under the most demanding conditions. The specialized design incorporates temperature-resistant rubber compounds that maintain structural integrity when conveying hot materials, while the integrated bucket system ensures efficient vertical transport without spillage or operational interruptions. These elevator belts are built to withstand continuous operation in challenging environments, making them the preferred choice for industries requiring consistent and dependable material handling solutions with minimal downtime.

These industrial elevator belts serve critical functions across multiple sectors including construction, mining, agriculture, and manufacturing. In construction an...
Our industrial heavy duty elevator belts with bucket represent advanced vertical material handling technology engineered for high-capacity industrial applications. These belts feature robust steel cable reinforcement that provides exceptional tensile strength and durability, ensuring reliable performance even under the most demanding conditions. The specialized design incorporates temperature-resistant rubber compounds that maintain structural integrity when conveying hot materials, while the integrated bucket system ensures efficient vertical transport without spillage or operational interruptions. These elevator belts are built to withstand continuous operation in challenging environments, making them the preferred choice for industries requiring consistent and dependable material handling solutions with minimal downtime.

These industrial elevator belts serve critical functions across multiple sectors including construction, mining, agriculture, and manufacturing. In construction and cement industries, they facilitate vertical transport of bulk materials to significant heights with precision and reliability. Mining operations utilize these belts for efficient ore and mineral handling, while agricultural facilities depend on them for grain and feed transportation. Chemical and fertilizer plants benefit from their resistance to various materials and temperatures. The versatility and robustness of these belts make them indispensable for any operation requiring vertical bulk material movement with consistent performance and maximum efficiency.

Businesses investing in our elevator belts gain significant operational advantages through enhanced reliability and reduced maintenance requirements. The steel cable reinforcement ensures extended service life even under heavy loads, while the temperature-resistant materials prevent degradation in high-heat environments. These features translate to lower total cost of ownership and improved operational continuity. The combination of durability, performance, and engineering excellence provides exceptional value for serious buyers seeking long-term material handling solutions that deliver consistent results and minimize operational disruptions.

Key Features:
- Steel cable reinforced construction for maximum strength and durability
- High-temperature resistant rubber materials for hot material handling
- Integrated bucket design for efficient vertical material transport
- Engineered for greater height applications and heavy-load capacity
- Robust construction suitable for continuous industrial operation

Benefits:
- Extended service life with minimal maintenance requirements
- Reliable performance in high-temperature environments
- Efficient vertical transport with minimal material spillage
- Suitable for heavy-load applications across multiple industries
- Reduced operational downtime and lower total cost of ownership
Specifications
| Additional Information | |
|---|---|
| Country of Origin | India |
Application
Our industrial heavy duty elevator belts with bucket are engineered for demanding vertical conveying applications across multiple industries. They ensure efficient and continuous material handling in challenging environments with high loads and elevated temperatures, providing reliable performance where standard belts fail. These industrial-grade belts are specifically designed for operations requiring consistent vertical transport of bulk materials. They maintain structural integrity under extreme conditions while delivering dependable performance that meets rigorous industry standards and operational requirements.
Real-world applications:
- Vertical transport of cement and construction materials in building projects
- Grain and agricultural product handling in silos and storage facilities
- Mining and mineral processing operations for ore transportation
- Fertilizer and chemical manufacturing plants for bulk material handling
- Power plants and industrial facilities for coal and ash conveyance
Trade Details
| Available Stock | In Stock |
| Sample Availability | No |
Payment Terms
| Payment Terms |
|
Company Profile
Vijay Enterprise, Gujarat
 Gujarat, India
Construction•Manufacturer
Factory Details
Factory SizeBelow 1000 sqm
Annual Production Capacity0
Main Markets
South Asia
Industrial Heavy Duty Elevator Belts With Bucket Steel Cable Reinforcement
Industrial heavy duty elevator belts with bucket feature steel cable reinforcement for reliable vertical material transport in construction, mining, and agriculture sectors with high-temperature resistance and superior durability.
Min. Order Quantity: 1 unit
Shipping
Shipping fee and delivery date to be negotiated. Contact supplier now for more details.
Vijay Enterprise
 Gujarat, India
ConstructionManufacturer